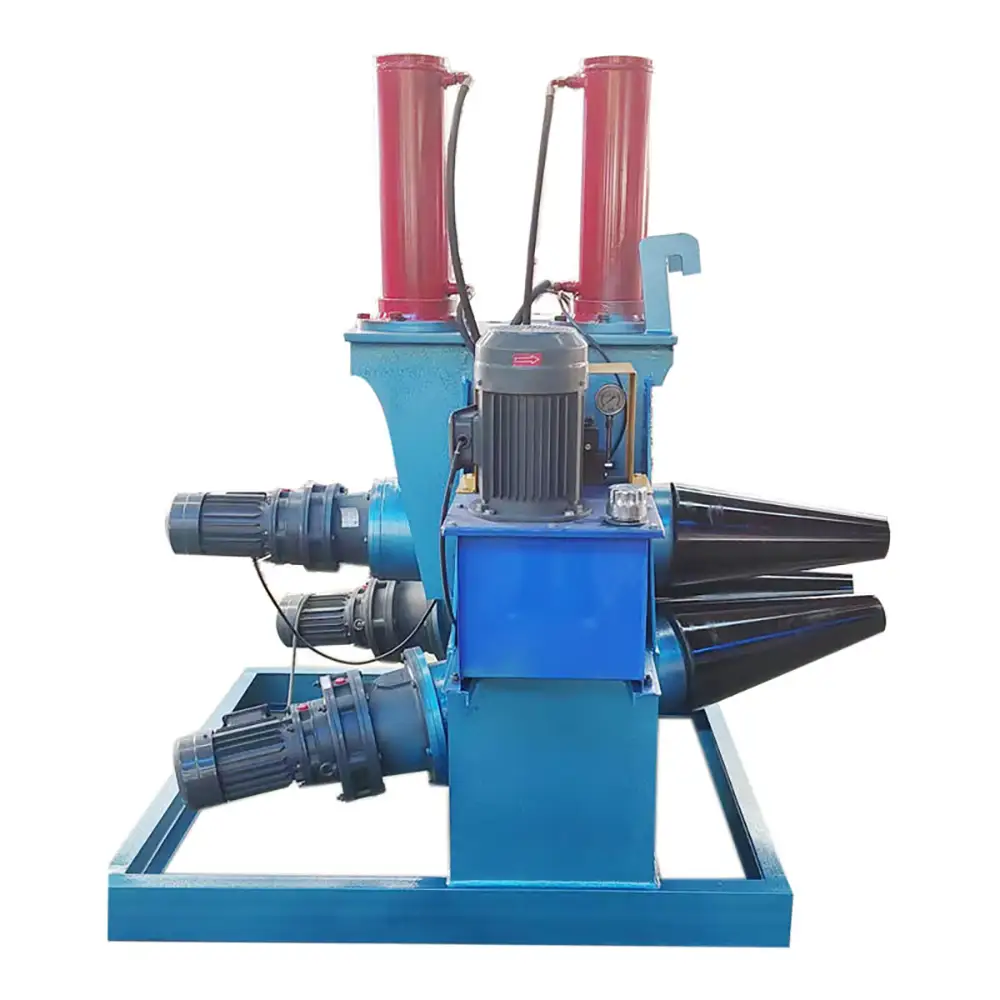
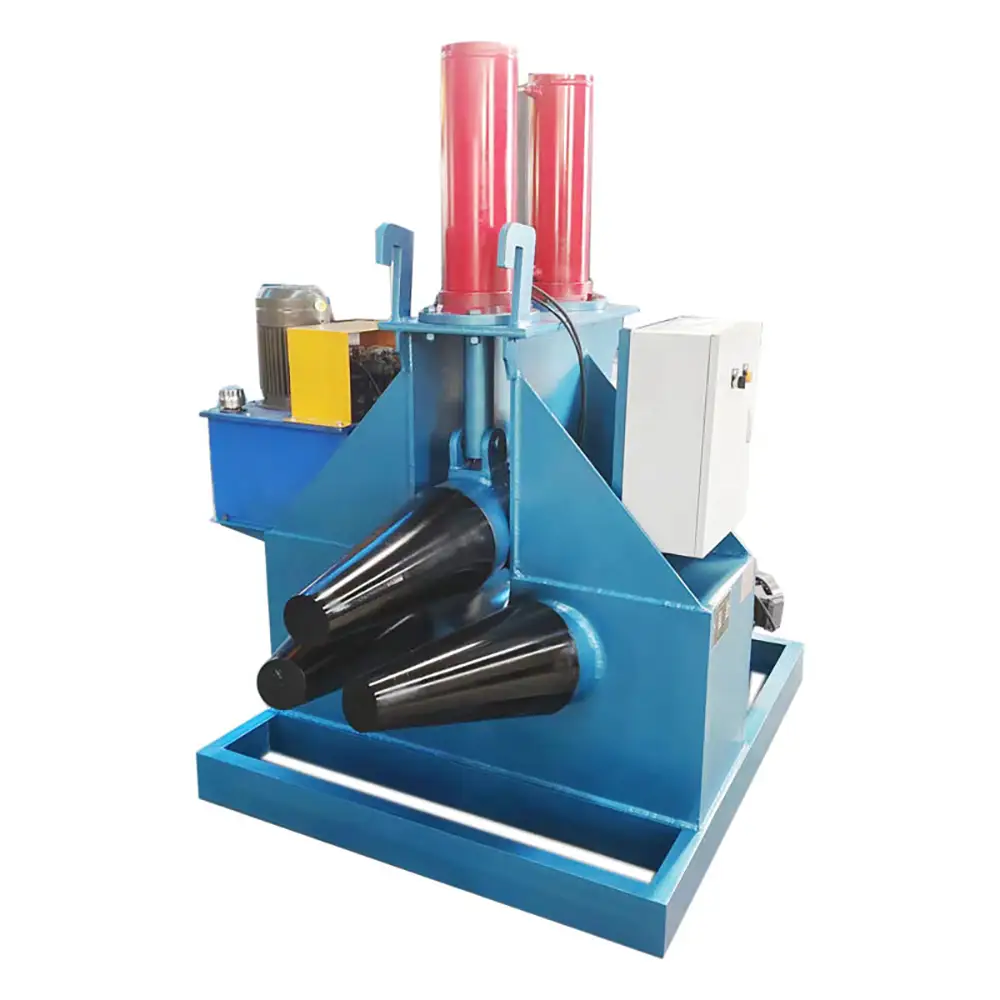
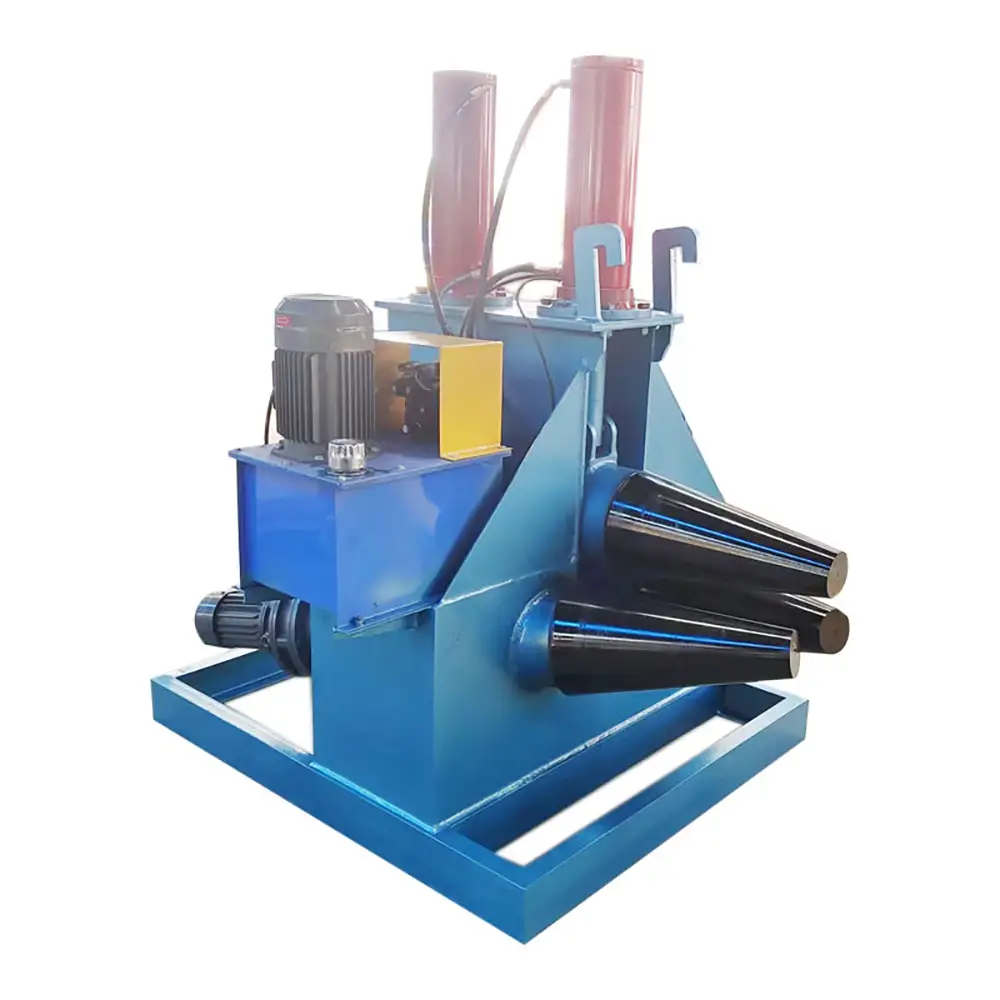
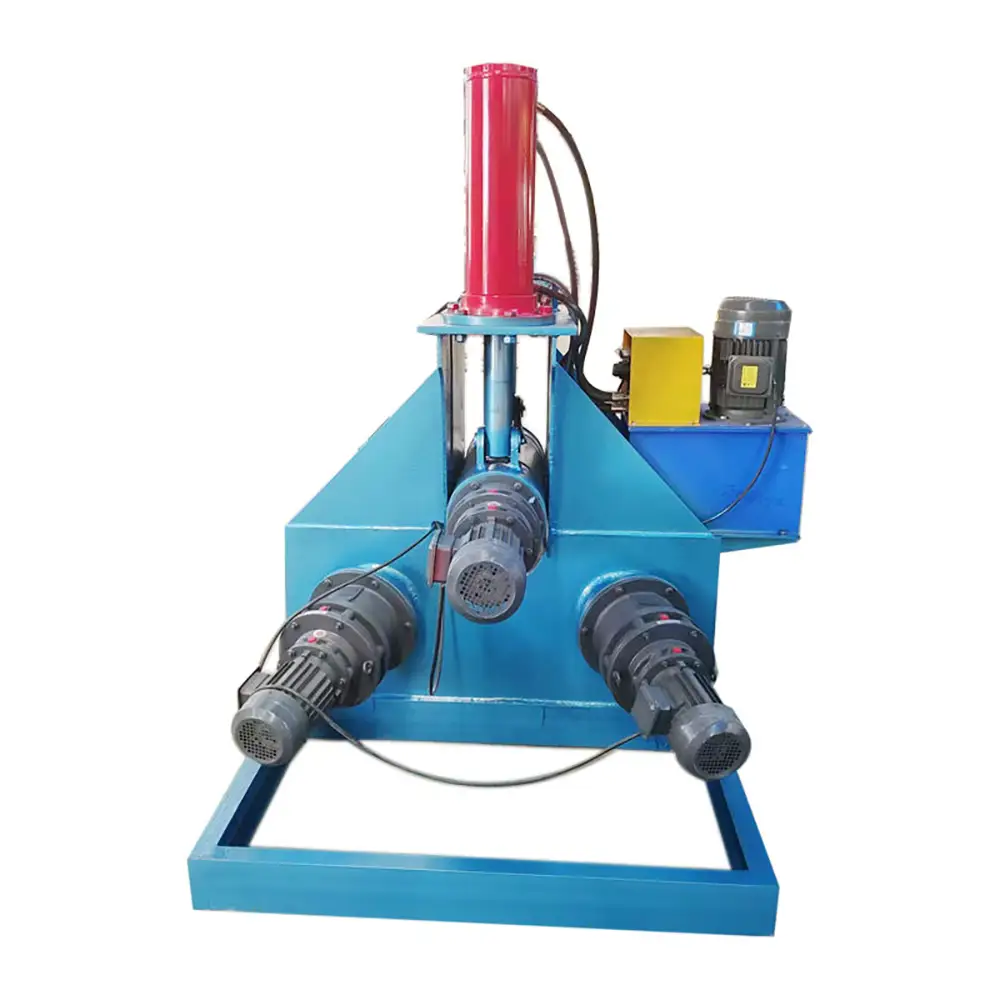
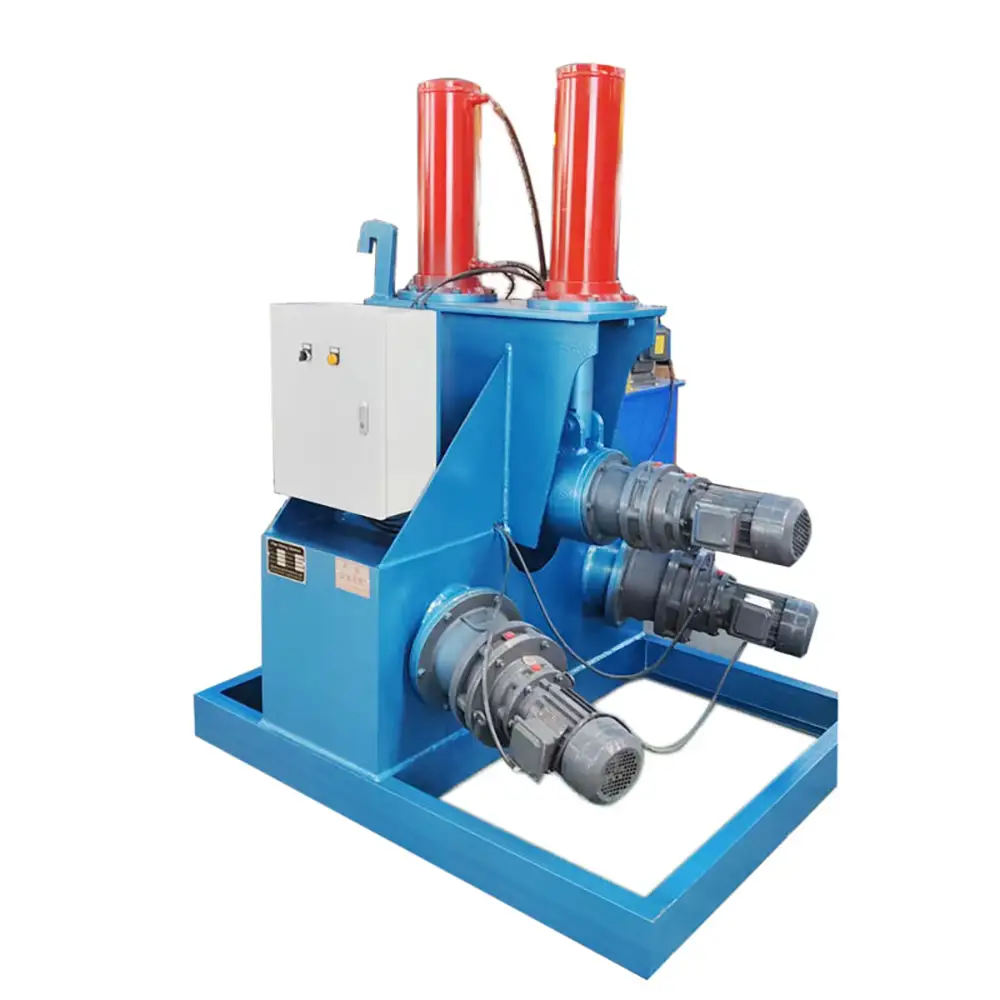
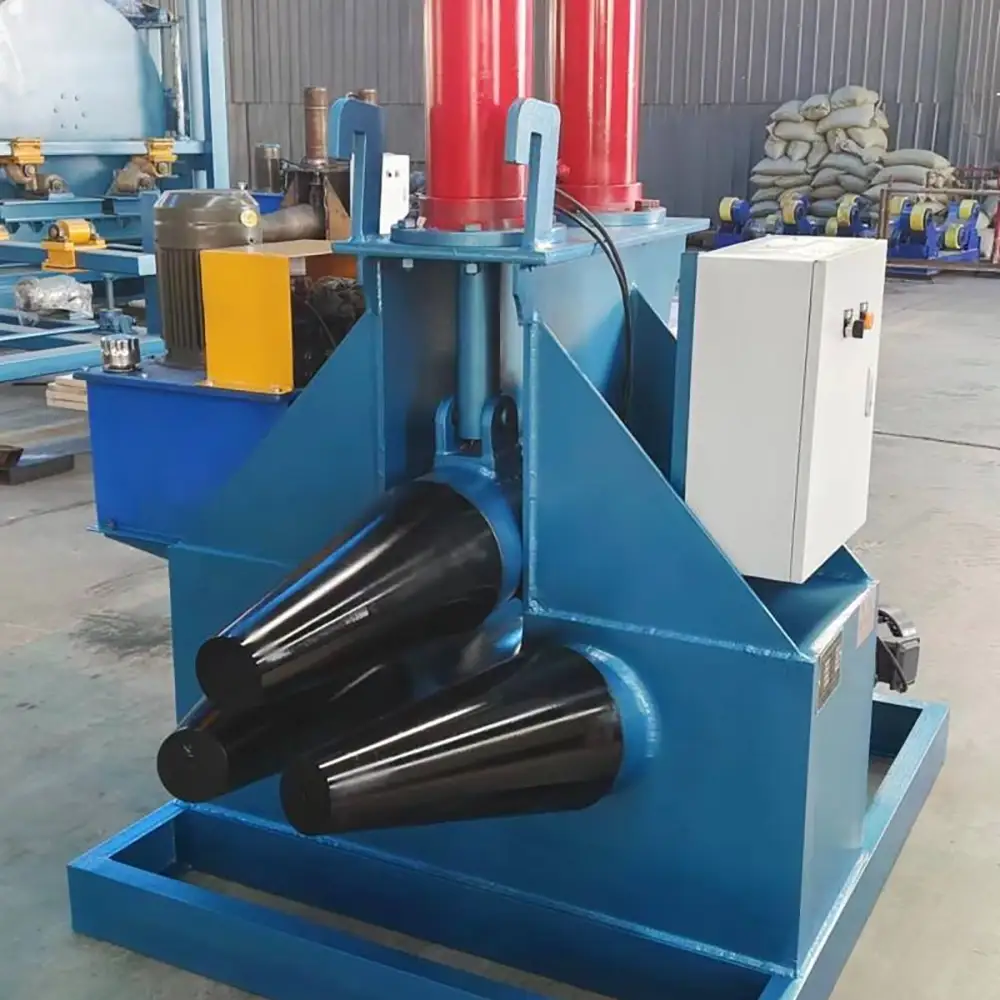
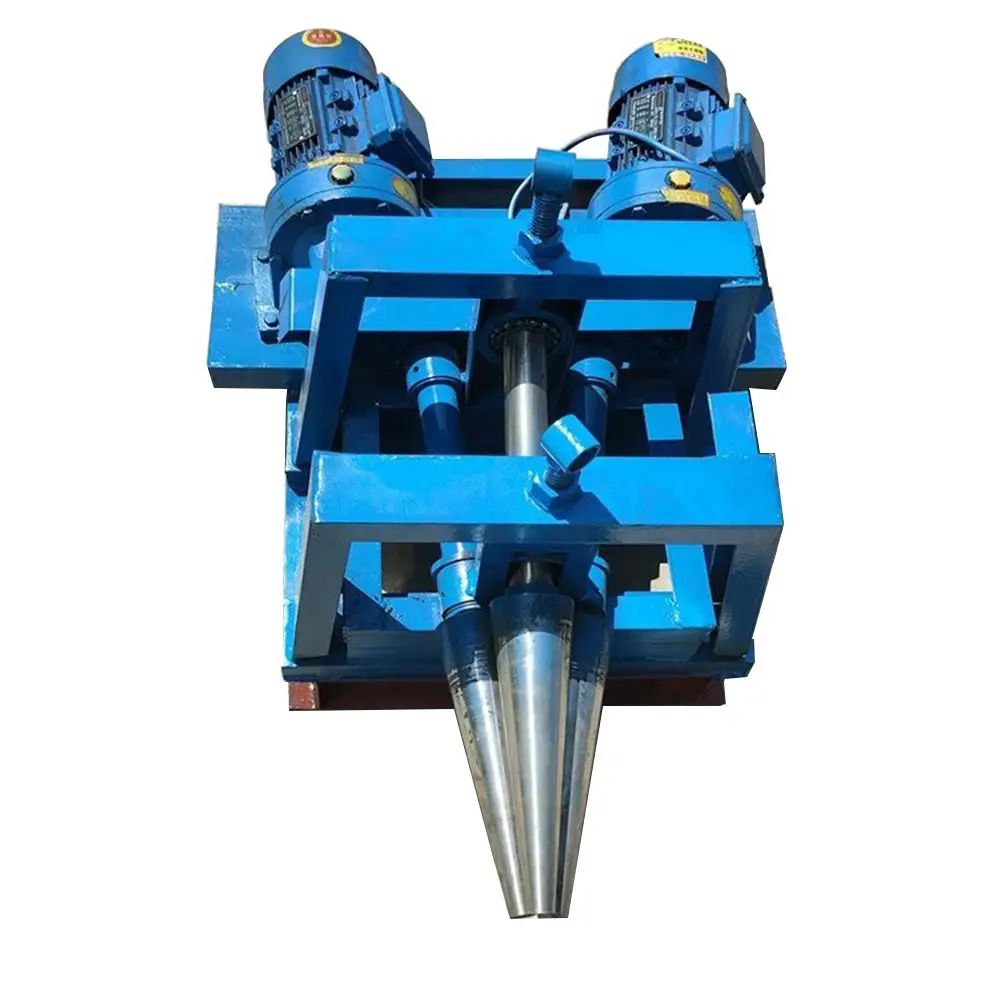
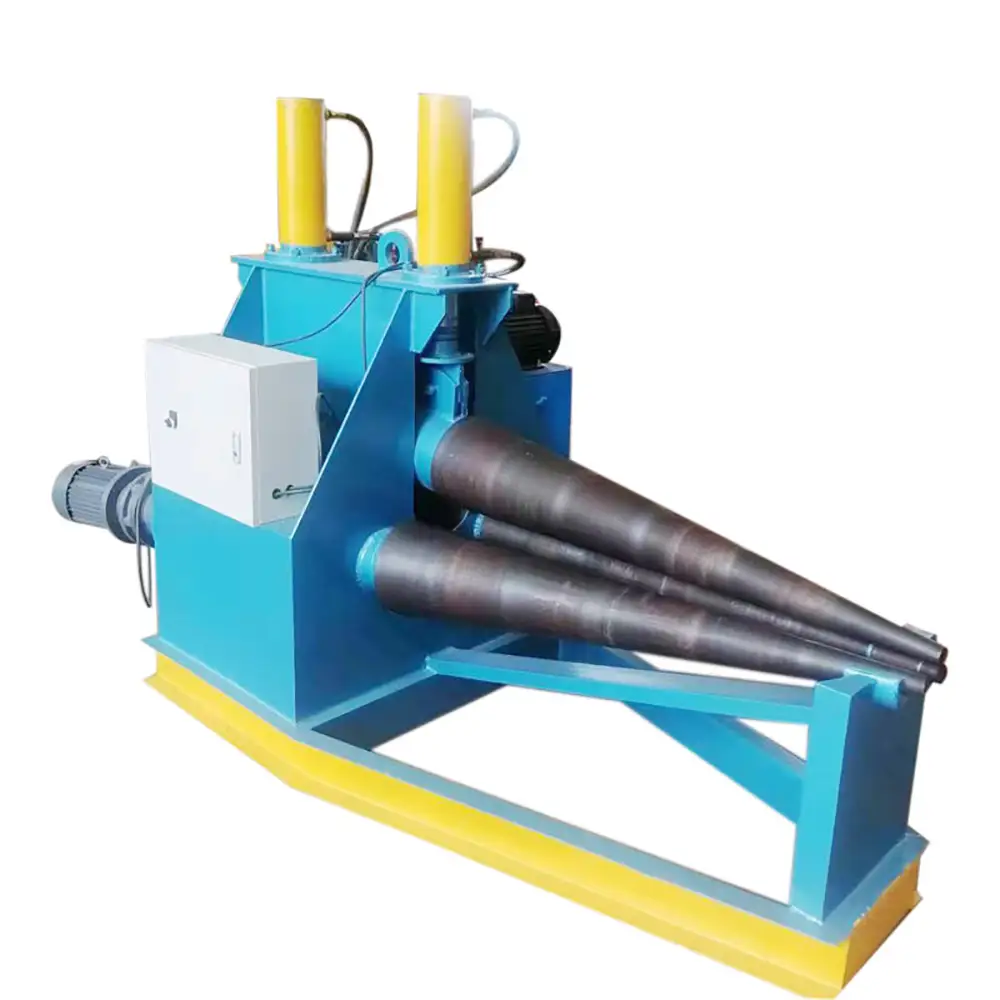
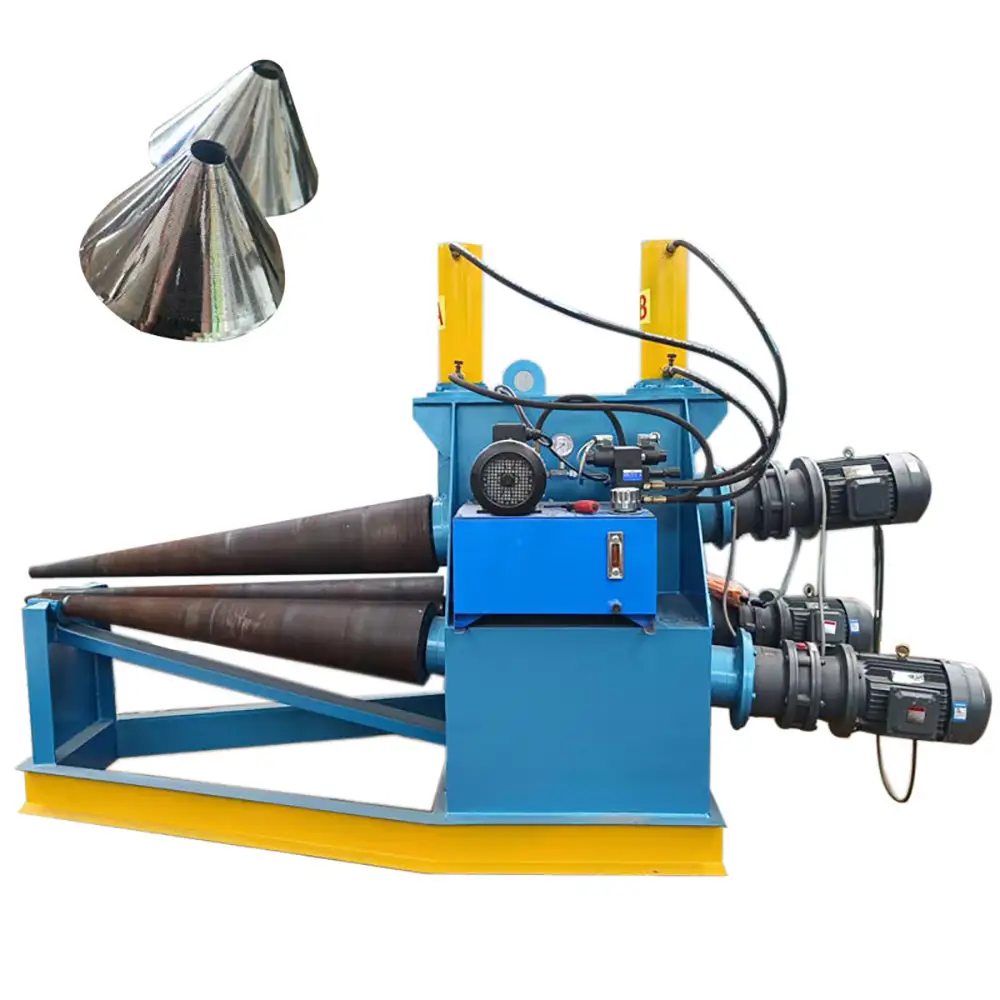
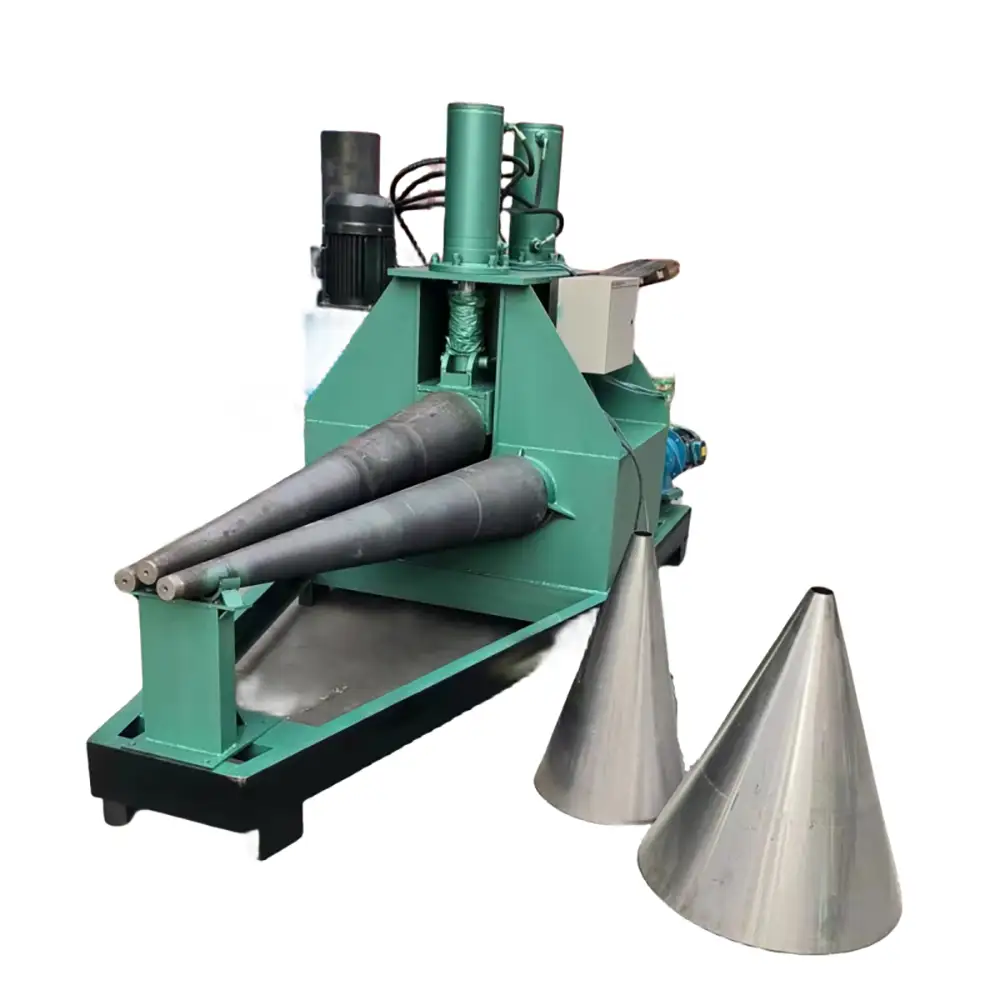
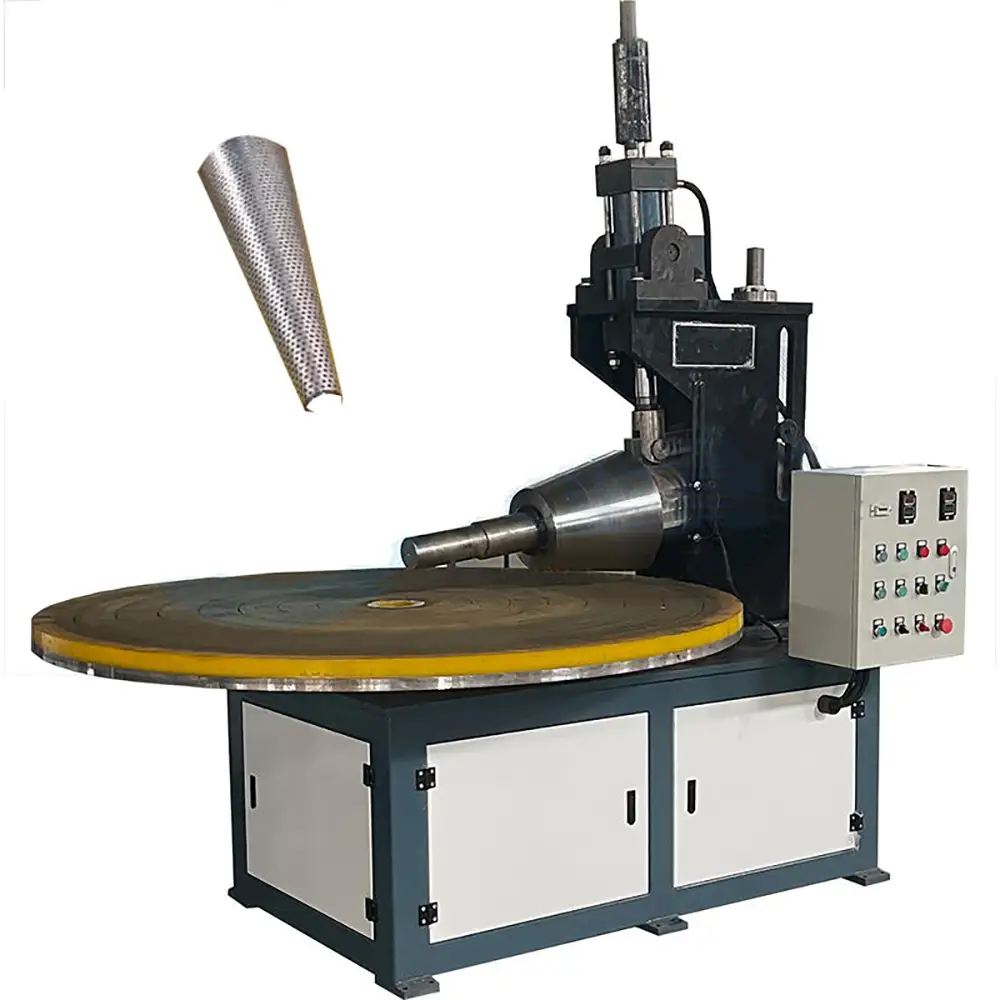
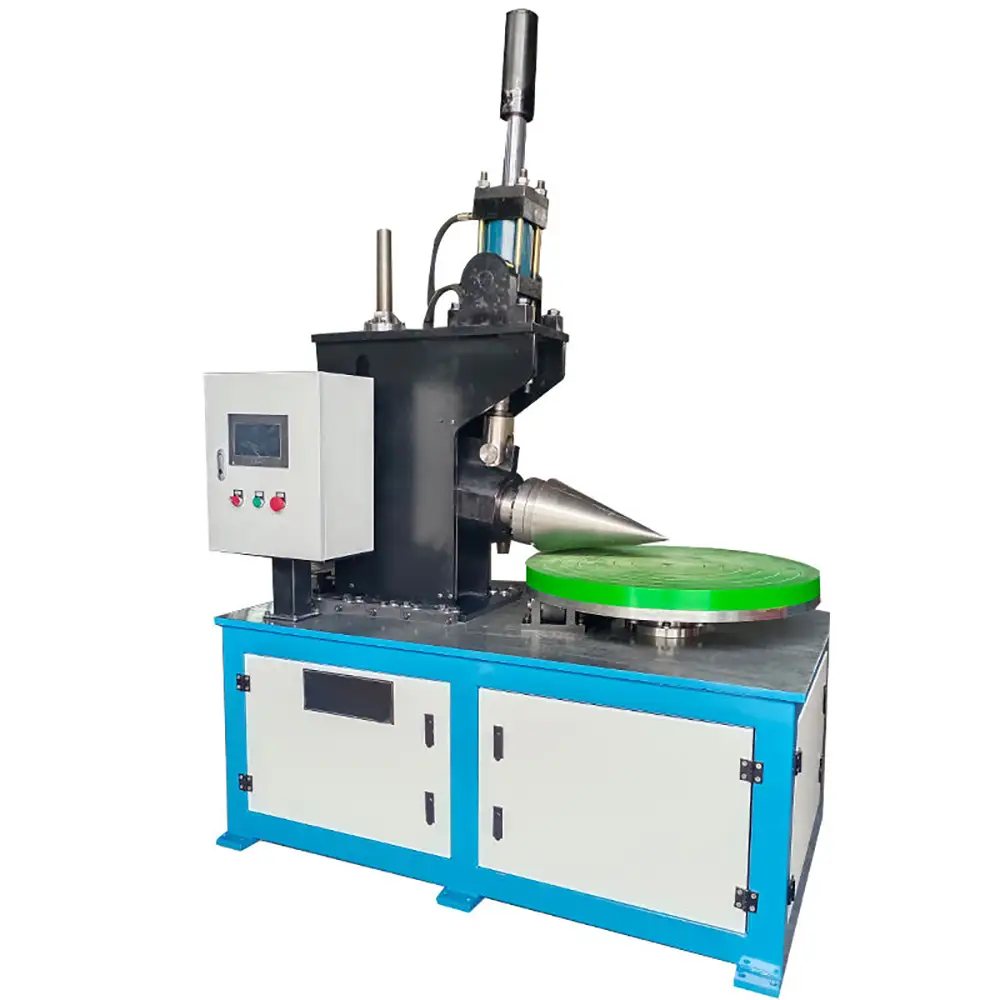
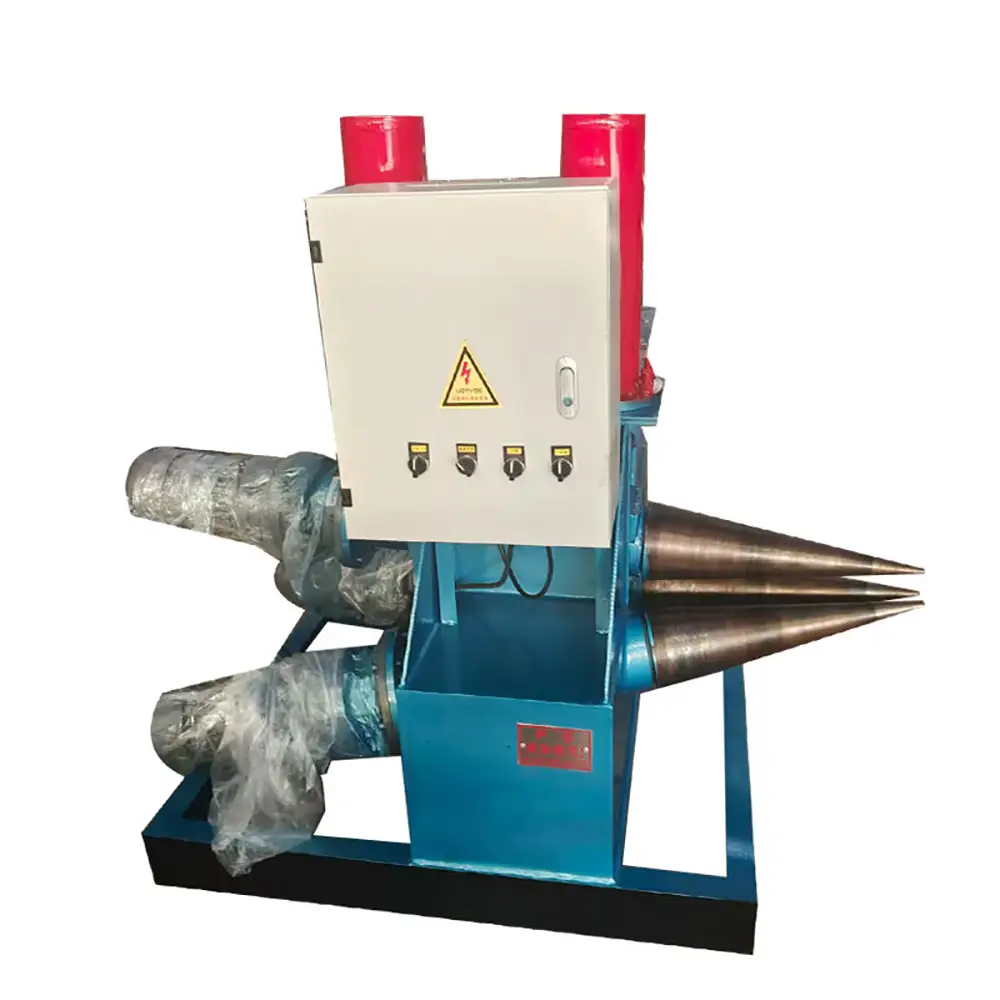
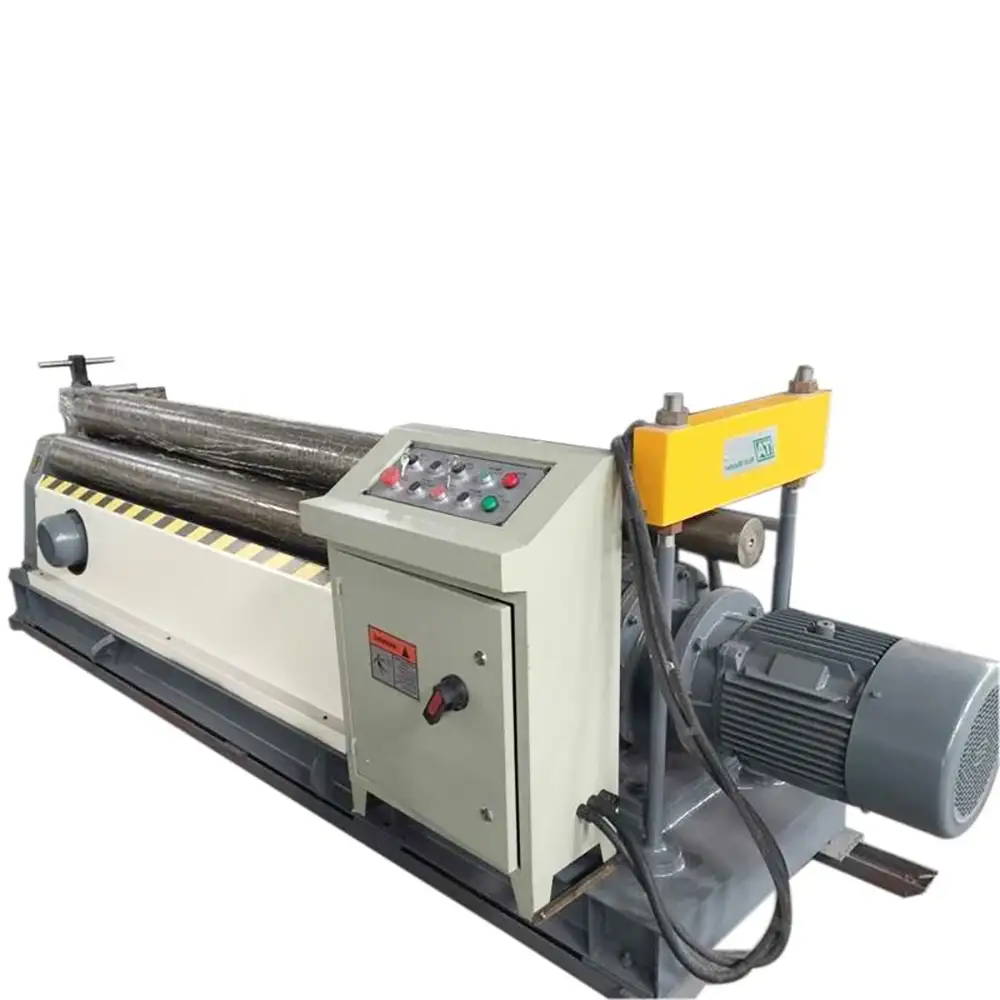
The plate rolling machine is a hydraulic three-roller cone plate rolling machine. The upper roller moves up and down at the symmetrical position in the center of the two bottom rollers, and adjustment power is obtained through hydraulic cylinder, and front and rear parts can be adjusted freely to make cones of different sizes. The bottom tapered rollers are respectively driven by a motor reducer (or driven by tow motors) to provide power for the sheet metal to run. The machine is electric rolling and hydraulic pressing.
|
Model |
3*500 |
4*1000 |
|
Roller big head diameter |
170mm |
220mm |
|
Roller small head diameter |
20 |
52 |
|
Roller length |
500mm |
1000mm |
|
Motor power |
3*750W |
3*1000w |
|
Oil station power |
3kw |
3kw |
|
Cylinder diameter |
110mm |
140mm |
|
Processing range |
Processable plate thickness stainless steel 2mm, Q235 plate 3mm |
High-frequency quenching treatment of roller
Machinable plate thickness stainless steel 3mm, Q235 plate 4mm |
|
Size |
1900x1500x1520mm |
2600x1200x1500 |
|
weight |
800kg |
1300kg |
The Multifunction Cone Rolling Machine is designed for manufacturers that need flexible and reliable equipment for forming tapered,conical,and pre-rolled metal components. Combining hydraulic roller adjustment with a multifunctional forming structure,the machine can be used for different cone sizes,materials,and production requirements.
A Pre Rolled Cone Machine is commonly used to transform flat sheet metal or steel plate blanks into conical or tapered sections before subsequent welding,finishing,and assembly. Compared with standard cylindrical plate rolling equipment,cone rolling requires controlled forming because the inner and outer circumferences of the workpiece are different.
The hydraulic rolling system provides controlled roller positioning and supports progressive forming of the metal blank. Depending on the machine configuration,it can be used for carbon steel,stainless steel,aluminum,and other suitable materials.
Multifunction Roller Design
The multifunction roller configuration allows the machine to support a wider range of forming applications. Different roller positions and forming adjustments can be used according to the required cone diameter,cone angle,plate thickness,and material.
A properly configured roller system helps distribute forming force across the workpiece and allows the operator to gradually develop the required tapered shape. For heavier plates,hydraulic adjustment can make machine setup and roller positioning more convenient.
The exact forming capability depends on the machine model and actual production parameters. Important factors include:
Maximum plate thickness
Maximum plate width
Material yield strength
Maximum cone diameter
Minimum cone diameter
Cone angle
Roller diameter
Required forming radius
Production volume
For this reason,customers should provide detailed drawings and material specifications when selecting a machine.
Hydraulic Cone Rolling Machine
The Hydraulic Cone Rolling Machine uses hydraulic power to assist with roller movement and workpiece forming. Hydraulic adjustment is particularly useful for industrial applications involving heavier steel plate or repeated production of tapered components.
During operation,the plate is positioned between the rollers,and the roller arrangement is adjusted according to the desired cone geometry. The material is then progressively rolled through controlled passes.
Instead of attempting to create the finished cone in one aggressive pass,the operator can gradually increase the forming deformation. This approach can help control springback and reduce the risk of excessive deformation.
For stainless steel and high-strength materials,the required forming force can be considerably different from that of mild steel. Machine capacity should therefore be selected based on actual material properties rather than plate thickness alone.
Pre-Rolled Cone Forming
The term Pre Rolled Cone Machine refers to equipment used to prepare conical metal sections before later fabrication operations. A typical process begins with a flat blank cut to the required development shape.
The blank is positioned in the machine and may undergo initial pre-bending where required. The rollers then progressively form the blank into a tapered section.
After rolling,the workpiece may be tack welded or fully welded along the required seam. Additional operations can include trimming,edge preparation,grinding,calibration,and dimensional inspection.
This makes the machine suitable for manufacturers that produce components in multiple stages rather than requiring the entire finished product from the rolling operation.
Applications of Pre-Rolled Cone Machines
A hydraulic cone rolling machine can be used to manufacture many types of tapered components. Common applications include:
Pipe reducers
Conical hoppers
Industrial funnels
Dust collector cones
Duct transitions
Exhaust cones
Tank transitions
Vessel components
Conical roofs
Chemical equipment
Agricultural equipment
Mining equipment
HVAC components
Custom fabricated cones
For example,a pipe reducer has different diameters at its two ends. A properly prepared flat blank can be rolled into the required tapered geometry before the longitudinal seam is welded.
Hoppers and funnels can also be manufactured using the same forming principle. The larger upper opening gradually transitions into a smaller discharge opening,providing a practical solution for material handling systems.
Sheet Metal and Steel Plate Cone Rolling
The machine can be configured for both sheet metal and steel plate applications. Thin sheet metal is often used for HVAC,ducting,and light fabrication,while thicker steel plate may be required for tanks,industrial equipment,and heavy-duty structures.
Different materials require different forming conditions. Carbon steel is commonly used for general industrial fabrication,while stainless steel is preferred when corrosion resistance or hygienic surfaces are important.
Aluminum offers low weight but may require careful roller adjustment to reduce surface marking or unwanted deformation. The actual material range should always be confirmed against the selected machine configuration.
Tapered Cone Forming Process
The forming process normally begins with accurate blank preparation. The flat blank should be cut according to the developed cone dimensions and checked for dimensional accuracy.
The operator then positions the blank in the machine. Depending on the workpiece design,the leading and trailing edges may require pre-bending.
The hydraulic rollers are adjusted to create the required forming condition. The plate passes through the rollers progressively while the operator monitors the cone angle and diameter.
Several passes may be required depending on plate thickness,material strength,and cone geometry. Gradual forming can help achieve more consistent results than excessive deformation in a single pass.
Once the desired shape is achieved,the formed cone can be removed for welding and subsequent fabrication.
Multifunctional Industrial Metal Forming
One of the main benefits of a multifunctional cone rolling machine is its ability to support different component geometries. Instead of using separate equipment for every tapered product,the same machine may be configured for different cone diameters and forming requirements.
This flexibility can be valuable for job shops,custom fabricators,and industrial manufacturers producing multiple product sizes.
For B2B users,the machine can also be integrated into a broader fabrication workflow involving CNC cutting,plate preparation,welding,grinding,inspection,and final assembly.
Machine Selection
Choosing the correct cone rolling machine requires more than simply comparing nominal plate thickness. The actual cone geometry has a major influence on forming requirements.
Customers should provide the manufacturer with:
Material type and grade
Maximum plate thickness
Minimum plate thickness
Plate width
Maximum cone diameter
Minimum cone diameter
Cone height
Cone angle
Required forming radius
Production quantity
Component drawings
These details allow the manufacturer to evaluate the required roller configuration,hydraulic capacity,and machine structure.
Custom and OEM Cone Rolling Equipment
Different industries have different requirements for cone dimensions,material thickness,and automation. Therefore,customized machine configurations can be developed for specific production applications.
OEM solutions may include customized working dimensions,hydraulic systems,control options,roller arrangements,side supports,and auxiliary equipment.
For customers producing large volumes of the same component,a programmable or CNC-assisted configuration may provide more consistent setup and positioning. For lower-volume custom fabrication,a hydraulic manually operated system may provide the required flexibility.
Quality Control After Cone Rolling
Cone rolling is one stage of the overall fabrication process. After forming,the finished workpiece should be inspected according to the requirements of the final product.
Typical checks may include:
Large-end diameter
Small-end diameter
Cone angle
Overall height
Roundness
Edge alignment
Seam fit-up
Surface condition
Welding and subsequent finishing can also affect the final dimensions. Proper inspection throughout the manufacturing process helps maintain consistency between production batches.
Why Choose Us
Multifunctional Cone Rolling Solutions
Our machines are designed to support different tapered and conical forming applications.
Hydraulic Roller Adjustment
Hydraulic systems provide controlled roller positioning for efficient industrial forming.
Pre-Rolled Cone Applications
The equipment is suitable for preparing conical sections before welding and final fabrication.
Flexible Material Compatibility
Configurations can be selected for carbon steel,stainless steel,aluminum,and other suitable metals.
Custom Machine Configuration
Working dimensions,roller systems,hydraulic capacity,and control options can be customized.
OEM Manufacturing
We support customized equipment based on production drawings and specific forming requirements.
B2B Factory Supply
We provide machinery solutions for metal fabricators,industrial manufacturers,distributors,and equipment suppliers.
Technical Support
We can assist customers with machine selection,configuration,forming requirements,and production considerations.
FAQs
1. What is a Multifunction Cone Rolling Machine?
It is a metal forming machine designed to produce tapered and conical sections from sheet metal or steel plate while supporting different forming configurations.
2. What is a Pre Rolled Cone Machine used for?
It is used to form flat metal blanks into conical or tapered sections before welding,trimming,grinding,assembly,and other fabrication operations.
3. Can the machine roll steel plate?
Yes,depending on the machine model and capacity. The required thickness,plate width,material strength,and cone dimensions should be confirmed before selection.
4. Can it process stainless steel?
Yes. Stainless steel can be rolled when the machine has sufficient forming capacity for the specified grade and thickness.
5. Can this machine produce pipe reducers?
Yes. It can form tapered blanks used for pipe reducers. Welding and finishing are normally performed after the rolling stage.
6. What materials can be processed?
Typical materials include carbon steel,mild steel,stainless steel,and aluminum. Other materials can be evaluated according to their forming characteristics.
7. Is the machine hydraulic?
Yes,this product is designed around hydraulic roller adjustment. The exact hydraulic system and control method depend on the selected configuration.
8. Can one machine make different cone sizes?
Yes,within its specified operating range. Different cone diameters and angles may require different roller settings and forming procedures.
9. Is the machine fully automatic?
Automation depends on the configuration. Hydraulic assistance does not necessarily mean fully automatic operation. CNC or programmable control can be specified when required.
10. Can the machine be customized?
Yes. OEM and Custom configurations can be developed according to material,plate size,cone geometry,production volume,and automation requirements.
11. What information should I provide for a quotation?
Provide the material,maximum and minimum plate thickness,plate width,large and small cone diameters,cone angle,cone height,production quantity,and preferably a product drawing.
12. What happens after the cone is rolled?
The formed cone may require seam welding,trimming,edge preparation,grinding,calibration,and final inspection depending on the finished component requirements.
Prev:
Machine Rolling Cone Hydraulic 3 Roller Plate Bending Machine
Next:
Taper Cone Rolling Machine Sheet Metal Steel Plate Bending Roller Cone Hydraulic Rolling Machine
TAG:
Cone Forming Machine,
Steel Plate Rolling Machine,
Automatic Cone Rolling Machine,
Three Roller Cone Rolling Machine,
Industrial Cone Rolling Machine,
Industrial Cone Forming Machine,
Hopper Cone Forming Machine,
Metal Plate Bending Machine,
Hydraulic Plate Rolling Machine,
Stainless Steel Cone Rolling Machine,
Steel Cone Rolling Machine,
Carbon Steel Cone Rolling Machine,
Steel Cone Forming Machine,
Sheet Metal Cone Bending Machine,
Tapered Metal Forming Machine,
Cone Rolling Machine,
Conical Plate Bending Machine,
Metal Sheet Bending Machine,
CNC Cone Rolling Machine,
Metal Cone Rolling Machine,
Metal Cone Forming Machine,
Hydraulic Cone Rolling Machine,
Cone Bending Machine,
Hopper Cone Rolling Machine,
Sheet Metal Cone Forming Machine,
Reducer Cone Rolling Machine,
Conical Hopper Forming Machine,
Conical Plate Rolling Machine,
Taper Cone Rolling Machine,
Taper Cone Bending Machine,
Related Category:
Multifunction Cone Rolling Machine,Multifunction Roller Cone Machine,Hydraulic Cone Rolling Machine,Pre Rolled Cone Mach China, suppliers, manufacturers, factory, customized, wholesale, quotation, made in China