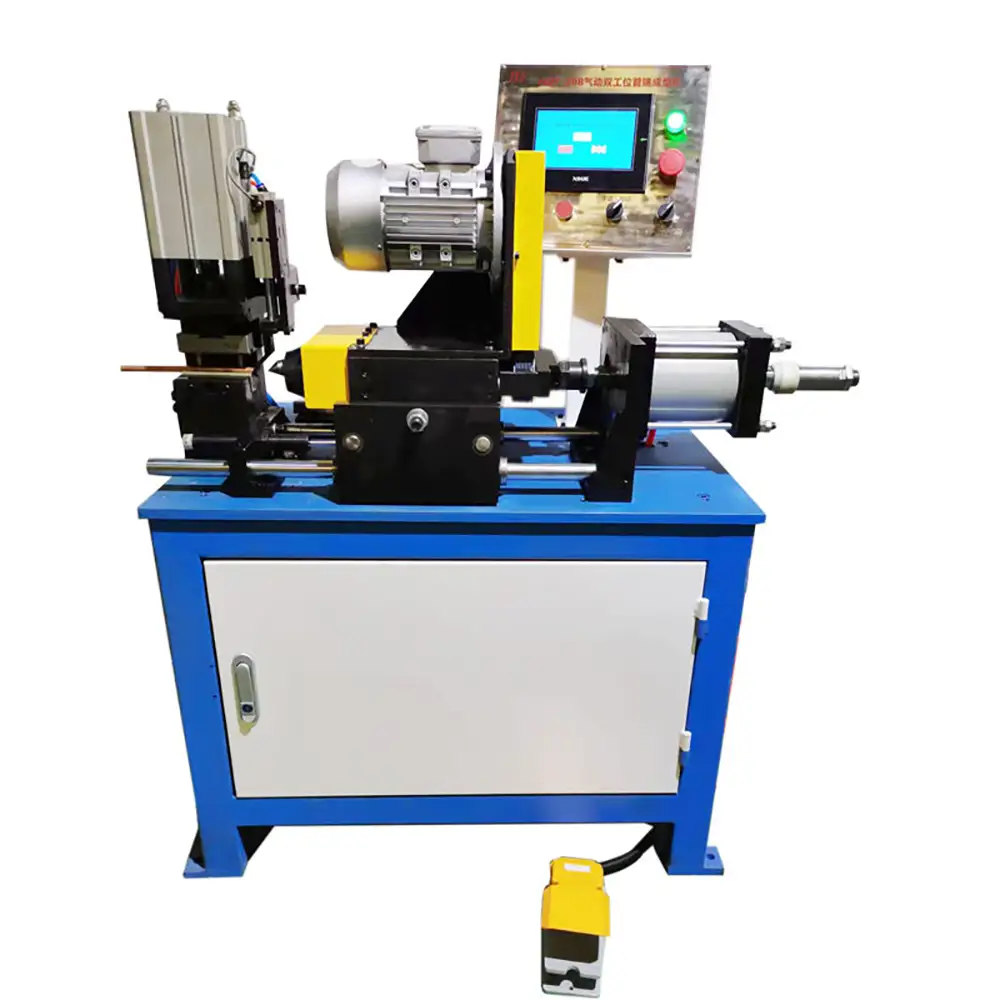
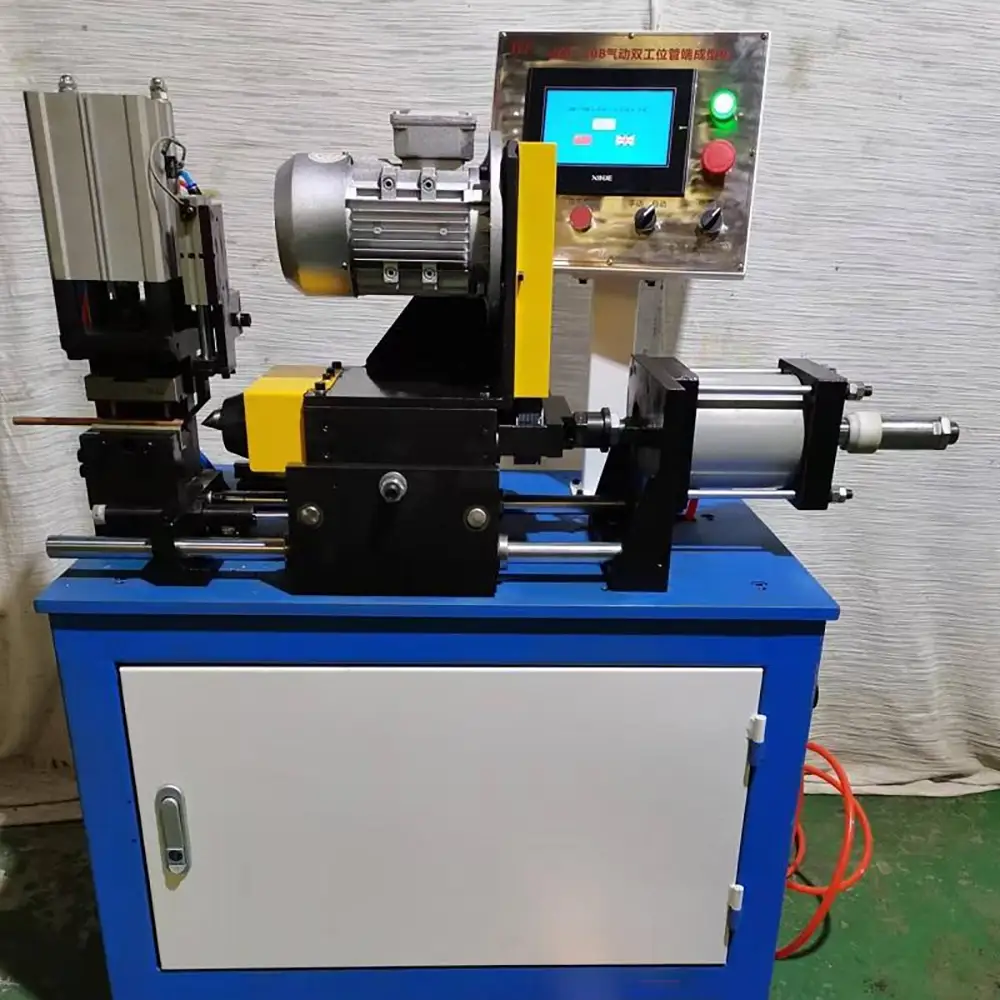
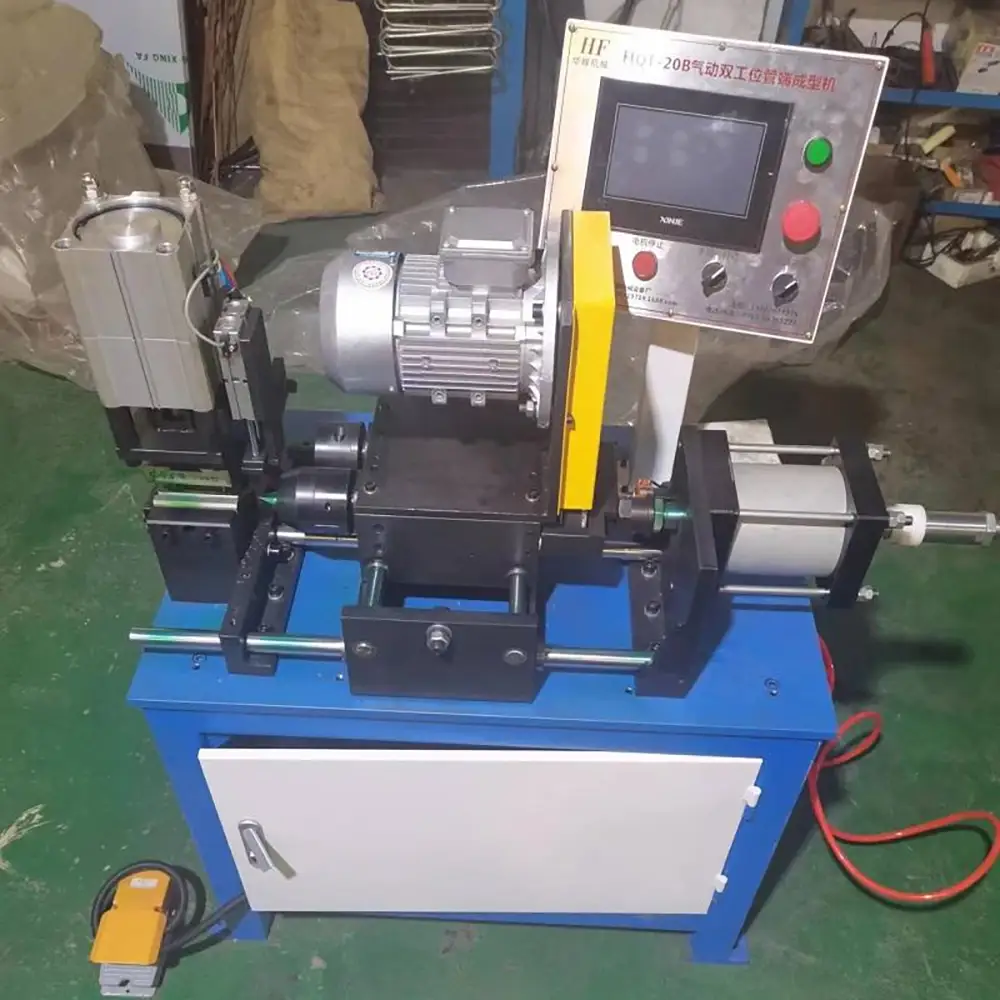
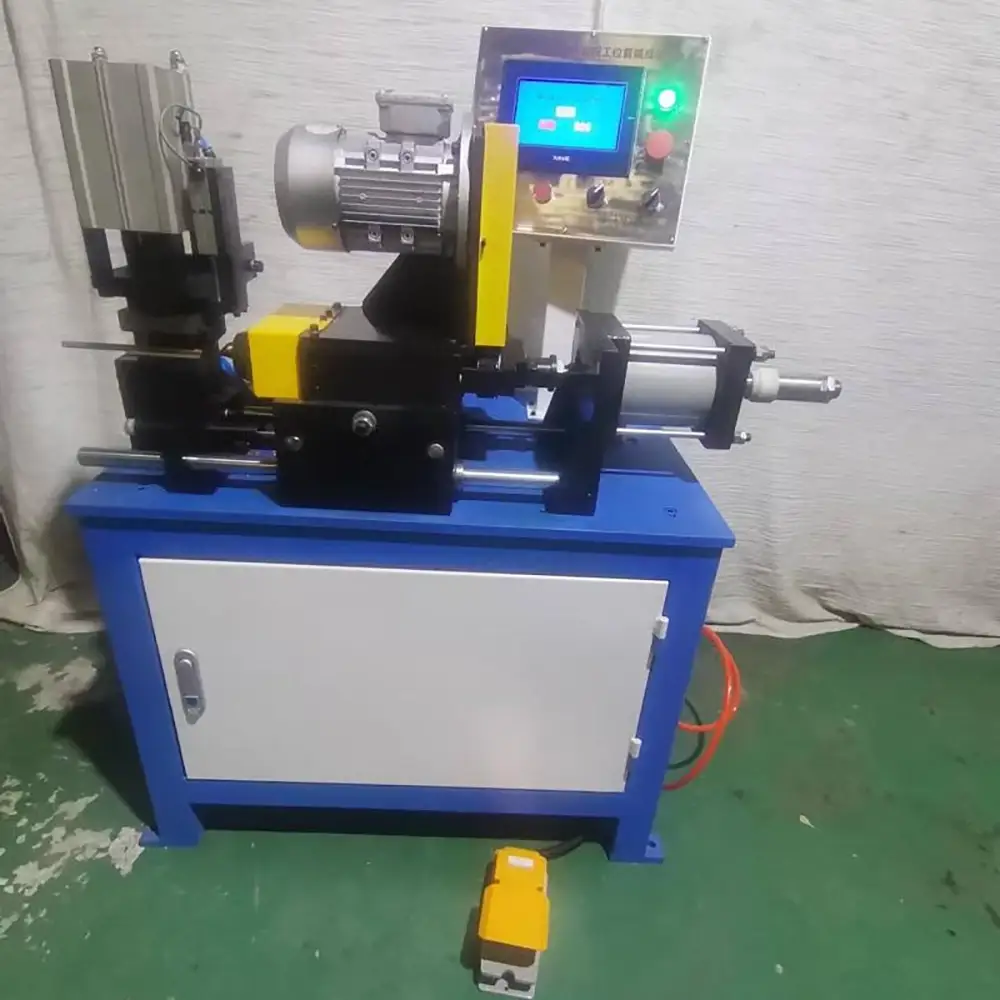
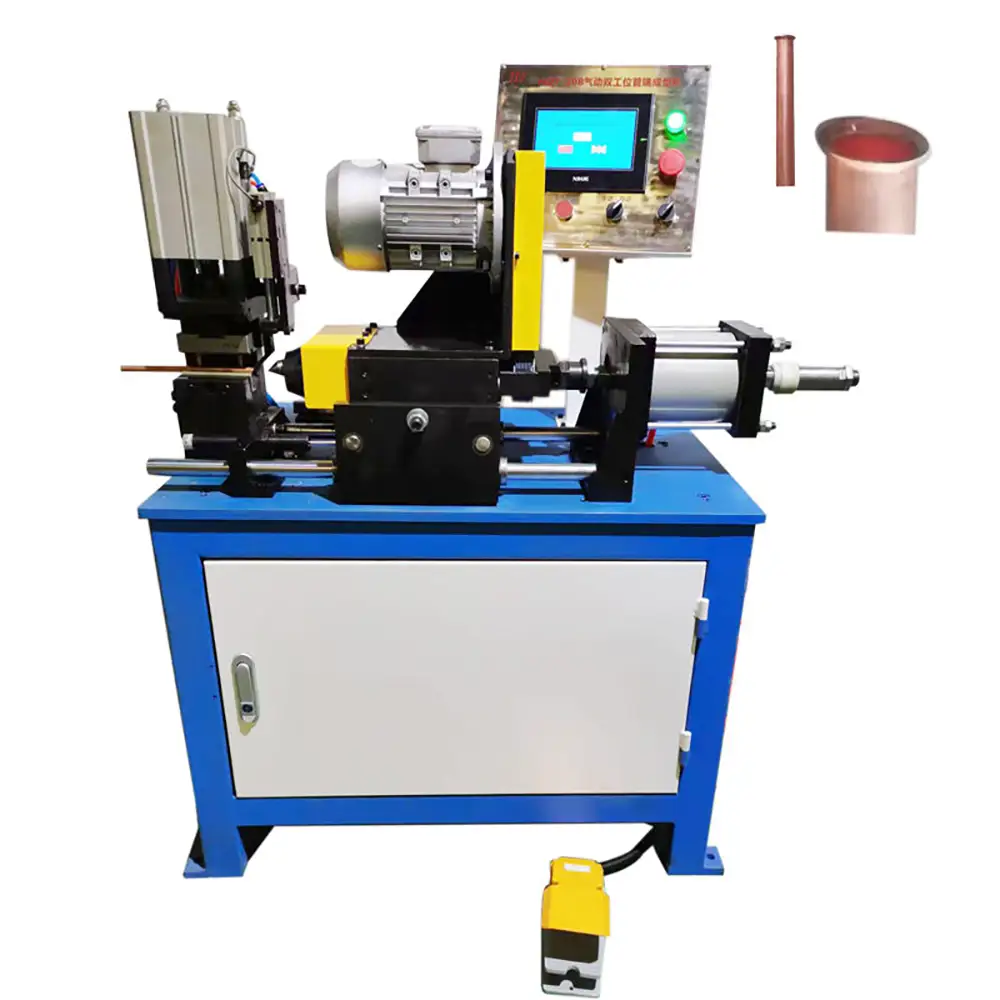
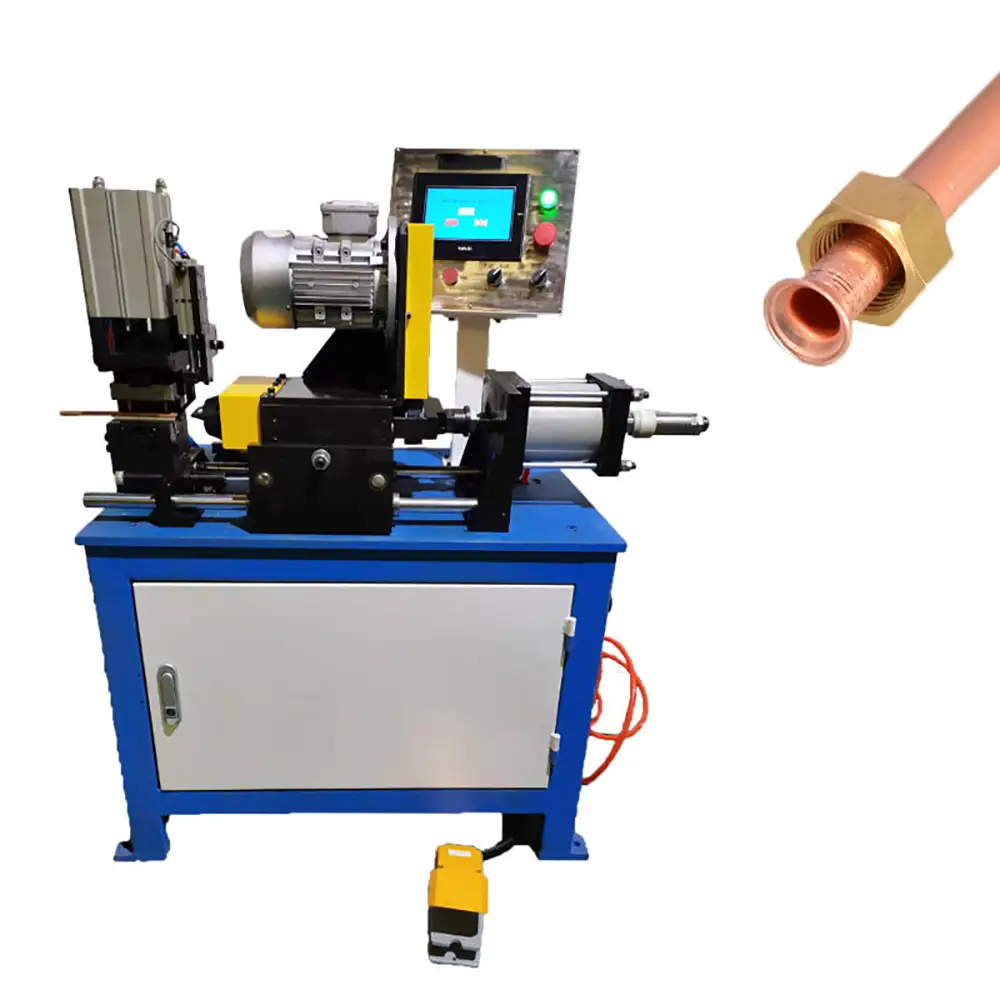
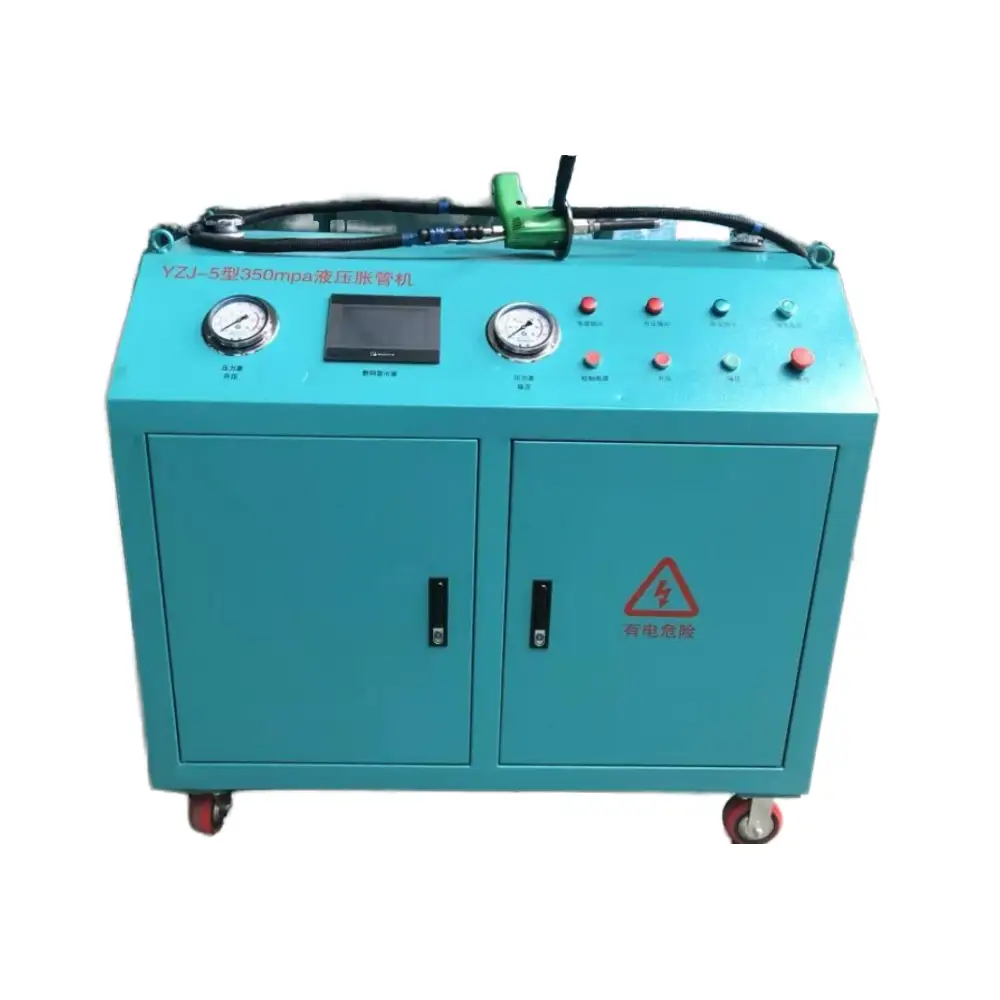
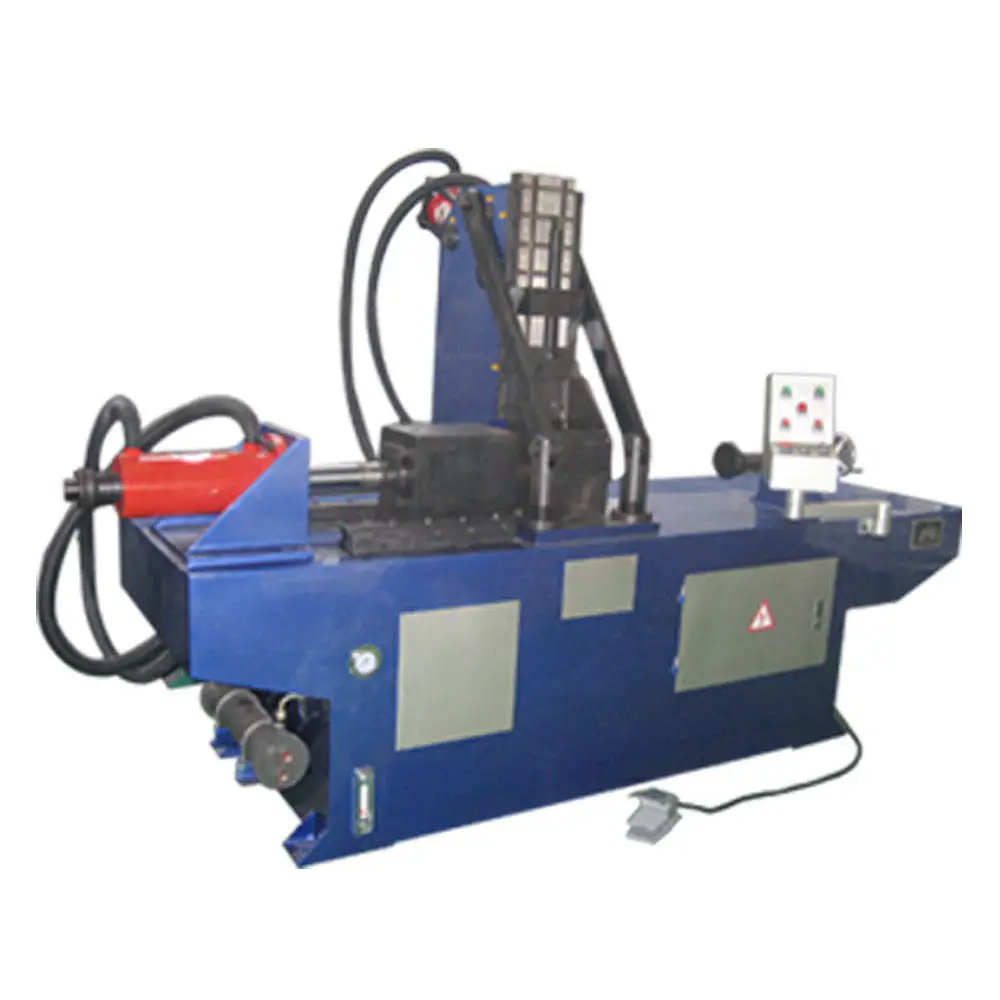
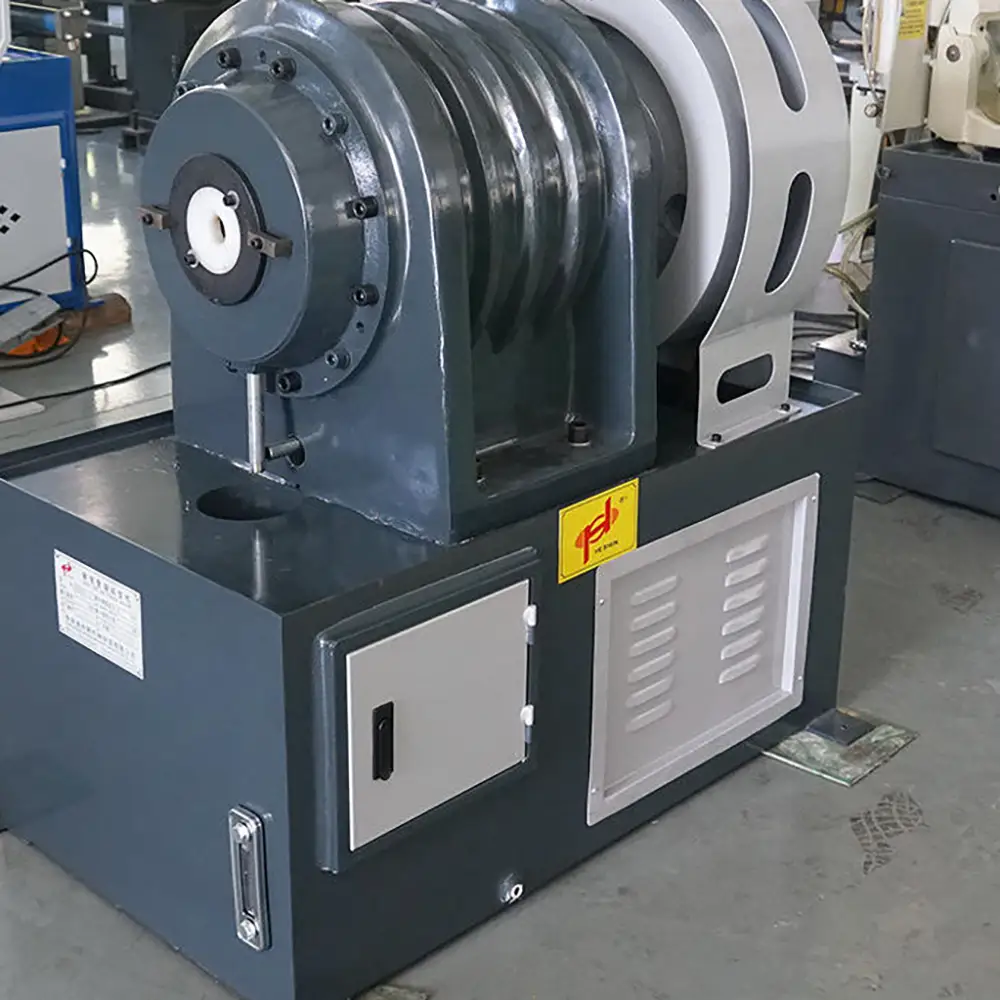
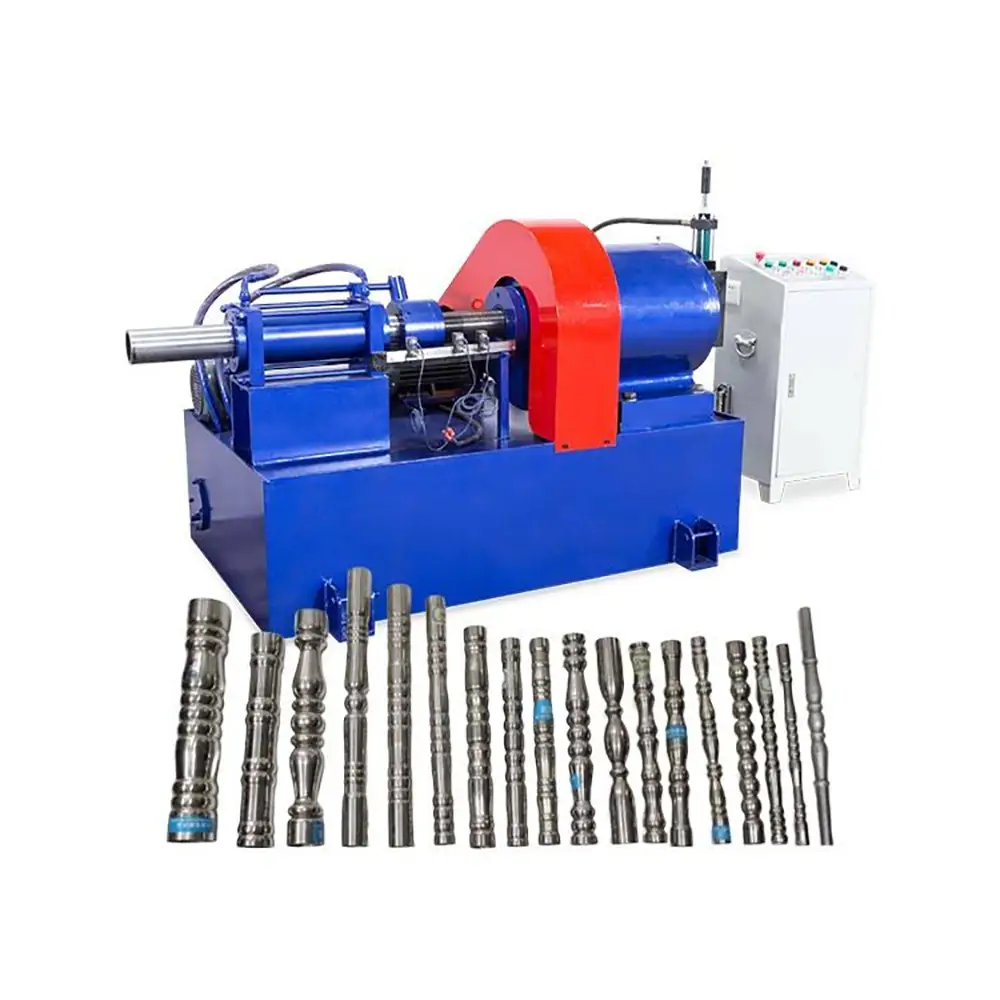
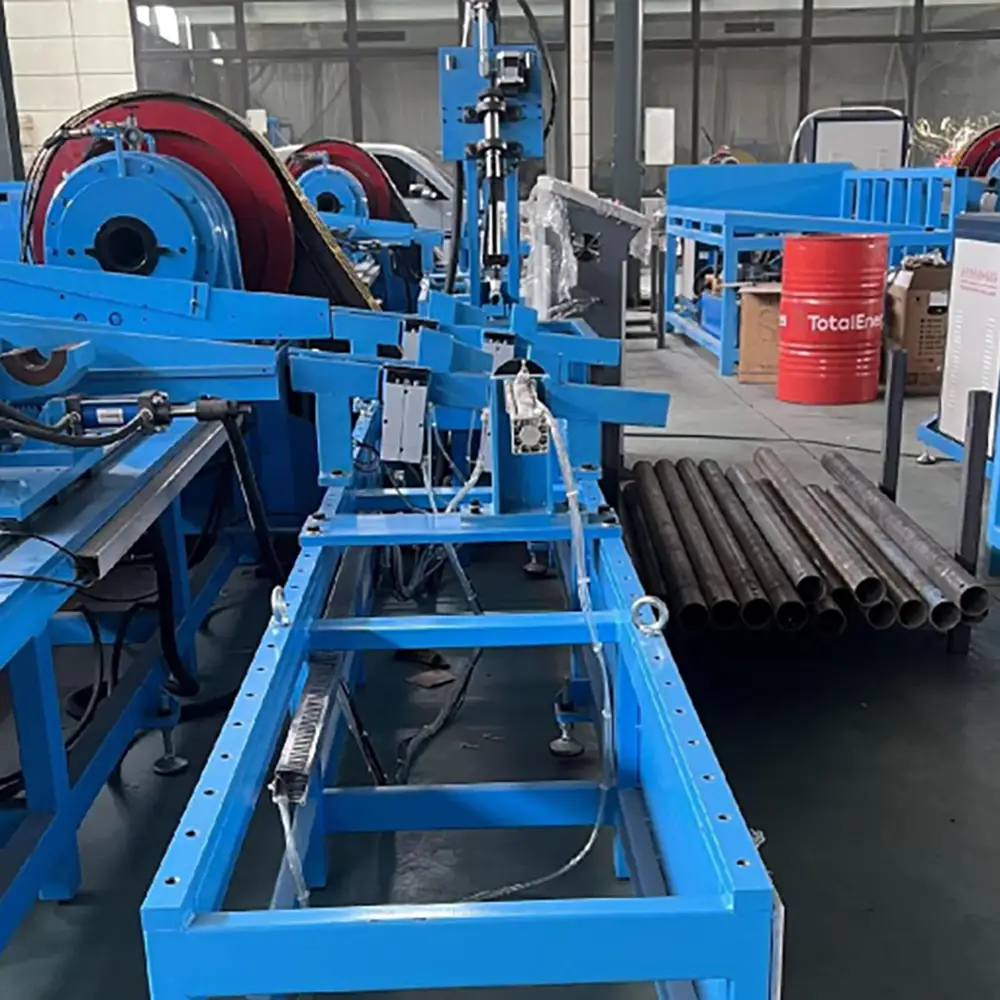
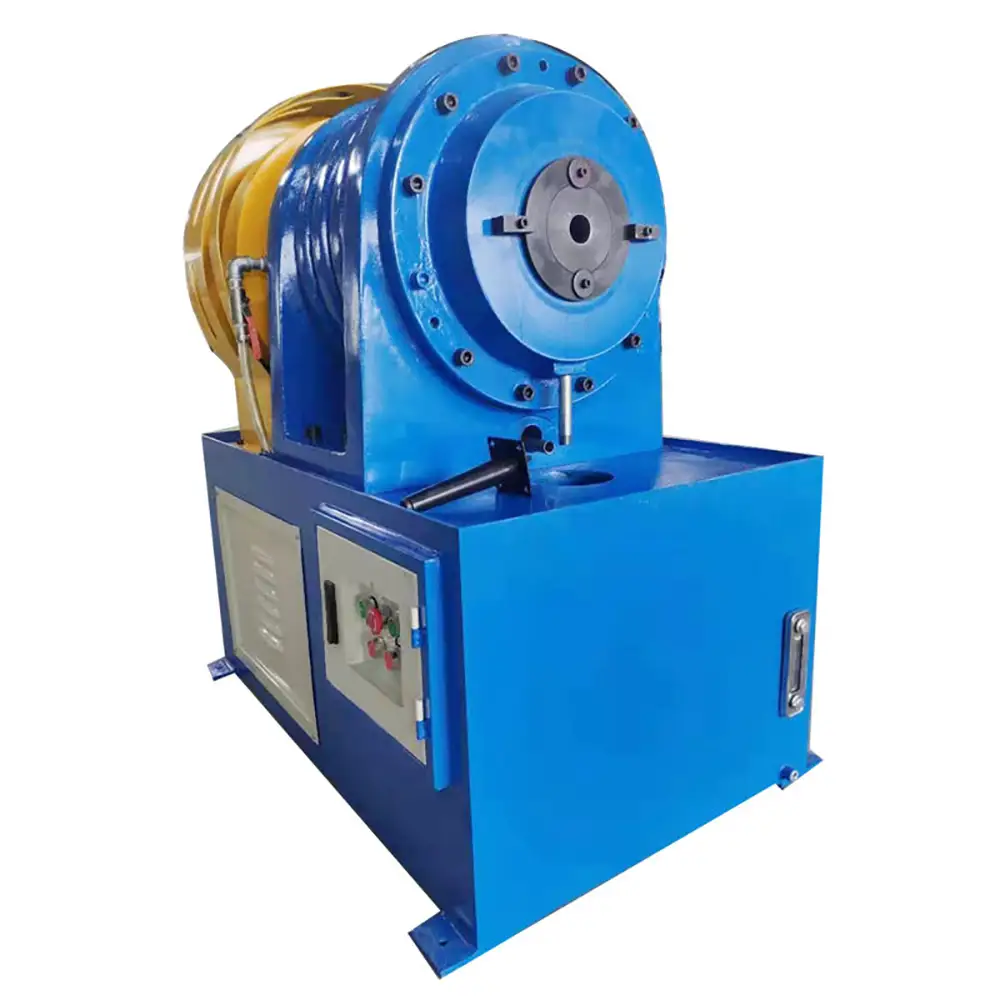
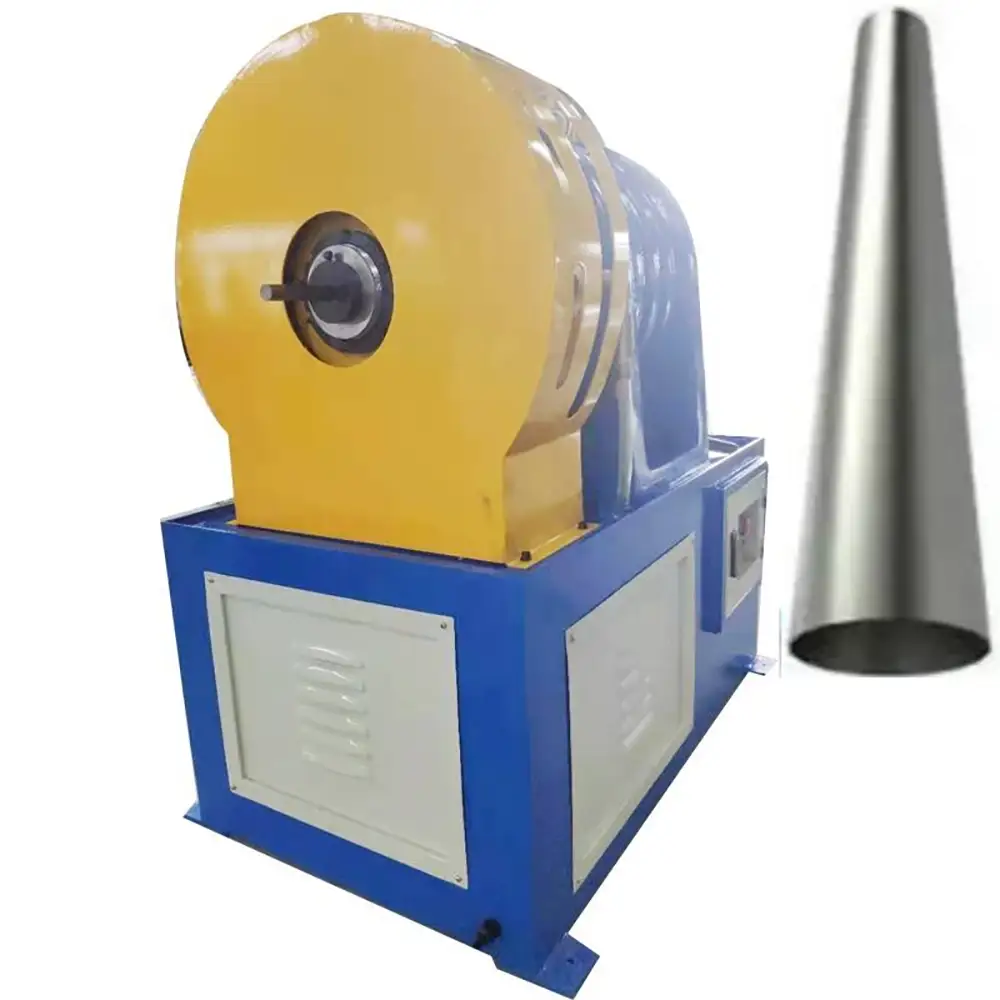
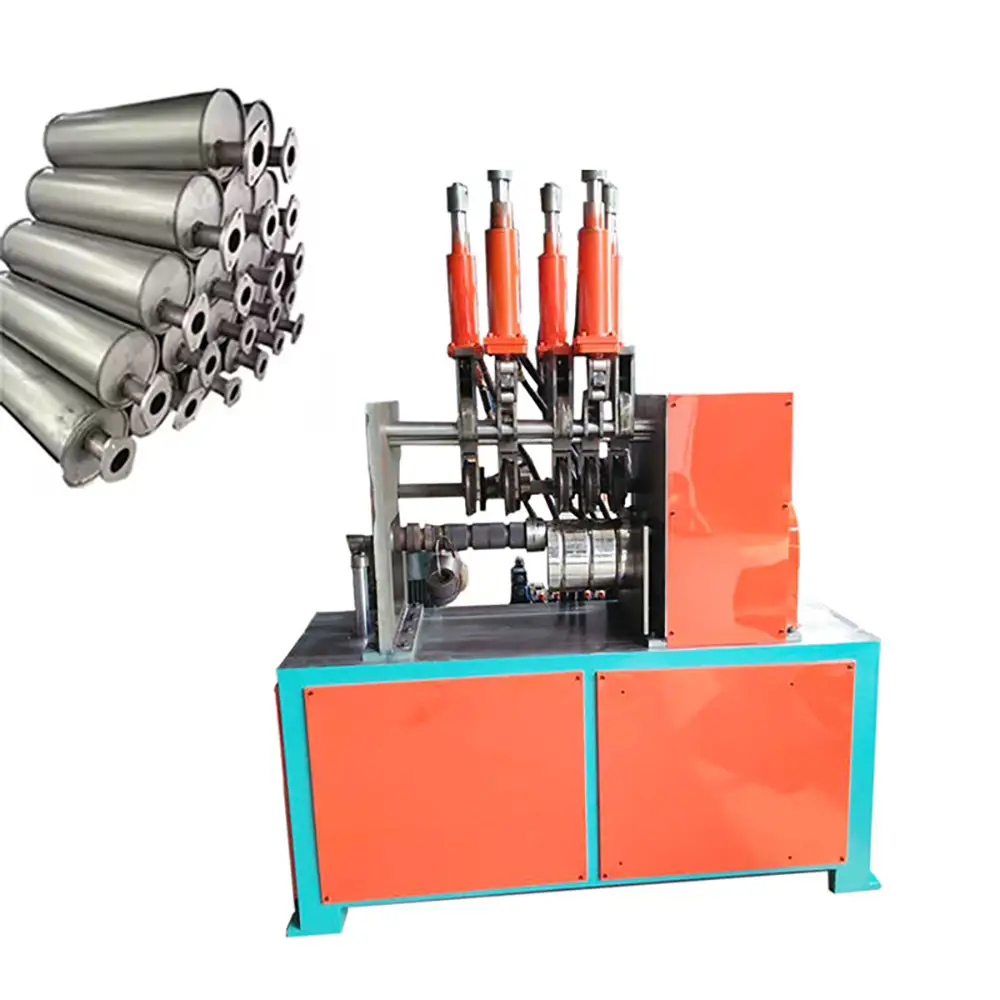
It is mainly composed of steel body, pneumatic tube clamping mechanism, linear guide mechanism rotary whole mouth + rotary flaring, positioning mechanism, pneumatic shifting mechanism, pneumatic flaring mechanism, mould, pneumatic components, electric cabinet and operation panel, etc.
Firstly, carry out manual debugging and confirm the workpiece is qualified. Manually put on the tube, put the tube into the clamping die and push it to the positioning block, the foot switch will automatically complete the automatic action and take the tube manually.
|
model |
HQT-20b |
|
Working air pressure |
0.4-0.8mPa |
|
Using power |
380V/50Hz |
|
Processing Tubes |
copper tube |
|
Processing pipe diameter |
belowΦ19.05 |
|
Flare shape |
Horn shape |
|
Moulds |
Customizable |
|
Dimension |
1000mm*580mm*1250mm |
|
Package Size |
1100mm*650mm*1350mm |
|
Machine weight |
250kg |
Semi-Automatic Pneumatic Rotary Tube Expander for Thin Pipe
The Semi-Automatic Pneumatic Rotary Thin Pipe Flared Tube Expander End Forming Machine is designed for controlled expansion,flaring,and end forming of suitable metal pipes and tubes. Combining pneumatic actuation with rotary forming technology,the machine provides a practical solution for manufacturers that need repeatable tube end processing without the complexity of a fully automated production line.
The equipment can be used for suitable thin-wall pipes,metal tubes,flared tubes,stainless steel tubes,aluminum tubes,copper tubes,and other compatible tubular components. Depending on the tooling and machine configuration,the forming process can create an expanded or flared tube end for connection,assembly,sealing,or subsequent manufacturing operations.
The semi-automatic operating concept provides a balance between operator flexibility and machine-assisted forming. The operator can load and position the tube while the pneumatic forming system performs the programmed or controlled expansion cycle.
Actual forming capacity depends on tube material,outside diameter,wall thickness,expansion ratio,flaring dimensions,forming length,tooling,and machine configuration.
Pneumatic Tube Expansion System
The machine uses compressed air to drive the forming mechanism. Pneumatic actuation can provide controlled and repeatable movement during the tube expansion process.
Compared with completely manual forming,pneumatic operation can reduce repetitive physical effort and help standardize the forming cycle. The actual air pressure required depends on the tube dimensions,material properties,tool geometry,and desired finished profile.
Thin-wall tubing requires particular attention during forming because excessive force can cause cracking,wrinkling,wall deformation,or dimensional variation. Correct tooling and suitable process parameters are therefore important.
Customers should provide the tube material,diameter,wall thickness,and finished dimensions when selecting the appropriate machine configuration.
Rotary Tube Expanding Process
The rotary forming system is designed to reshape the tube end around its circumference. Depending on the specific machine design,the expansion tooling may rotate or use a rotary forming action to progressively enlarge the selected tube section.
Rotary expansion can help distribute the forming process around the circumference and may be suitable for applications where a controlled,uniform tube end is required.
Potential applications include:
Tube end expansion
Pipe end flaring
Connection preparation
Tube coupling preparation
HVAC tube processing
Refrigeration tube forming
Automotive tube processing
Custom metal tube forming
The finished result depends on tube alignment,tooling geometry,forming force,rotation,material properties,and machine setup.
Thin Pipe and Thin-Wall Tube Forming
Thin pipes and thin-wall tubes are commonly used where reduced weight and efficient material usage are important. However,thin-wall materials can be more sensitive to forming pressure.
The machine can be configured for suitable thin tubes used in:
Air conditioning tubing
Refrigeration tubing
Automotive components
Exhaust components
Heat transfer systems
Furniture tubing
Decorative metal tubes
General industrial assemblies
There is no universal definition of “thin pipe” because acceptable wall thickness depends on tube diameter,material,and application.
For production requiring strict dimensional accuracy,testing samples before final machine selection can help determine suitable tooling and forming parameters.
Tube Flaring and Flared End Forming
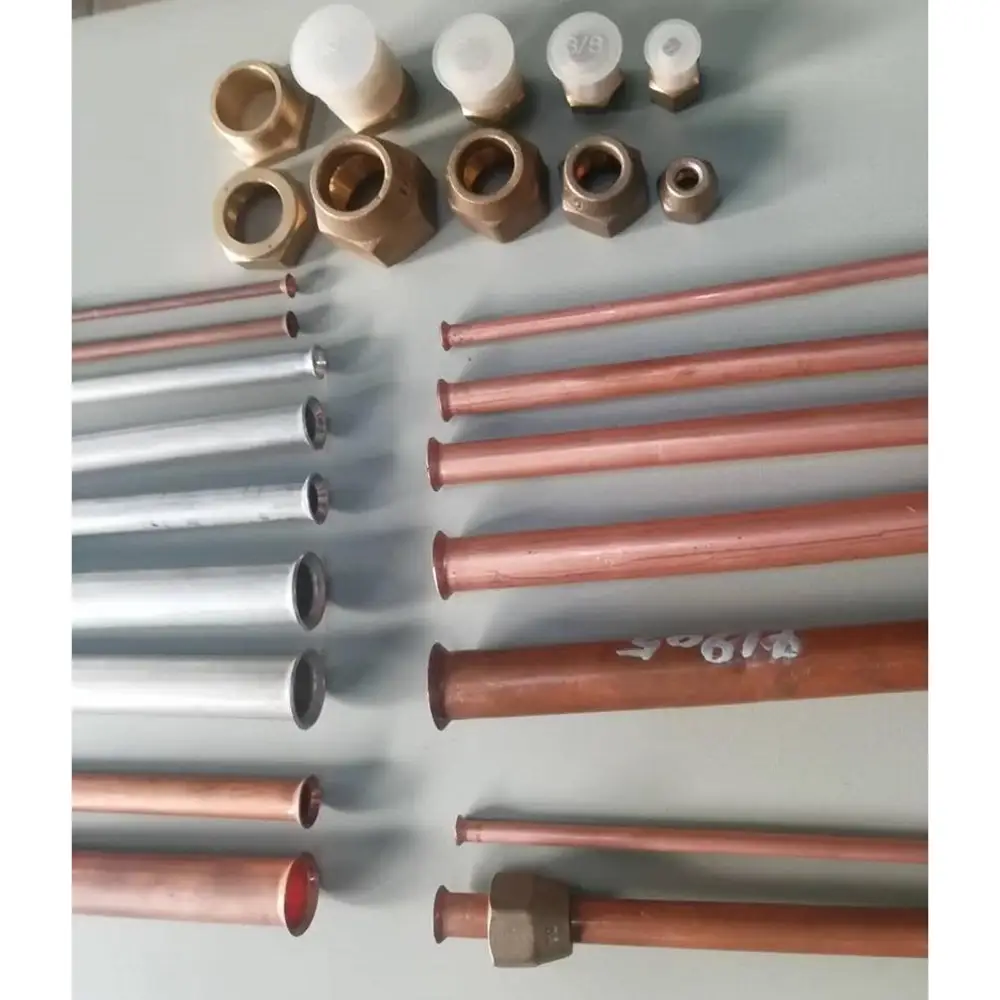
Tube flaring creates an enlarged or angled tube end that can be used for connection or sealing applications. The final flare shape depends on the forming die and machine configuration.
Flared tube ends are commonly associated with tubing systems where a formed end interfaces with another component. Depending on the application,flaring can help create a suitable mechanical connection or assembly surface.
The machine can be evaluated for suitable flaring applications involving copper,aluminum,stainless steel,carbon steel,and other compatible tube materials.
The actual flare angle,diameter,and forming length should be specified by the customer when requesting tooling.
Semi-Automatic Operating Workflow
The semi-automatic configuration allows the operator to maintain control over workpiece loading and positioning while using pneumatic machine assistance for the forming operation.
A typical cycle may include:
Loading the tube into the fixture.
Positioning the tube according to the required forming length.
Clamping or securing the workpiece.
Activating the pneumatic forming cycle.
Completing the rotary expansion or flaring operation.
Returning the forming mechanism.
Removing the finished tube.
The exact workflow varies according to machine design.
Semi-automatic operation can be particularly useful for manufacturers that process multiple tube sizes or product variations because operators can change workpieces without requiring a fully automated feeding system.
Tube End Forming Applications
Tube expansion and flaring are part of a broader group of tube end-forming processes. Depending on the tooling,the same general equipment category may support selected operations such as:
Expansion
Flaring
Reducing
Necking
Swaging
Tapering
Beading
Custom end shaping
Not every configuration supports all operations. The actual functions depend on the forming head,tooling,and machine structure.
Custom dies can be developed when a standard expansion or flare profile does not meet the required finished dimensions.
Materials
The machine can be configured for suitable metal tubing,including:
Copper
Aluminum
Stainless steel
Carbon steel
Mild steel
Galvanized steel
Other compatible metal alloys
Different materials have different forming characteristics. Copper and aluminum are generally more ductile than many steel grades,while stainless steel can require careful control because of its strength and work-hardening behavior.
The selected tooling and forming parameters should therefore match the actual material grade and tube dimensions.
HVAC and Refrigeration Tube Applications
Tube expansion and flaring are commonly associated with HVAC,refrigeration,and heat transfer applications.
Suitable tubes may be used for connection preparation,component assembly,or other tube-processing operations. Copper and aluminum tubing are frequently used in thermal management and refrigeration-related products,while stainless steel and steel tubes may be used in other industrial systems.
For HVAC or refrigeration applications,the required finished dimensions should be determined by the mating components and connection design.
Customers should provide tube diameter,wall thickness,material,and required flare or expansion dimensions when selecting the machine.
Automotive and Exhaust Applications
The machine can also be considered for automotive and motorcycle tube processing. Tube expansion can create connection sections between tubular components,while flaring or other end-forming operations can produce specific assembly profiles.
Potential applications include:
Automotive tubing
Motorcycle components
Exhaust connectors
Muffler tubes
Resonator tubes
Fluid transfer tubes
Engine-related tubular components
The machine should be selected according to the tube material,diameter,wall thickness,and required finished profile.
Tooling and Custom Dies
Tooling plays an important role in tube expansion and flaring quality. The forming die determines the final tube geometry and must be matched to the original tube dimensions.
Custom tooling can be developed for:
Specific tube diameters
Thin-wall tubing
Custom flare profiles
Expanded tube ends
Multi-step forming
Connection preparation
Special OEM components
For customized projects,customers should provide CAD drawings,samples,material specifications,and required finished dimensions.
These details help determine the appropriate forming tooling and machine configuration.
Production Efficiency and Repeatability
The semi-automatic pneumatic system can help standardize repeated tube-forming operations.
Once the correct tooling,fixture,and process settings are established,operators can repeat the same forming cycle on similar tubes. This can help reduce variations associated with completely manual forming.
Actual production output depends on tube size,forming depth,cycle time,loading method,material properties,tool changes,and operator workflow.
For high-volume applications,the machine can potentially be combined with automatic feeding or material handling systems when supported by the selected configuration.
Quality Control
Finished tubes should be inspected according to the requirements of the application.
Important inspection points may include:
Expanded diameter
Flare diameter
Flare angle
Forming length
Wall deformation
Roundness
Concentricity
Surface condition
Overall dimensional consistency
First-piece inspection can help establish suitable forming parameters. Periodic inspection can then be used to monitor tooling wear and production consistency.
For precision applications,the final acceptance tolerances should be established before production.
Maintenance and Safety
Regular maintenance helps keep the machine operating reliably. Operators should inspect pneumatic hoses,fittings,valves,forming dies,fixtures,rotary components,and other moving parts according to the manufacturer's recommendations.
Compressed-air systems should be checked for leaks and operated within the recommended pressure range.
The forming area may contain moving parts and pinch points. Operators should keep hands away from the tooling during operation and use appropriate personal protective equipment.
Guards,emergency-stop functions,and other safety features depend on the actual machine configuration. Operators should follow the manufacturer's operating instructions and applicable workplace safety requirements.
OEM and Custom Tube Forming Solutions
The Semi-Automatic Pneumatic Rotary Tube Expander can be customized for different tube-processing requirements.
Potential options may include:
Custom expansion dies
Flare-forming tooling
Tube fixtures
Pneumatic system configuration
Adjustable positioning
Rotary forming tooling
PLC-assisted control
Automatic feeding
Special workholding systems
Customers should provide tube material,outside diameter,wall thickness,required flare or expansion dimensions,forming length,production volume,and drawings or samples.
This information helps determine the appropriate machine configuration and tooling solution.
Why Choose Us
Semi-Automatic Operation — Provides a practical balance between operator flexibility and machine-assisted tube forming.
Pneumatic Forming System — Uses controlled compressed-air actuation for repeatable expansion and flaring operations.
Rotary Tube Expansion — Designed for circumferential tube end forming with dedicated rotary tooling.
Thin-Wall Tube Applications — Suitable configurations can be developed for selected thin pipes and thin-wall tubes.
Expansion and Flaring — Supports suitable tube end expansion,flaring,and selected custom forming applications.
Multiple Material Options — Can be configured for copper,aluminum,stainless steel,carbon steel,and other compatible tubes.
Custom Tooling Support — Expansion dies,flare dies,fixtures,and workholding systems can be customized.
OEM & B2B Manufacturing Service — Suitable for manufacturers,distributors,wholesalers,and international buyers sourcing tube end-forming equipment.
FAQs
1. What is a pneumatic rotary tube expander?
A pneumatic rotary tube expander is a machine that uses compressed air and rotary forming tooling to expand or reshape a suitable tube end.
2. Can it process thin-wall tubes?
Yes. It can be configured for suitable thin-wall tubing,but the actual range depends on tube material,diameter,wall thickness,tooling,and required expansion.
3. What is tube flaring?
Tube flaring is a forming process that enlarges or reshapes the end of a tube to create a specified flare profile for connection or assembly.
4. Can the machine expand and flare tubes?
Yes,when equipped with appropriate expansion and flaring tooling. The available functions depend on the machine configuration.
5. What materials can be processed?
Depending on the configuration,the machine may process copper,aluminum,stainless steel,carbon steel,mild steel,galvanized steel,and other compatible tubing.
6. Is it suitable for copper tubes?
Yes. Copper tubing can be processed when the tooling and forming parameters are correctly matched to the tube dimensions and material.
7. Can stainless steel tubes be flared?
Suitable stainless steel tubes can be flared when the machine,tooling,and forming parameters are appropriate for the specific material and tube dimensions.
8. Is the machine fully automatic?
No. The described configuration is semi-automatic. Operators generally load and position the tube while the machine assists with the forming cycle.
9. What industries can use this machine?
Potential applications include HVAC,refrigeration,automotive,motorcycle,exhaust,heat transfer,furniture,and general metal tube manufacturing.
10. What affects tube expansion quality?
Tube material,diameter,wall thickness,forming ratio,tooling geometry,air pressure,alignment,rotary movement,and machine rigidity can all affect the finished result.
11. Can custom flaring or expansion dies be supplied?
Yes. Custom dies can be developed according to tube drawings,samples,required flare dimensions,and finished product specifications.
12. What information is needed for a quotation?
Provide the tube material,outside diameter,wall thickness,required expanded or flared diameter,flare angle if applicable,forming length,production volume,and drawings or samples.
Prev:
Heating Tube Taper Machine Pipe Taper Reducing Machine Tube Multifunction End Forming Machine
Next:
Single Head Steel Tube Shrinking Machine Reducing Pipe End Former for Stainless Steel Aluminum Motor Engine Core
TAG:
Pipe End Processing Machine,
Tube End Processing Machine,
Exhaust Pipe End Forming Machine,
Automotive Tube End Forming Machine,
Tube End Forming Equipment,
Pipe Flaring Machine,
Pipe End Forming Equipment,
Pipe Beading Machine,
Tube Beading Machine,
Pipe Tapering Machine,
Tube Flaring Machine,
Pipe Necking Machine,
Tube Necking Machine,
Tube Tapering Machine,
Pipe Reducing Machine,
Pipe End Expanding Machine,
Tube Reducing Machine,
Tube End Forming Machine,
Pipe End Forming Machine,
Tube End Expanding Machine,
Pipe Expanding Machine,
Tube Expanding Machine,
Industrial Tube Forming Machine,
Industrial Pipe Forming Machine,
Semi Automatic Tube Forming Machine,
Tube End Swaging Machine,
Pipe End Swaging Machine,
Pipe End Shaping Machine,
Tube End Shaping Machine,
Rotary Tube Forming Machine,
Related Category:
Semi-Automatic Pneumatic Rotary Tube Expander,Semi-Automatic Tube Expanding Machine,Pneumatic Rotary Pipe Expander China, suppliers, manufacturers, factory, customized, wholesale, quotation, made in China