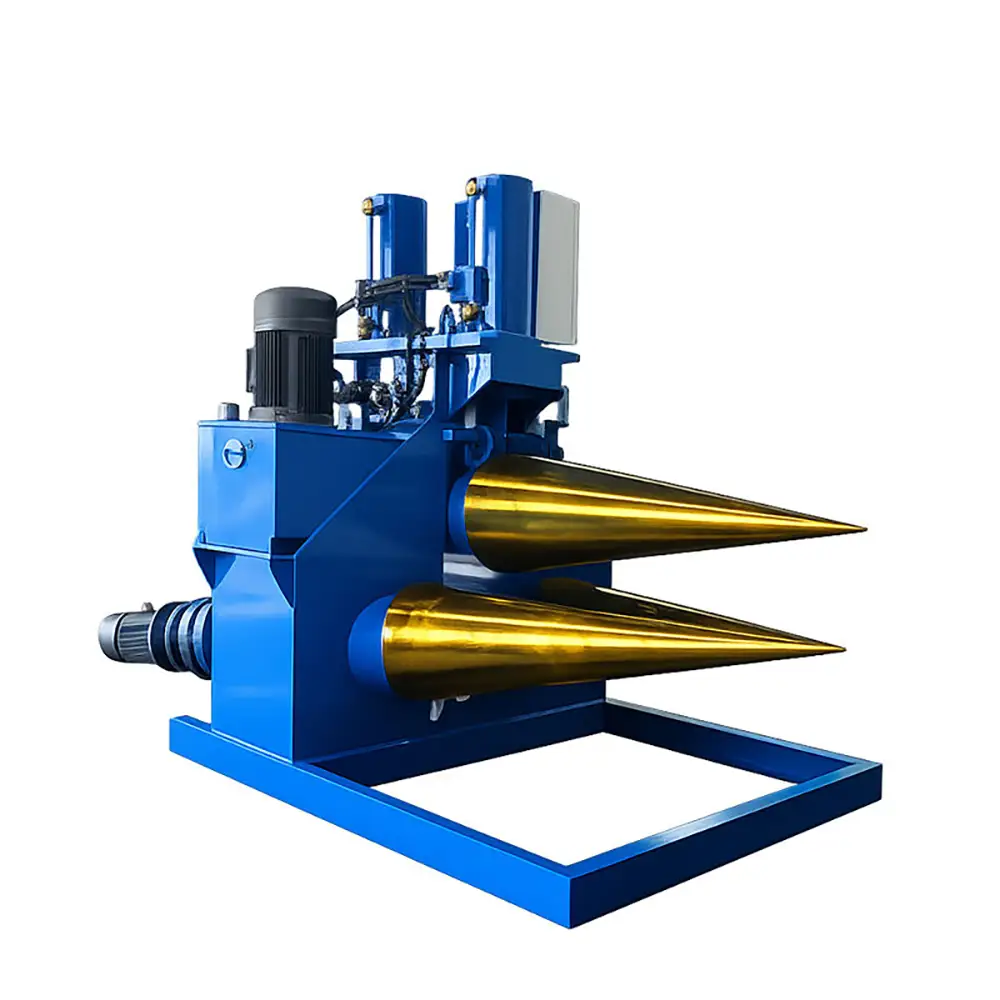
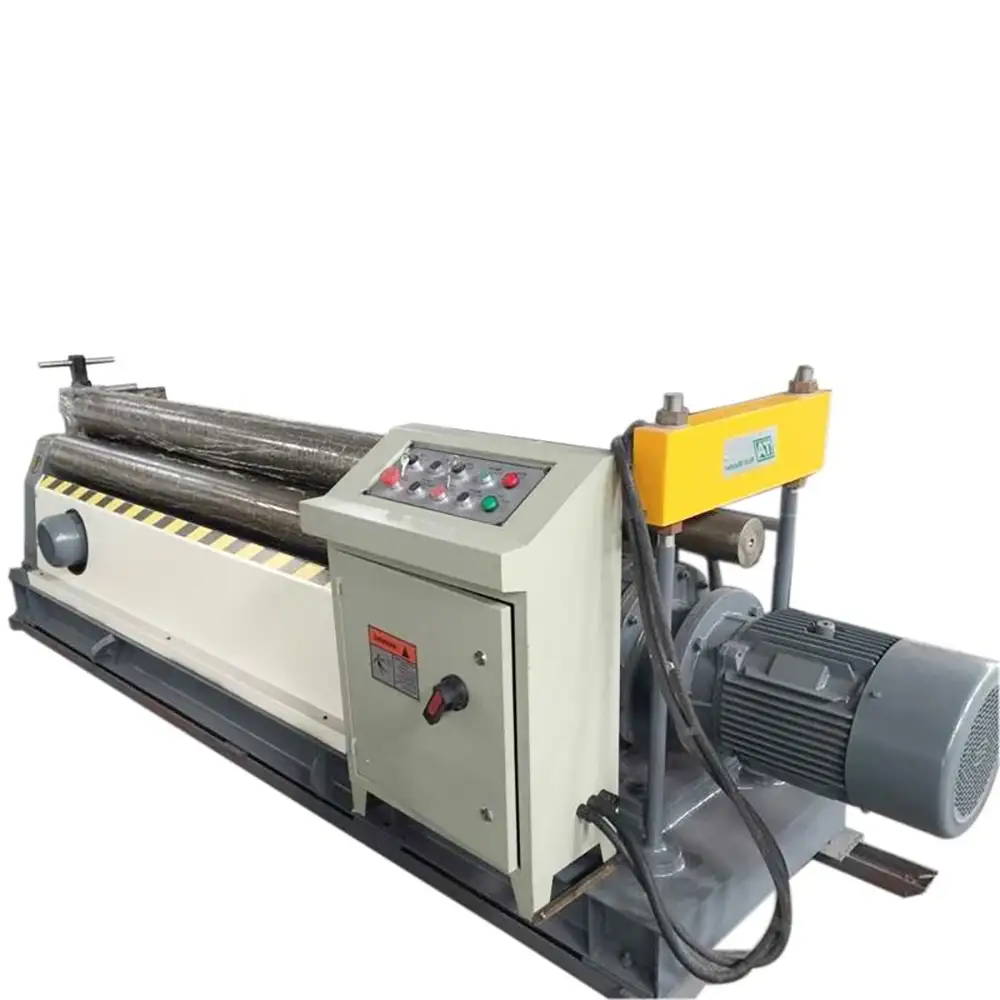
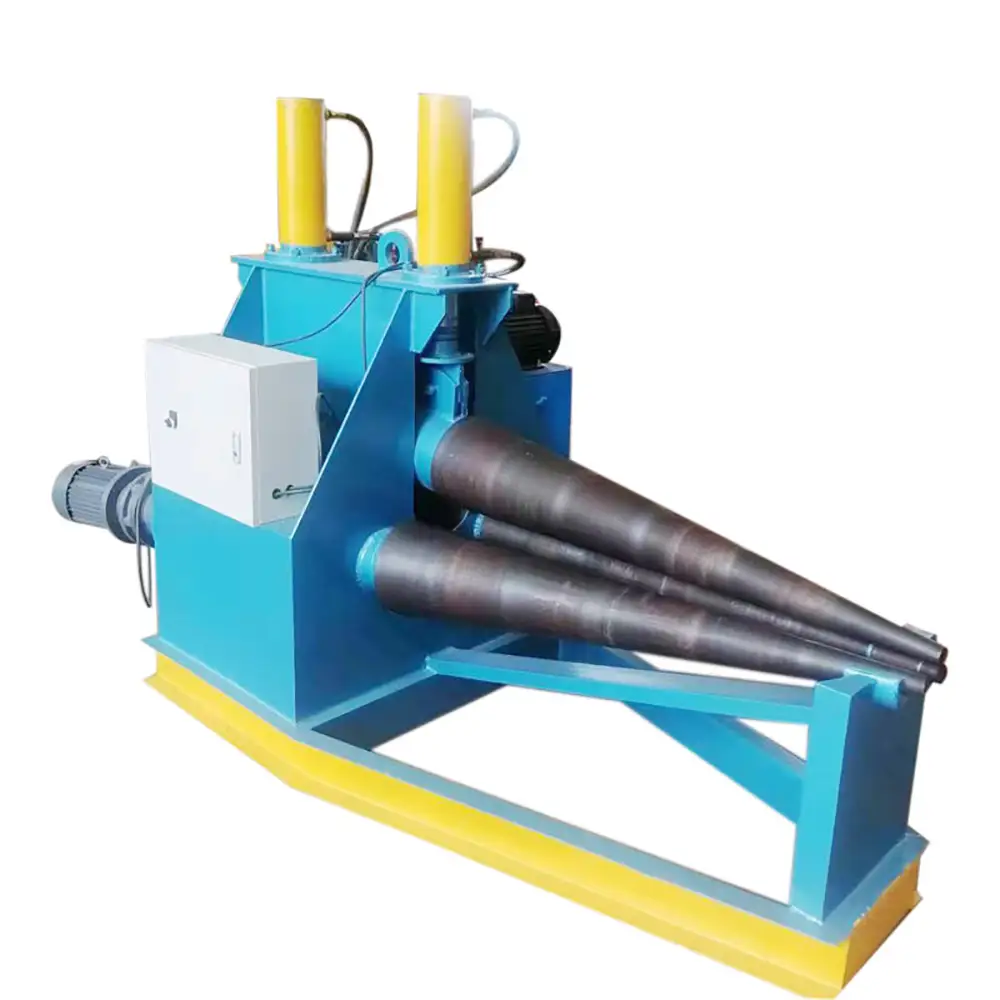
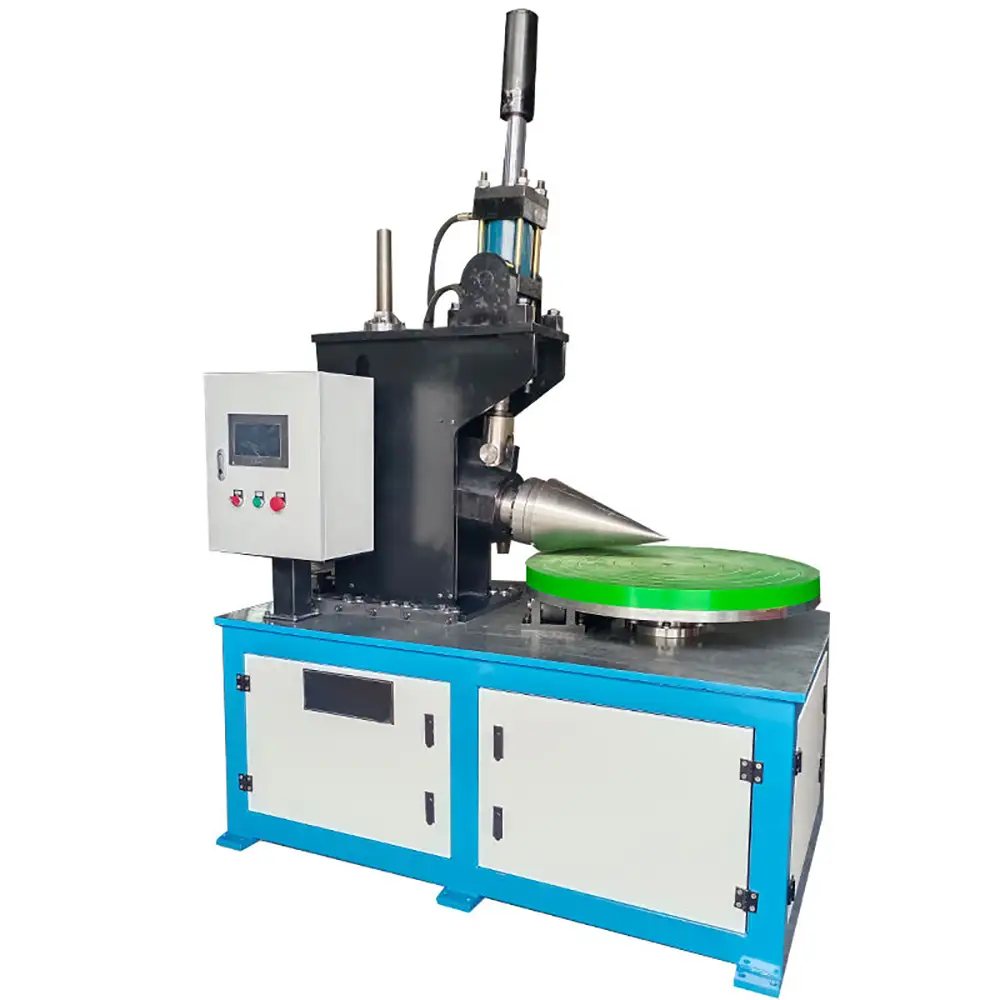
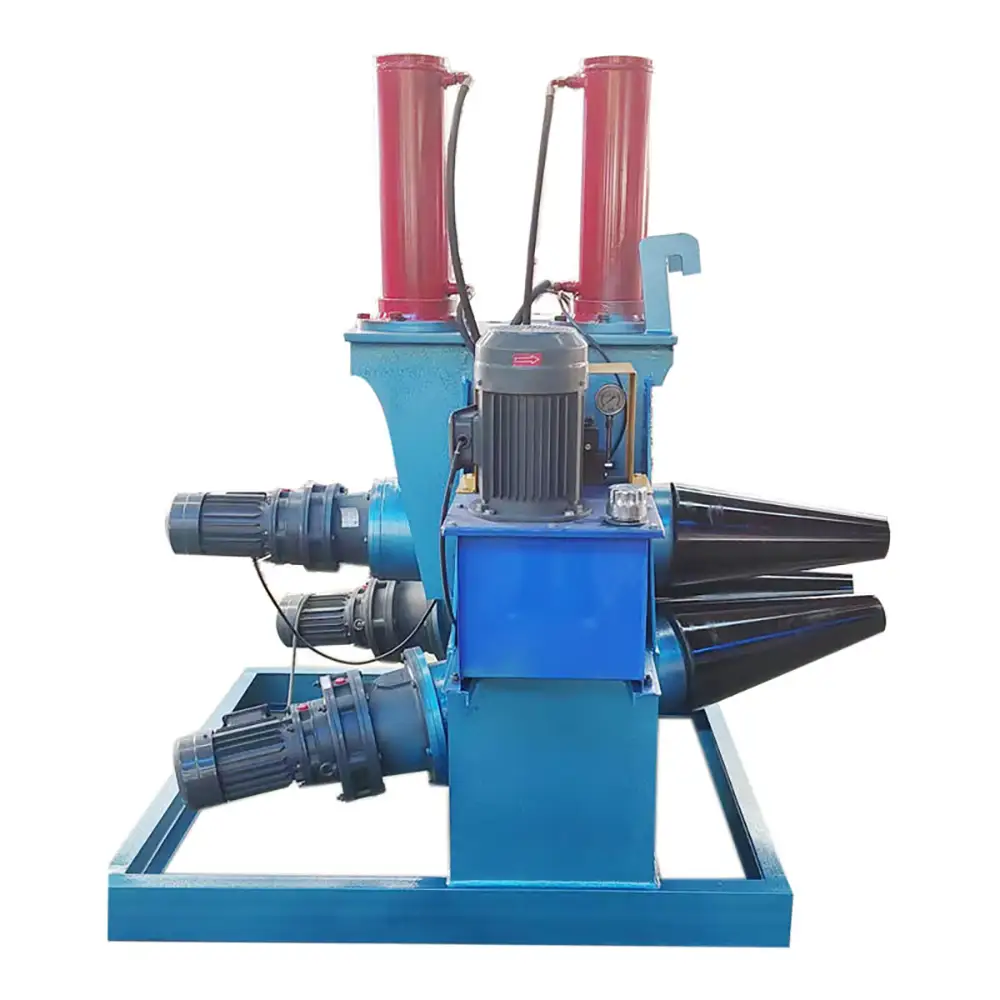
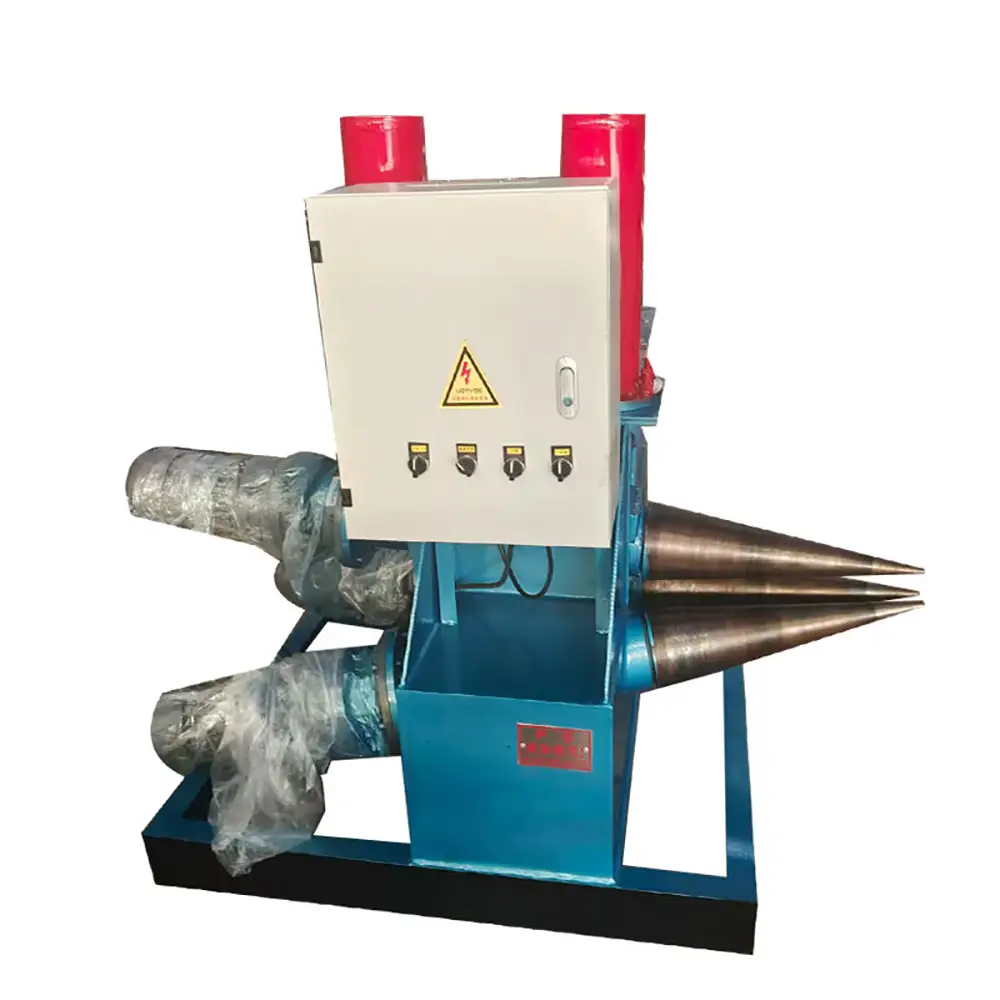
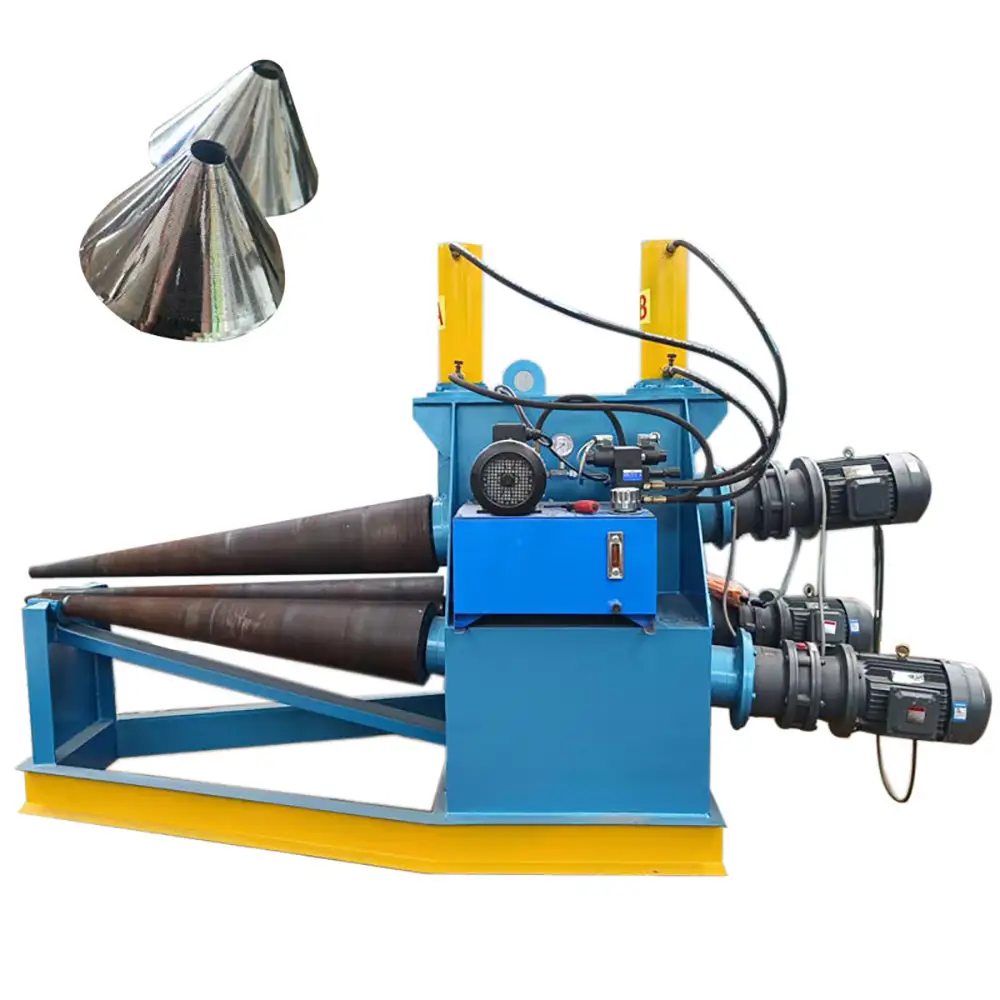
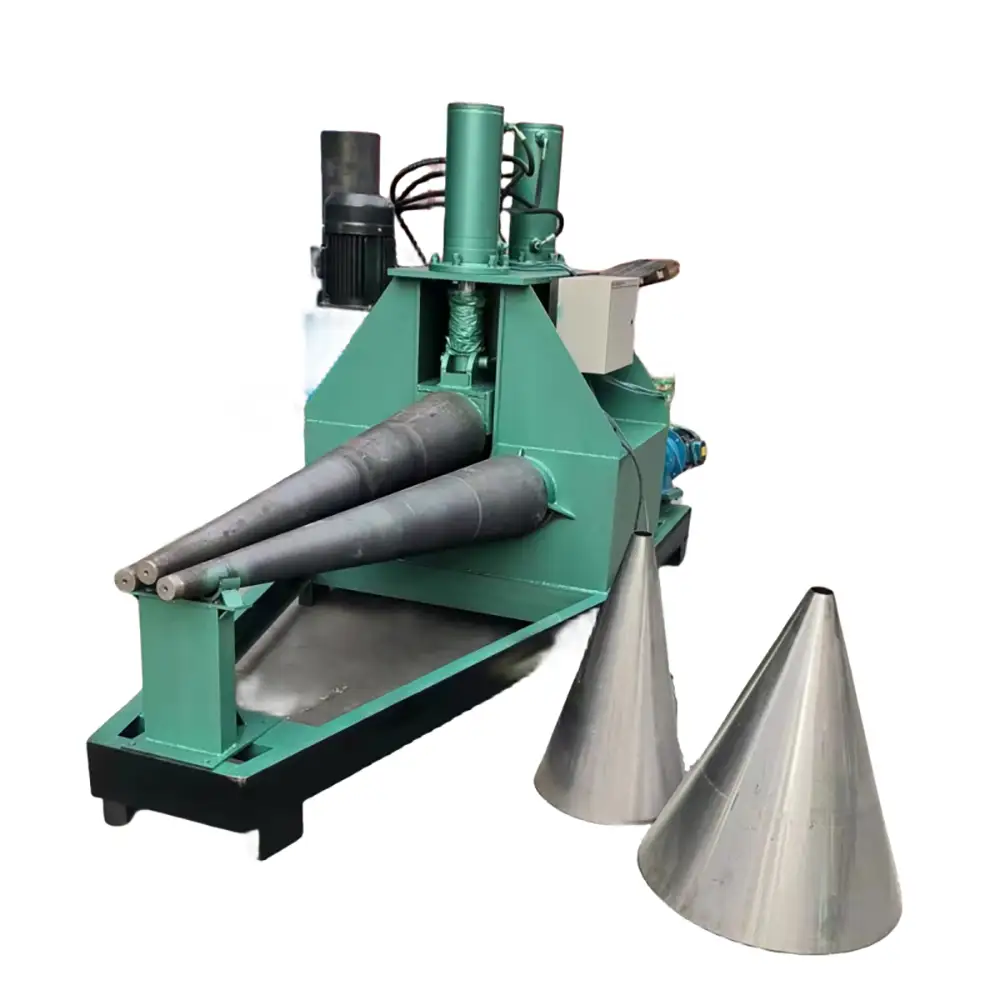
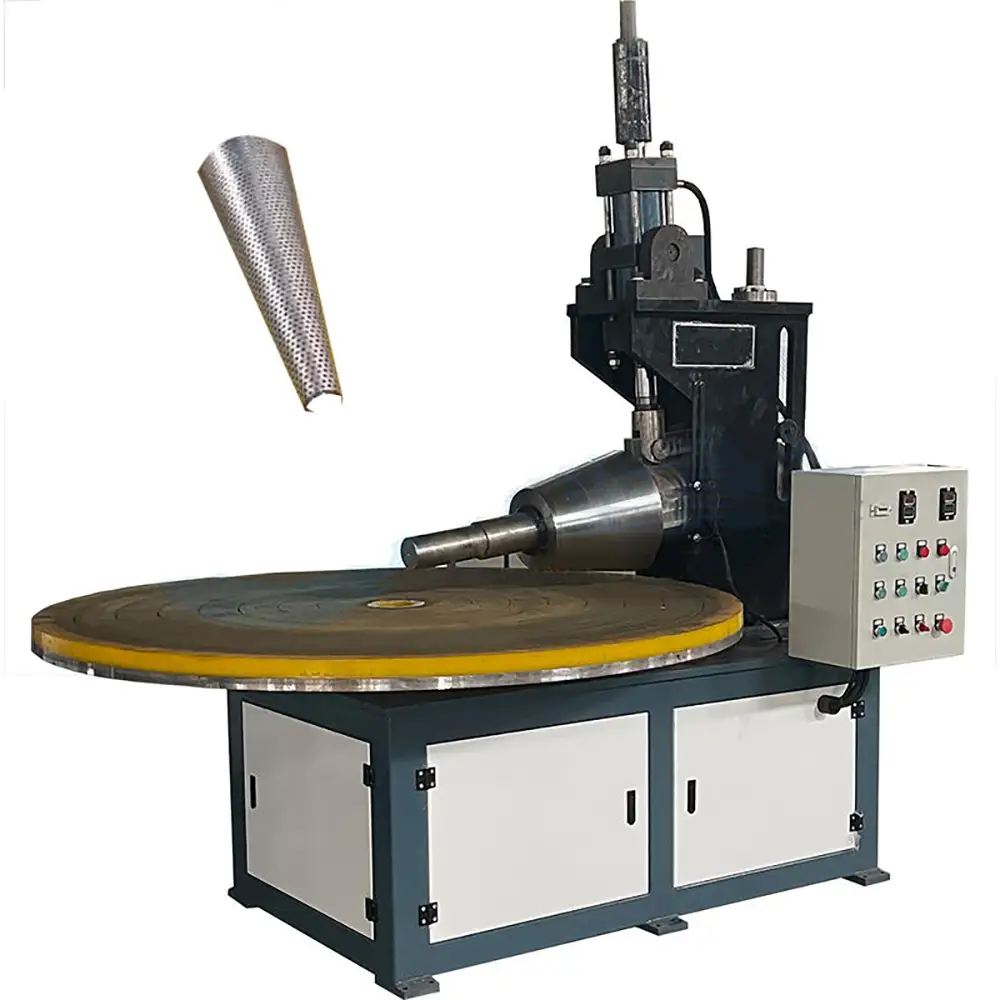
Semi-Automatic Cone Rolling Technology
Cone rolling differs from conventional cylindrical plate rolling because the two edges of a conical blank travel different distances during forming. The larger end of the cone has a greater circumference than the smaller end, requiring differential bending across the plate.
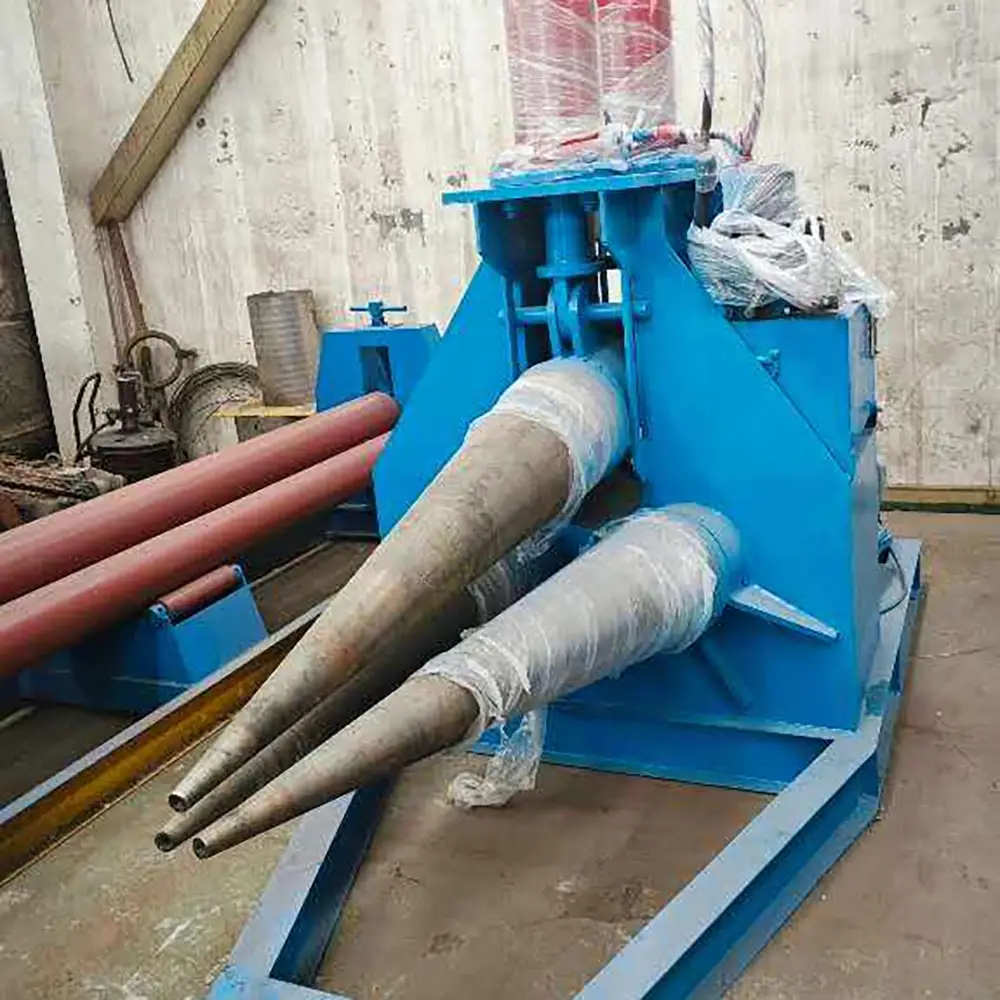
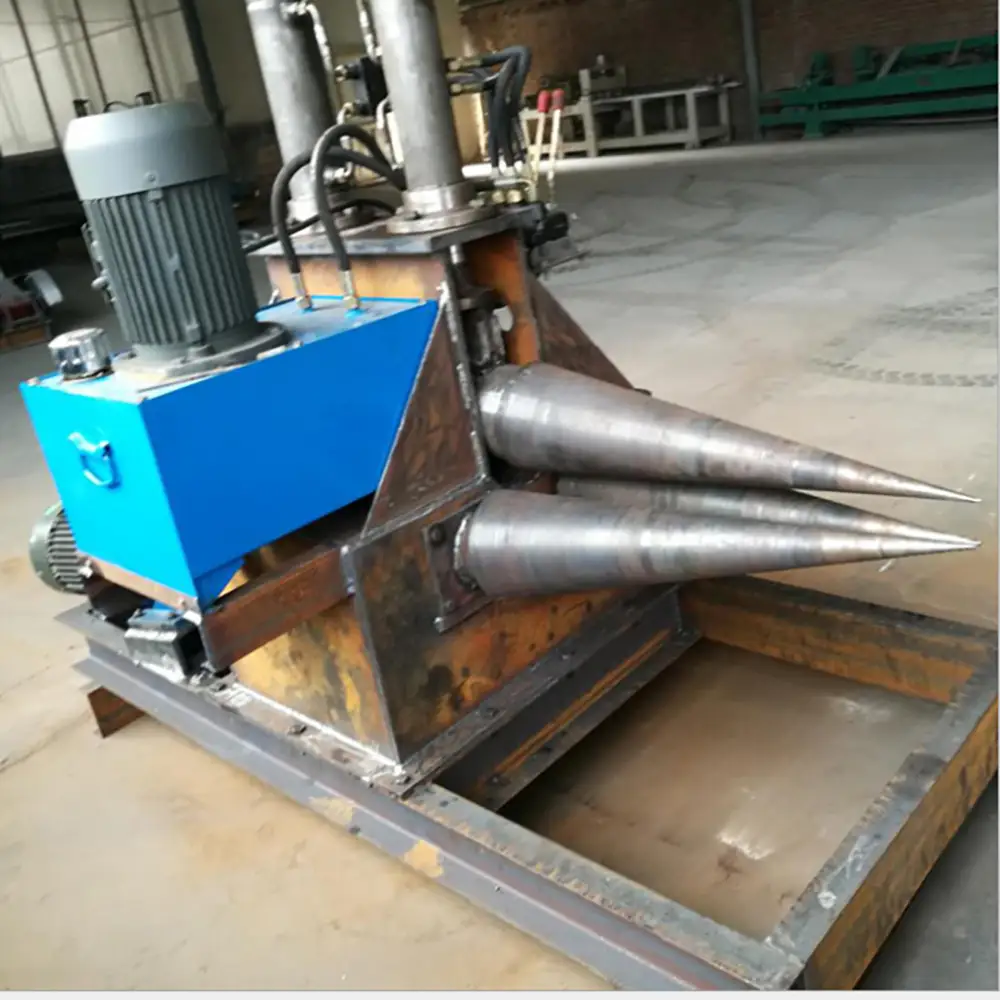
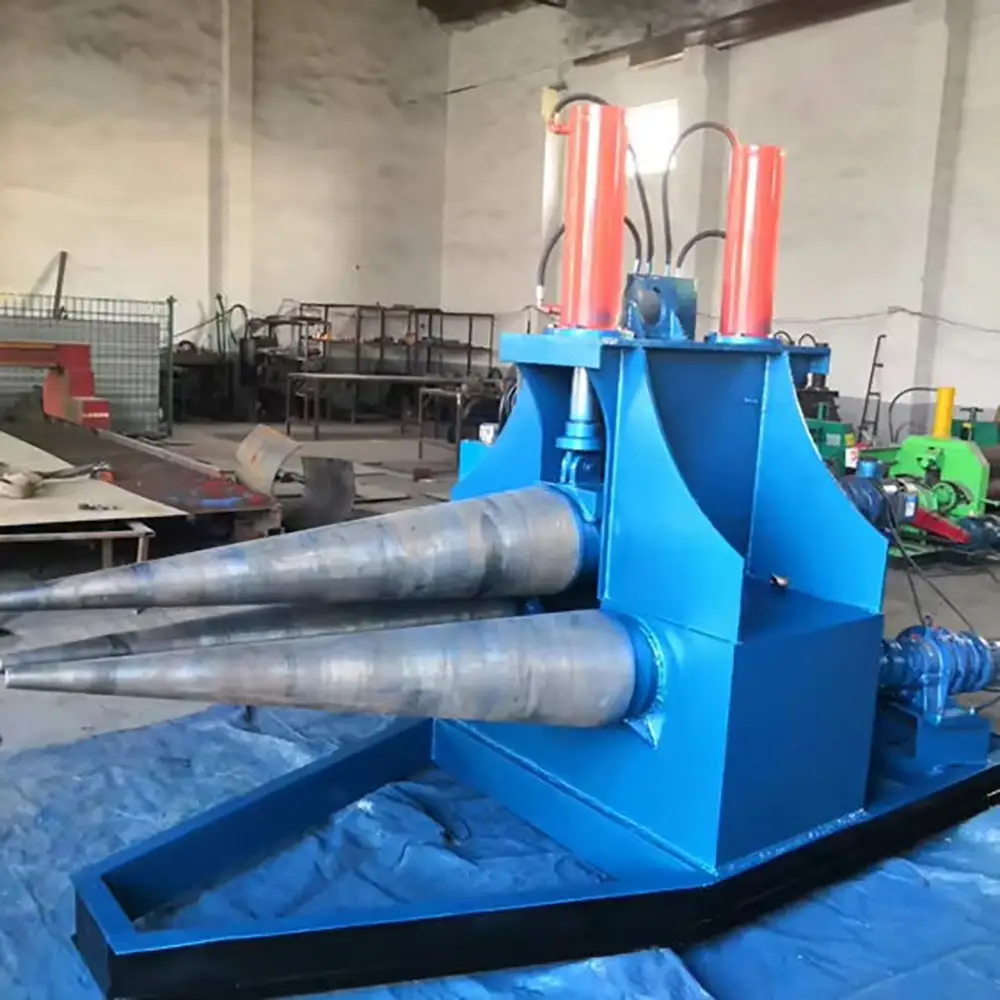
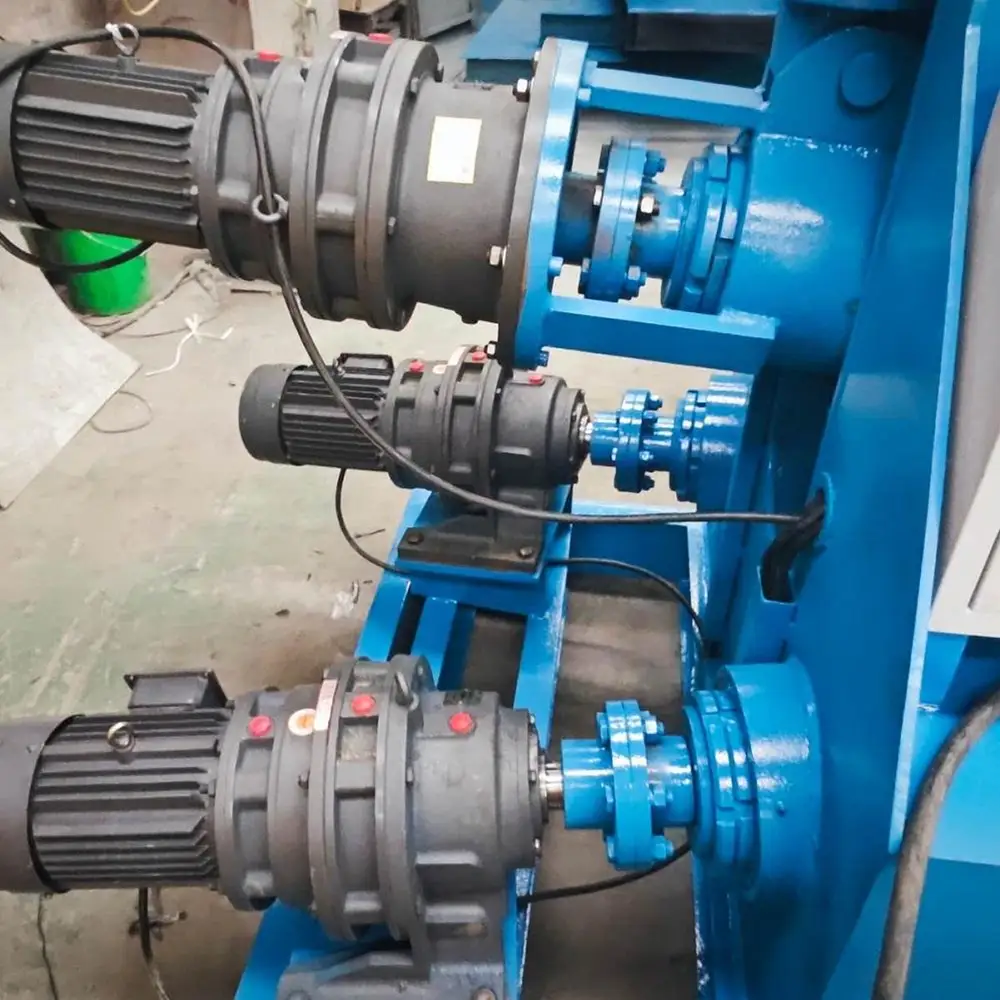
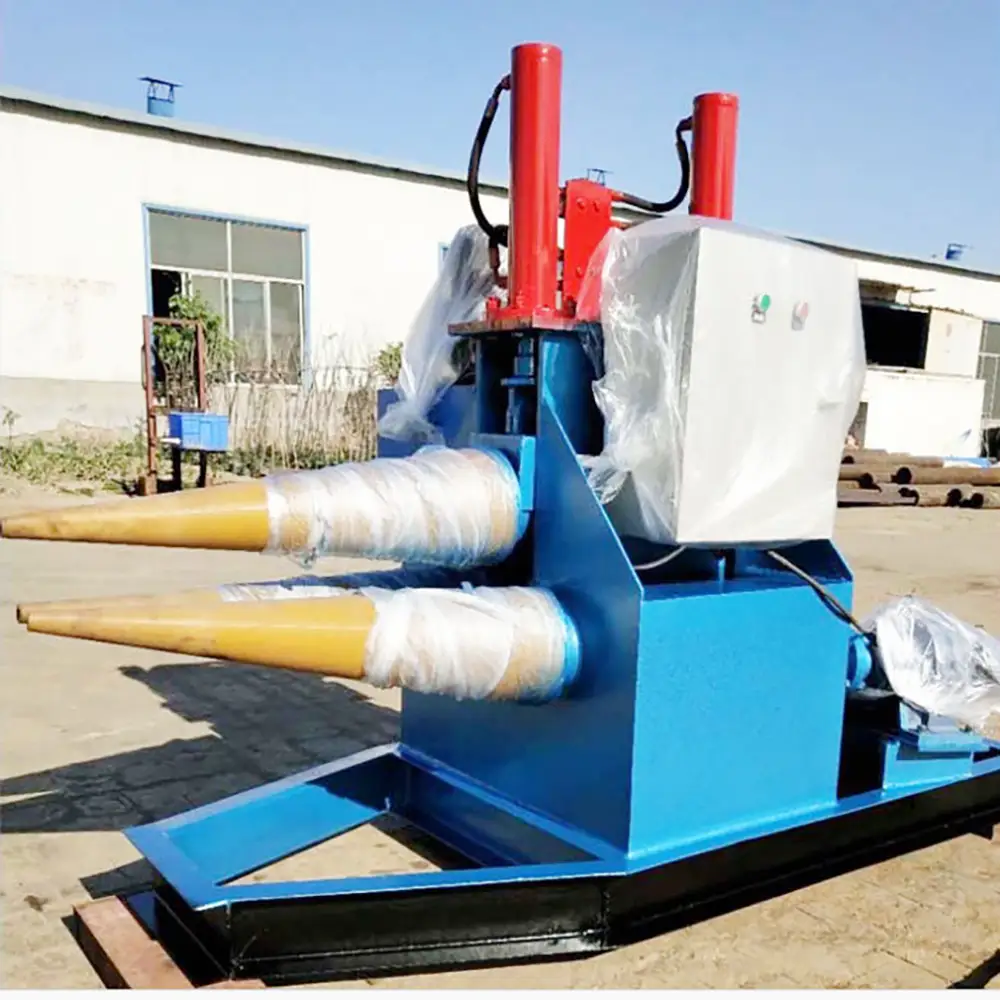
The machine uses forming rolls to gradually bend the prepared blank. Depending on the machine configuration, powered roller rotation and hydraulic or mechanical adjustment can be used to control the forming process.
The operator loads and positions the material, sets the required forming parameters, and monitors the rolling process. Several passes may be required depending on material thickness, cone angle, diameter, and forming requirements.
Actual forming capacity depends on the machine model, roller dimensions, material strength, plate width, thickness, and target cone geometry.
Provide material type, thickness, plate width, larger diameter, smaller diameter, cone height or angle, production quantity, and workpiece drawings if available.
|
model |
6x1200 |
6x1300 |
6x2000 |
6x600 |
|
max plate thickness(mm) |
6(Q235) |
6(Q235) |
6 |
6 |
|
Cone Rolling Length |
1200mm |
1300mm |
2000mm |
600mm |
|
max yield strength of plate(Mpa) |
245 |
245 |
304 |
304 |
|
Upper Roll Diameter (mm) |
240mm |
250mm |
500mm |
10*200mm |
|
Lower Roll Diameter (mm) |
240mm |
250mm |
500mm |
10*200mm |
|
Large End Diameter of Taper Roll |
240mm |
250mm |
500mm |
200mm |
|
Small End Diameter of Taper Roll |
20mm |
40mm |
50mm |
10mm |
|
Rolling Speed(m/min) |
4 |
4 |
4 |
4 |
|
Main Motor Power(KW) |
1.5KW*3 |
1.5KW*3 |
5.5KW*3 |
1.5KW*3 |
|
Hydraulic Motor Power(KW) |
3KW |
3KW |
7.5KW |
3KW |
Hopper and Funnel Cone Forming
One of the key applications of this equipment is manufacturing hopper and funnel shapes. Conical components are widely used in material handling, processing equipment, agricultural machinery, chemical systems, dust collection equipment, food-processing machinery, and industrial production lines.
The cone rolling process can create tapered sections that are subsequently welded, trimmed, calibrated, or assembled into complete products.
Typical components include:
Industrial hoppers
Material funnels
Steel cones
Stainless steel funnels
Transition sections
Reducers
Discharge cones
Dust collection cones
Feed hoppers
Duct transitions
Exhaust components
Custom tapered shells
For welded components, the rolled cone can be transferred to tack welding and final welding after forming. Additional edge preparation, grinding, trimming, and inspection may be required according to the final design.
Stainless Steel Cone Rolling
Stainless steel is widely used for cones and funnels where corrosion resistance, cleanability, or appearance is important. The semi-automatic cone rolling machine can be configured for suitable stainless steel applications within its rated forming capacity.
Stainless steel may require careful forming because different grades have different strength, ductility, work-hardening behavior, and springback characteristics. Appropriate roller settings and forming procedures can help achieve the desired geometry.
For stainless steel components used in food processing, chemical equipment, pharmaceutical equipment, or other specialized applications, surface protection and careful material handling can also be important.
Aluminum Cone Forming
Aluminum provides a lightweight option for many conical components. It can be used for equipment where reducing component weight is beneficial.
Because aluminum has different mechanical properties from steel, forming parameters should be selected according to the specific alloy, thickness, cone dimensions, and machine configuration.
Roller surfaces and workpiece handling should also be considered when appearance or surface quality is important. Suitable machine setup can help minimize unnecessary marks during the forming process.
Carbon Steel Cone Rolling
Carbon steel is one of the most common materials used for industrial cone and hopper fabrication. It offers a combination of strength, availability, and cost efficiency for many general fabrication applications.
The machine can be selected according to the required carbon steel thickness, plate width, cone diameter, and production volume. Heavy-duty applications may require greater forming force and a stronger machine structure.
For thick carbon steel plates, pre-bending and multiple forming passes may be used depending on the workpiece geometry and machine design.
CNC-Assisted Operation
A CNC or digital control system can help simplify parameter management and improve repeatability for recurring production tasks. Depending on the configuration, CNC functions may control or assist with roller positioning, forming sequences, or other machine operations.
The level of automation varies by machine model. A semi-automatic machine still typically requires operator involvement for loading, positioning, inspection, and process supervision.
CNC-assisted operation can be particularly useful when producing multiple cones with similar dimensions. Standardized parameters can help reduce setup variation between batches.
Actual dimensional accuracy and repeatability depend on the machine structure, control system, material properties, tooling, blank accuracy, and production procedures.
Engine Core and Machinery Components
Conical and tapered metal components can also be used in machinery and engine-related applications. Depending on the specific design, cone rolling may be part of the manufacturing process for engine housings, transition sections, air or exhaust-related components, ducts, covers, and other formed metal parts.
The term engine core can refer to different components depending on the application. For this reason, the machine should be selected based on the actual workpiece drawing and forming requirements rather than the application name alone.
Customers can provide component drawings, material specifications, dimensions, and production quantities to determine whether the machine is suitable for their intended engine or machinery component.
Production Efficiency
Semi-automatic operation provides a useful balance between flexibility and productivity. Powered rolling reduces some of the physical effort associated with manual forming while allowing operators to make adjustments during production.
For repeated hopper and funnel production, standardized blank dimensions and forming parameters can improve workflow consistency. Operators can inspect the cone during the rolling process and make adjustments when necessary.
Actual production cycle time depends on material, plate thickness, cone size, cone angle, number of forming passes, loading method, and operator experience.
For larger production operations, the cone rolling process can be integrated with laser or plasma cutting, edge preparation, welding, grinding, inspection, and assembly.
Quality Control
Good cone-forming results depend on accurate blank preparation, correct roller setup, material characteristics, and controlled forming procedures.
Before production, operators should verify the material thickness, blank dimensions, cone diameter, and required cone angle. During rolling, the developing shape can be inspected to identify uneven curvature or incorrect taper.
After forming, dimensional checks can include the larger diameter, smaller diameter, cone height, cone angle, roundness, and seam alignment.
For applications requiring tighter dimensional tolerances, additional measuring equipment or CNC-assisted control may be considered.
Maintenance and Safety
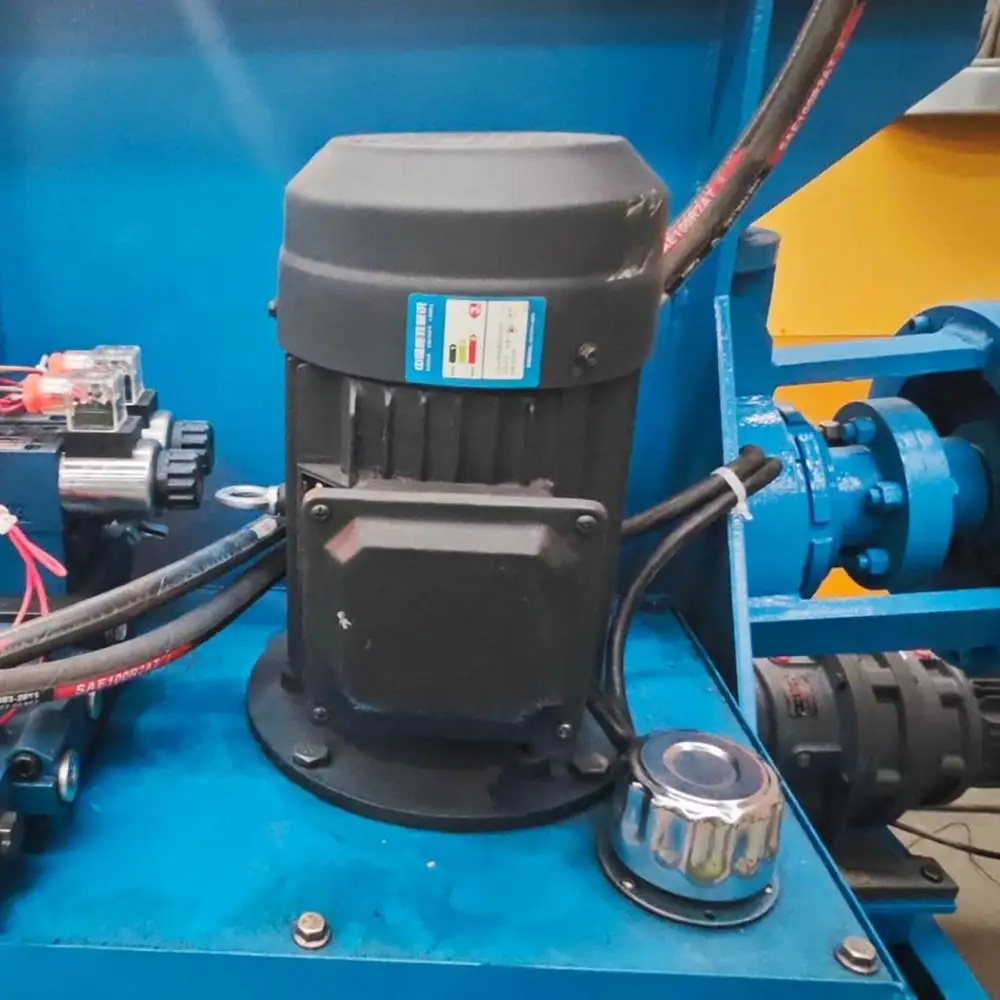
Regular maintenance helps maintain stable machine performance. Hydraulic components, if equipped, should be checked for leakage, while rollers, bearings, drive components, electrical connections, and fasteners should be inspected according to the manufacturer's maintenance schedule.
Roll surfaces should remain clean and free of debris that could affect forming quality.
Because cone rolling involves substantial mechanical force, operators should receive appropriate training. Hands, clothing, and tools must be kept away from rotating rollers and moving components.
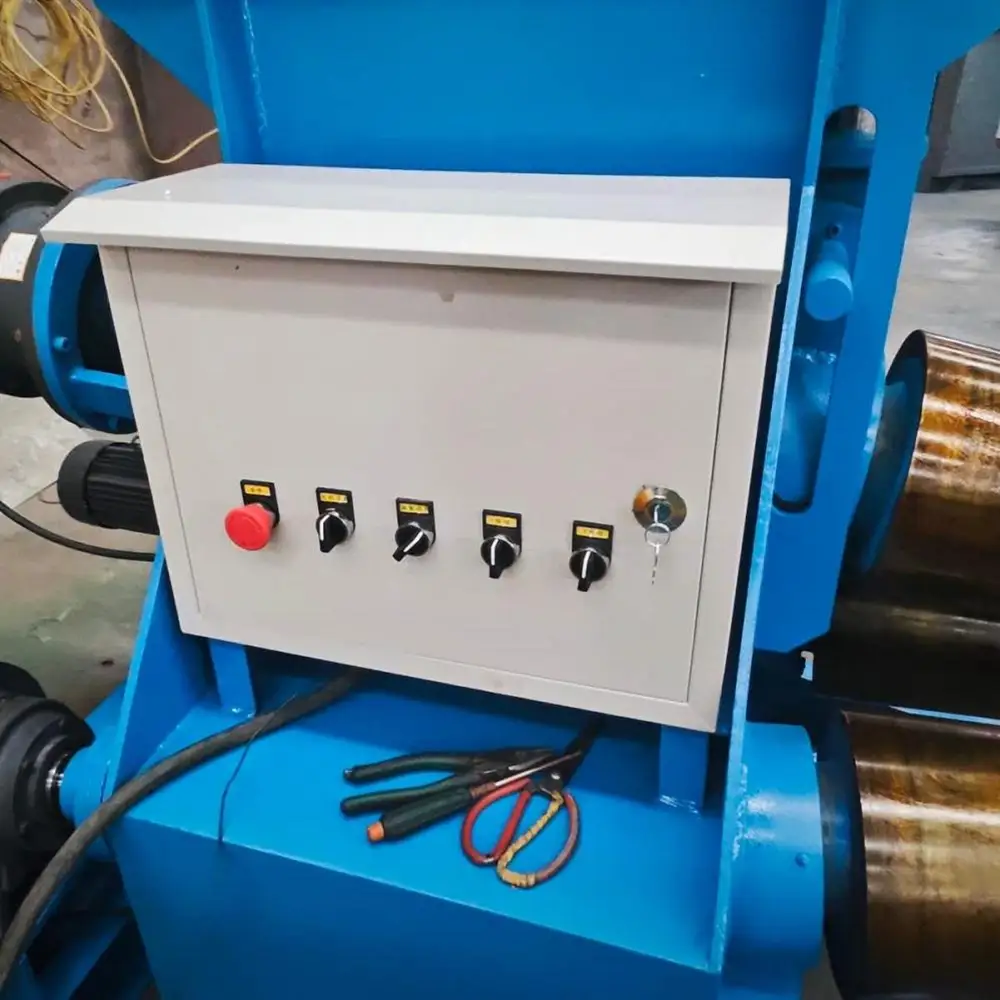
Depending on the machine configuration, safety features may include emergency stops, guards, electrical protection, and other safety-oriented devices. Operators should follow the manufacturer's instructions and applicable workplace safety requirements.
OEM and Custom Cone Rolling Solutions
Every fabrication business may have different requirements for cone dimensions, material, production quantity, and automation level. A professional manufacturer can configure the machine around the customer's actual workpieces.
For an accurate machine recommendation, customers should provide material type, material thickness, plate width, larger and smaller cone diameters, cone height or angle, production volume, and drawings when available.
OEM and custom options may include roller specifications, machine dimensions, drive system, control system, electrical standards, hydraulic configuration, tooling, documentation, and other production requirements.
Why Choose Us
Professional Cone Rolling Equipment
We provide semi-automatic cone rolling solutions for industrial sheet and plate forming applications.
Hopper and Funnel Applications
The machine is suitable for producing tapered components such as hoppers, funnels, reducers, and transition sections.
Multiple Material Options
Suitable configurations can be selected for stainless steel, aluminum, carbon steel, and other compatible metals.
Semi-Automatic Operation
Powered rolling can reduce manual effort while maintaining operator control over material positioning and forming.
CNC-Assisted Solutions
Selected configurations can incorporate CNC or digital control features for repeatable production.
Flexible Industrial Applications
The equipment can be used for machinery, material handling, ductwork, exhaust components, and custom fabrication.
OEM and Custom Support
We can evaluate machine requirements based on drawings, material specifications, dimensions, and production volume.
International B2B Service
We support overseas customers with technical communication, machine configuration, documentation, packaging, shipping coordination, and after-sales assistance.
FAQs
1. What is a semi-automatic cone rolling machine?
It is a powered metal-forming machine designed to roll sheet or plate into conical shapes while retaining operator control over material loading, setup, inspection, and forming.
2. Can it make hopper and funnel shapes?
Yes. Hopper cones, funnels, reducers, transition sections, and other tapered components are common applications for cone rolling equipment.
3. Can it process stainless steel?
Yes. Stainless steel can be processed when the machine has adequate forming capacity for the selected grade, thickness, width, and cone dimensions.
4. Can aluminum be rolled into cones?
Yes. Suitable aluminum sheets or plates can be formed into cones when the machine configuration and forming parameters match the material.
5. Is carbon steel suitable for this machine?
Yes. Carbon steel is a common material for industrial cone, hopper, funnel, and transition-component fabrication.
6. What does semi-automatic operation mean?
It generally means the machine provides powered or controlled forming functions while the operator remains involved in material loading, positioning, setup, monitoring, and inspection.
7. Does the machine support CNC control?
CNC or digital control can be available depending on the machine configuration. The specific automation level should be confirmed according to production requirements.
8. Can it manufacture engine components?
It can be used for suitable conical or tapered engine-related components, but suitability depends on the actual component drawing, material, dimensions, tolerances, and forming requirements.
9. What determines the maximum cone thickness?
Maximum forming thickness depends on material strength, plate width, roller diameter, machine structure, forming force, cone diameter, and other machine parameters.
10. Can the finished cone be welded?
Yes. Rolled cones are often transferred to tack welding and final welding after forming, depending on the component design.
11. Can the machine produce different cone sizes?
Yes, within its adjustment range and rated capacity. The achievable range depends on roller dimensions, machine configuration, material, and required cone geometry.
12. What information is needed to select the machine?
Semi-Automatic Cone Rolling Machine,Semi Automatic Cone Roller,CNC Cone Rolling Machine,Hopper Cone Rolling Machine China, suppliers, manufacturers, factory, customized, wholesale, quotation, made in China