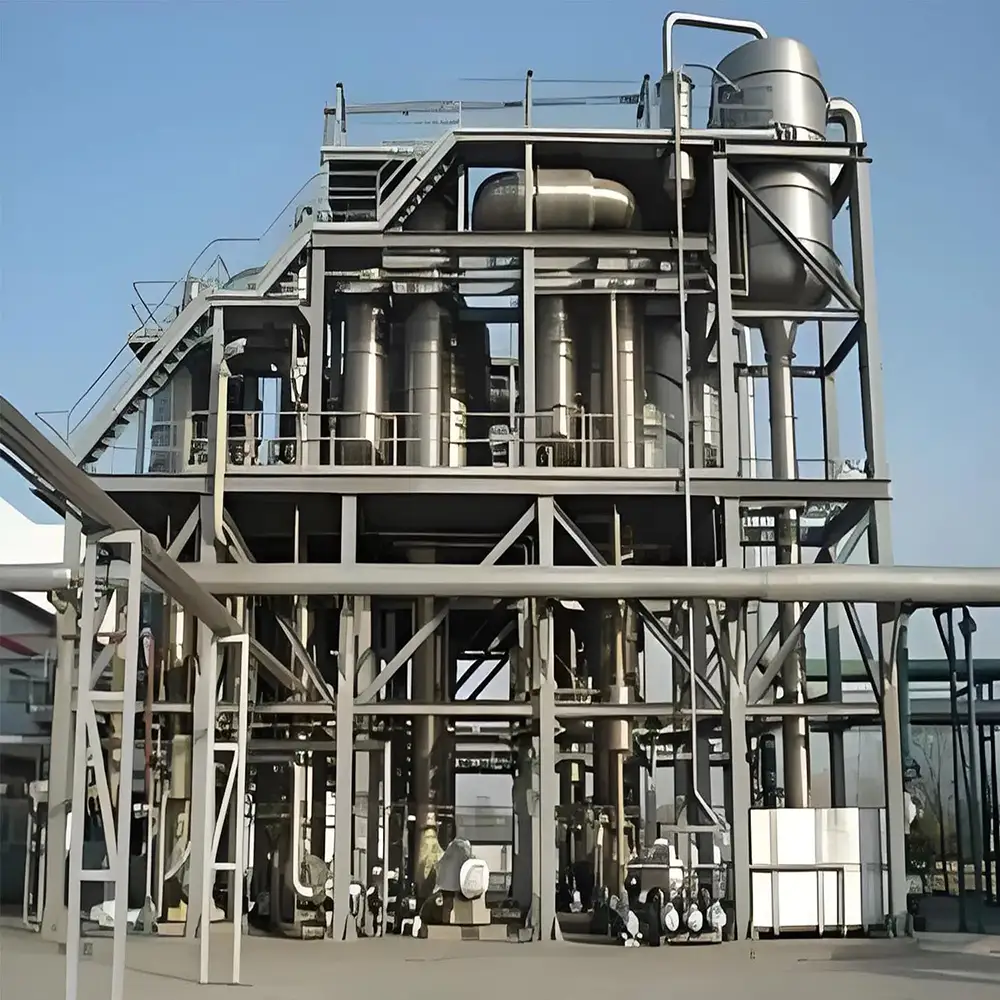
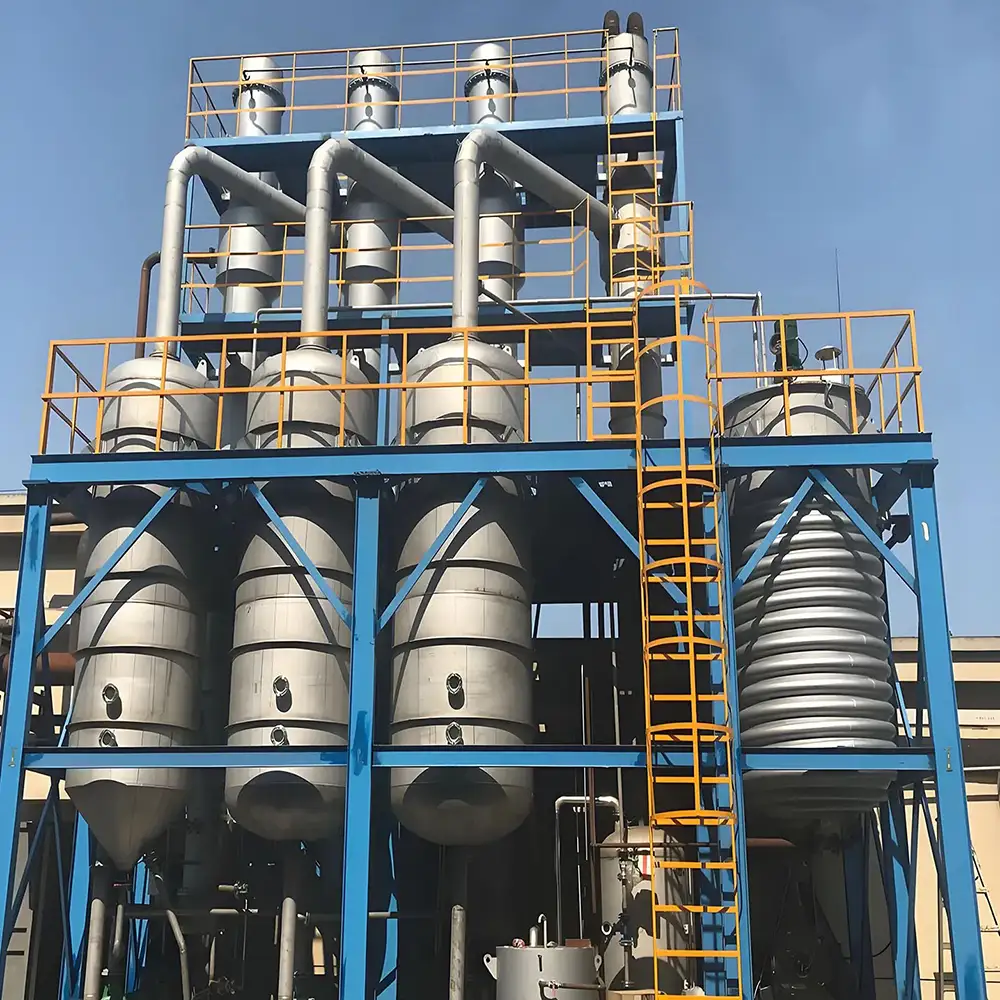
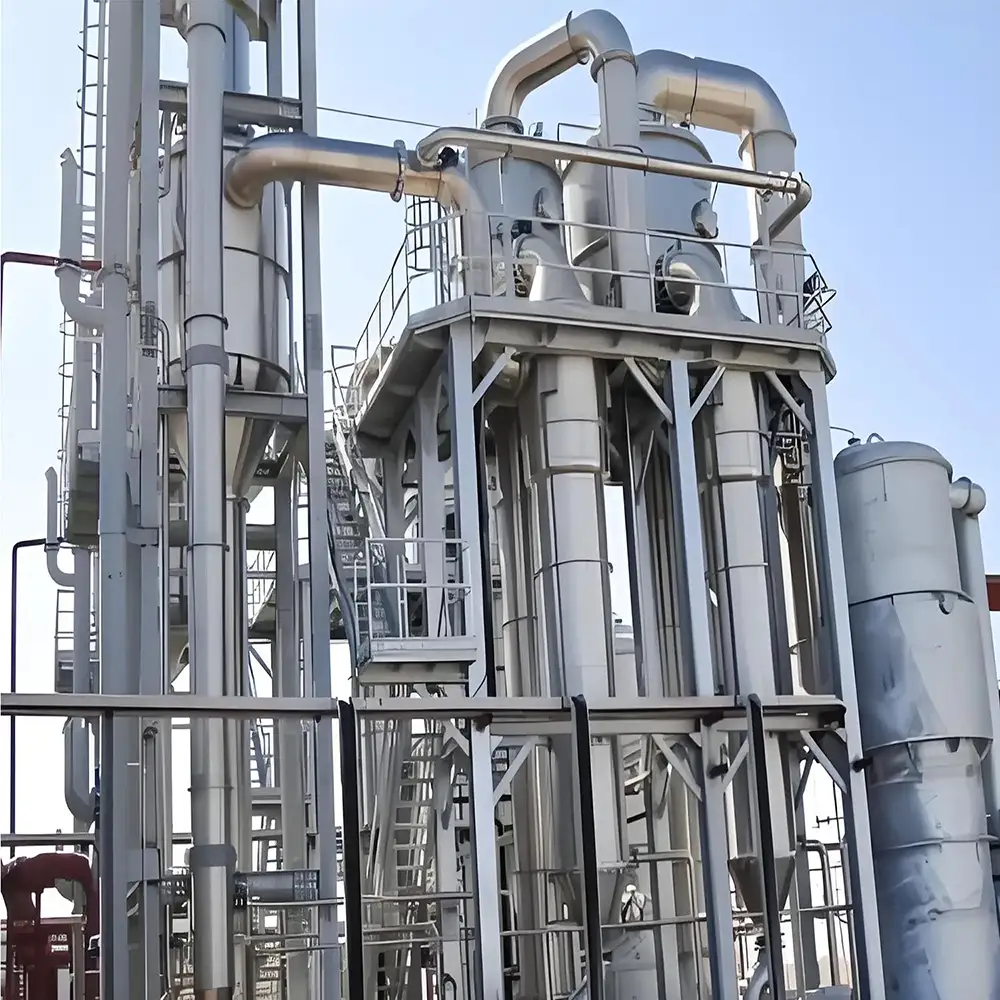
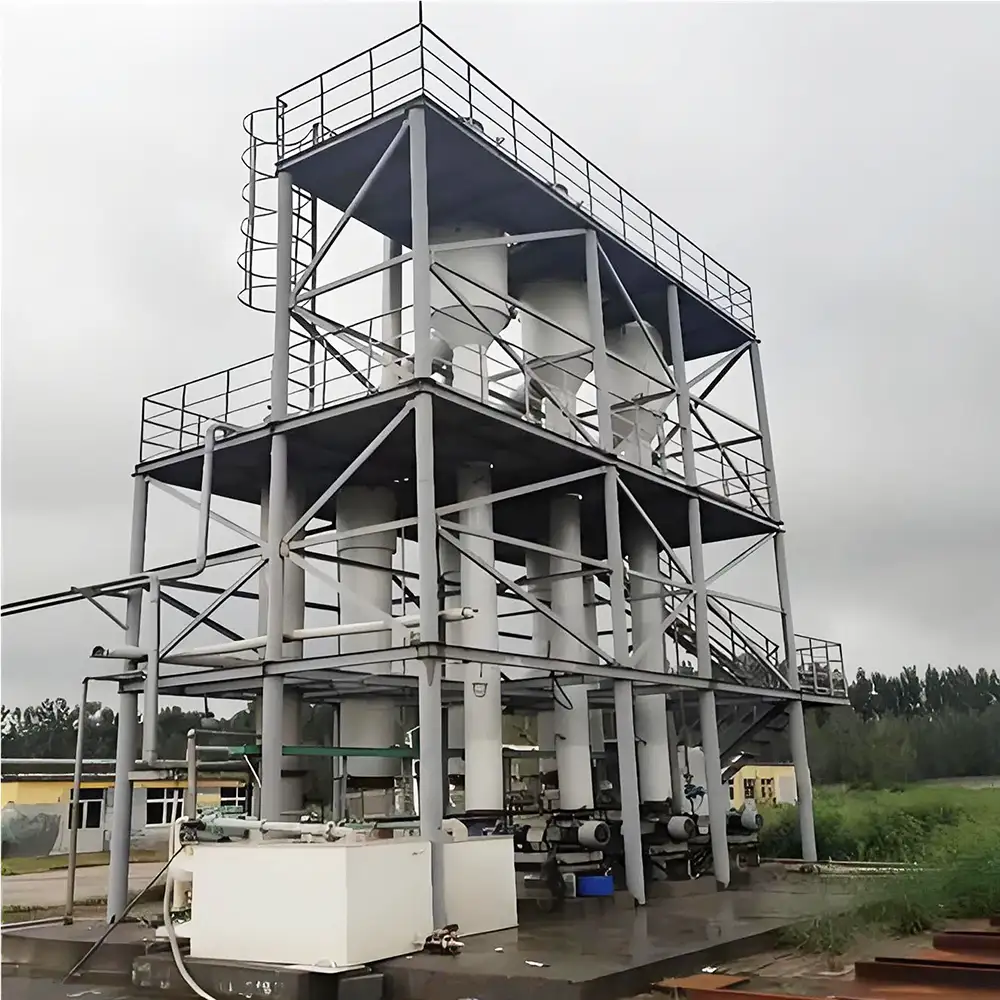
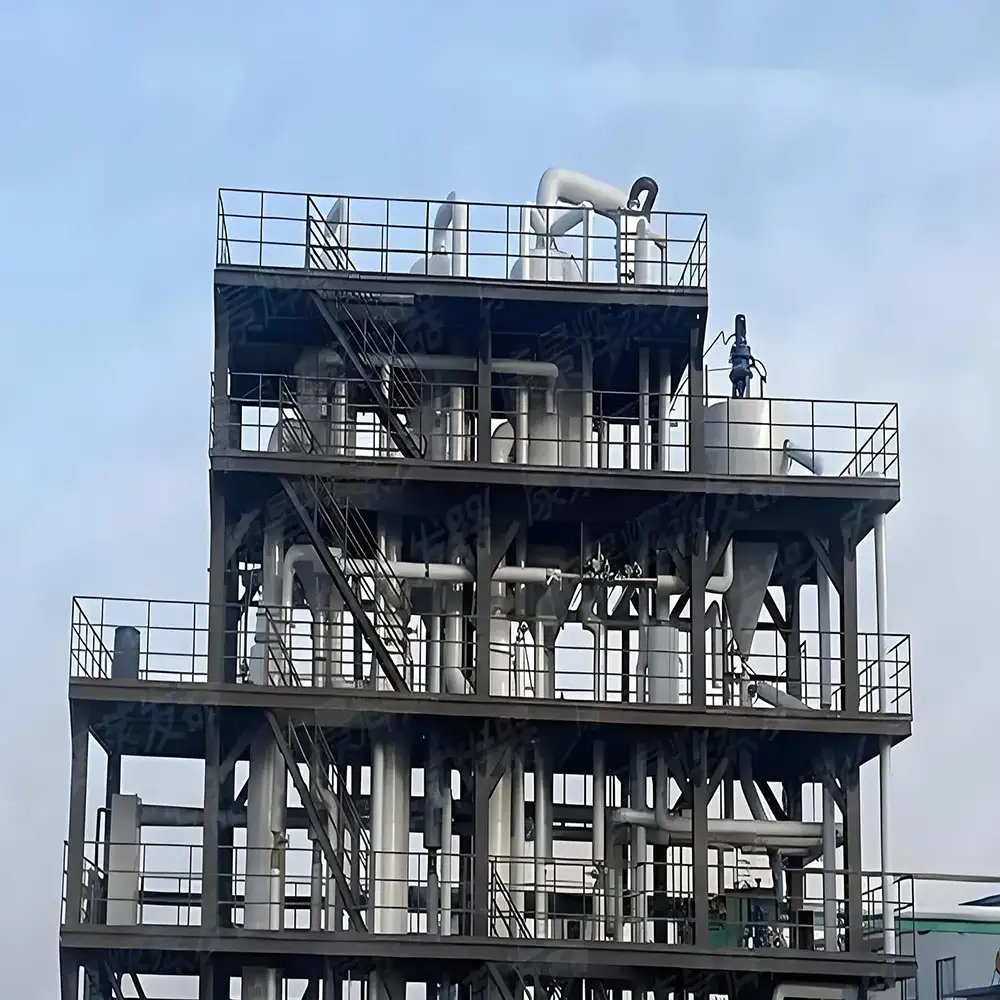
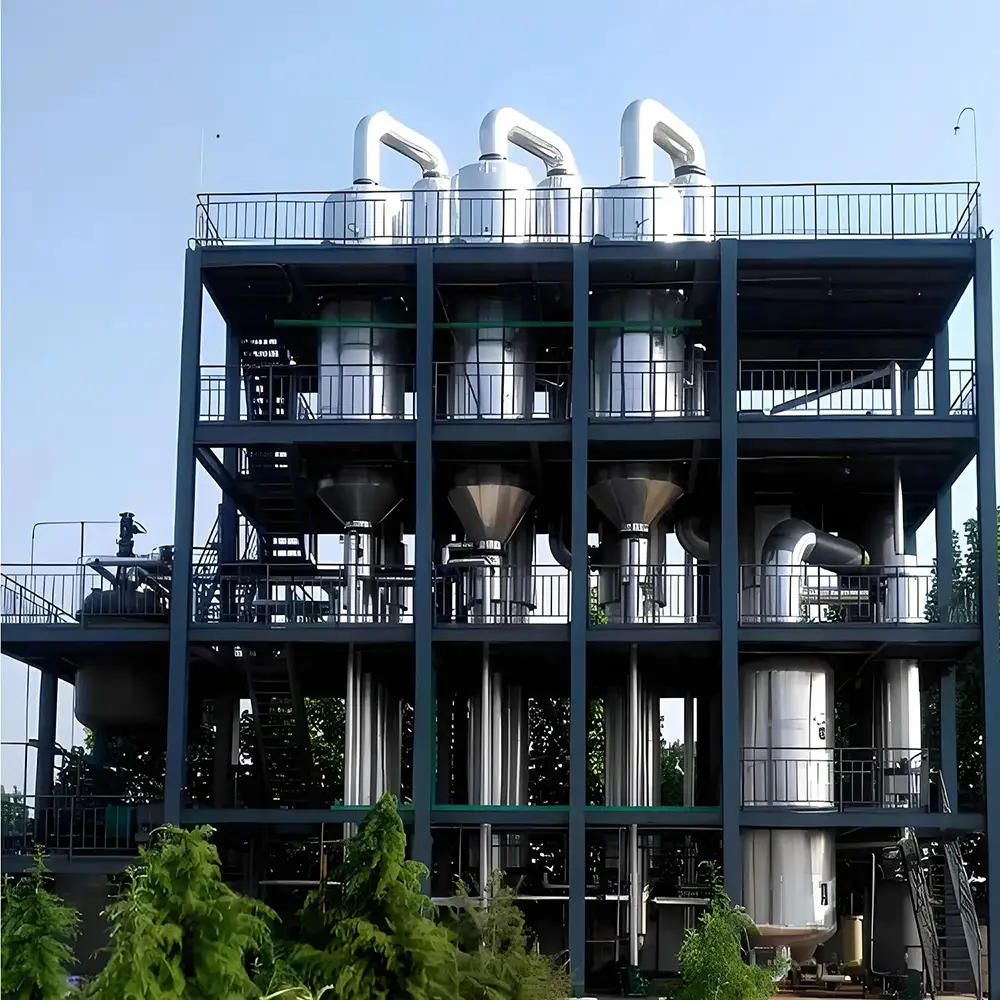
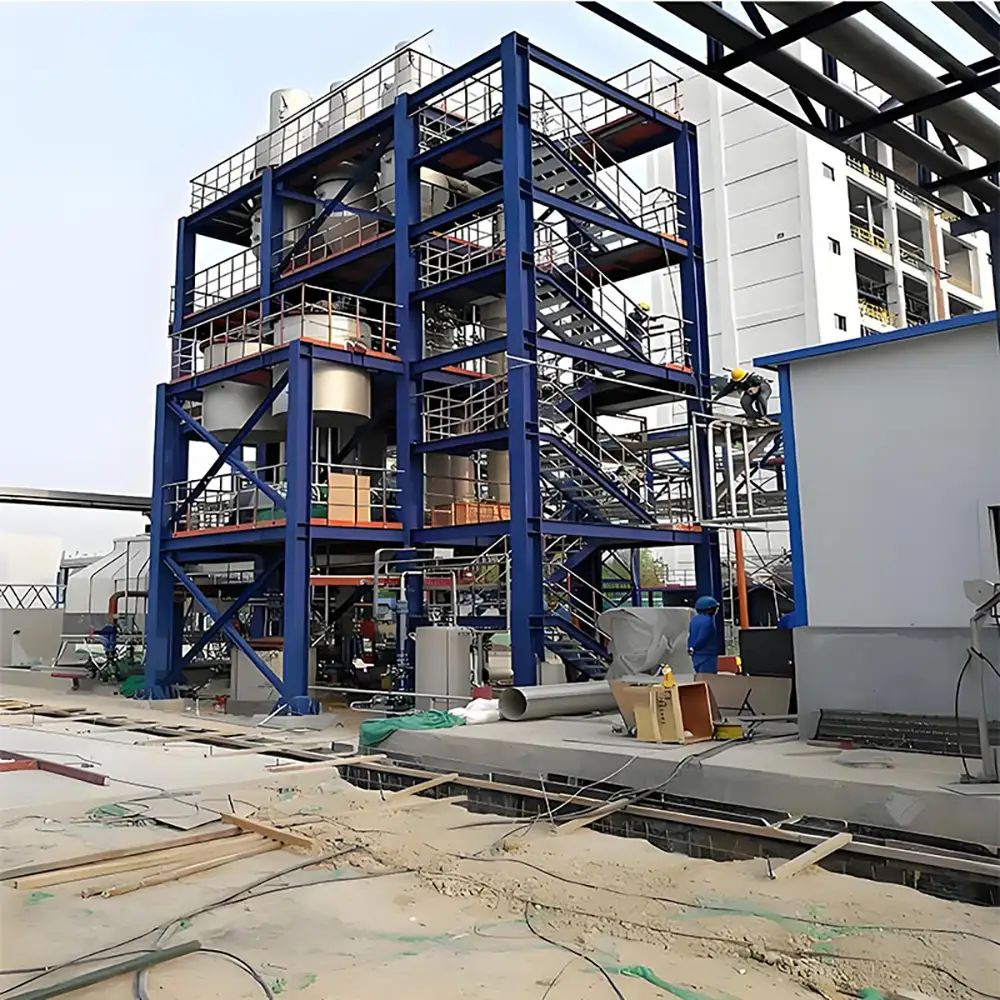
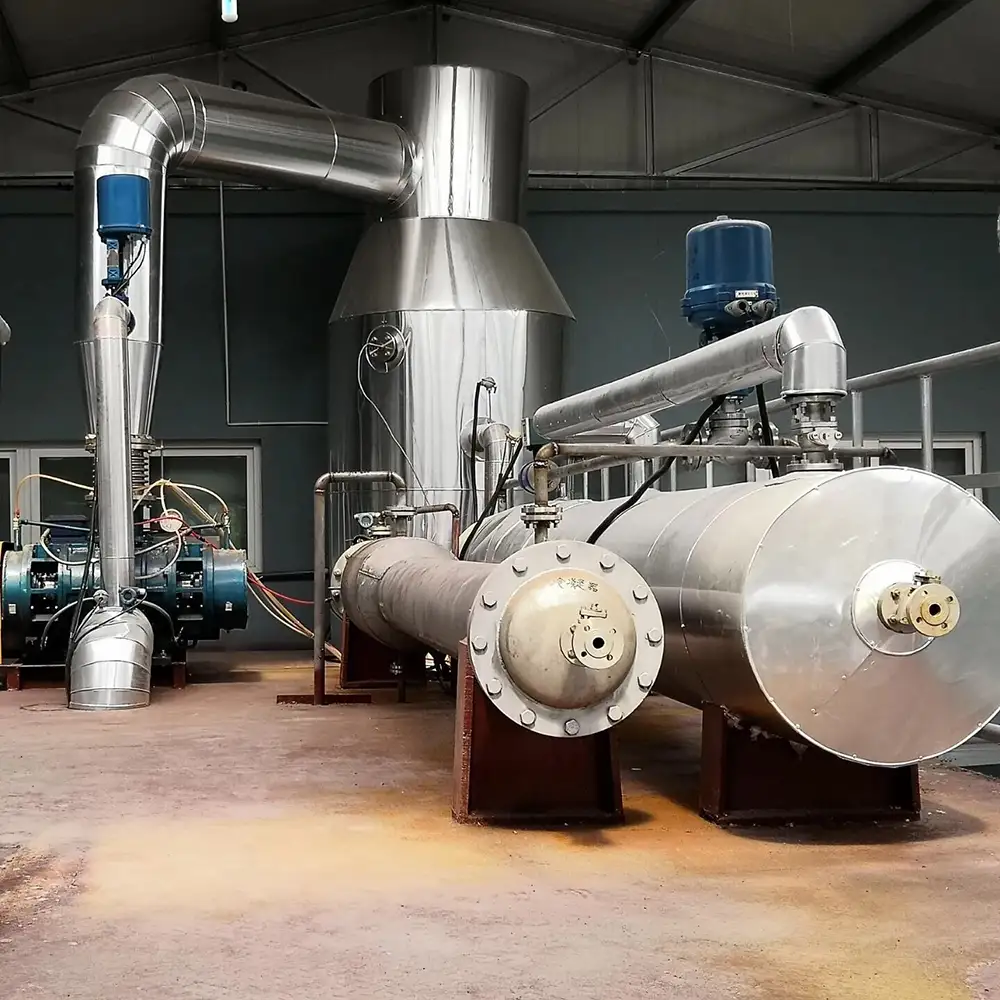
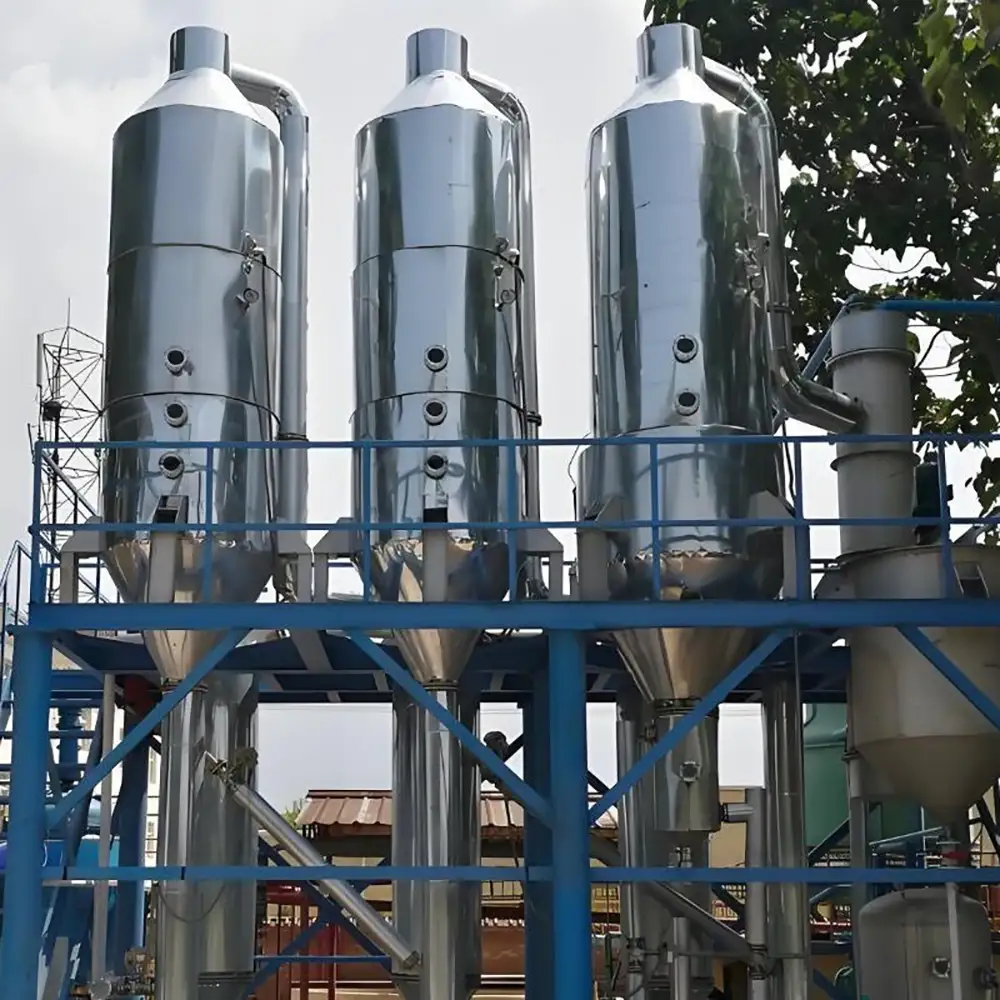
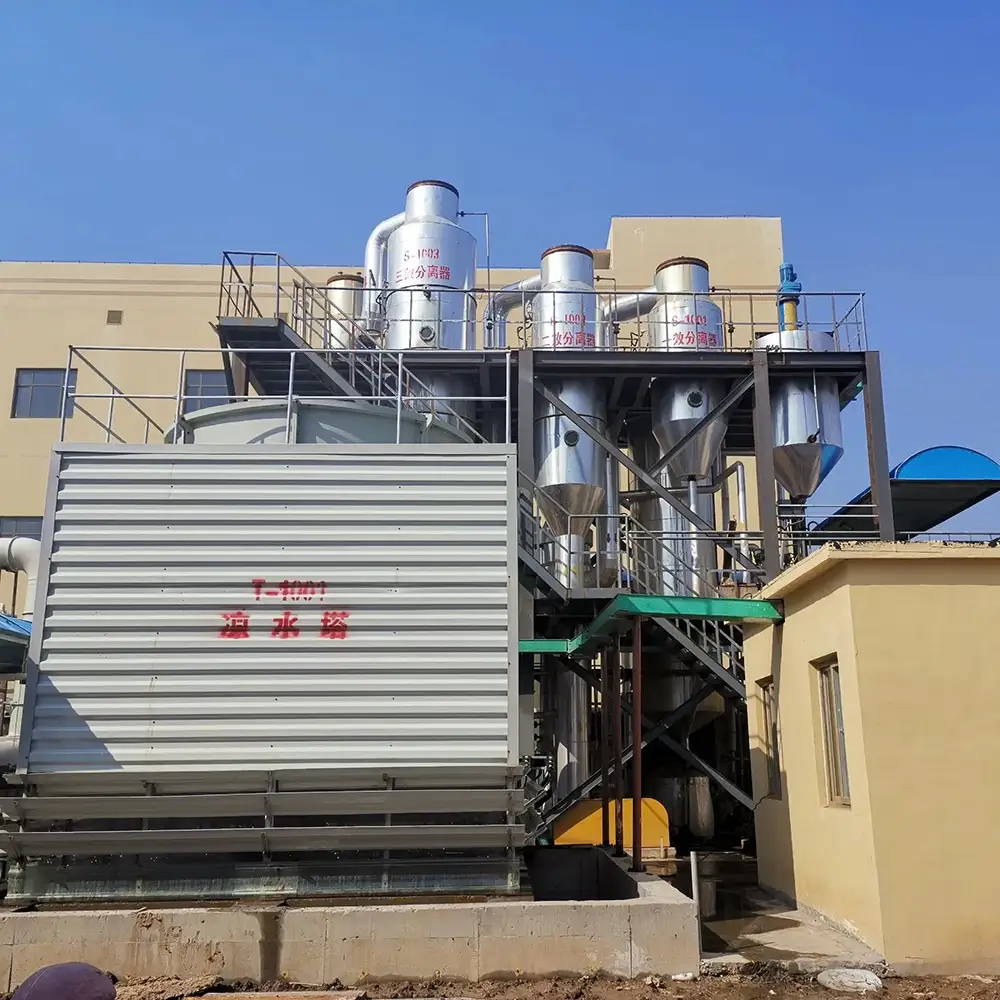
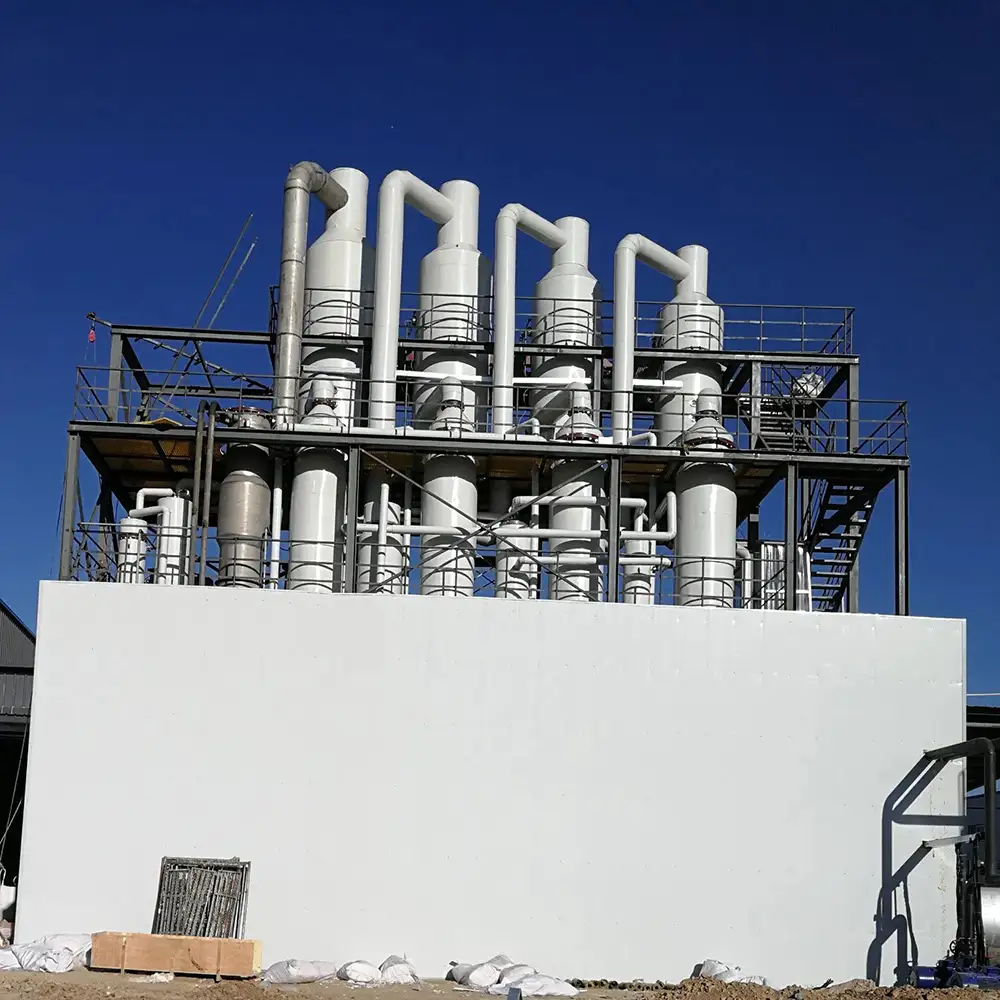
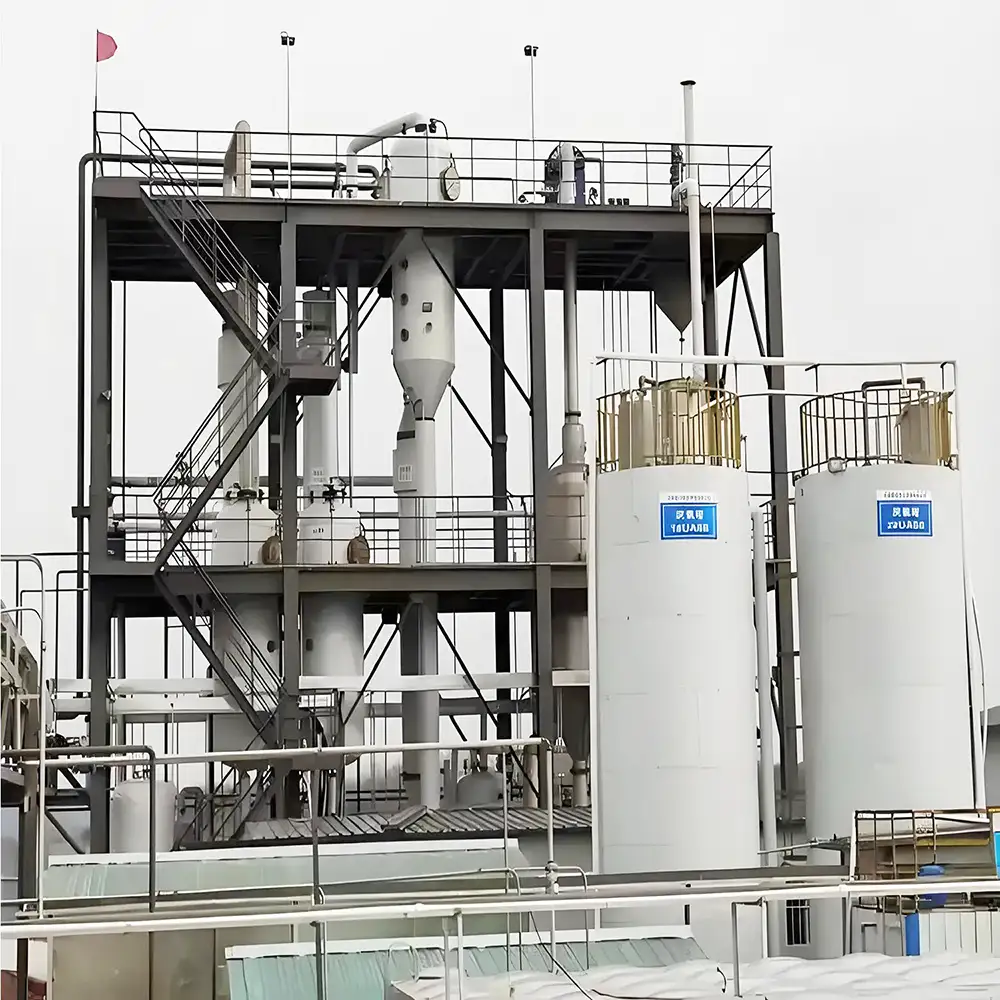
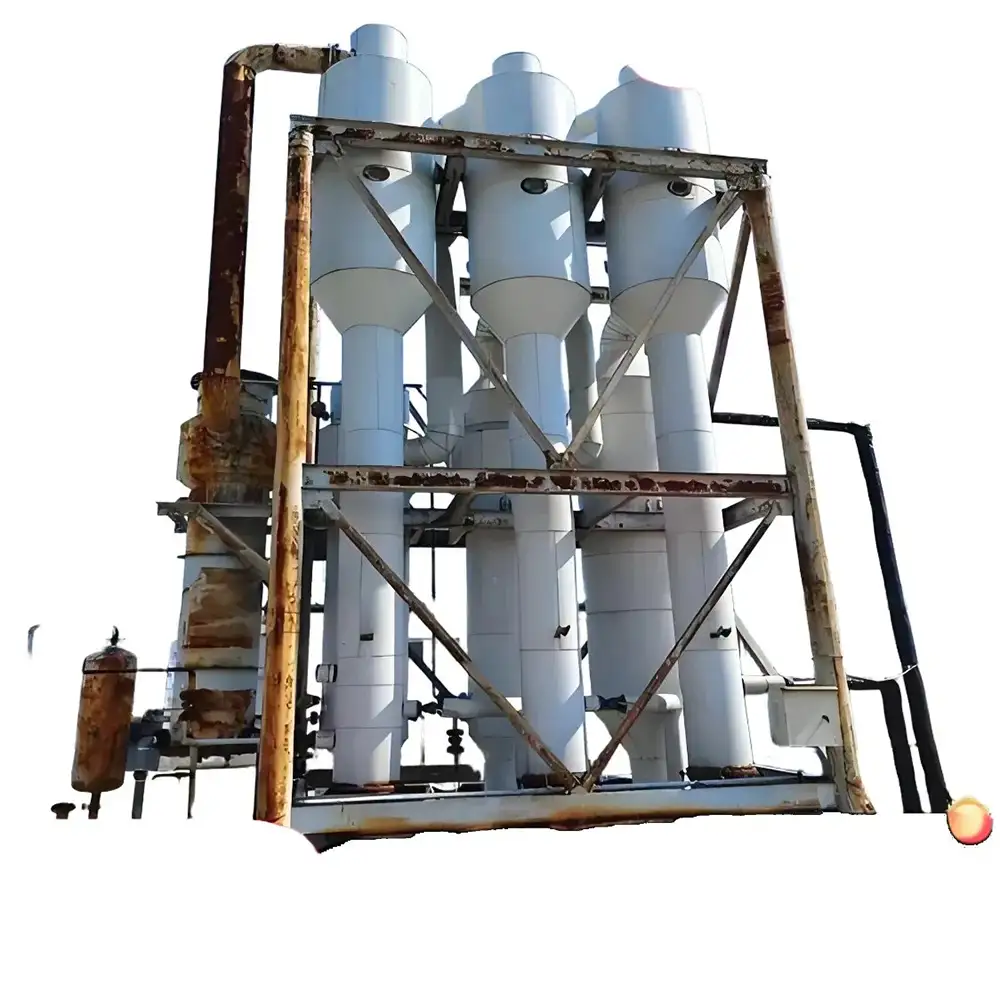
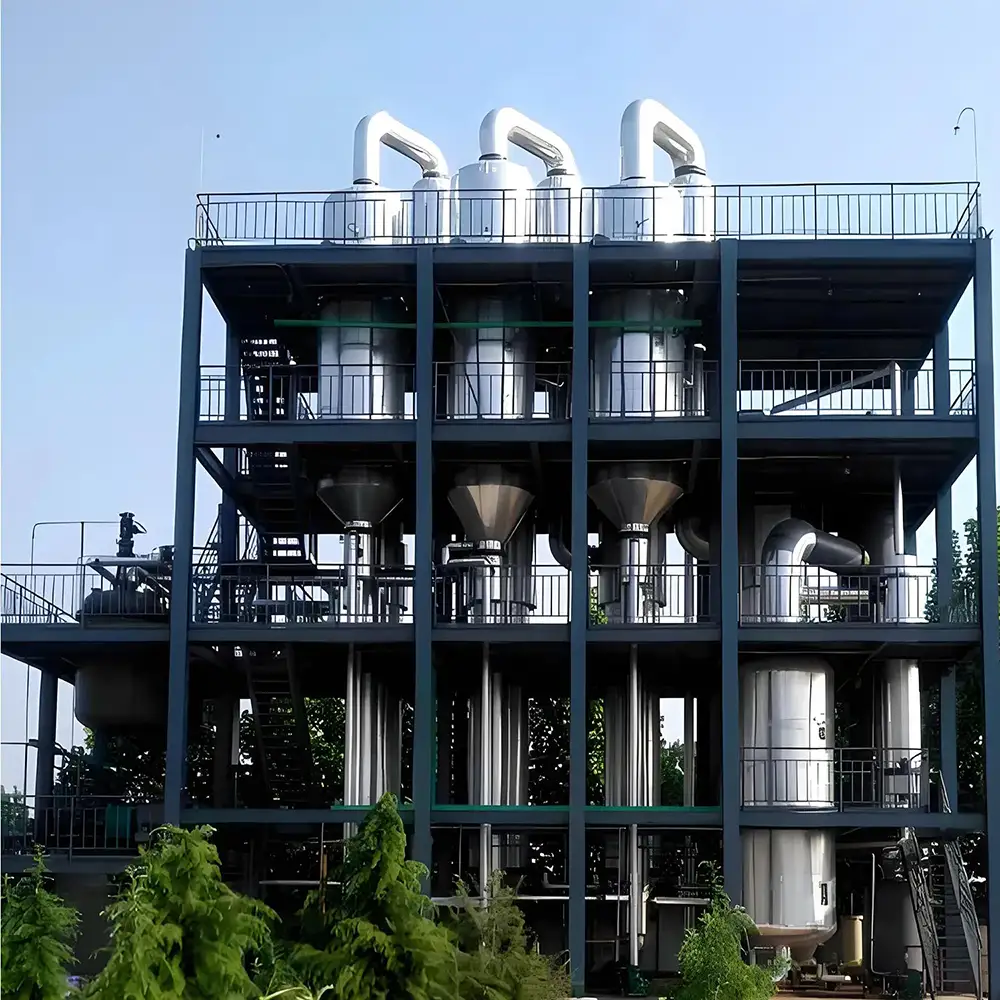
MVR stands for Mechanical Vapor Recovery. MVR is a technology that reuses the energy generated by its own secondary steam to reduce the demand for external energy. This technology is applied in industries such as chemical, pharmaceutical, papermaking, sewage treatment, and seawater desalination.
The working process involves the compression of low-temperature steam by a compressor, which increases the temperature and pressure, increases the enthalpy, and then enters a heat exchanger for condensation to fully utilize the latent heat of the steam. Except for starting the car, only a small amount of steam is required during the entire evaporation process.
In the process of multi effect evaporation, the secondary steam of one effect of the evaporator cannot be directly used as the heat source of the main effect, but can only be used as the heat source of the secondary effect or several secondary effects. As a heat source for this effect, additional energy must be provided to increase its temperature (pressure). The steam jet pump can only compress a portion of the secondary steam, while the MVR evaporator can compress all the secondary steam in the evaporator The solution is circulated in a falling film evaporator through a material circulation pump in the heating tube. The initial steam is heated by fresh steam outside the tube, which heats and boils the solution to produce secondary steam. The generated secondary steam is sucked in by a turbocharged fan, and after being pressurized, the temperature of the secondary steam increases and enters the heating chamber as a heating source for circulating evaporation. After normal start-up, the turbo compressor sucks in secondary steam, which is then pressurized and converted into heated steam. This continuously circulates and evaporates, and the evaporated water is eventually discharged as condensed water.
Reliable MVR Evaporator for Biotechnology and Chemical Industry
The Reliable MVR Evaporator for Biotechnology and Chemical Industry is an advanced industrial evaporation system designed for wastewater concentration, water recovery, and difficult industrial wastewater treatment. Using Mechanical Vapor Recompression (MVR) technology together with multi-effect evaporation principles, the system can significantly reduce wastewater volume while recovering water and concentrating dissolved solids.
Biotechnology and chemical industries generate wastewater with complex compositions, including high concentrations of dissolved organic matter, salts, solvents, nutrients, chemicals, and other contaminants. Conventional biological treatment or membrane processes may not always provide sufficient concentration or final volume reduction.
An MVR evaporation system provides a thermal separation process that can be integrated into industrial wastewater treatment lines, Zero Liquid Discharge (ZLD) systems, and resource recovery processes.
MVR Evaporation Technology
Mechanical Vapor Recompression is an energy-saving evaporation technology that recycles secondary vapor generated during the evaporation process.
Instead of continuously releasing the vapor and requiring a large amount of fresh steam, the MVR system compresses the secondary vapor using a mechanical vapor compressor. Compression increases the vapor pressure and temperature, allowing the vapor to be reused as a heating source.
This recycling of latent heat can substantially reduce external steam consumption compared with conventional single-effect evaporation systems.
MVR technology is therefore particularly attractive for industrial facilities operating continuously and looking to reduce long-term evaporation energy costs.
Multi Effect Evaporation
Multi-effect evaporation uses several evaporation stages operating at different pressures and temperatures. Vapor generated in one effect can be used as the heating source for another effect.
Combining multiple effects with MVR technology provides additional flexibility for optimizing heat utilization and wastewater concentration.
The number of effects and system configuration can be selected according to wastewater flow rate, evaporation capacity, boiling point elevation, required concentration, available utilities, and energy-saving objectives.
Biotechnology Wastewater Treatment
Biotechnology and fermentation processes can generate wastewater containing organic compounds, nutrients, salts, fermentation residues, and other dissolved substances.
The composition of biotechnology wastewater can vary considerably depending on the production process. When conventional treatment cannot economically remove or concentrate certain dissolved components, evaporation can provide an additional treatment stage.
The MVR evaporator can reduce wastewater volume and concentrate non-volatile substances. The resulting condensate can be collected and subjected to additional treatment or reuse depending on its quality.
For biotechnology facilities, the evaporation system can be integrated with pretreatment, biological treatment, filtration, membrane concentration, crystallization, and other processes.
Chemical Industry Wastewater Treatment
Chemical production can generate wastewater containing inorganic salts, organic compounds, acids, alkalis, solvents, and other complex substances.
MVR evaporation is suitable for selected chemical wastewater streams because thermal separation does not depend on microorganisms and can handle high concentrations of dissolved solids.
The system can be configured according to wastewater characteristics, including pH, salt concentration, COD, TDS, suspended solids, viscosity, boiling point elevation, and scaling tendency.
Proper pretreatment is important for protecting the evaporator and maintaining stable heat-transfer performance.
Wastewater Concentration and Volume Reduction
One of the main purposes of an industrial evaporator is to reduce the volume of wastewater requiring final disposal.
During evaporation, water is converted into vapor while non-volatile substances remain in the concentrated liquid. The vapor is subsequently condensed to produce recovered water.
By reducing wastewater volume, the system can lower the amount of concentrated waste requiring downstream treatment, crystallization, drying, or disposal.
This makes MVR evaporation particularly useful as a concentration stage before crystallization or ZLD treatment.
Condensate Recovery
The vapor generated during evaporation can be condensed through a dedicated condenser or heat-transfer system.
Depending on the wastewater composition and treatment configuration, the condensate may have significantly lower concentrations of dissolved solids than the original wastewater. It can then be further polished through filtration, activated carbon, RO, or other suitable treatment processes.
Recovered water may be reused for selected industrial applications when it meets the required quality specifications.
Water recovery can reduce freshwater consumption and improve overall plant resource efficiency.
Zero Liquid Discharge Applications
MVR evaporation is frequently considered as part of a Zero Liquid Discharge system.
A typical ZLD process may include pretreatment, filtration, RO concentration, MVR evaporation, crystallization, and solid-liquid separation.
The MVR evaporator concentrates the liquid stream to a high solids content, while a downstream crystallizer can further process the concentrated brine and convert dissolved salts into solid crystals.
The exact ZLD configuration depends on wastewater chemistry, target recovery rate, salt composition, scaling potential, and required solid handling method.
Automatic Operation and Process Control
Reliable industrial evaporation requires accurate monitoring of operating conditions.
The MVR system can use sensors and automated controls to monitor feed flow, temperature, pressure, vacuum level, liquid level, conductivity, circulation flow, compressor operation, and other important parameters.
Automated valves, pumps, control instruments, and safety systems can coordinate different process stages.
Automatic operation reduces manual intervention and helps maintain stable evaporation conditions during continuous industrial production.
Energy Efficiency and Operating Cost
Energy consumption is one of the most important factors when evaluating wastewater evaporation equipment.
The MVR compressor recycles vapor energy within the system, reducing the need for continuous external steam input. Proper heat-transfer design and optimized evaporation conditions can further improve thermal efficiency.
Although actual energy consumption depends on wastewater characteristics and evaporation capacity, MVR technology is generally well suited to applications where the system operates for long periods and energy costs are a major consideration.
Industrial Applications
The MVR multi-effect evaporator can be applied to many industrial wastewater treatment processes, including:
Biotechnology Wastewater
Pharmaceutical Wastewater
Chemical Industry Wastewater
Fermentation Wastewater
Food Processing Wastewater
High-Salt Wastewater
High-TDS Wastewater
Brine Concentration
Industrial Wastewater Reuse
Zero Liquid Discharge Systems
The equipment configuration should be selected according to the actual wastewater composition and required treatment objectives.
Maintenance and Long-Term Reliability
Evaporation equipment requires proper maintenance to preserve heat-transfer efficiency and operating stability.
Scaling, fouling, corrosion, and crystallization can affect performance depending on wastewater characteristics. Appropriate pretreatment, regular cleaning, correct operating parameters, and suitable material selection can help reduce these risks.
Important components such as the vapor compressor, heat exchangers, circulation pumps, valves, sensors, condensers, and control system should be inspected according to the recommended maintenance schedule.
Why Choose Us
Selecting an MVR evaporator requires careful consideration of wastewater characteristics, evaporation capacity, energy consumption, concentration requirements, and downstream treatment.
Our industrial evaporation solutions focus on:
MVR Energy Recovery: Mechanical vapor recompression recycles secondary vapor energy.
Multi-Effect Operation: Multiple evaporation stages can improve overall heat utilization.
Industrial Wastewater Treatment: Suitable for selected biotechnology, chemical, pharmaceutical, and high-salt wastewater streams.
High Concentration Capability: Supports significant wastewater volume reduction and dissolved-solids concentration.
Water Recovery: Condensate can be collected for further treatment and potential reuse.
ZLD Integration: Can be integrated with RO, crystallization, and solid-liquid separation systems.
Automatic Operation: Process monitoring and control support stable continuous operation.
Flexible Configuration: System design can be matched to wastewater composition and plant capacity.
Long-Term Efficiency: Energy-saving operation can help reduce operating costs for suitable continuous applications.
Frequently Asked Questions
1. What is an MVR evaporator?
An MVR evaporator uses a mechanical vapor compressor to recycle secondary vapor generated during evaporation and reuse its heat, reducing the need for fresh steam.
2. Can MVR evaporators treat chemical wastewater?
Yes. MVR evaporation can be used for suitable chemical wastewater streams, especially wastewater containing high concentrations of dissolved salts and non-volatile substances.
3. Is MVR suitable for biotechnology wastewater?
Yes. It can be applied to selected biotechnology and fermentation wastewater streams for concentration, water recovery, and downstream ZLD treatment.
4. What is a multi-effect evaporator?
A multi-effect evaporator uses multiple evaporation stages operating at different pressure and temperature levels, allowing vapor from one stage to provide heat for another.
5. What is the main advantage of MVR technology?
The main advantage is energy recovery. Secondary vapor is compressed and reused as a heating source, which can significantly reduce external steam requirements in suitable applications.
6. Can the system recover water?
Yes. Water evaporated from the wastewater is condensed into condensate, which can be further treated and potentially reused depending on its quality.
7. Can MVR evaporation be used for ZLD?
Yes. MVR evaporation can serve as a key concentration stage in ZLD systems and can be combined with crystallization and solid-liquid separation.
8. Does the system require pretreatment?
Pretreatment may be necessary depending on suspended solids, hardness, scaling compounds, oils, organic matter, and other wastewater characteristics.
9. Can the evaporator handle high-salt wastewater?
Yes. MVR evaporation is suitable for many high-salinity wastewater applications, although the specific salt composition and scaling tendency must be evaluated.
10. What information is needed to select an MVR evaporator?
Important parameters include wastewater flow rate, composition, TDS, COD, pH, salt concentration, temperature, boiling point elevation, required evaporation capacity, final concentration, condensate quality, and operating hours.
Prev:
Automatic Yeast Waste Water Industrial M Falling Film Vacuum Evaporator for High-Salt Wastewater Crystallization
Next:
Vacuum Industrial Multi Effect Mvr Evaporator for Waste Water Treatment
TAG:
Industrial Wastewater Treatment Equipment,
Food Industry Wastewater Treatment,
Industrial Wastewater Treatment System,
Industrial Wastewater Treatment,
Wastewater Reuse System,
Chemical Wastewater Treatment,
Chemical Wastewater Treatment Equipment,
ZLD Wastewater Treatment,
ZLD Evaporator,
Zero Liquid Discharge,
Wastewater Volume Reduction,
Brine Concentration Equipment,
High Salinity Wastewater Treatment,
High Salt Wastewater Treatment,
Brine Evaporation System,
Multi Effect Evaporation System,
Multiple Effect Evaporator,
MVR Evaporation System,
Mechanical Vapor Recompression Evaporator,
Mechanical Vapor Recompression System,
Industrial Evaporation Equipment,
Industrial Evaporation System,
Wastewater Concentration Equipment,
Wastewater Concentration System,
High TDS Wastewater Treatment,
High TDS Wastewater Evaporator,
Industrial Wastewater Evaporation,
Wastewater Evaporation System,
Industrial Wastewater Crystallizer,
MVR Evaporator,
Related Category:
MVR Evaporator, MVR Wastewater Evaporator, Multi Effect Evaporator, Industrial Wastewater Evaporator, Biotechnology Wast China, suppliers, manufacturers, factory, customized, wholesale, quotation, made in China