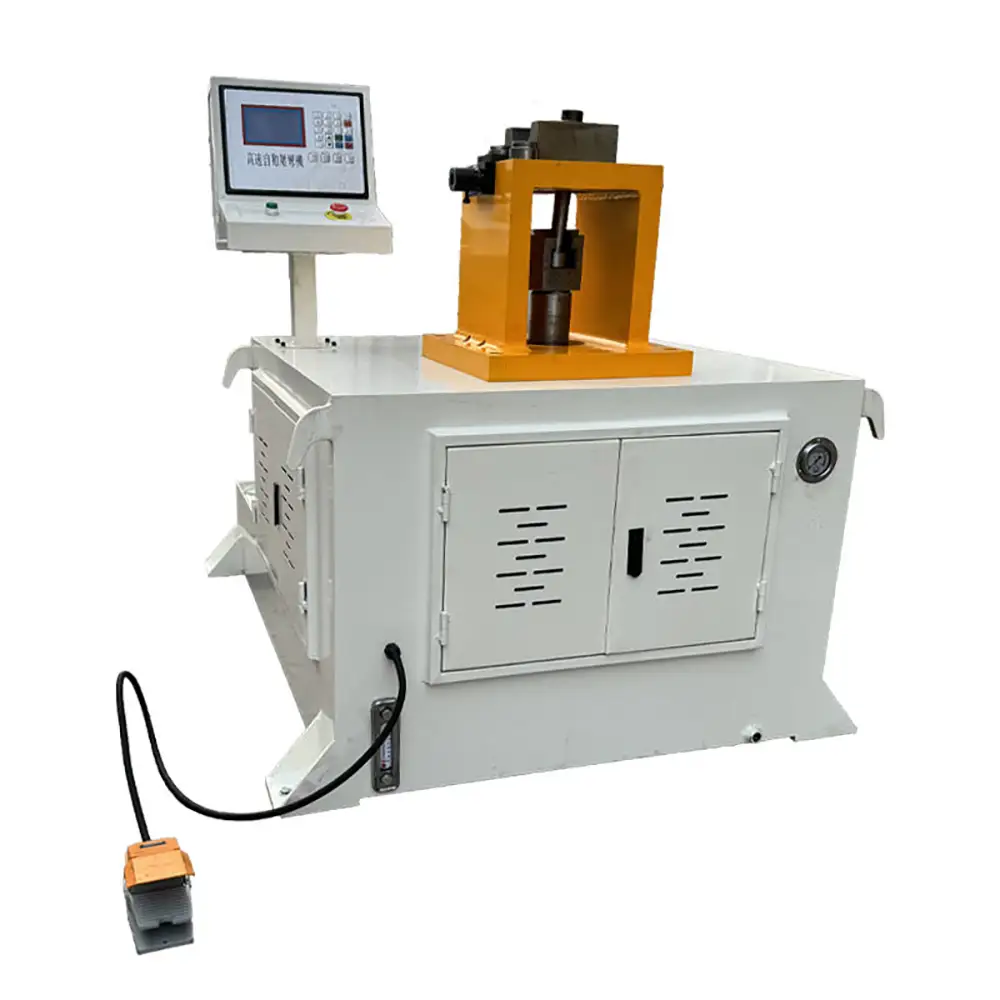
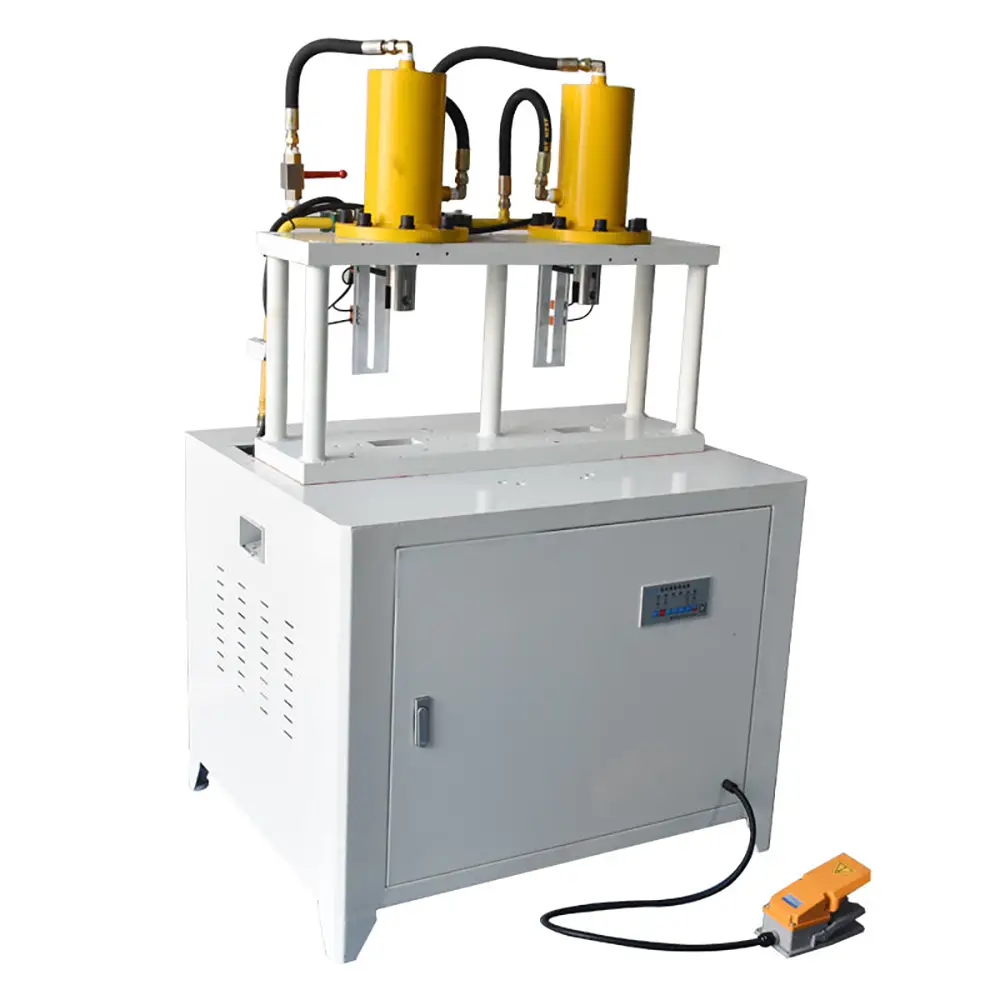
Equipment configuration and functional characteristics:
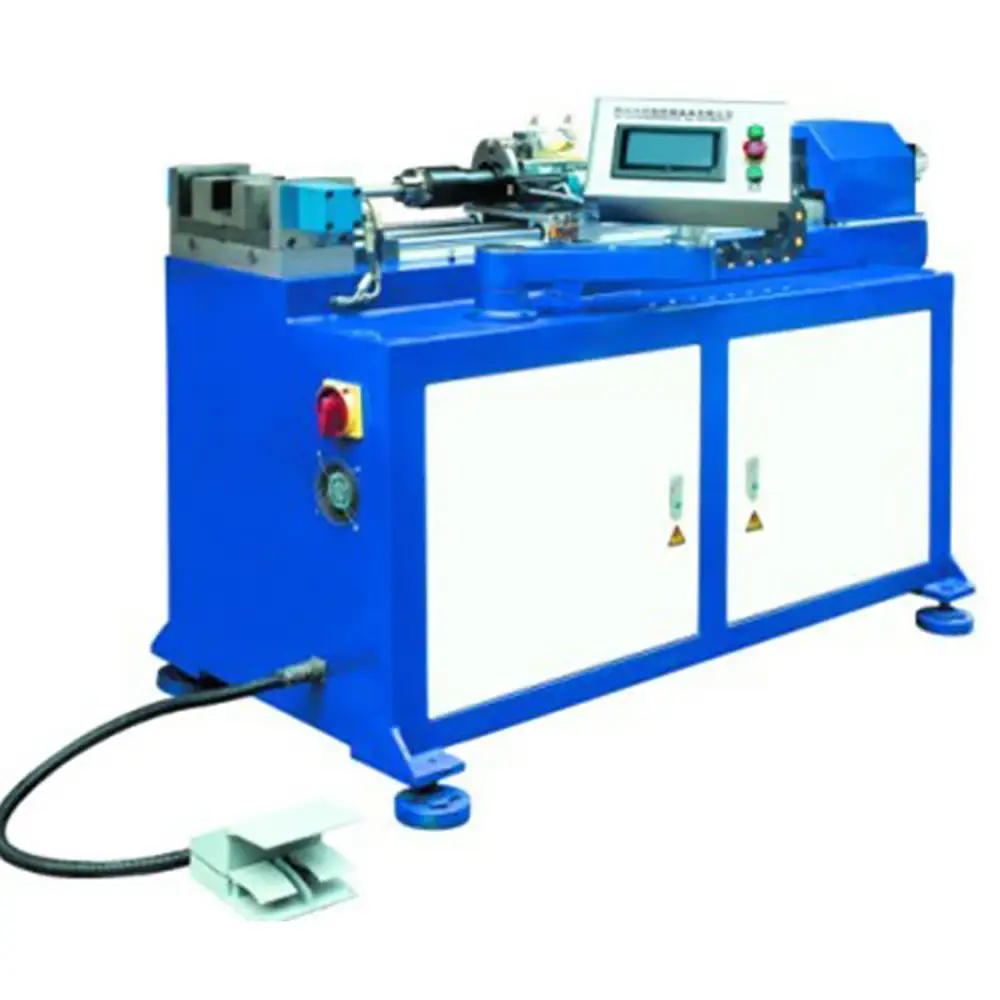
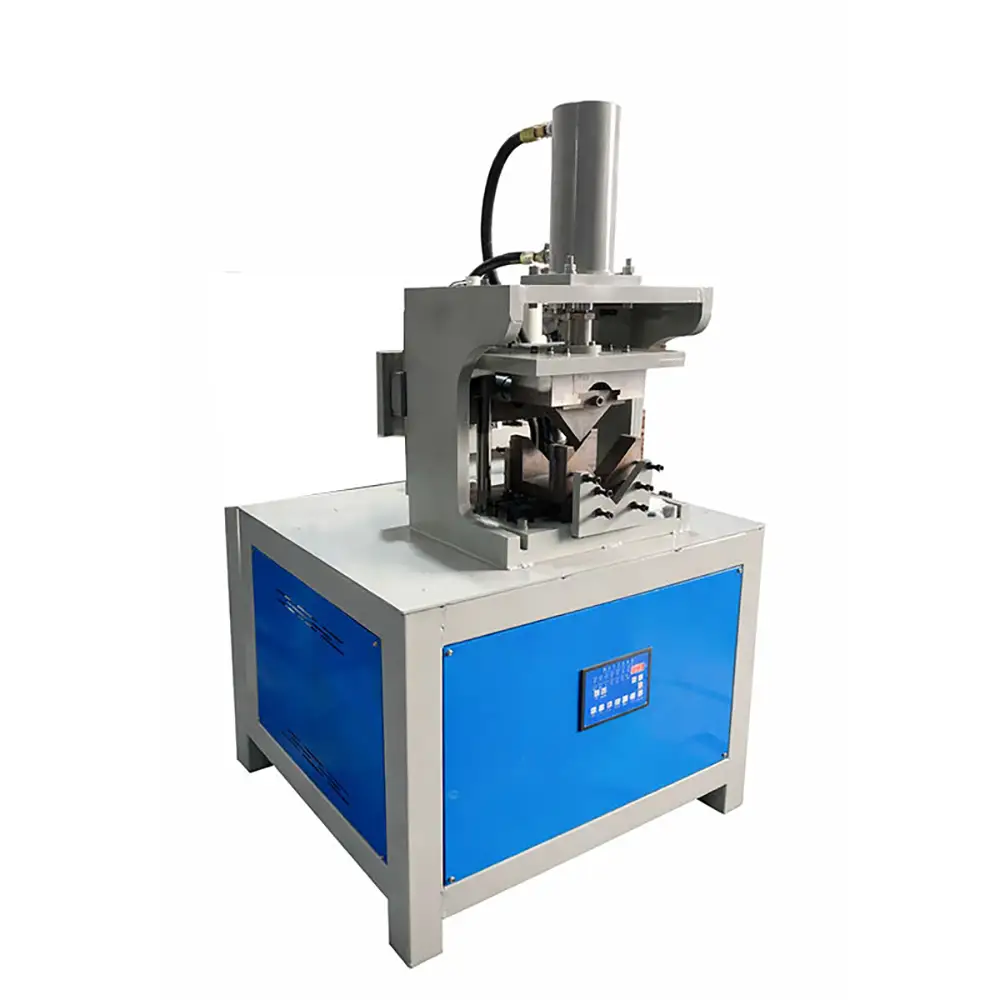
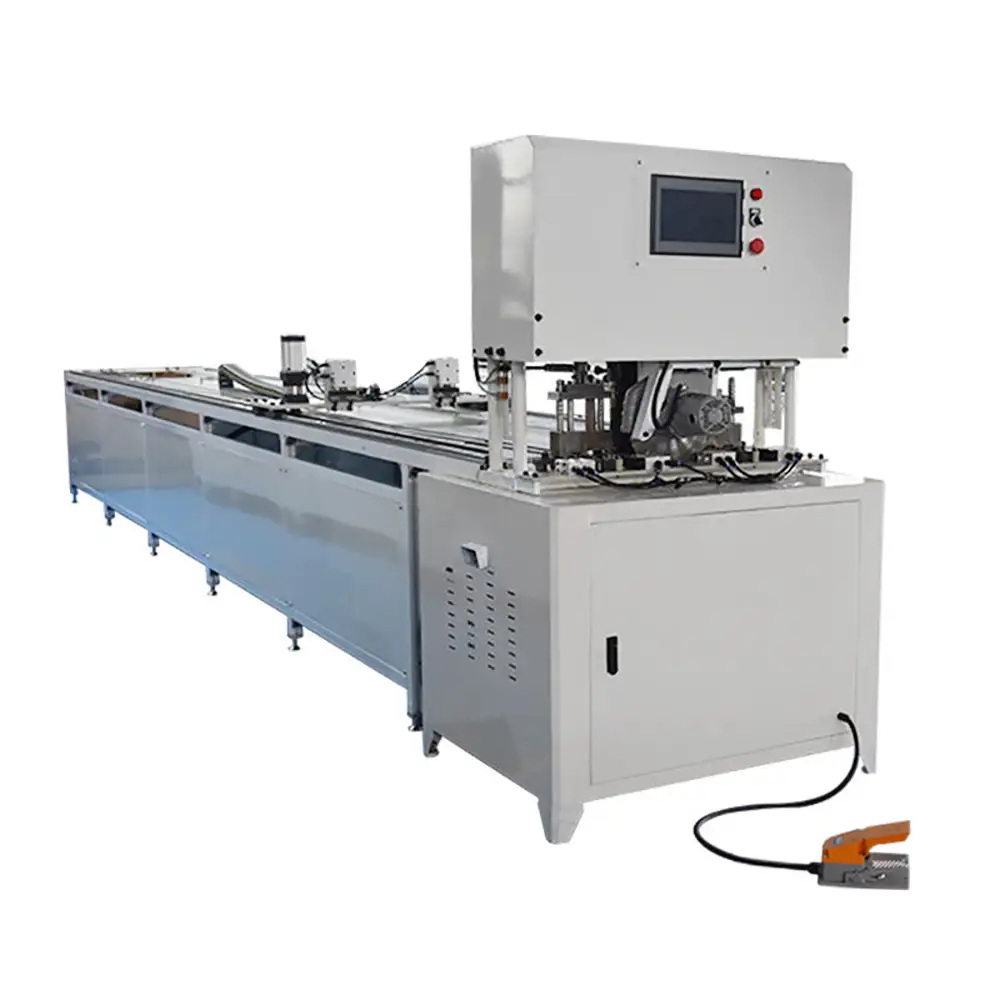
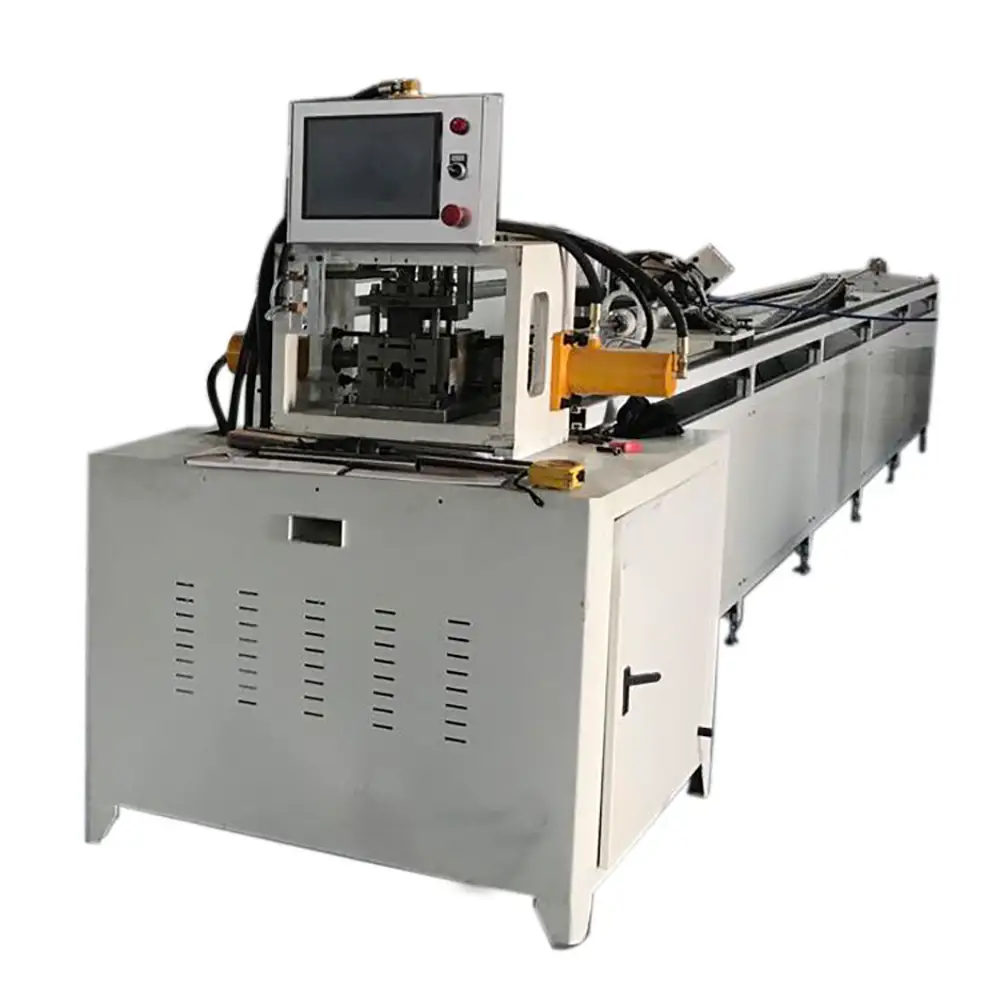
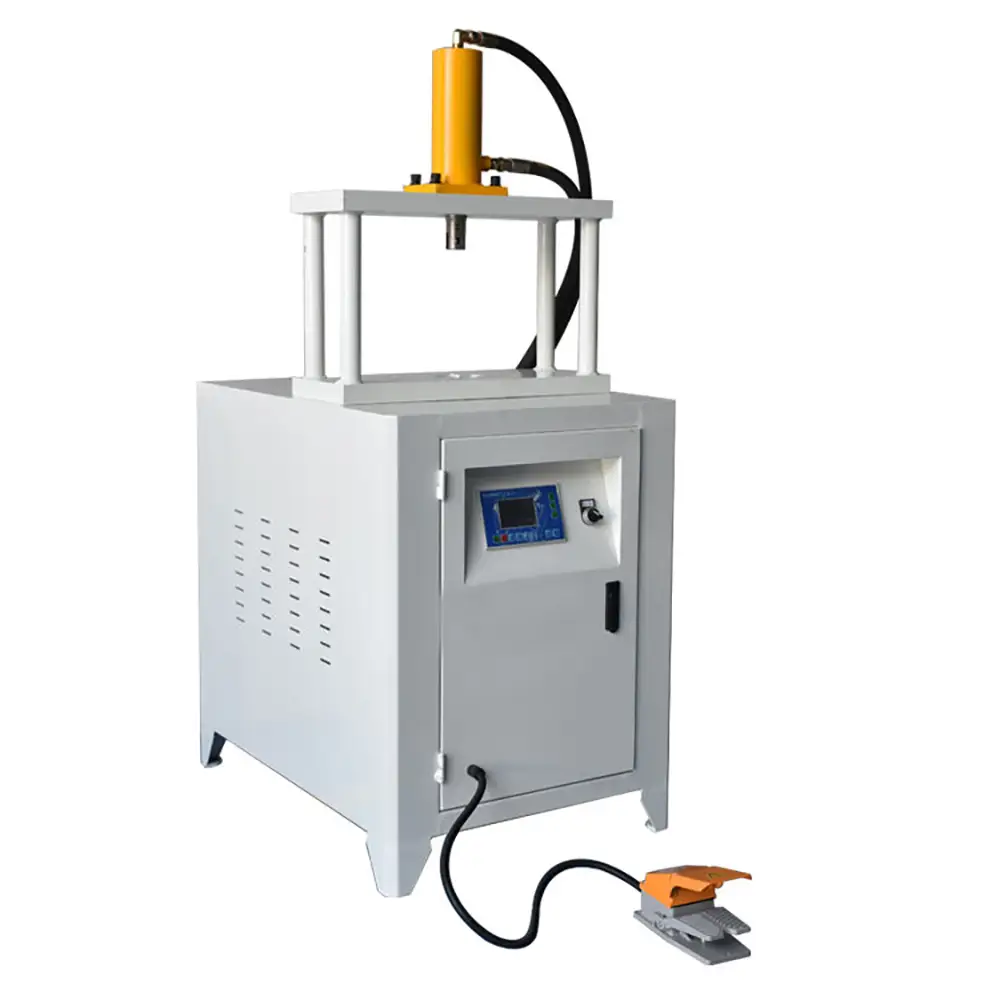
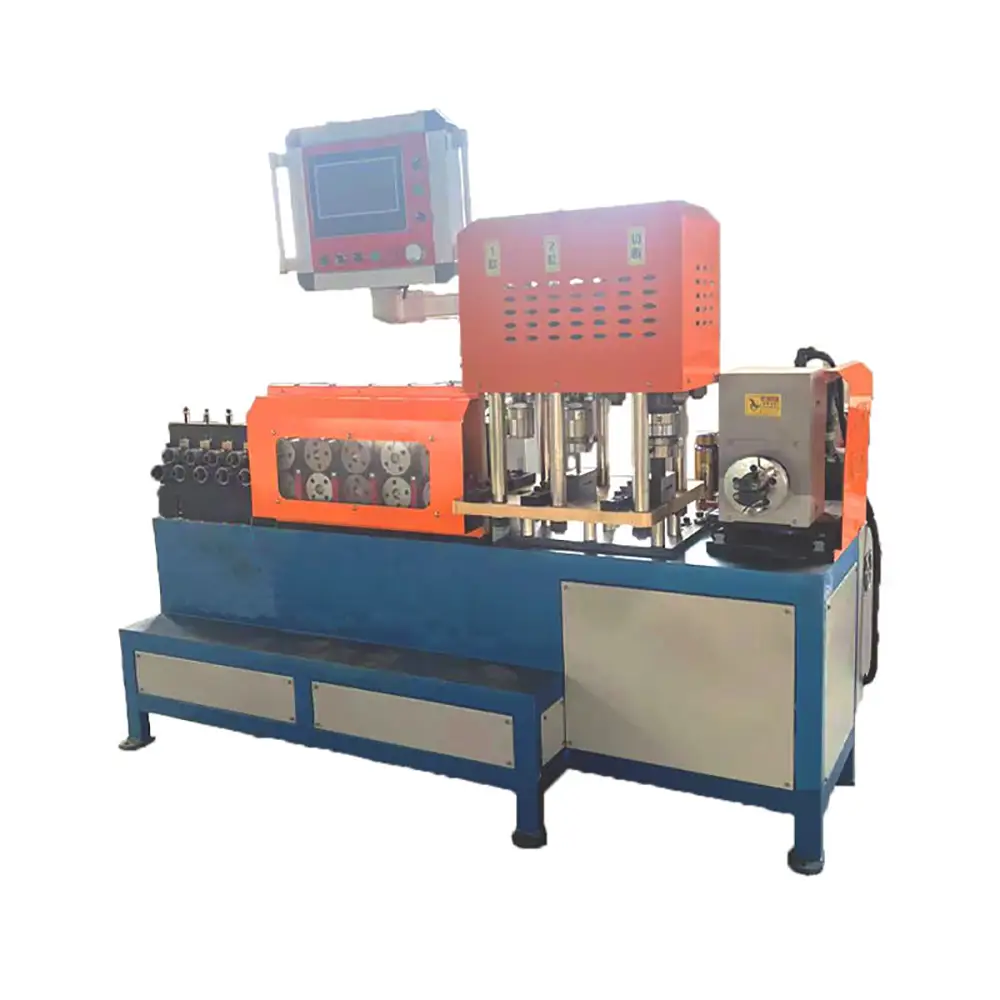
1. This machine is composed of main body, punching and flanging mechanism, feeding mechanism, rotating mechanism, clamping mechanism, hydraulic system, electric control system and cooling system.
2. The machine body structure adopts welded parts, the national rectangular tube and the steel plate are welded and subjected to vibration aging treatment, then the entire worktable is milled by gantry milling to prevent the bed from deforming.
3. The hydraulic system is cooled by a water cooler to ensure that the equipment's hydraulic system dissipates well.
4. The configuration of the hydraulic system components is: the hydraulic station motor, oil pump, solenoid valve are all domestic brands;
5. Parts electroplating, blackening, quenching, carburizing, electrostatic spraying, painting, etc.
6. The feeding mechanism adopts ball screw + linear shaft transmission, and is driven by a servo motor, so as to achieve precise displacement of the workpiece.
7. The rotating mechanism is driven by a servo motor, so that the workpiece can be accurately displaced by 360 ° rotation.
8. The workpiece clamping mechanism is driven by an oil cylinder, and the punching and flanging mechanism is driven by an oil cylinder. It is composed of an outer sleeve, an inner core rod, a punching and flanging die and a clamping die. The service life of the conventional punch die meets 80,000-100,000 times (holes) / support, and the material uses imported die steel.
9. The whole machine adopts PLC + Delta touch screen as the core controller. The operation electric box is arranged above the left side of the bed. The operation electric box is arranged with relevant operation buttons, indicators and counters. The proximity switch adopts French Schneider.
10. The equipment control system has an automatic counting function, which automatically reaches the set output shutdown alarm function, which can count the number of processing and facilitate production management.
|
Item |
Parameter |
|
Max processing OD |
50mm carbon steel |
|
Max processing pipe Thickness |
1.5mm SS pipe |
|
Punching and flanging hole |
10mm-20mm(customized ) |
|
Minimum center distance between holes |
67mm(customized) |
|
Flanging height |
2.5mm-3.0mm(according to the stretch of pipe material) |
|
Maximum length of feeding |
1400mm |
|
Number of hole, hole diameter and hole position |
Set program according to drawings |
|
Maximum pipe length |
1400mm(customized) |
|
Punching and flanging efficiency |
7-8S/punching and flanging (adjusted ) |
|
Feeding speed |
800mm/s(adjusted) |
|
Linear motion accuracy(servo motor) |
±0.05mm |
|
Clamping force |
1200Kgf |
|
Processing force |
1200Kgf |
|
Operation methods |
Auto/manual/semi auto |
|
Loading and unloading method |
Manual |
|
Clamping method |
Hydraulic |
|
Control |
NC |
|
Cooling method |
Water |
|
Weight |
1800kg |
|
Voltage |
380°±10V,50HZ(customized) |
|
Total power |
9kw |
|
Max working pressure |
12-14Mpa(150-200kgpressure) |
|
Punching and flanging |
100mm×2piece,80×2piece |
|
dimension(L×W×H) |
3600×1200×2000mm(for reference) |
The Full Automatic Pipe Punching and Flanging Hole Extruding Machine is a specialized tube processing solution designed to combine multiple operations in one efficient production workflow. By integrating pipe punching,flanging,and hole extruding functions,the machine can help manufacturers process repetitive metal tube components with reduced manual handling and improved production consistency.
Pipe and tube components are widely used in automotive exhaust systems,furniture frames,industrial equipment,construction components,heat exchangers,agricultural machinery,and general metal fabrication. Many of these applications require accurately positioned holes,formed hole edges,or flanged openings before the tube is assembled,welded,connected,or installed. An integrated pipe processing machine provides a practical solution for these applications.
Automatic Pipe Punching
The punching station is designed to create holes at predetermined locations on metal pipes or tubes. Depending on the tooling and machine configuration,the system can process different hole sizes and shapes.
Automatic feeding and positioning can reduce repetitive manual measurement and handling. Once the tube is properly loaded,the machine can perform the programmed or preset processing sequence according to its configuration.
The actual punching capacity depends on tube material,outer diameter,wall thickness,material strength,hole diameter,tooling,and machine force. Customers should provide detailed tube specifications before selecting the appropriate machine configuration.
Pipe Hole Extruding
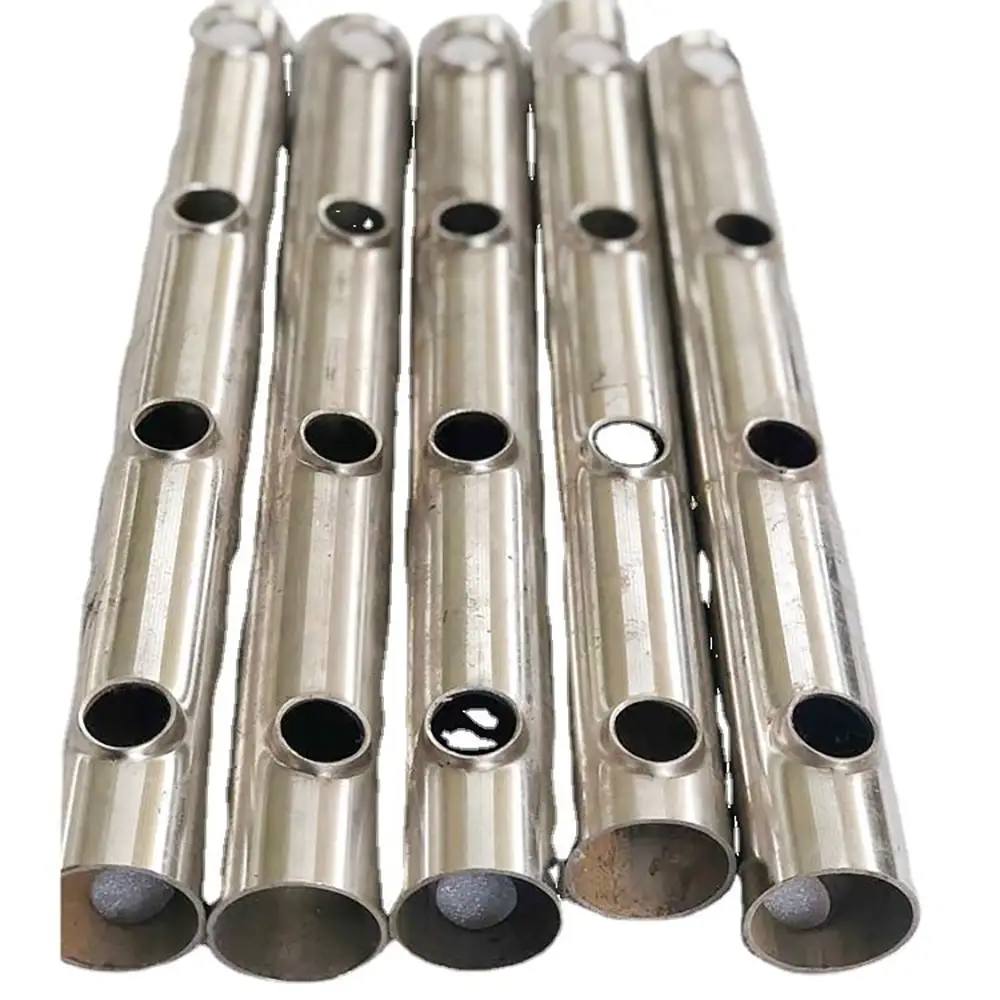
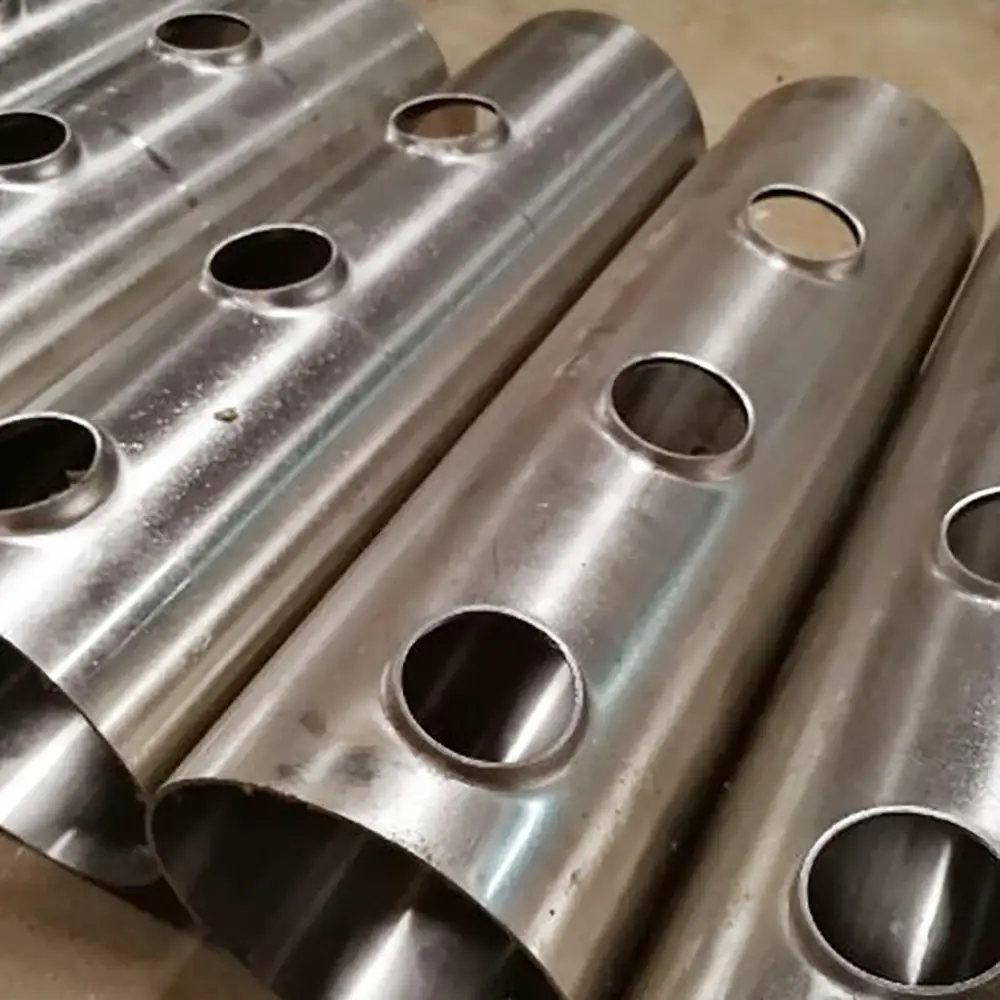
Hole extruding is an important process when a tube requires a formed opening with an extended collar or raised edge. Instead of simply creating a flat punched hole,the extrusion process can form material around the opening to create a more functional connection area.
This type of processing is commonly associated with tube branches,fluid connections,ventilation components,heat exchanger parts,and other fabricated tube assemblies. The resulting hole geometry depends on the extrusion tooling,material properties,and processing parameters.
Proper tooling design is essential because tube diameter,wall thickness,and material ductility can significantly affect the forming result.
Pipe Flanging
The flanging function is designed to form or reshape the edge of a pipe opening or tube end according to the required component geometry. Flanged tube sections can be useful for assembly,connection,reinforcement,and subsequent fabrication operations.
Depending on the machine design,flanging may be performed after punching or hole forming as part of an integrated processing sequence. Combining operations can reduce workpiece transfers and help establish a more consistent production workflow.
The actual flanging geometry and available processing range depend on the machine tooling and tube specifications.
Full Automatic Processing
A full automatic configuration can help reduce repetitive manual operations during tube processing. Feeding,positioning,punching,forming,and other steps can be coordinated according to the machine's control system and mechanical configuration.
Automation is particularly useful when manufacturers produce large quantities of similar tube components. Repeatable processing sequences can help reduce operator workload and improve production organization.
Actual cycle time depends on tube dimensions,number of holes,forming operations,feeding method,tooling,machine configuration,and production layout. Production samples should be evaluated when establishing expected output.
Suitable Materials
The machine can be configured for suitable carbon steel,stainless steel,mild steel,aluminum,and other metal tubes depending on the application. Material properties should be evaluated before selecting punches,forming tools,and extrusion tooling.
Stainless steel may require different tooling and forming parameters than mild steel because of its strength and work-hardening characteristics. Aluminum may require careful control of forming conditions to reduce cracking or deformation.
For specialized materials,testing is recommended before final machine configuration.
Tube and Pipe Applications
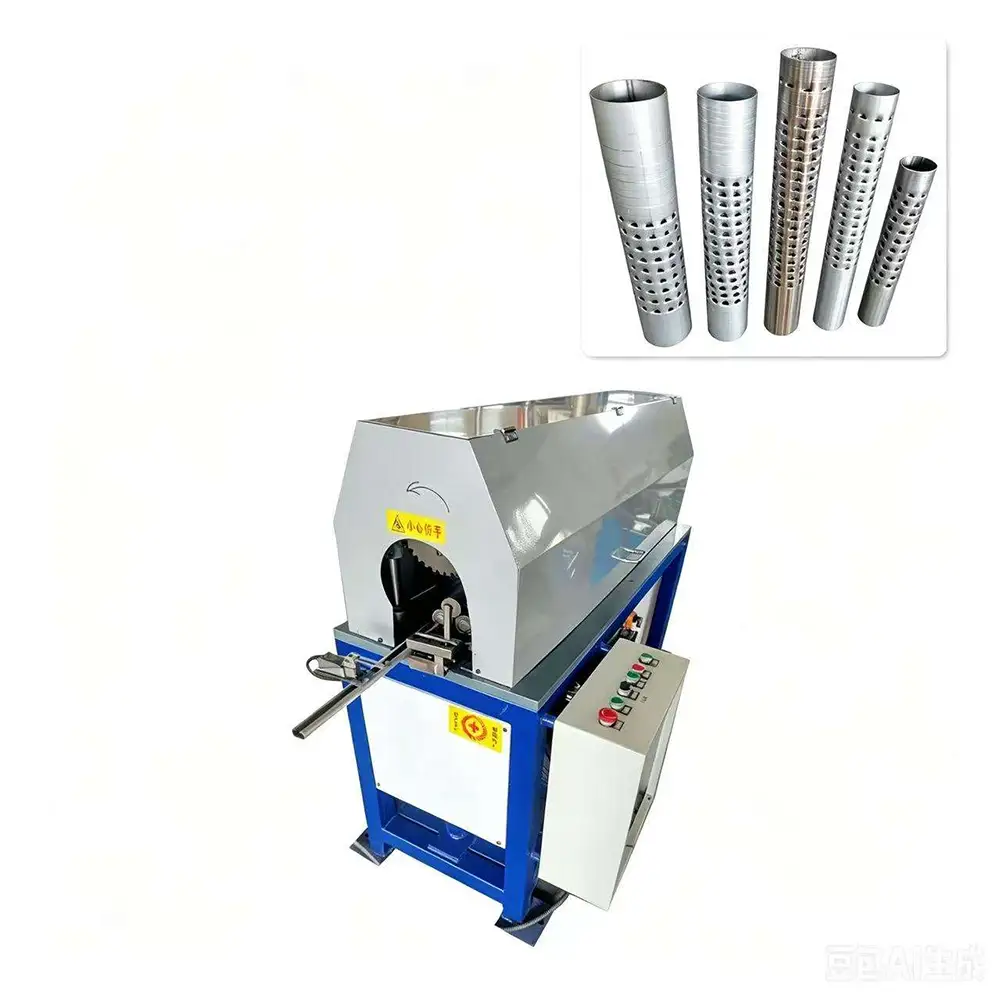
This automatic pipe punching and flanging machine can be used in many industries. Typical applications include automotive exhaust components,muffler tubes,air-conditioning components,heat exchanger tubes,plumbing components,metal furniture frames,industrial equipment,agricultural machinery,construction products,and general tube fabrication.
For exhaust applications,the machine can be configured for suitable hole punching and formed openings required for tube connections or related components. For furniture and frame production,it can support repetitive hole-making and tube-end processing.
Custom Tooling
Punches,dies,extrusion mandrels,and flanging tools are critical to the final processing result. Tooling should be matched to the tube diameter,wall thickness,material,and required hole or flange geometry.
Custom tooling can be developed for special tube profiles,hole locations,extrusion diameters,and flange dimensions. Multiple tooling sets may also be considered when manufacturers process different tube sizes.
Fixtures are equally important because they help support the tube and maintain the correct position during punching and forming.
Production Efficiency
Combining punching,flanging,and hole extrusion into one machine can reduce unnecessary movement between separate processing stations. This integrated workflow can be especially useful for repetitive production.
Automatic positioning and feeding systems can further improve process consistency by reducing manual measurement. However,actual productivity depends on the complete production sequence and machine configuration.
Manufacturers should evaluate loading time,processing cycle,tool changes,unloading time,and inspection requirements when calculating production capacity.
Quality Control
Quality inspection should include hole diameter,hole position,extrusion height,flange dimensions,tube deformation,and overall component dimensions. Consistent tooling and stable workholding are important for maintaining repeatable results.
Punches and forming tools should be inspected regularly because wear can affect hole quality and forming dimensions. Production samples can be used to verify tooling selection and processing parameters before large-scale manufacturing.
Maintenance and Safety
Regular maintenance helps support stable automatic operation. Operators should inspect punches,dies,forming tools,fixtures,hydraulic components,and moving parts according to the manufacturer's recommendations.
The working area should be kept clean,and worn tooling should be replaced when necessary. Operators should receive proper training and follow machine-specific safety procedures.
Guards,emergency stops,and other protective devices should be used where provided. The machine should be installed and operated according to applicable local workplace safety requirements.
Custom & OEM Solutions
Different tube products can require different hole patterns,extrusion dimensions,flange shapes,and production sequences. We can support OEM and ODM solutions based on customer drawings,sample components,and technical specifications.
Customization may include punching tools,extrusion tooling,flanging tools,fixtures,feeding systems,positioning mechanisms,and control configurations. This makes the machine suitable for manufacturers with specialized tube-processing requirements.
Why Choose Us
Multi-Process Tube Processing – Combines punching,flanging,and hole extruding operations in one integrated solution.
Automatic Production Workflow – Automatic feeding and positioning options can reduce repetitive manual handling.
Wide Tube Applications – Suitable for selected steel,stainless steel,aluminum,and other metal tube applications.
Custom Tooling Support – Punches,dies,extrusion tools,and flanging tooling can be developed for specific components.
Production Consistency – Stable fixtures and repeatable processing sequences support consistent tube fabrication.
Industrial Applications – Suitable for automotive,exhaust,furniture,construction,industrial,and general metal fabrication.
OEM & ODM Capability – Machine configurations can be adapted to customer drawings,samples,and production requirements.
Complete B2B Support – Suitable for manufacturers,metal fabricators,distributors,and industrial equipment buyers.
FAQs
1. What does this machine do?
It combines pipe punching,flanging,and hole extruding operations for integrated metal tube processing.
2. What is hole extruding?
Hole extruding forms a raised or extended edge around a punched tube opening. It can provide a formed connection area for certain tube assemblies.
3. Can it punch holes automatically?
Yes. The machine can be configured with automatic feeding and positioning functions depending on the specific machine design.
4. What materials can be processed?
Suitable carbon steel,mild steel,stainless steel,and aluminum tubes may be processed depending on the machine configuration and tooling.
5. Can stainless steel tubes be processed?
Yes,provided the tube dimensions,material grade,and wall thickness are within the machine's processing range and appropriate tooling is selected.
6. Can the machine perform pipe flanging?
Yes. The machine is designed to integrate flanging into the tube processing workflow according to its tooling configuration.
7. Can the hole size be customized?
Yes. Hole size can generally be customized through appropriate punch and die tooling. The required hole diameter should be confirmed before tooling design.
8. Can different tube diameters be processed?
Potentially yes. Different tube diameters may require different fixtures and tooling. The actual processing range should be confirmed for the specific machine.
9. Is this machine suitable for exhaust pipes?
It can be used for suitable exhaust and muffler tube applications requiring punching,forming,or related tube processing operations.
10. Does automatic operation mean no operator is required?
Not necessarily. Automatic functions can reduce repetitive operations,but loading,unloading,inspection,tool changes,and process supervision may still require an operator depending on the configuration.
11. Can custom tooling be provided?
Yes. Custom punches,dies,extrusion tools,flanging tools,and fixtures can be considered for specialized tube components.
12. What information is needed for machine selection?
Provide tube material,outer diameter,wall thickness,hole diameter,hole location,flange or extrusion dimensions,production quantity,and sample drawings or photos when available.
Prev:
CNC Full Automatic Angle Steel Punching Hole Machine Angle Steel End Cutting
Next:
Angle Steel Punch Hole and Cut off Machine
TAG:
Tube End Forming Machine,
Pipe End Forming Machine,
Metal Tube Processing Machine,
Pipe Forming Machine,
Tube Forming Machine,
Pipe Fabrication Machine,
Tube Fabrication Machine,
Industrial Pipe Processing Machine,
Tube Punching Equipment,
Automatic Tube Punching Machine,
Automatic Pipe Punching Machine,
Pipe Hole Punching Machine,
Tube Punching Machine,
Tube Hole Punching Machine,
Pipe Punching Machine,
Stainless Steel Tube Punching Machine,
Stainless Steel Pipe Punching Machine,
Metal Pipe Processing Machine,
Automatic Pipe Forming Machine,
Pipe Flanging Machine,
Tube Flanging Machine,
Automatic Tube Processing Machine,
Automatic Pipe Processing Machine,
Steel Pipe Punching Machine,
Steel Tube Punching Machine,
Metal Pipe Hole Punching Machine,
Hydraulic Pipe Punching Machine,
Hydraulic Tube Punching Machine,
Hydraulic Pipe Flanging Machine,
Metal Tube Fabrication Machine,
Related Category:
Automatic Pipe Punching Machine,Automatic Tube Punching Machine,Pipe Flanging Machine,Hole Extruding Machine China, suppliers, manufacturers, factory, customized, wholesale, quotation, made in China