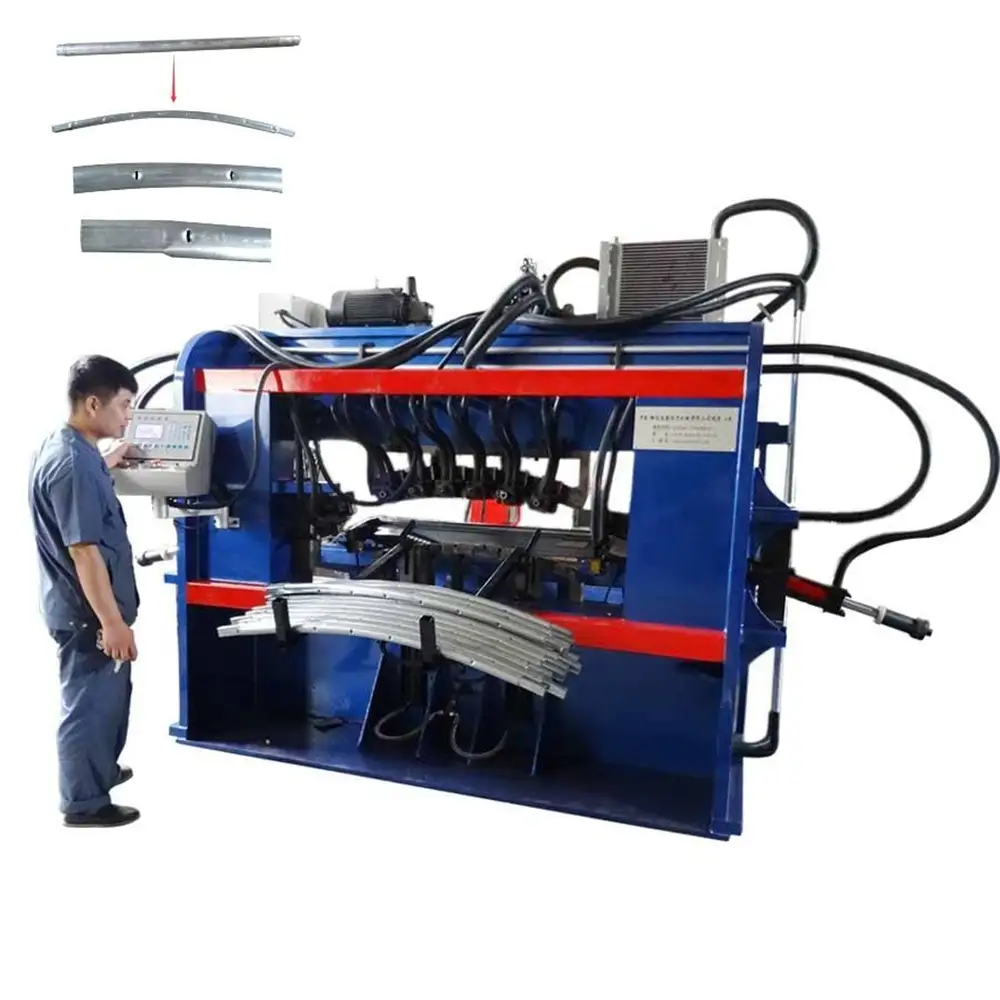
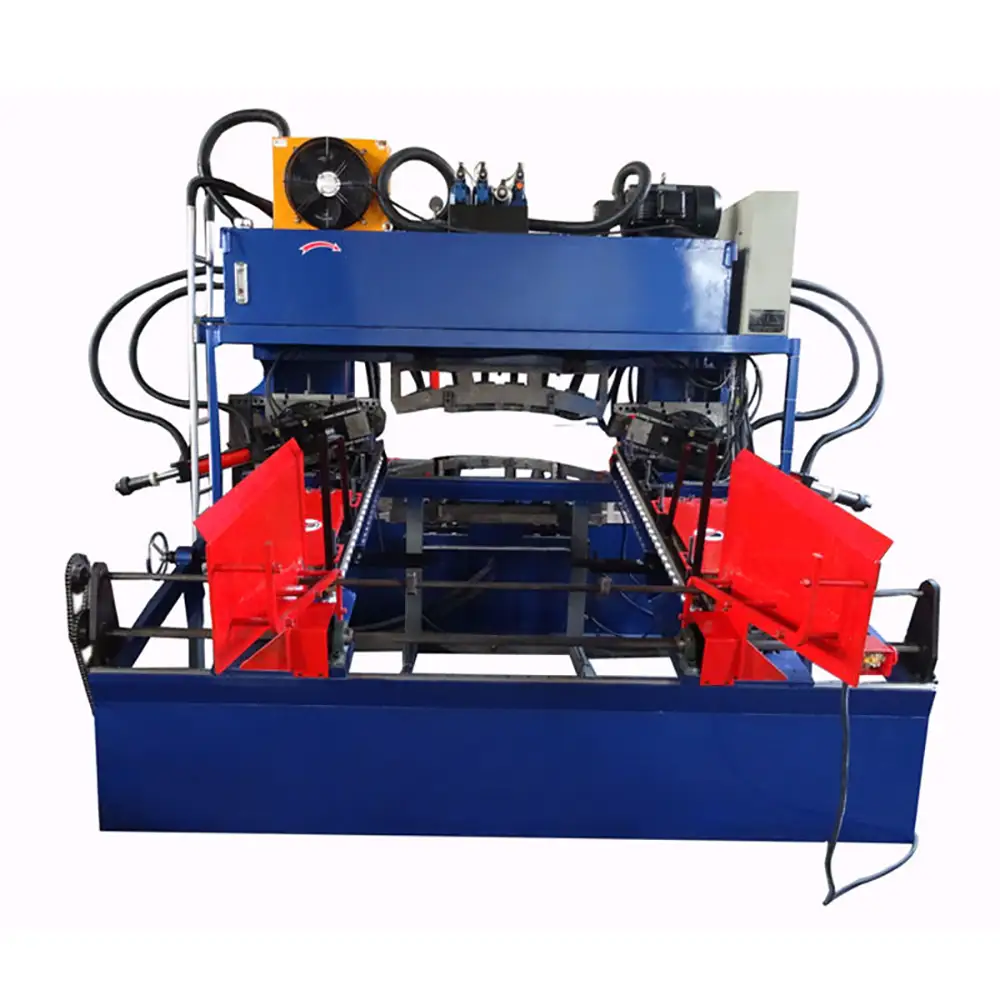
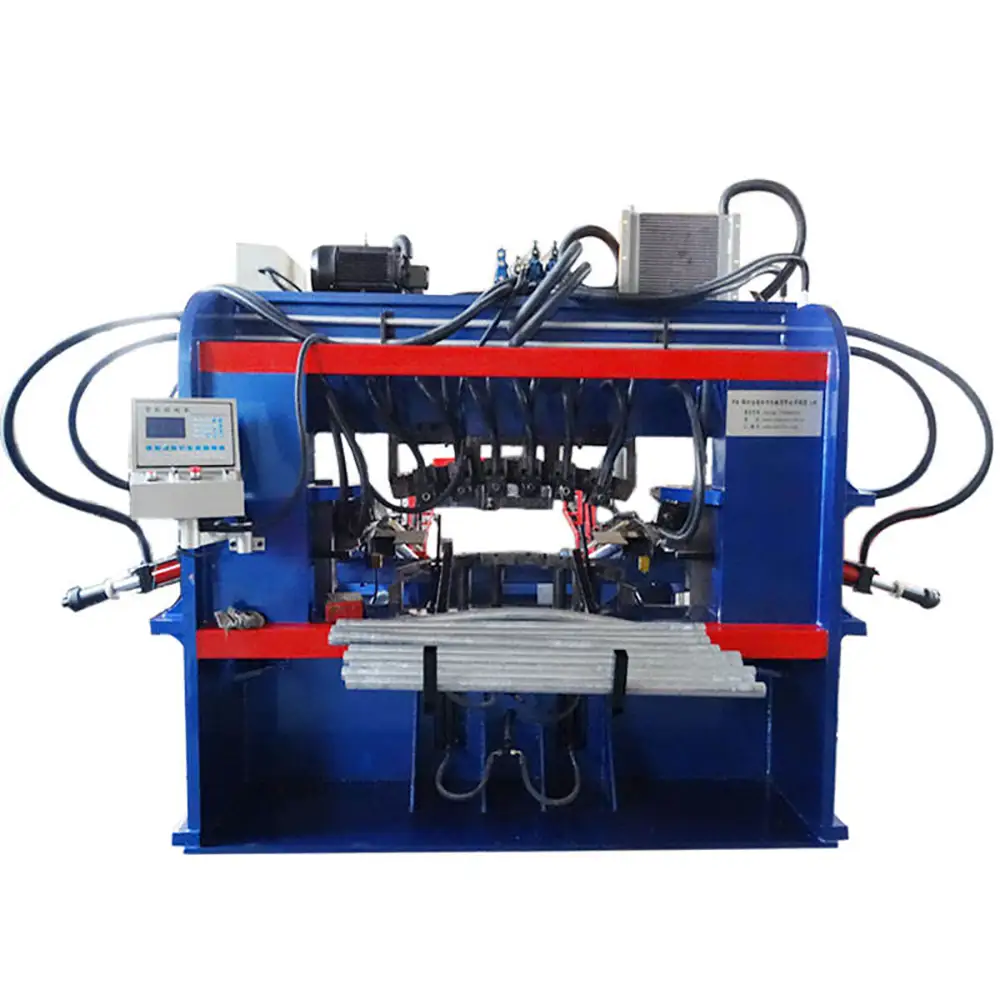
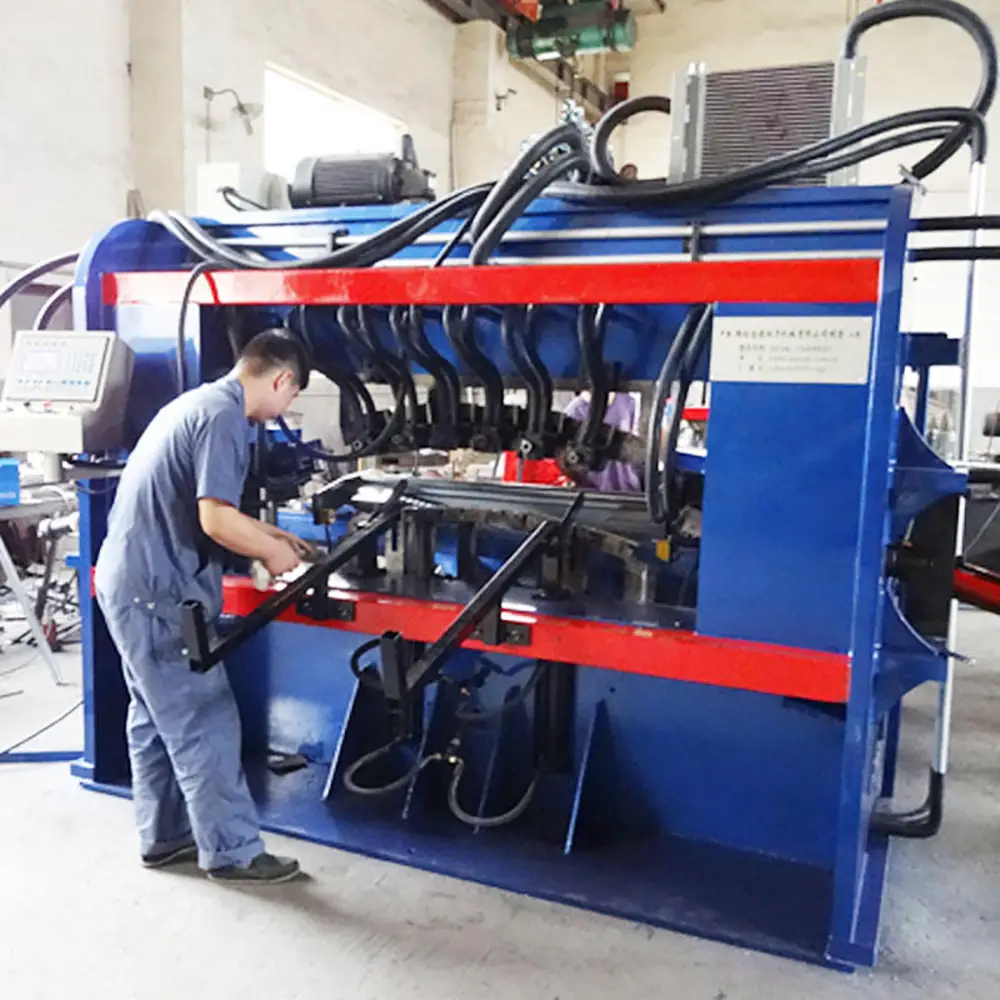
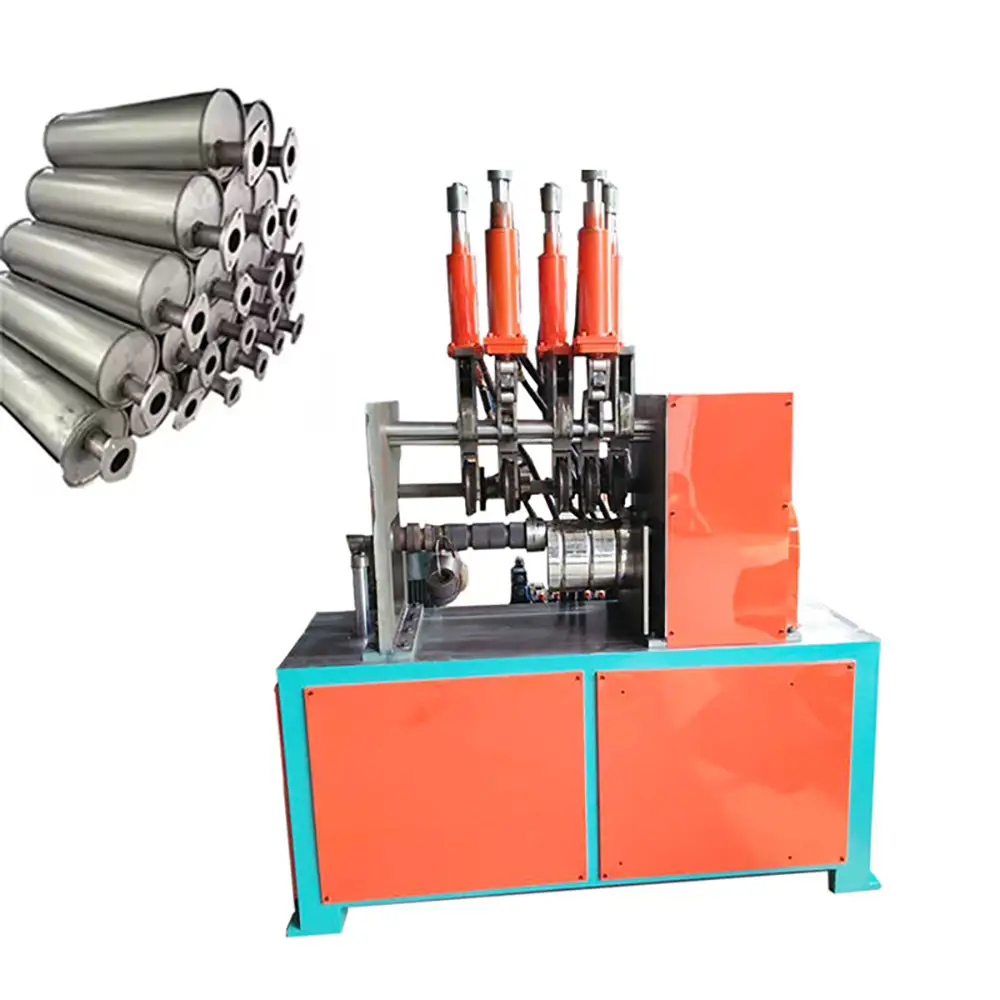
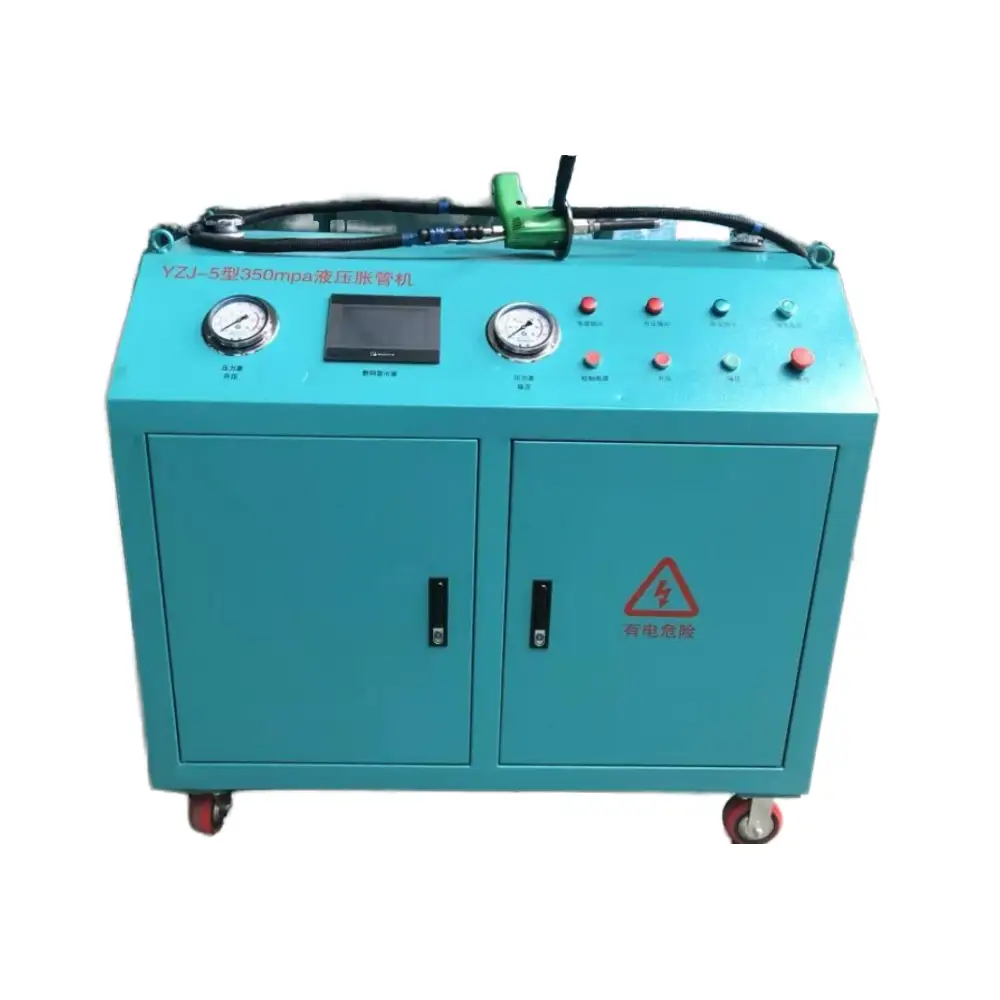
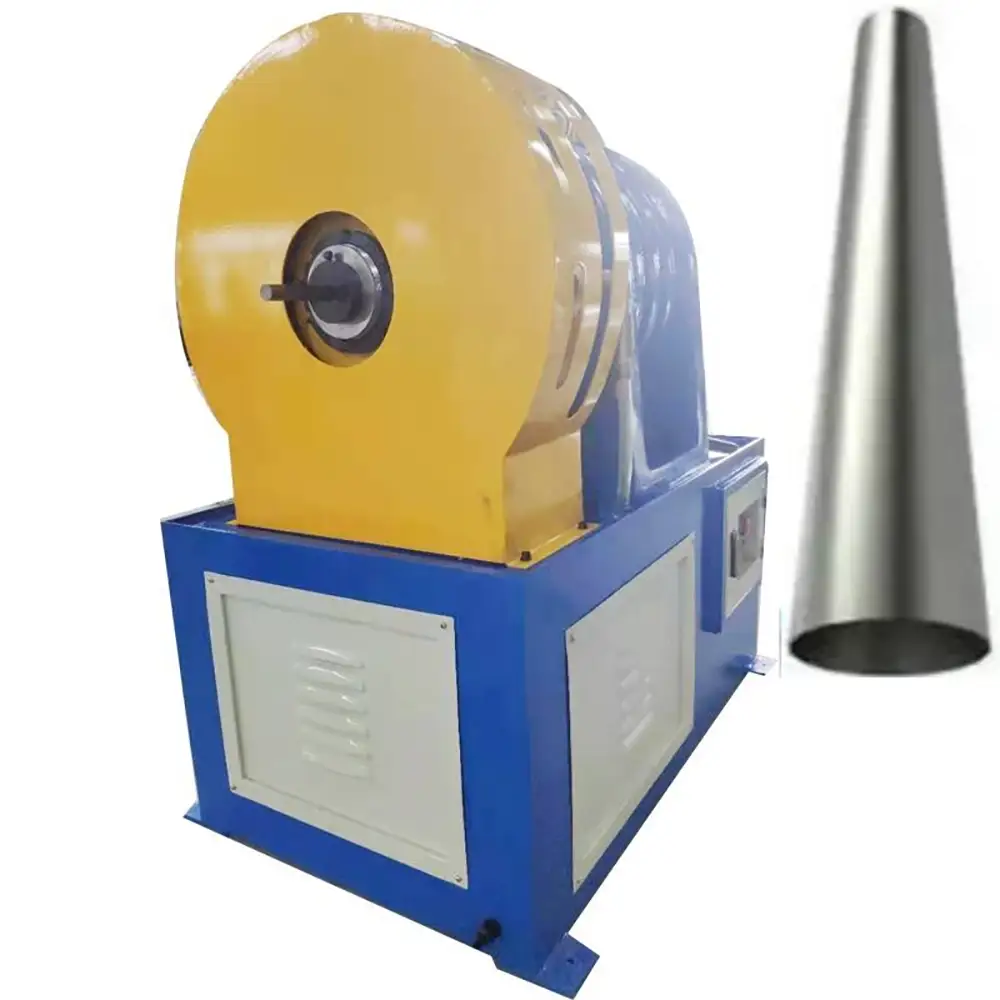
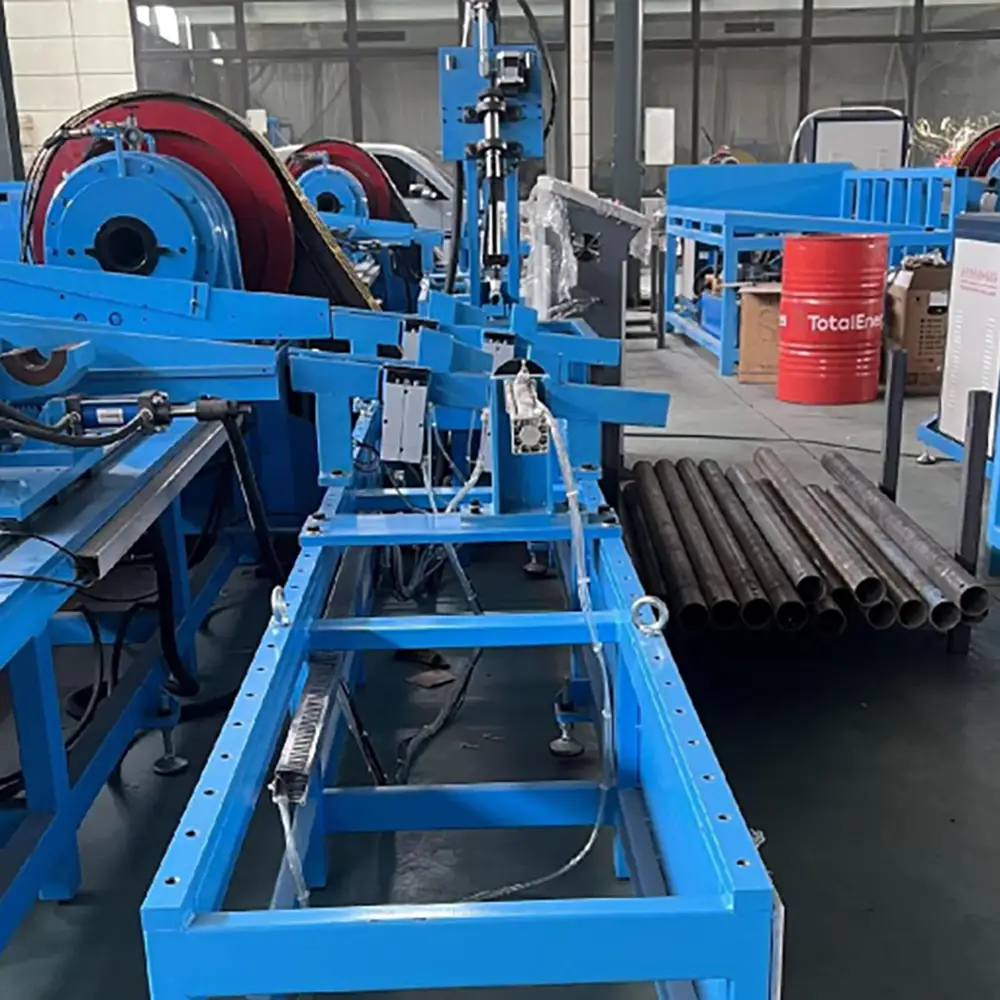
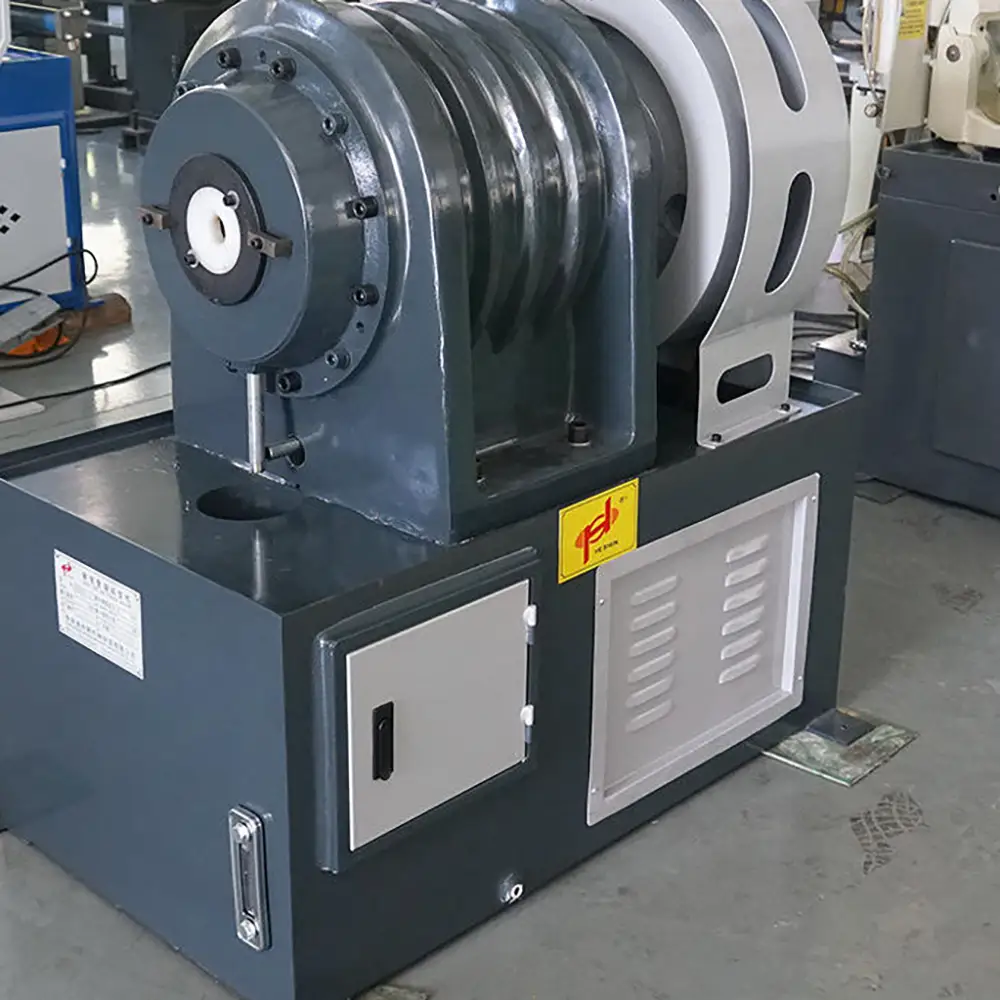
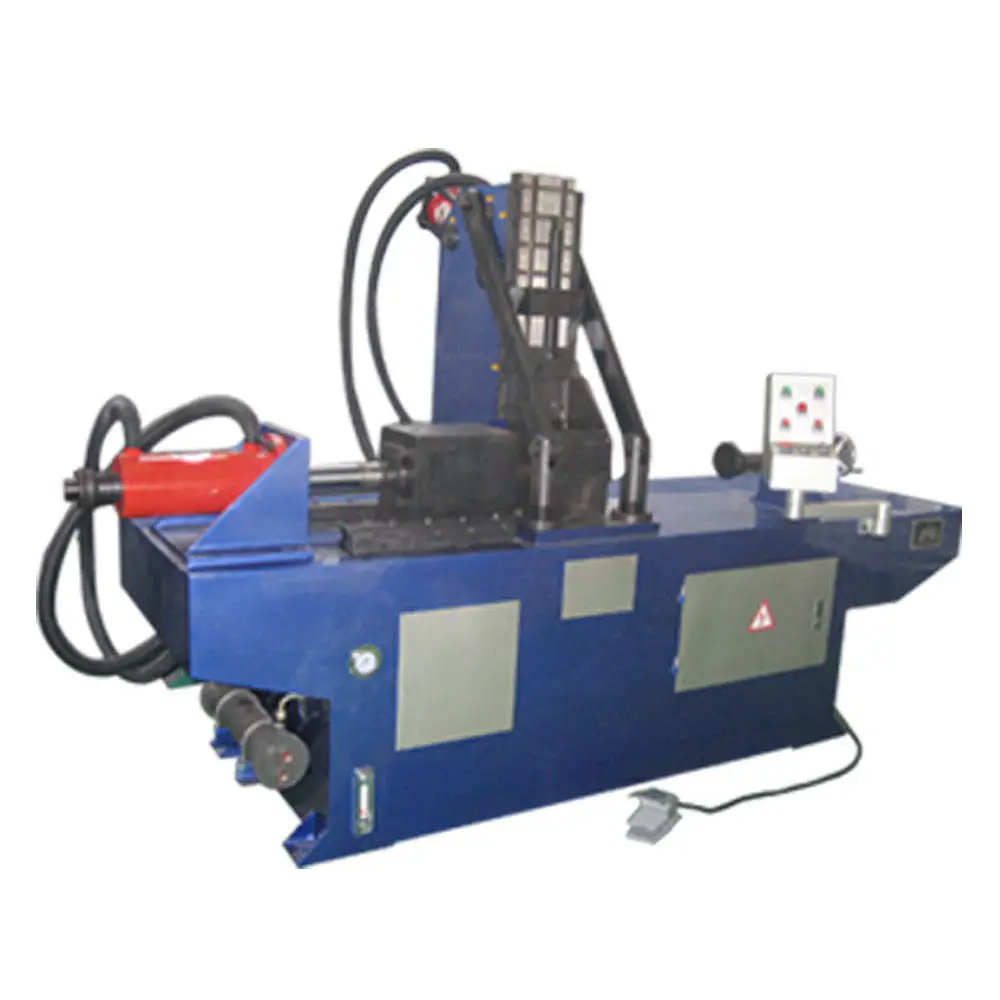
1. microcomputer control,Manually or semi-automatic, hydraulic and Servo motor system driven.
2.The motion pedal switches, tightly stops, continuously tightly stops, high security.
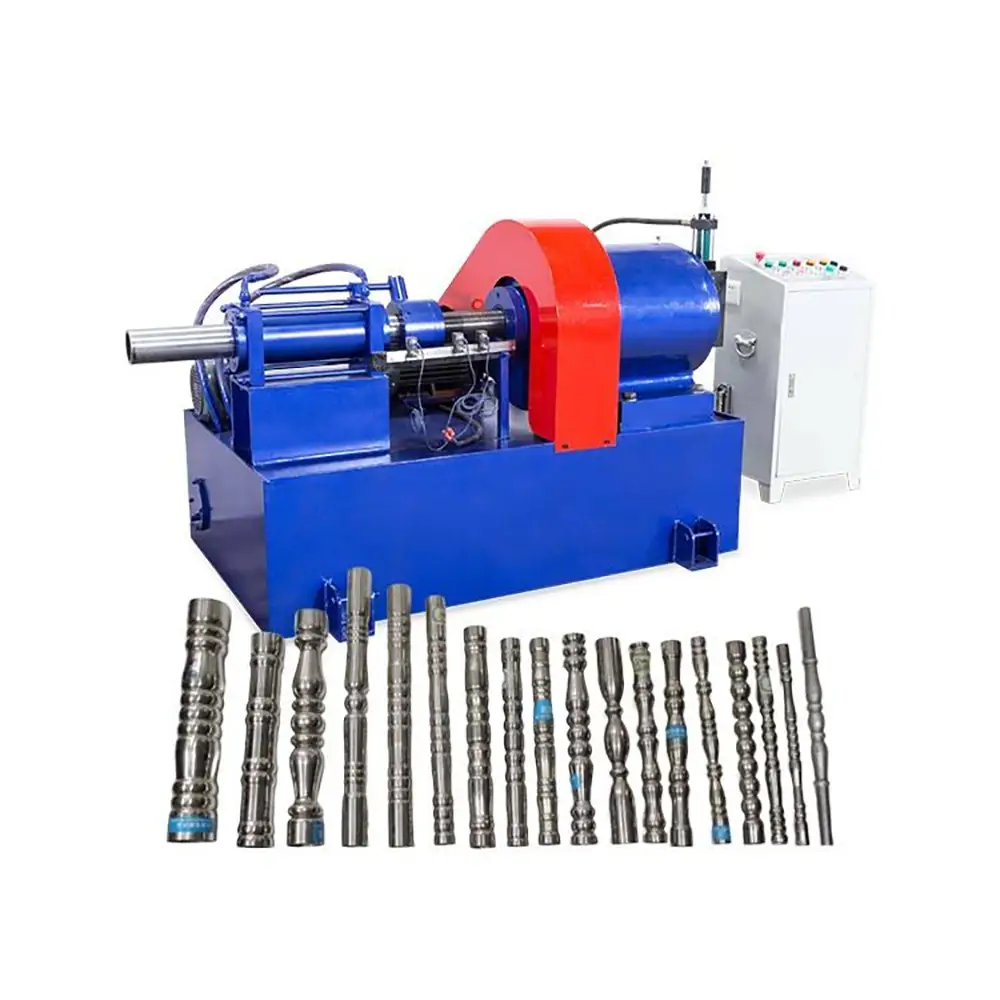
3.Processing shapes: convex-shaped, concavity-shaped, nodular shape, long partial shape, square shape, topological shape, oblique shape, V-shape, cracking type and flat type. The shape of the mould shall be subject to the object to be processed.
4.The mold replacement is simple.
|
model |
CX42CNC |
|
Max diameter |
Φ42mm |
|
Max thickness |
2mm |
|
Power |
12.08KW |
|
Hydraulic |
21Mpa |
|
Length |
2500x2400x2500mm |
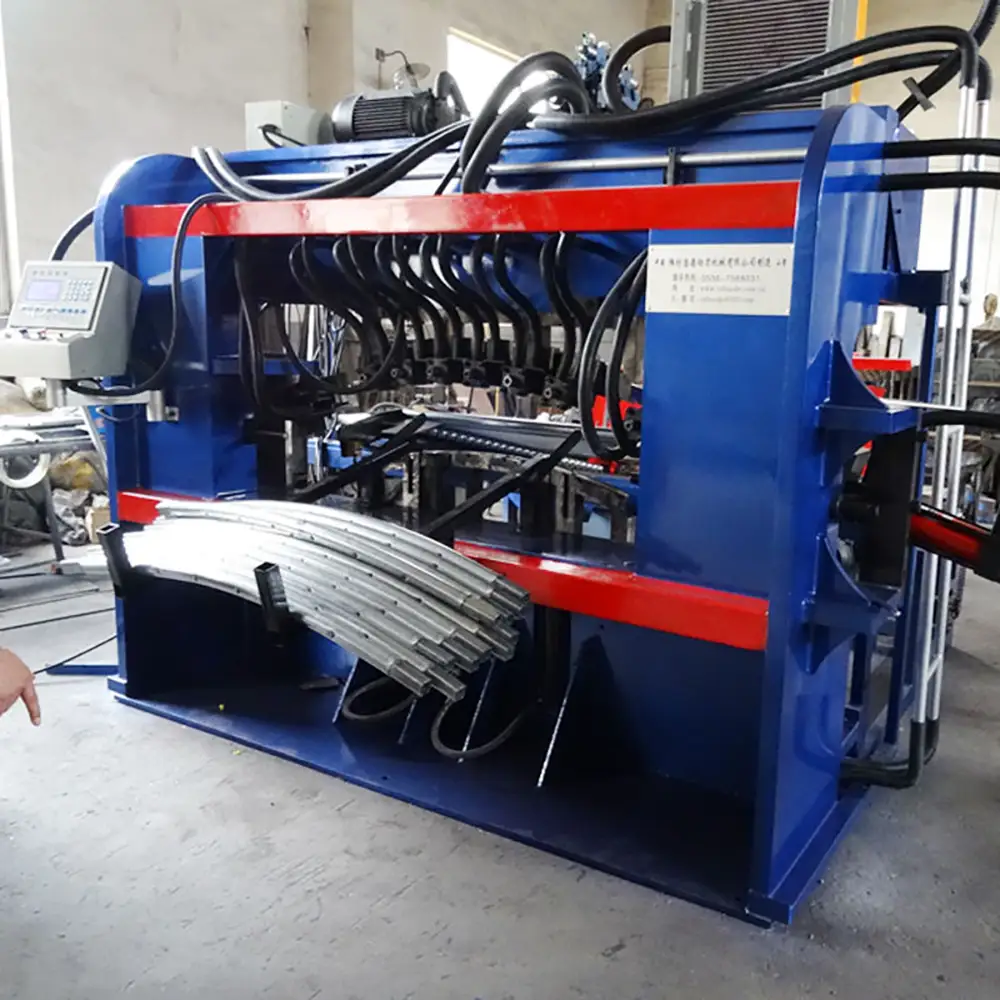
Automatic Pipe Press Arch Punching Hole and Tube End Forming Machine for Trampoline
The Automatic Pipe Press Arch Punching Hole and Tube End Forming Machine for Trampoline is designed for efficient processing of metal tubes used in trampoline frames and other tubular structures. By combining pipe pressing,arch forming,hole punching,and tube end forming functions into an integrated production solution,the machine can help manufacturers streamline repetitive tube fabrication processes.
Trampoline frames commonly require curved or arch-shaped tubes with accurately positioned holes and specially formed tube ends. These features allow individual frame sections to connect with brackets,bolts,support components,and other structural parts during final assembly.
Instead of using separate machines for every operation,a multifunction tube processing system can combine several forming and punching steps within a coordinated workflow. This can reduce repeated material handling and help improve production consistency for manufacturers producing trampoline frames in batches.
The actual forming capacity,maximum tube dimensions,punching diameter,and production speed depend on the specific machine configuration,material,tooling,and workpiece design.
Automatic Pipe Pressing and Arch Forming
Arch forming is an important process when producing curved trampoline frame tubes. A straight metal tube can be shaped into a controlled arc or curved profile using suitable forming tooling.
The machine uses a press-forming mechanism to apply controlled force to the tube according to the required shape. Proper tooling design helps distribute forming pressure and minimize unwanted deformation.
The required arch radius depends on the trampoline frame design. Different trampoline sizes and frame structures may require different bending or pressing tools.
For production applications,the customer should provide tube diameter,wall thickness,material,arch radius,and finished dimensions so the appropriate forming method and tooling can be evaluated.
Pipe Hole Punching
Hole punching is another important operation for trampoline frame production. Holes may be required for bolts,pins,brackets,connecting components,or other assembly parts.
A dedicated punching system can create holes at predefined locations without requiring separate manual drilling for every workpiece.
The punching force depends on material type,tube wall thickness,hole diameter,punch geometry,and machine configuration. Punch and die clearance should be selected according to the material and required hole quality.
For repeat production,fixtures can help position the tube consistently before punching. This can improve repeatability between individual frame components.
Tube End Forming
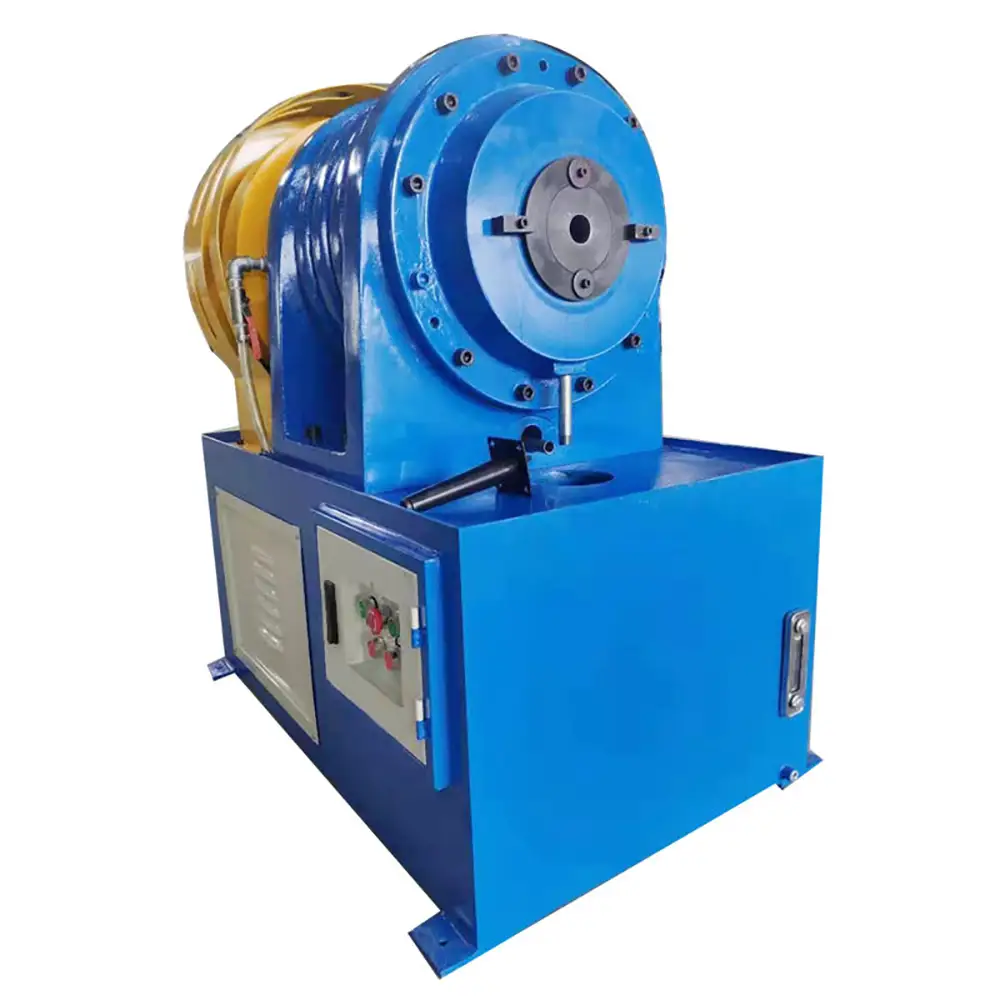
Tube end forming modifies the end section of a metal tube to create a specific profile for assembly or connection.
Depending on the tooling,the machine may be configured for operations such as end flattening,expanding,reducing,swaging,notching,flaring,or other tube-end processing.
For trampoline frames,the tube ends may require a specific shape to connect with frame joints or other components. Dedicated dies can be designed around the required finished geometry.
The actual end-forming process should be selected according to the tube material,diameter,wall thickness,and final product design.
Trampoline Frame Manufacturing
Trampoline frames are generally made from tubular metal components that must provide structural support while maintaining consistent dimensions.
During manufacturing,the tubes may need to undergo several processes before final assembly. These can include cutting,bending or arch forming,punching,end forming,and surface finishing.
Combining multiple operations in one machine can simplify the production workflow and reduce the number of times the tube must be transferred between separate workstations.
For manufacturers producing multiple trampoline models,interchangeable tooling can provide greater flexibility for different tube sizes and frame designs.
Automatic Production Workflow
The automatic or machine-assisted workflow can help reduce repetitive manual operations. Depending on the configuration,a typical process may involve loading the tube,positioning it in the fixture,performing arch pressing,punching required holes,and completing the specified tube-end forming operation.
Automation level varies between machine models. Some configurations may require manual loading and unloading while the forming and punching cycles are controlled automatically.
Production output depends on tube size,number of operations,tool changes,loading method,cycle settings,and operator workflow.
For high-volume trampoline frame production,the complete production cycle should be evaluated rather than relying only on the nominal machine cycle time.
Hydraulic Press Forming
A hydraulic press system can provide controlled forming force for tube pressing and punching operations.
Hydraulic force is useful when processing metal tubes that require substantial forming pressure. The required force depends on tube material,wall thickness,diameter,forming geometry,and tooling design.
The hydraulic system should be selected according to the actual application rather than assuming that a particular motor or pressure specification is suitable for every tube.
Customers should provide sample tubes or drawings when requesting a customized machine configuration.
Suitable Tube Materials
The machine can be configured for compatible metal tubes such as:
Carbon steel tubes
Mild steel tubes
Galvanized steel tubes
Stainless steel tubes
Aluminum tubes
Other suitable metal tubing
Trampoline frames commonly use steel tubing,although the appropriate material depends on the product design and structural requirements.
Material strength and wall thickness directly affect forming and punching force. High-strength or harder materials may require different tooling and process parameters.
Applications Beyond Trampolines
Although the machine is designed for trampoline tube processing,the same forming and punching principles can be applied to other tubular products.
Potential applications include:
Fitness equipment frames
Playground equipment
Sports equipment
Outdoor furniture
Metal furniture frames
Bicycle components
Storage racks
Guardrail components
Agricultural equipment
Tubular structures
Custom steel frames
The actual application range depends on the machine's forming capacity and tooling configuration.
Production Consistency and Quality
Consistent positioning is important when producing large quantities of identical trampoline frame tubes. Small differences in hole location or arch dimensions can make final assembly more difficult.
Dedicated fixtures and forming dies can help maintain consistent positioning between workpieces.
Quality inspection may include checking tube diameter,arch radius,hole position,hole diameter,end profile,and overall workpiece dimensions.
First-piece inspection is recommended when introducing a new tube size or changing the tooling.
Tooling and Custom Dies
Tooling is one of the most important components of a tube processing machine. The punch,die,forming fixture,and tube support should all match the workpiece requirements.
Custom tooling can be developed for:
Trampoline arch tubes
Hole punching
Tube end forming
End flattening
Tube expanding
Tube reducing
Swaging
Notching
Special connection profiles
Customers can provide CAD drawings,finished samples,tube dimensions,and required hole locations for tooling evaluation.
For manufacturers with several trampoline frame models,tooling can be designed to support different tube sizes or interchangeable production configurations.
Maintenance and Safety
Regular maintenance helps maintain stable production performance. Hydraulic components,punches,dies,fixtures,guide systems,and electrical components should be inspected according to the manufacturer's recommendations.
Punches and dies should be checked for wear because worn tooling can affect hole quality and forming dimensions.
Operators should receive appropriate training before operating the machine. Guards,emergency stops,electrical protection,and other safety features depend on the actual machine configuration and applicable local requirements.
Custom & OEM Manufacturing Solutions
Trampoline manufacturers may have specific requirements for tube diameter,arch radius,hole position,end shape,and production volume. The machine can therefore be customized around the actual manufacturing process.
OEM and ODM options may include custom punches,dies,fixtures,feeding systems,hydraulic configurations,control systems,and production tooling.
For a quotation,customers should provide tube material,outer diameter,wall thickness,tube length,arch dimensions,hole size,hole position,end-forming requirements,and expected production volume.
This information helps the manufacturer develop a suitable automatic trampoline tube punching and forming machine for the intended application.
Why Choose Us
Multi-Function Tube Processing — Combines arch pressing,hole punching,and tube end forming within one production-oriented machine.
Trampoline Frame Application — Designed around the requirements of tubular trampoline frame manufacturing.
Automatic Machine-Assisted Processing — Helps reduce repetitive manual forming and punching operations.
Precision Hole Punching — Dedicated punches and fixtures support consistent hole positioning for assembly.
Custom Tube Forming — Dies can be developed for arch shapes,end profiles,and special tube geometries.
Flexible Material Processing — Suitable configurations can be developed for compatible steel,stainless steel,galvanized steel,and aluminum tubes.
OEM & ODM Support — Machine configuration and tooling can be developed according to drawings,samples,and production requirements.
B2B Manufacturing Solution — Suitable for trampoline manufacturers,fitness equipment companies,sports equipment producers,metal fabricators,and industrial distributors.
FAQs
1. What is a trampoline tube end forming machine?
It is a machine designed to process metal tubes used for trampoline frames by performing operations such as arch forming,hole punching,and tube-end forming.
2. Can the machine punch holes in trampoline frame tubes?
Yes. With suitable punches,dies,and fixtures,the machine can create holes at specified positions on compatible metal tubes.
3. Can it form curved or arch-shaped tubes?
Yes. The machine can be configured with suitable pressing or forming tooling for required tube arch profiles.
4. What tube materials can be processed?
Depending on the machine configuration,it can process suitable carbon steel,mild steel,galvanized steel,stainless steel,aluminum,and other compatible tubes.
5. Can the tube ends be formed?
Yes. Suitable tooling can be used for tube-end operations such as flattening,reducing,expanding,swaging,notching,or other customized profiles.
6. Is the machine fully automatic?
The automation level depends on the specific configuration. Automatic processing can be combined with manual tube loading and unloading.
7. Can different trampoline frame sizes be processed?
Yes,if the machine is equipped with appropriate interchangeable tooling and fixtures. Different tube dimensions and arch shapes should be confirmed before ordering.
8. What affects punching quality?
Material strength,tube wall thickness,hole diameter,punch and die clearance,tool condition,fixture stability,and machine force all affect punching quality.
9. Can custom punches and dies be supplied?
Yes. Custom tooling can be developed according to tube drawings,samples,hole dimensions,and required end-forming profiles.
10. What other products can the machine process?
Depending on its capacity,the machine may also process tubes for fitness equipment,playground equipment,furniture,sports equipment,racks,and other tubular structures.
11. What information is needed for a quotation?
Provide tube material,outer diameter,wall thickness,tube length,arch radius,hole diameter,hole position,end shape,and production volume.
12. Can you provide OEM tube processing solutions?
Yes. OEM and ODM machine configurations,custom tooling,fixtures,and production solutions can be developed according to customer drawings or samples.
Prev:
Ectric Swagging Machine with Threading Flanging and Reeling Function
Next:
Tube Reducer Machine for Pipe Expanding and Shrinking
TAG:
Pipe Shaping Machine,
Pipe End Processing Machine,
Automatic Tube End Forming Machine,
Tube End Processing Machine,
Tube Shaping Machine,
Hydraulic Tube Forming Machine,
Tube End Forming Equipment,
Hydraulic Pipe Forming Machine,
Pipe End Forming Equipment,
Tube Flaring Machine,
Tube Swaging Machine,
Tube Reducing Machine,
Tube End Forming Machine,
Pipe End Forming Machine,
Tube Expanding Machine,
Metal Tube Processing Machine,
Pipe Processing Machine,
Tube Processing Machine,
Tube Flattening Machine,
Fitness Equipment Tube Forming Machine,
Metal Tube Punching Machine,
Automatic Tube Punching Machine,
Automatic Pipe Punching Machine,
Trampoline Tube Forming Machine,
Trampoline Frame Punching Machine,
Trampoline Frame Tube Machine,
Trampoline Tube Punching Machine,
Trampoline Manufacturing Machine,
Pipe Hole Punching Machine,
Tube Hole Punching Machine,
Related Category:
Automatic Pipe Press Machine,Arch Punching Machine,Pipe Hole Punching Machine,Tube End Forming Machine China, suppliers, manufacturers, factory, customized, wholesale, quotation, made in China