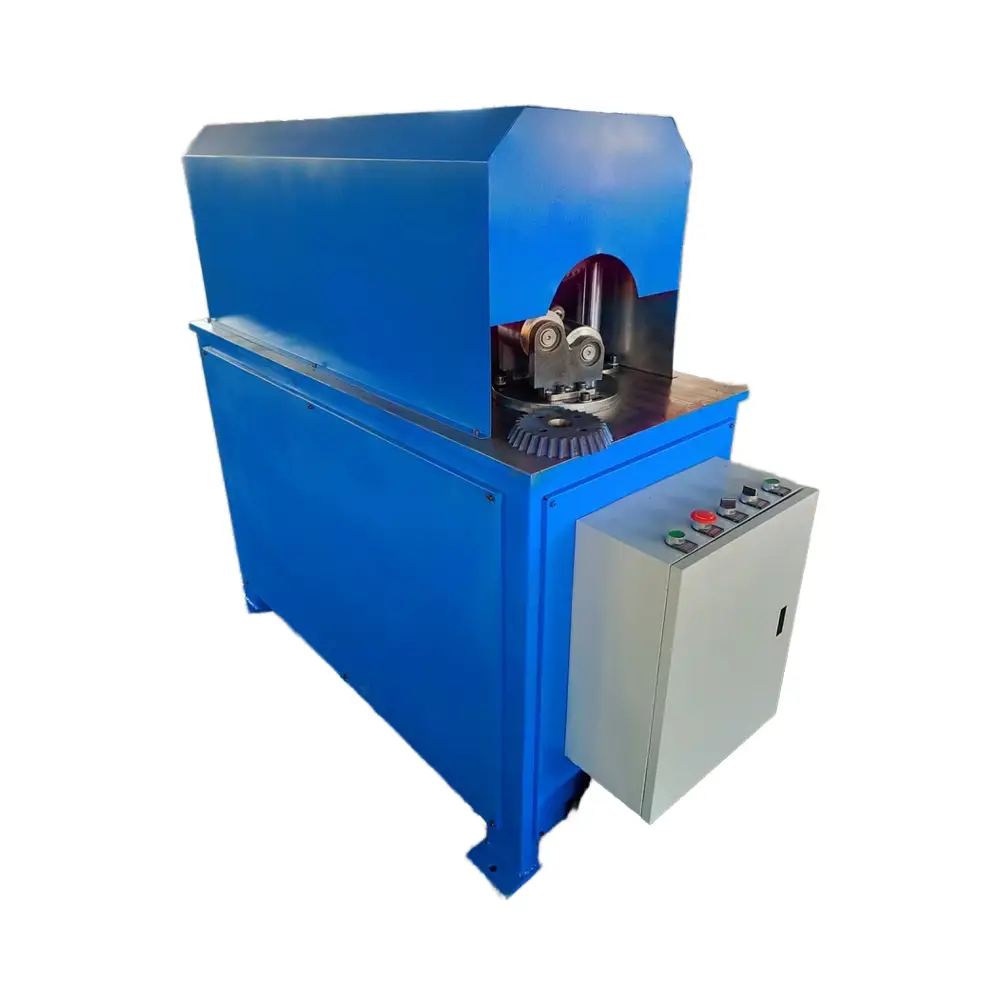
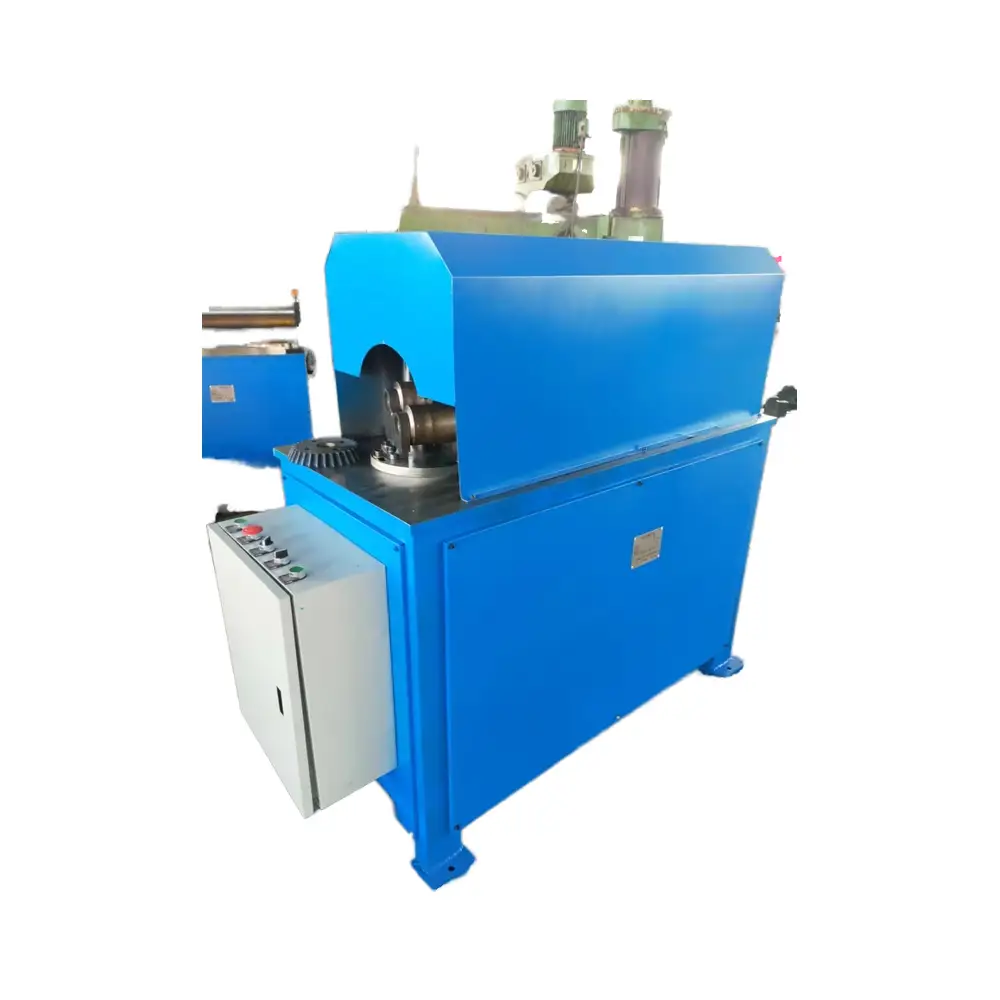
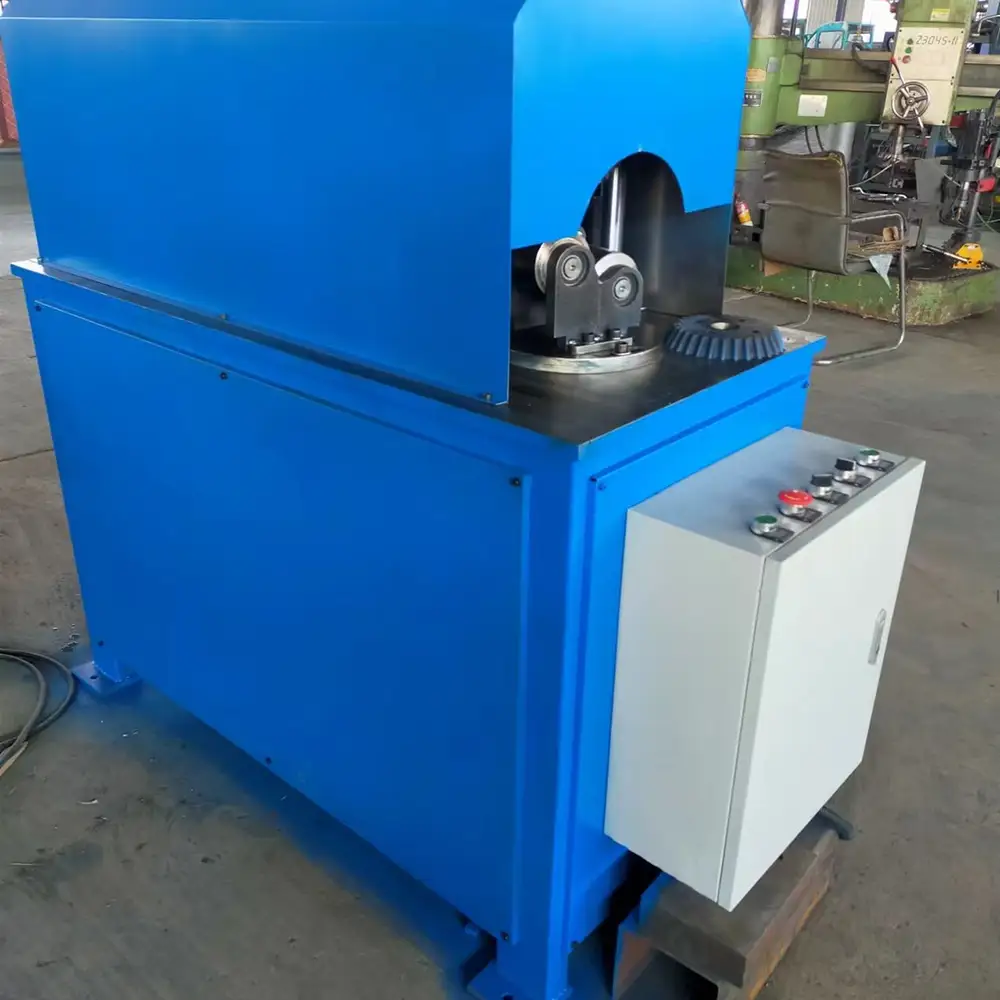
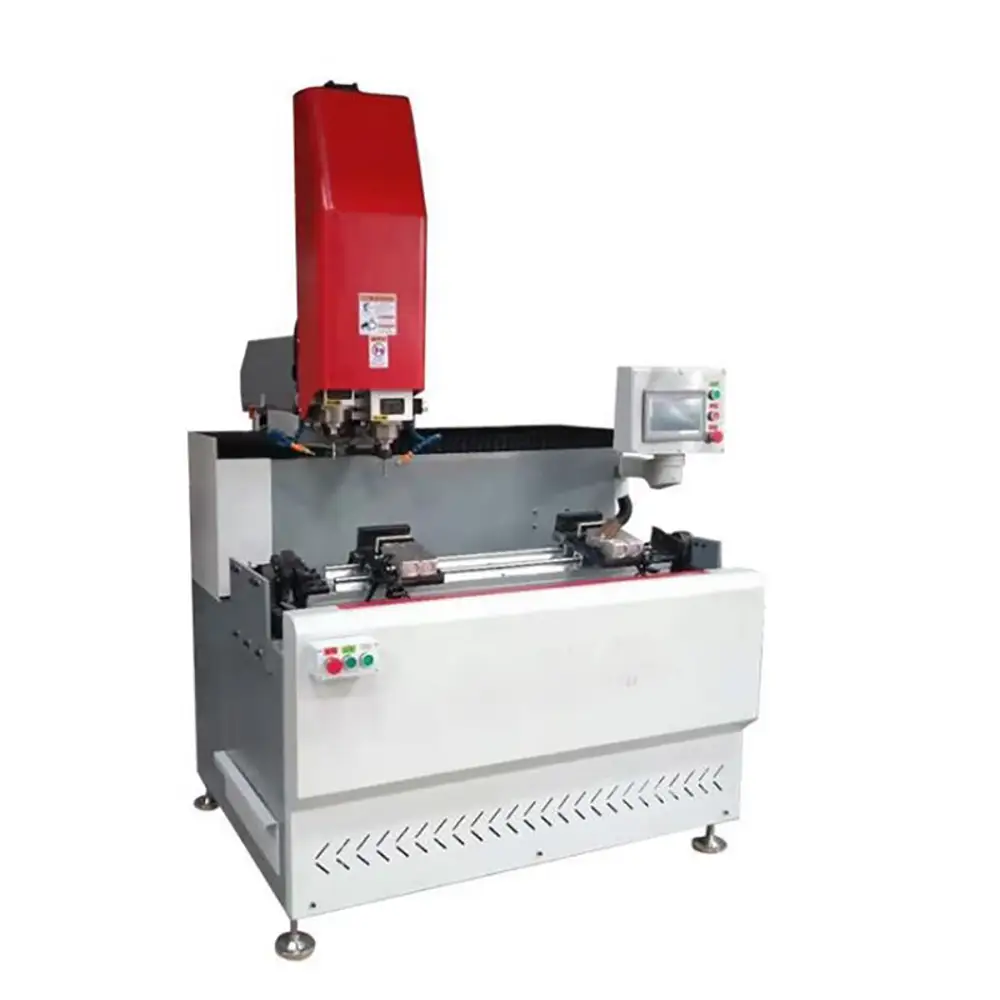
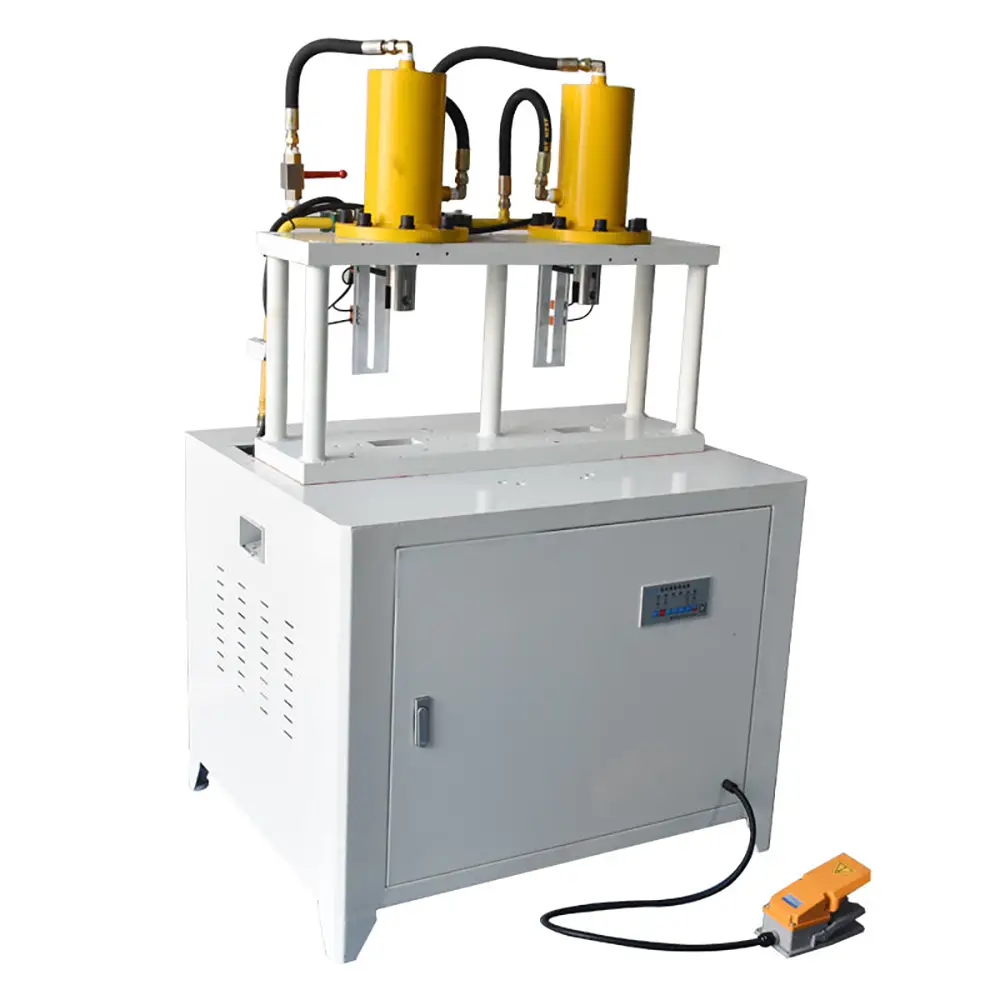
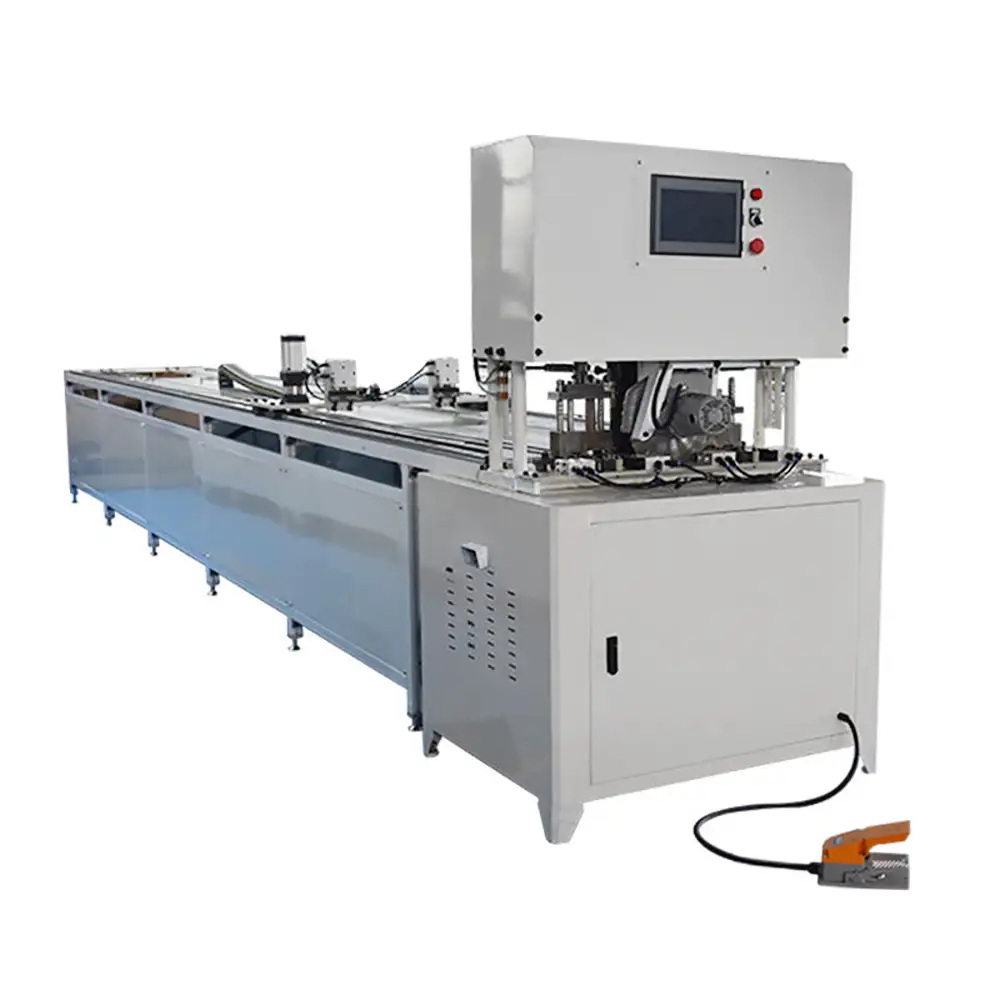
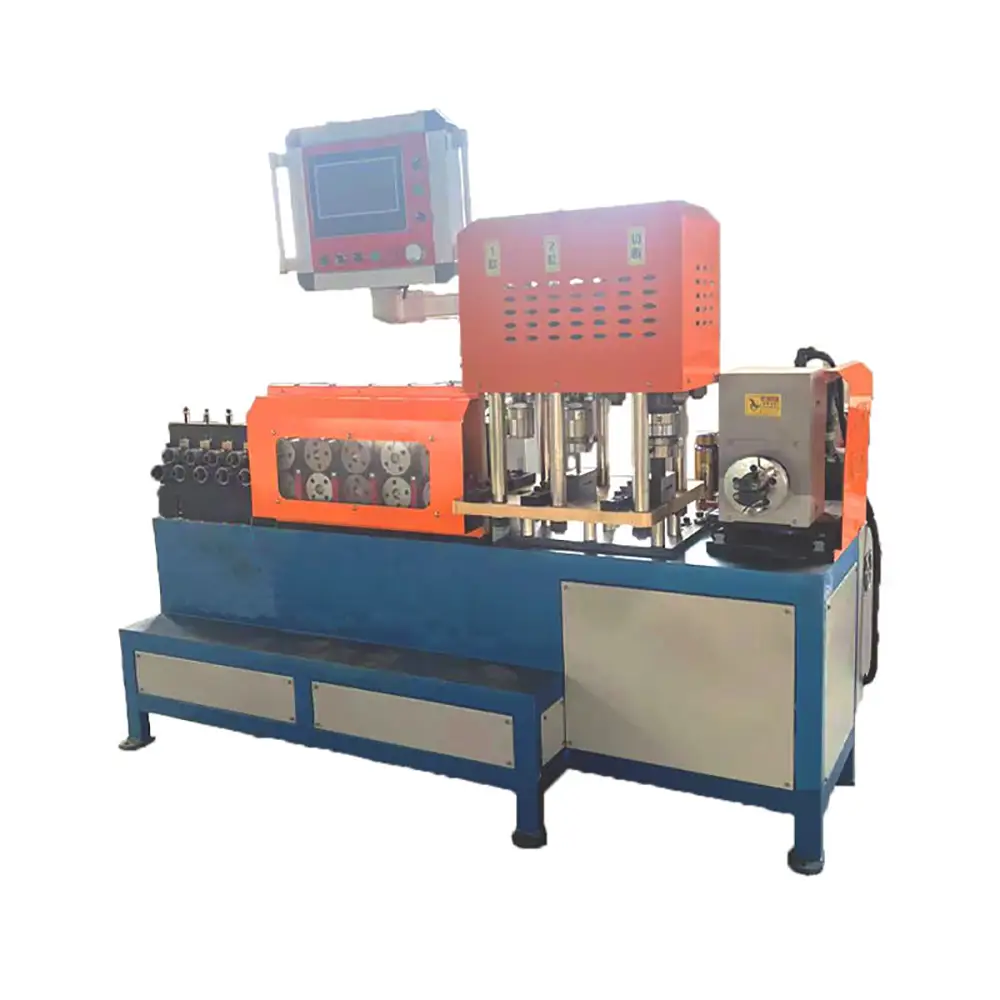
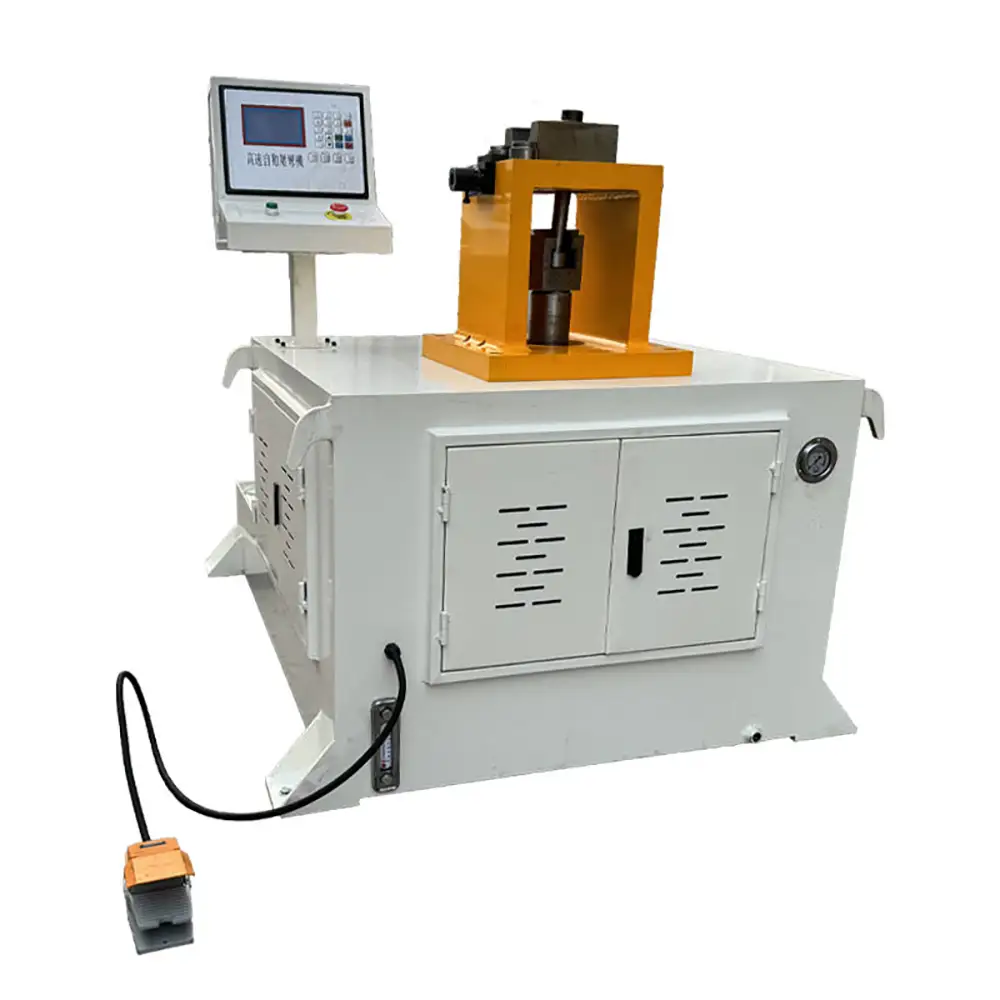
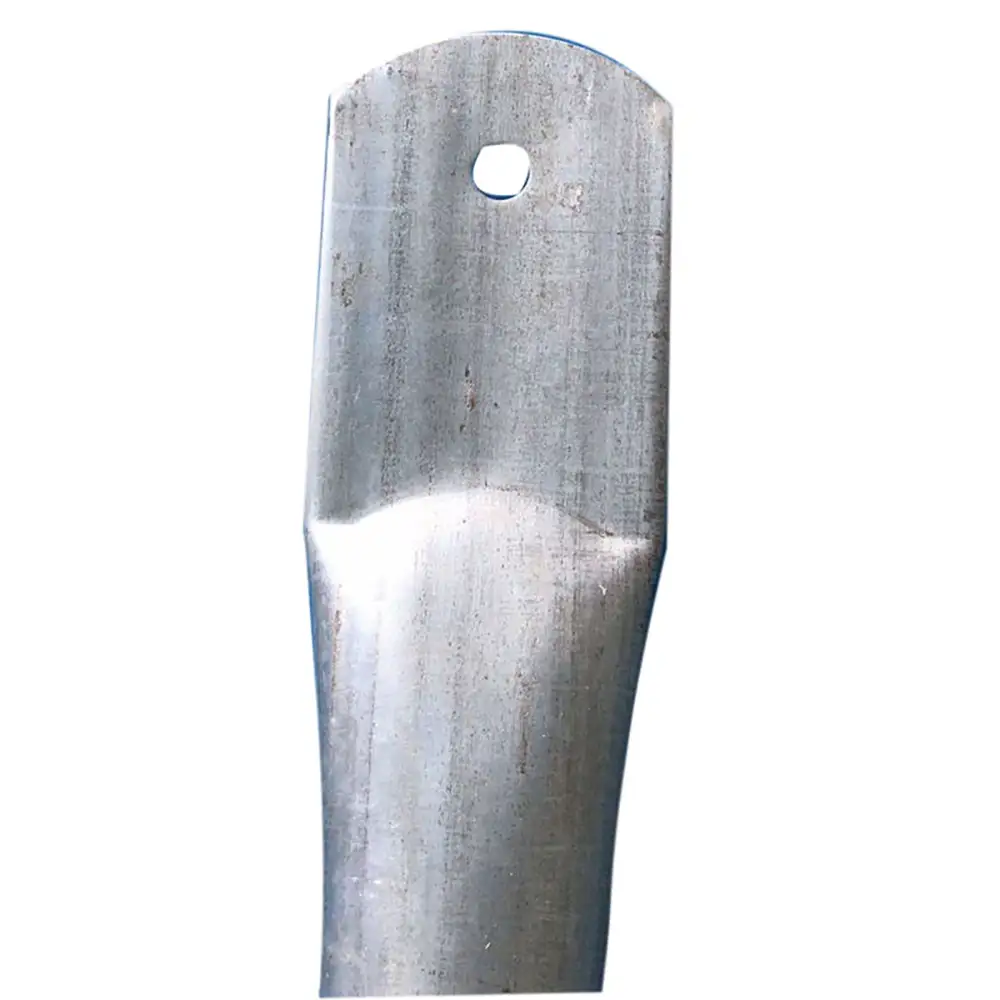
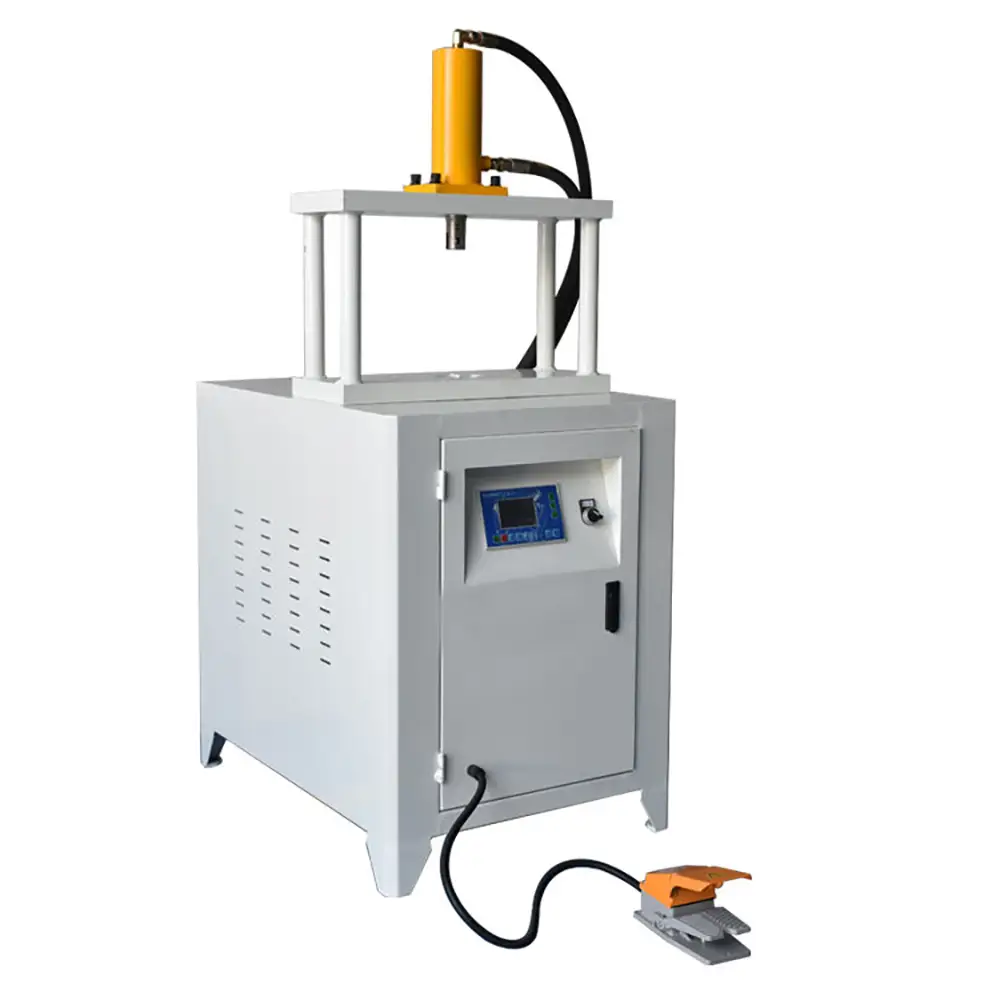
Exhaust Muffler Perforation Machine for High-Quality Hole Punching
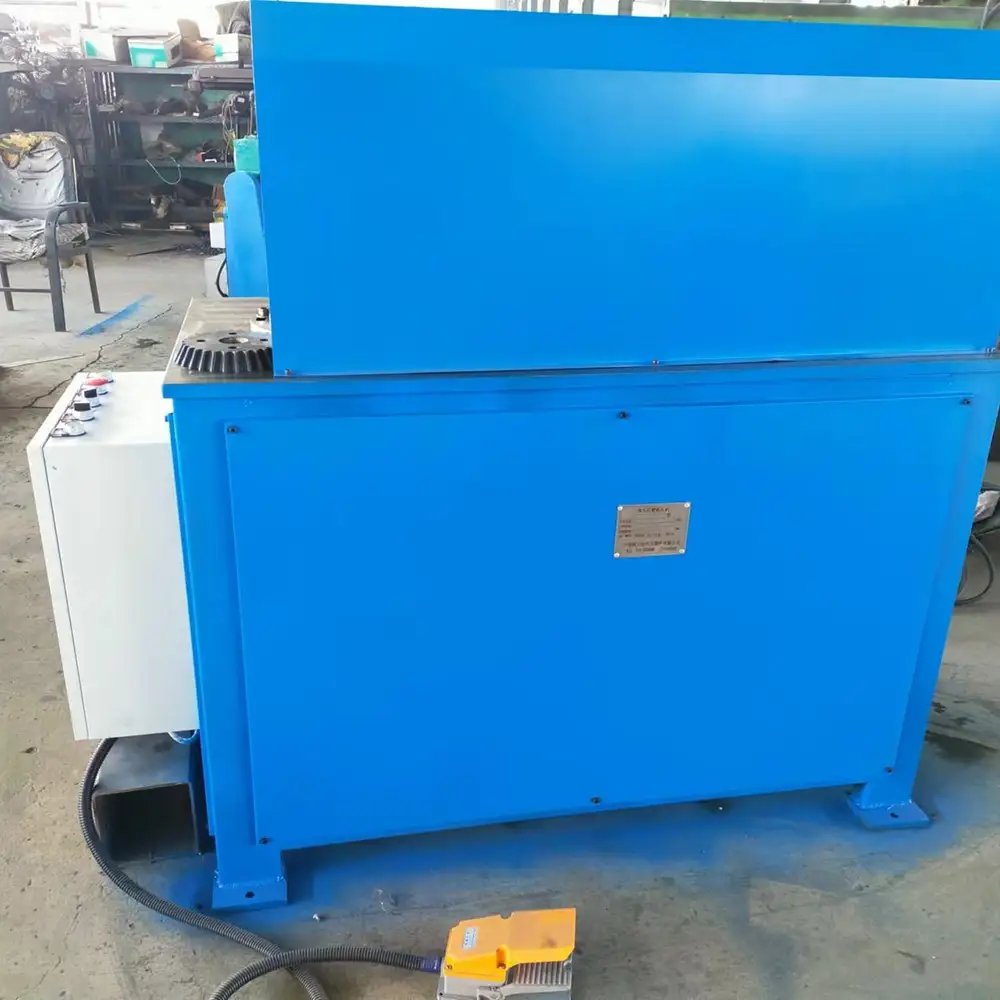
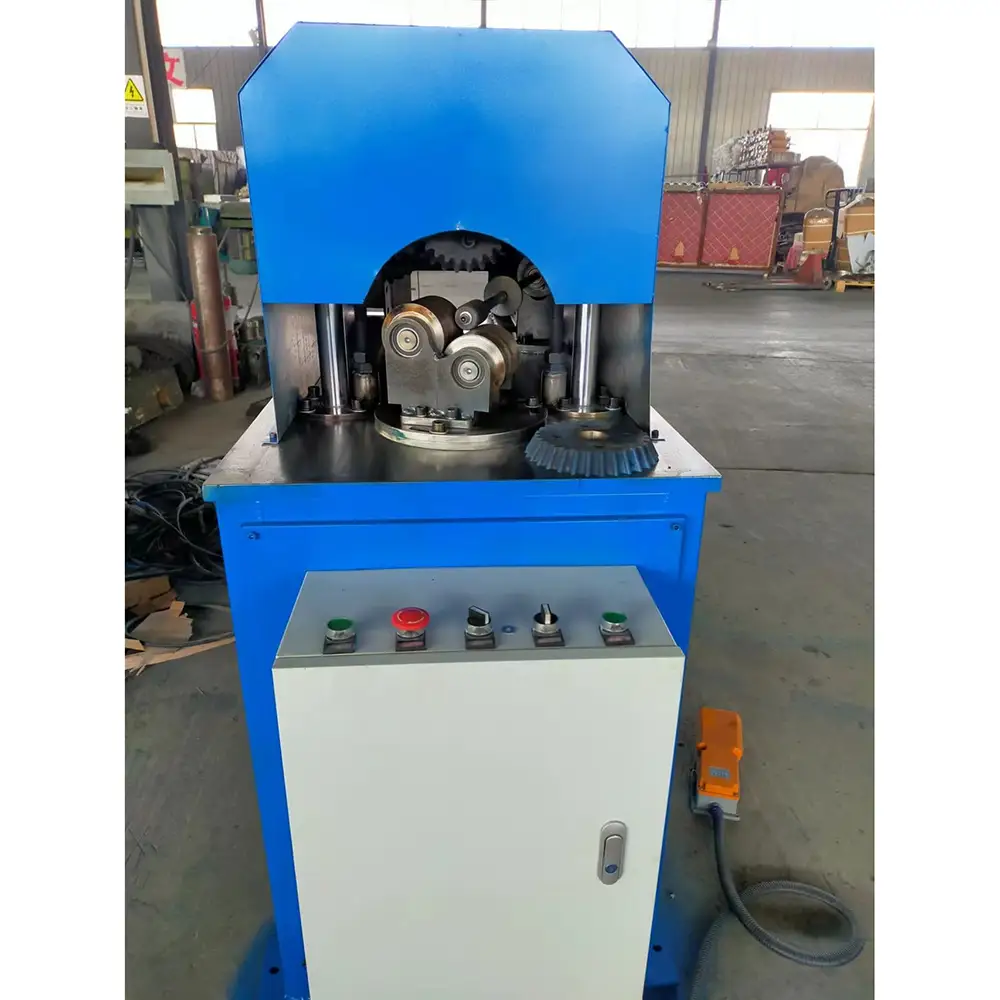
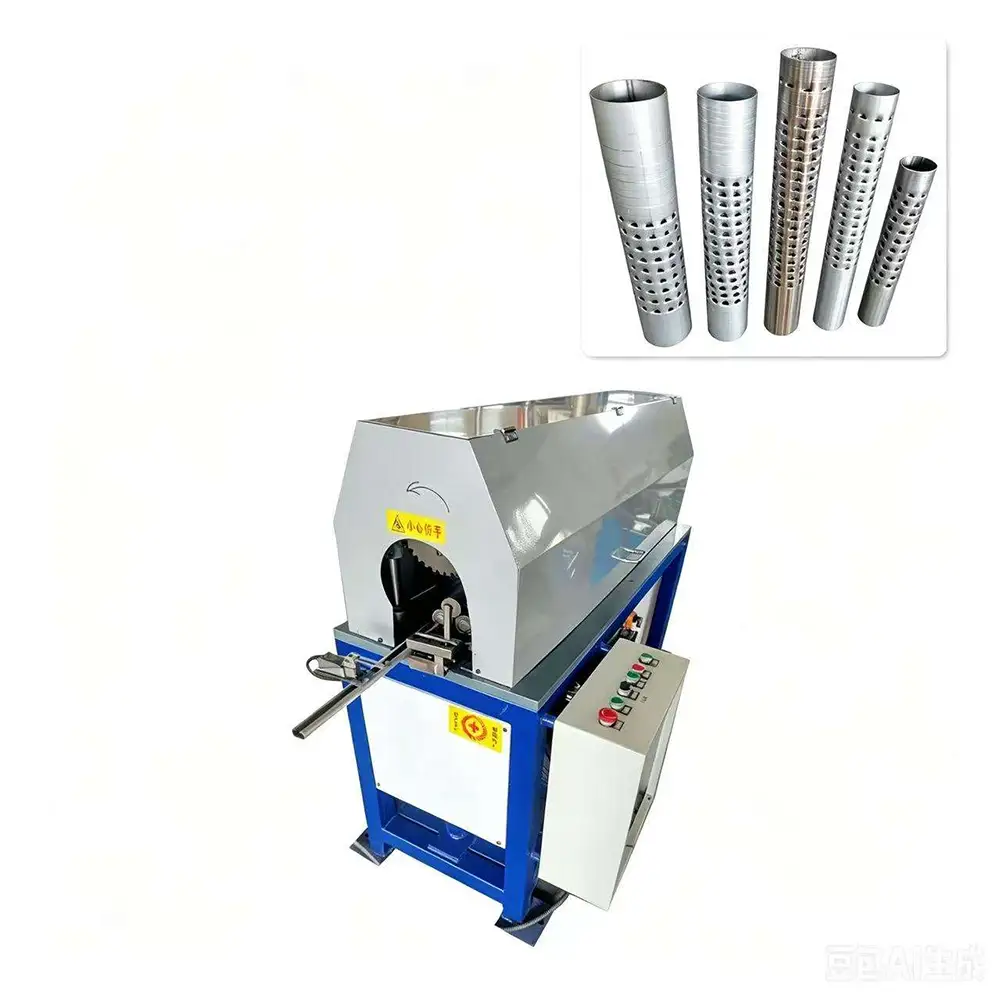
The Exhaust Muffler Perforation Machine is designed for efficient and repeatable hole punching and perforation of exhaust pipes, muffler tubes, perforated tubes, and related metal components. It provides a specialized solution for manufacturers that need consistent hole patterns and reliable processing during exhaust system production.
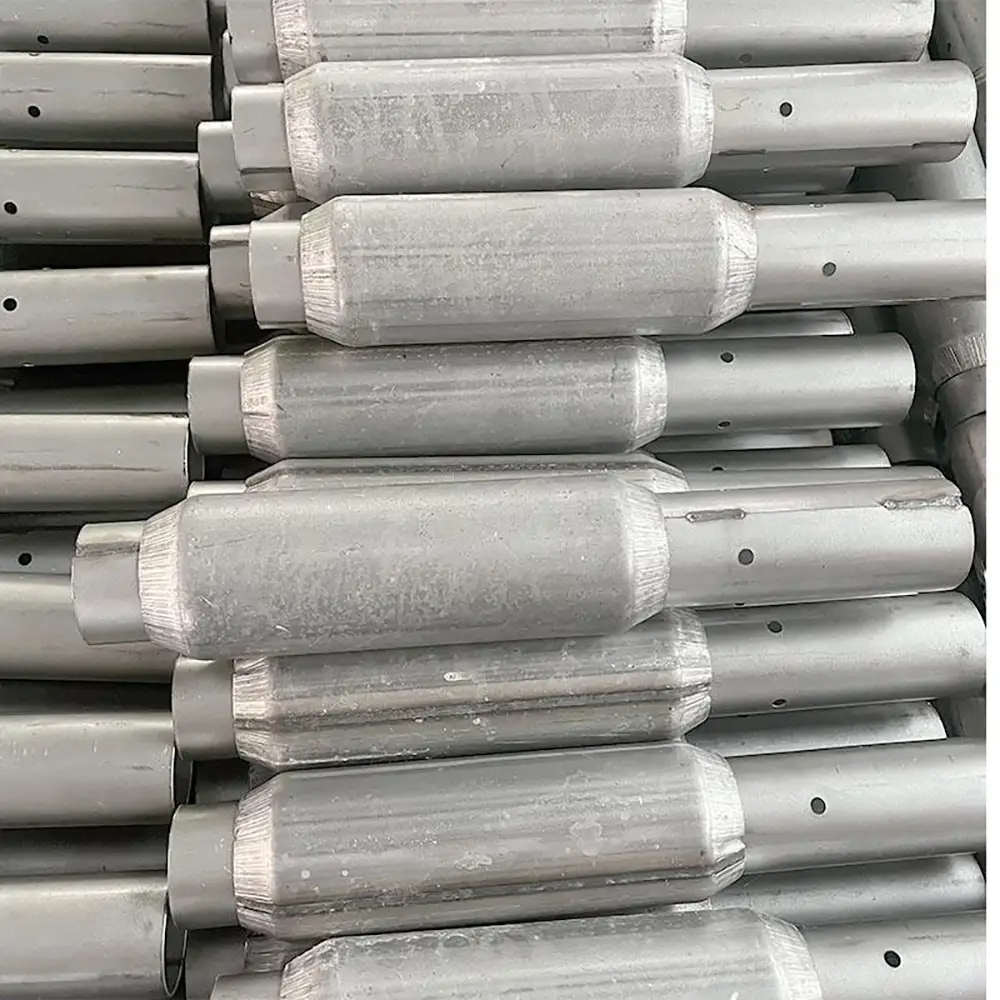
Perforation is an important manufacturing process for many muffler and exhaust components. Perforated tubes can be used as internal components of exhaust systems to help manage exhaust gas flow and acoustic performance according to the overall muffler design. Producing these components requires controlled hole positioning, consistent hole geometry, and suitable tooling.
Compared with manual drilling or individually processing holes, a dedicated perforation machine can provide a more organized production process for repetitive manufacturing. The machine can be configured according to the tube diameter, material, wall thickness, hole size, hole spacing, and required perforation pattern.
Actual punching capacity and production performance depend on the machine configuration, tooling, material properties, tube dimensions, and production requirements.
|
voltage |
220V, 380V |
|
motor power (kw) |
0.4 |
|
power source |
Electromotor |
|
weight (t) |
200 |
|
brand name |
SOAR |
|
dimension(l*w*h) |
760*570*1230mm |
|
Skiving range |
4~ 70mm |
|
Supporting mandrel |
04,05,06,08,10,12,16,20,24,32 |
|
Spindle speeds |
288 r/min |
|
Characteristic |
Spindle rotate in skiving inner rubber, Spindle non-rotation in skiving outer rubber |
|
Accuracy |
0.1-0.2mm |
|
Packing |
Wooden |
Exhaust Muffler Tube Perforation
The primary application of this machine is perforating tubes used in muffler and exhaust system manufacturing. Depending on the product design, the tube may require a series of round holes or other specified perforation patterns along a defined section.
A dedicated exhaust muffler perforation machine helps manufacturers establish repeatable processing positions and reduce manual measurement. Proper fixtures can hold the tube securely during punching, helping maintain consistent hole locations.
The final hole pattern should be determined according to the exhaust system design and engineering requirements. Different muffler structures may require different hole diameters, spacing, quantities, and perforated lengths.
High-Quality Hole Punching
High-quality perforation requires suitable punch and die selection, accurate workholding, and stable machine operation. The punching process creates holes through controlled mechanical force rather than relying on individual manual drilling operations.
Proper tooling can help produce clean and consistent holes while reducing unnecessary deformation of the tube.
Hole quality depends on factors including material type, tube wall thickness, punch geometry, die clearance, tooling condition, punching force, and machine settings.
For stainless steel and other high-strength materials, tooling and process parameters should be selected according to the actual material characteristics.
Stainless Steel Exhaust Pipe Processing
Stainless steel is widely used in exhaust and muffler components because of its corrosion resistance and suitability for elevated-temperature applications.
The machine can be configured for compatible stainless steel tubes and other metal exhaust components. However, the appropriate machine capacity and tooling should be selected according to the stainless steel grade, tube diameter, wall thickness, hole dimensions, and required production volume.
Carbon steel, mild steel, and other compatible metal tubes may also be processed depending on the machine configuration.
Before mass production, sample testing can help confirm hole quality, tooling selection, tube positioning, and finished-product requirements.
Tube Positioning and Fixtures
Accurate tube positioning is essential when producing repeated perforation patterns. A suitable fixture can help prevent unnecessary movement during the punching cycle and maintain the desired relationship between the tube and punching tooling.
Fixtures can be designed according to tube diameter, length, profile, and perforation requirements.
For specialized exhaust products, custom workholding solutions can help accommodate different tube shapes or production requirements.
Customers should provide tube drawings, samples, dimensions, and hole patterns when requesting a customized fixture or tooling solution.
Perforation Patterns
Exhaust muffler tubes may require different perforation arrangements depending on the final exhaust system design.
Common requirements may include:
Straight rows of holes
Multiple circumferential rows
Staggered hole patterns
Repeated hole spacing
Partial tube perforation
Defined perforated sections
Customized hole arrangements
The actual pattern depends on the engineering design of the muffler or exhaust component.
A dedicated machine can help standardize the production process once the correct tooling and positioning parameters have been established.
Production Efficiency
For manufacturers producing exhaust components in batches, an automatic or semi-automatic perforation process can reduce repetitive manual operations.
Instead of marking and drilling individual holes manually, the operator can use dedicated fixtures and machine settings to perform a standardized punching sequence.
Production efficiency depends on tube dimensions, hole quantity, perforation length, machine cycle, tooling arrangement, loading and unloading method, and operator workflow.
For high-volume production, dedicated tooling and optimized fixtures can further improve process consistency.
Applications
The Exhaust Muffler Perforation Machine can be used in several metal fabrication and exhaust component manufacturing applications, including:
Automobile muffler production
Motorcycle exhaust systems
Truck exhaust components
Industrial exhaust systems
Agricultural machinery exhausts
Generator exhaust systems
Construction equipment exhausts
Perforated metal tubes
Muffler internal tubes
Exhaust pipe components
Customized metal tube fabrication
The actual application range depends on the machine's processing capacity and tooling configuration.
Tooling and Customization
Tooling is one of the most important factors in exhaust tube perforation. Punches, dies, fixtures, tube supports, and positioning components can be customized according to the customer's requirements.
Custom tooling may be developed for different tube diameters, hole sizes, hole patterns, perforation lengths, and material thicknesses.
For OEM projects, buyers can provide CAD drawings, tube samples, material information, hole dimensions, hole spacing, and expected production quantities.
This information helps determine the appropriate punching method and tooling configuration.
Quality Control
Quality inspection should focus on hole diameter, hole position, spacing, perforated length, tube deformation, and overall dimensional consistency.
For production batches, first-piece inspection can help verify tooling and machine settings before continuing with larger quantities.
Regular inspection of punches and dies is also important. Tool wear can gradually affect hole quality and dimensional consistency.
For demanding exhaust applications, manufacturers should establish appropriate inspection procedures based on their product drawings and engineering specifications.
Maintenance and Safety
Regular maintenance helps keep the Exhaust Muffler Perforation Machine operating consistently. Operators should inspect punches, dies, fixtures, guides, drive components, electrical systems, and other wear parts according to the manufacturer's maintenance recommendations.
Tooling should be kept clean and properly aligned. Worn punches or dies should be replaced or serviced when required.
Operators should receive appropriate training before operating the machine. Guards, emergency stops, electrical protection, and other safety features should be checked according to the actual machine configuration and applicable local requirements.
Custom & OEM Solutions
The machine can be customized for specific exhaust and muffler production requirements. Custom solutions may include punching tools, dies, tube fixtures, positioning systems, feeding arrangements, perforation patterns, and production layouts.
Whether you manufacture automotive mufflers, motorcycle exhausts, industrial exhaust components, or specialized perforated tubes, providing detailed product drawings and samples allows the machine configuration to be matched to the actual application.
The machine is suitable for manufacturers, wholesalers, distributors, exhaust component suppliers, purchasing agents, and international B2B buyers looking for a dedicated exhaust tube perforation solution.
Why Choose Us
Dedicated Exhaust Perforation — Designed specifically for repetitive hole punching and perforation of exhaust and muffler tubes.
High-Quality Hole Processing — Proper tooling and controlled punching help support consistent hole geometry and positioning.
Stainless Steel Compatibility — Can be configured for compatible stainless steel and other metal exhaust tubes.
Custom Perforation Patterns — Hole size, spacing, arrangement, and perforated sections can be adapted to product requirements.
Dedicated Tube Fixtures — Custom workholding solutions can improve tube positioning and production repeatability.
Production Efficiency — Reduces repetitive manual drilling and supports standardized batch manufacturing.
OEM & ODM Support — Tooling, fixtures, machine configuration, and processing solutions can be customized.
B2B Industrial Solution — Suitable for exhaust manufacturers, metalworking factories, wholesalers, distributors, and industrial buyers.
FAQs
1. What is an exhaust muffler perforation machine?
It is a specialized machine designed to punch or perforate holes in metal tubes used for mufflers, exhaust systems, and related components.
2. What tubes can the machine process?
Depending on the configuration, it can process compatible stainless steel, carbon steel, mild steel, and other metal tubes used for exhaust components.
3. Can it process stainless steel exhaust pipes?
Yes. The machine can be configured for compatible stainless steel tubes. The appropriate tooling should be selected according to the stainless steel grade, thickness, and tube dimensions.
4. What types of holes can it make?
The standard configuration is generally intended for punched holes, while hole size, shape, spacing, and pattern depend on the tooling and machine configuration.
5. Can the perforation pattern be customized?
Yes. Hole spacing, hole quantity, perforated length, and other pattern requirements can be configured through suitable tooling and positioning arrangements.
6. Is the machine automatic?
The automation level depends on the specific configuration. Automatic or semi-automatic feeding, positioning, and punching functions may be available depending on the machine design.
7. Can it be used for motorcycle exhaust pipes?
Yes, when the tube dimensions, material, and perforation requirements are within the machine's configured processing range.
8. Can it produce muffler internal perforated tubes?
Yes. It can be configured for compatible perforated tubes used as internal muffler components, subject to the required tube dimensions and hole pattern.
9. Can custom punching dies be supplied?
Yes. Custom punches, dies, fixtures, tube supports, and positioning components can be designed according to customer requirements.
10. How do I select the right machine?
Provide the tube material, outside diameter, wall thickness, length, hole diameter, hole spacing, perforation pattern, and expected production volume.
11. How can hole quality be maintained?
Proper punch and die selection, suitable die clearance, accurate tube positioning, regular tooling inspection, and appropriate process parameters all contribute to consistent hole quality.
12. Can you provide OEM exhaust perforation solutions?
Yes. OEM solutions can include customized tooling, fixtures, perforation patterns, positioning systems, and machine configurations based on customer drawings or samples.
Prev:
Multi-function Automatic Hydraulic Four Holes Curtain Eyelet Punch Equipment Punching Machine
Next:
5-Station Ladder Multi-Function Punching & Bending Machine
TAG:
Metal Tube Punching Machine,
Exhaust System Manufacturing Machine,
Muffler Manufacturing Machine,
Automotive Muffler Production Machine,
Automatic Exhaust Pipe Punching Machine,
Exhaust Pipe Perforation Equipment,
Exhaust Tube Hole Making Machine,
Perforated Tube Punching Machine,
Industrial Exhaust Pipe Punching Machine,
Custom Exhaust Muffler Punching Machine,
Exhaust Tube Punching Machine,
Exhaust Pipe Punching Machine,
Exhaust Pipe Hole Punching Machine,
Muffler Tube Punching Machine,
Stainless Steel Exhaust Pipe Punching Machine,
Stainless Steel Muffler Punching Machine,
Muffler Tube Hole Punching Machine,
Exhaust Pipe Perforating Machine,
Metal Tube Perforating Machine,
Exhaust Pipe Hole Making Machine,
Muffler Perforation Machine,
Muffler Tube Perforation Machine,
Exhaust Tube Perforation Machine,
Exhaust Muffler Punching Machine,
Exhaust Muffler Perforation Machine,
Related Category:
Exhaust Muffler Perforation Machine,Exhaust Muffler Punching Machine,Muffler Perforation Machine,Exhaust Pipe Perforatin China, suppliers, manufacturers, factory, customized, wholesale, quotation, made in China