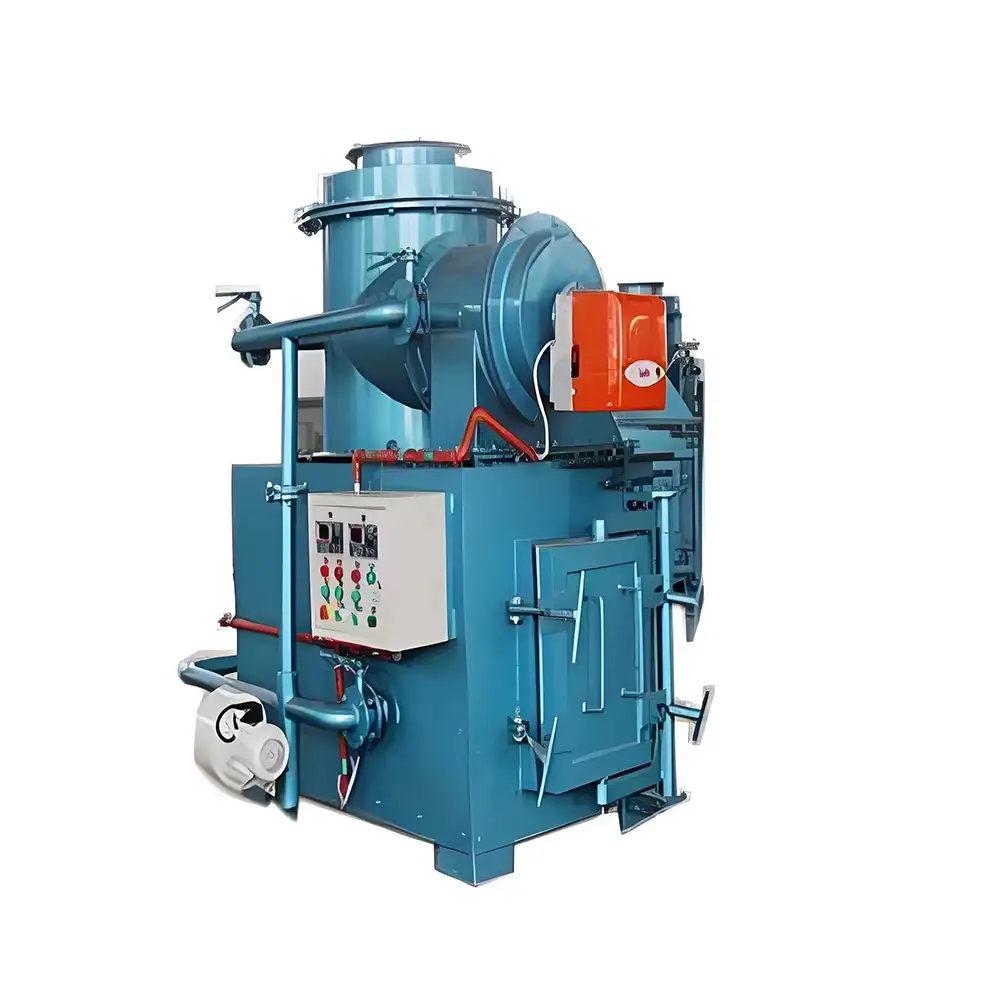
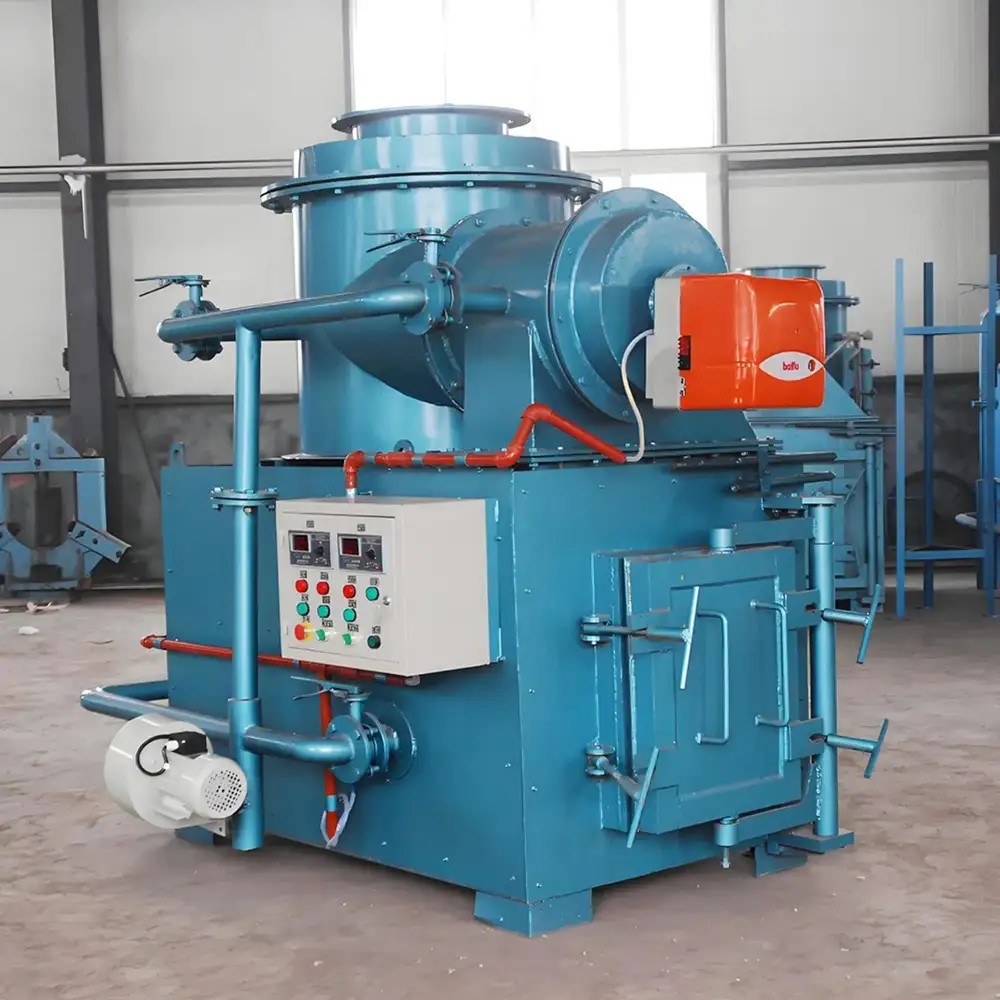
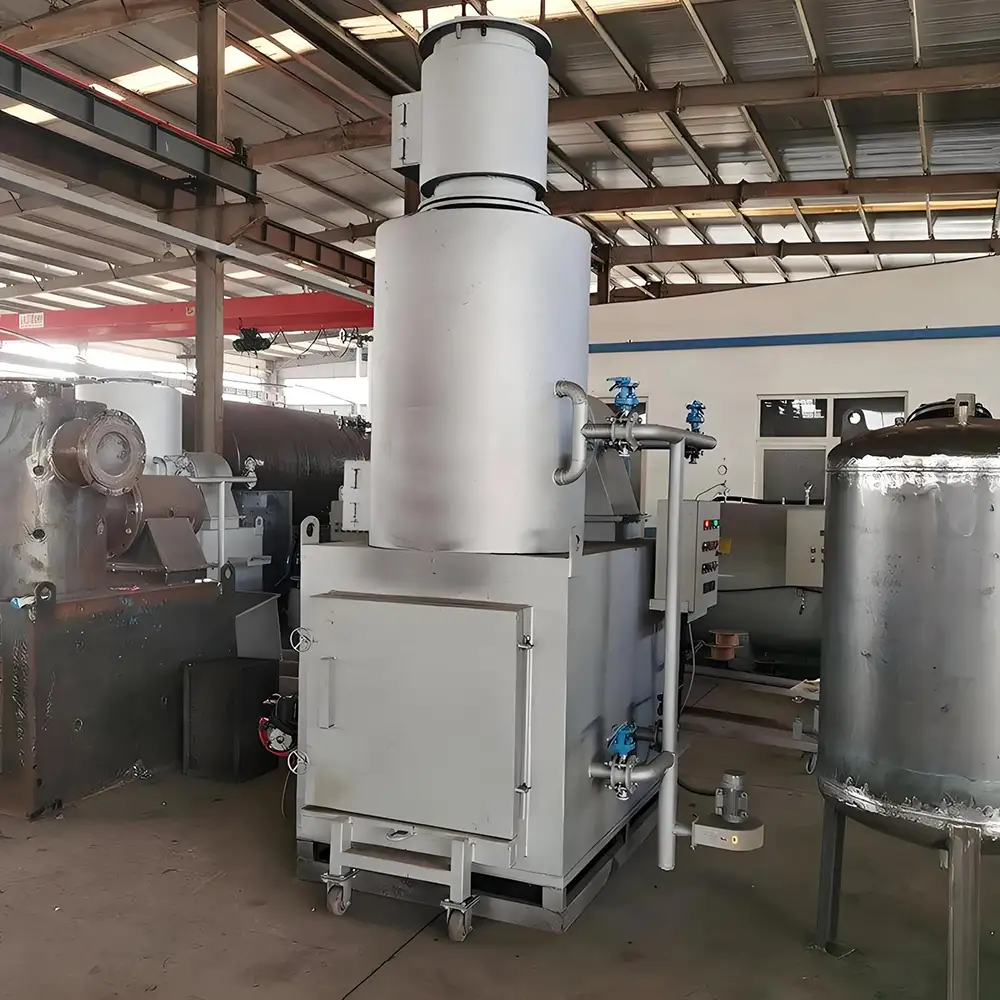
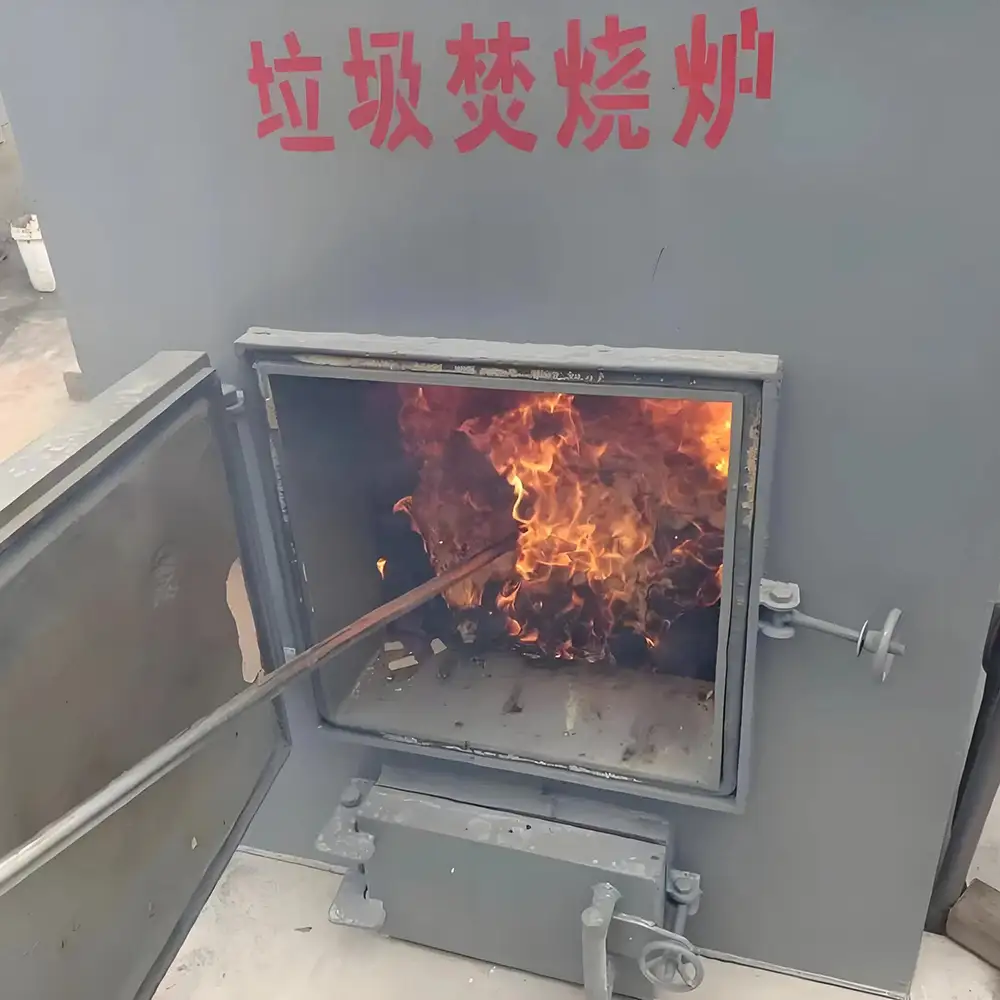
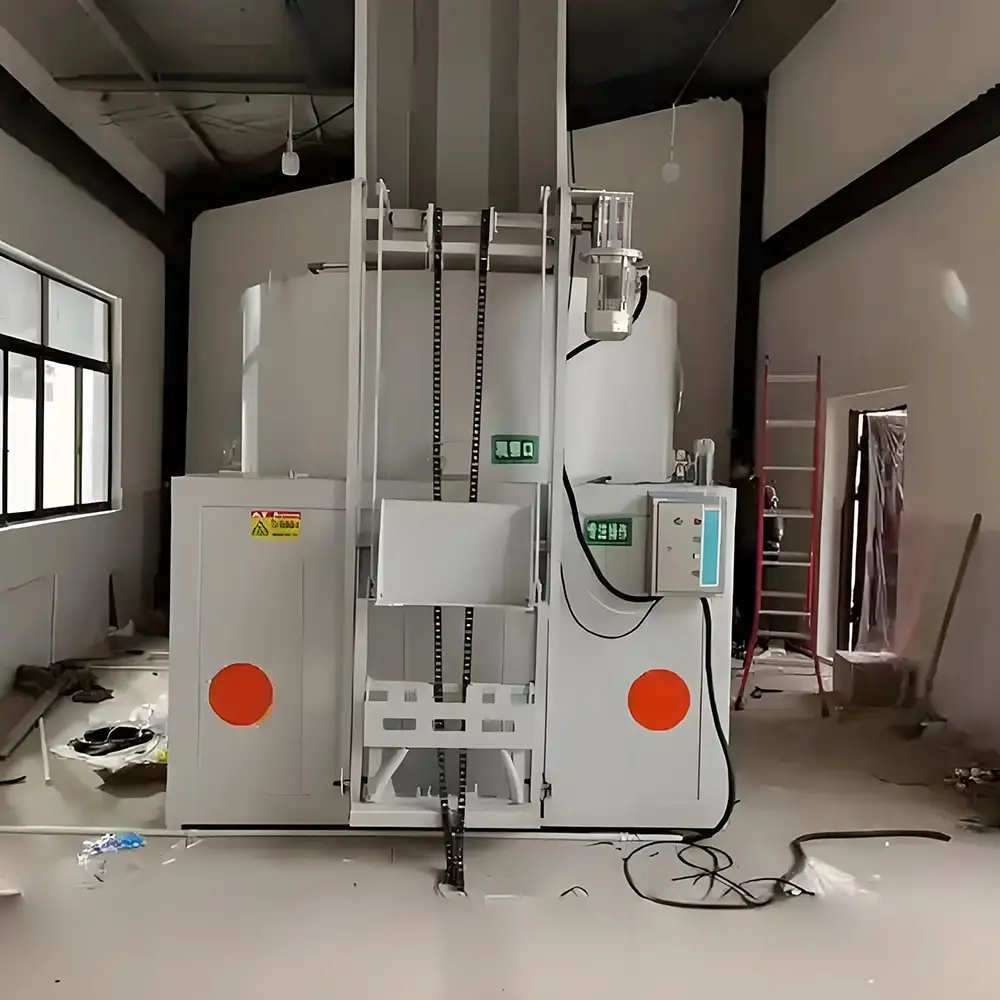
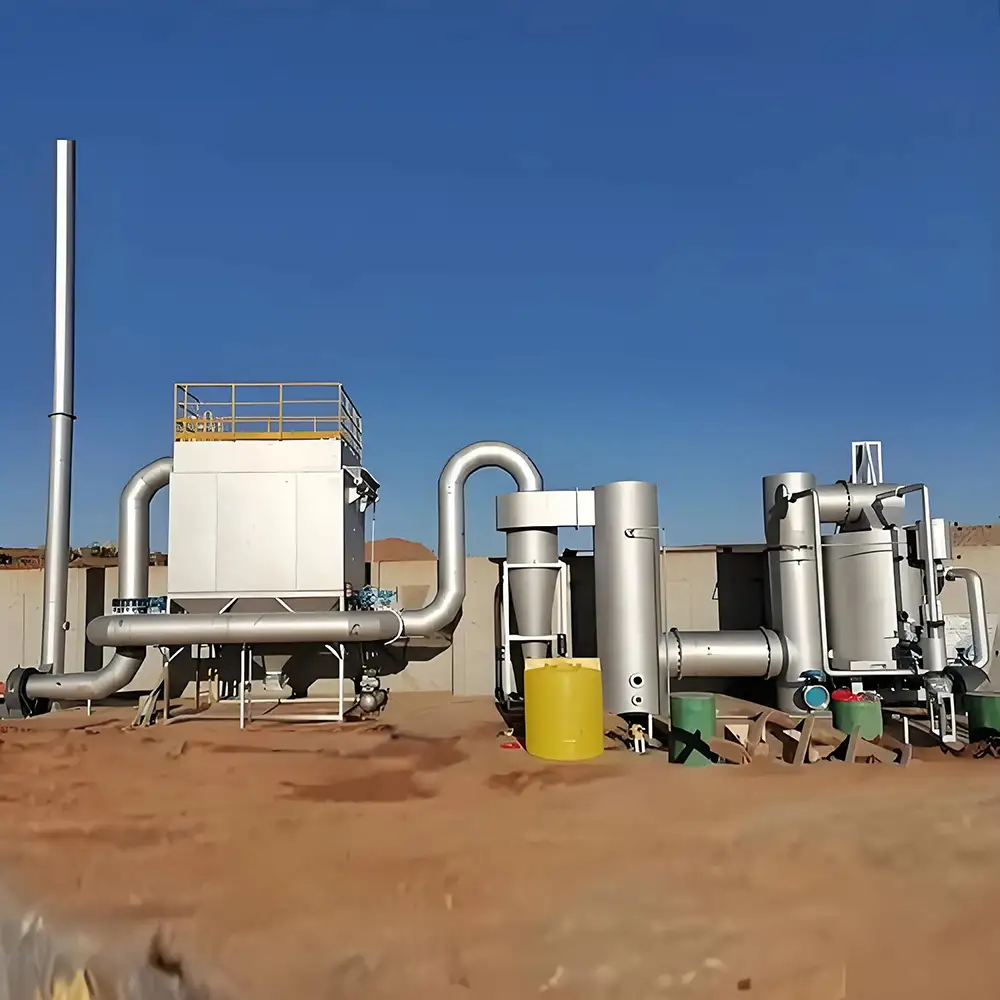
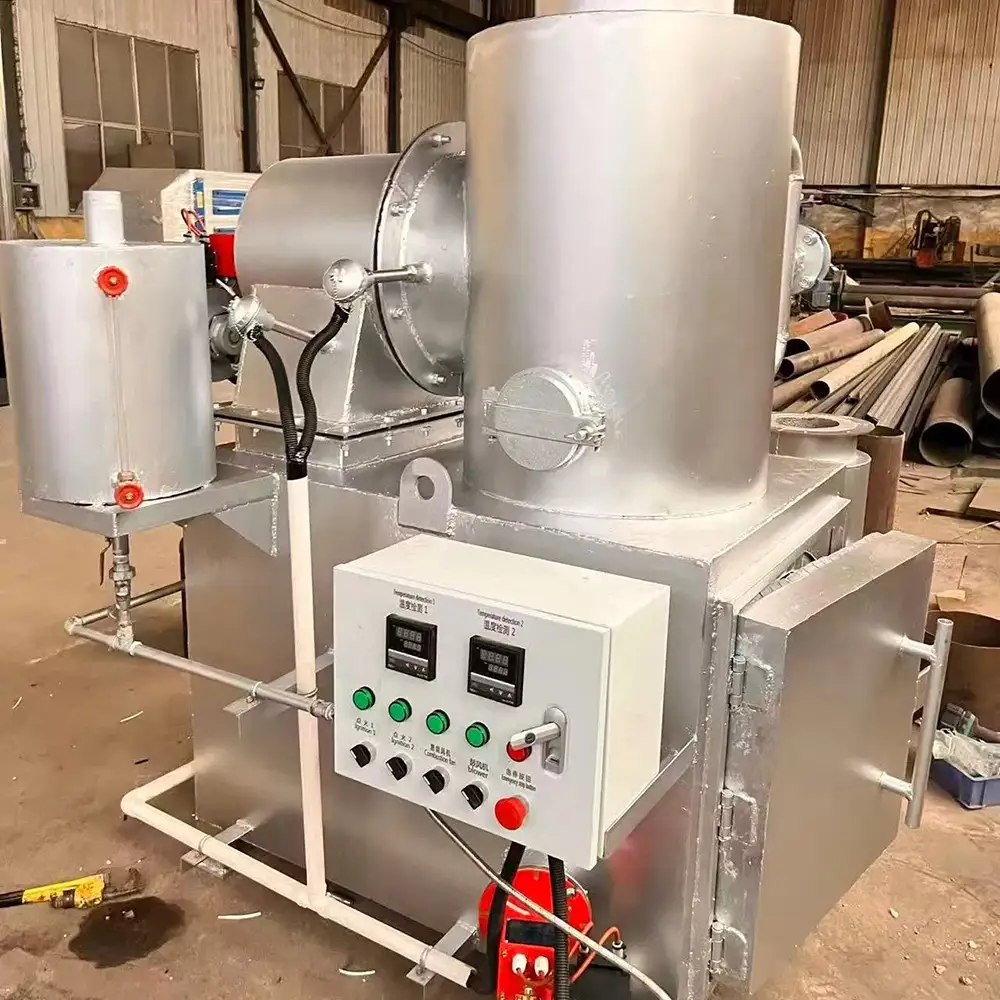
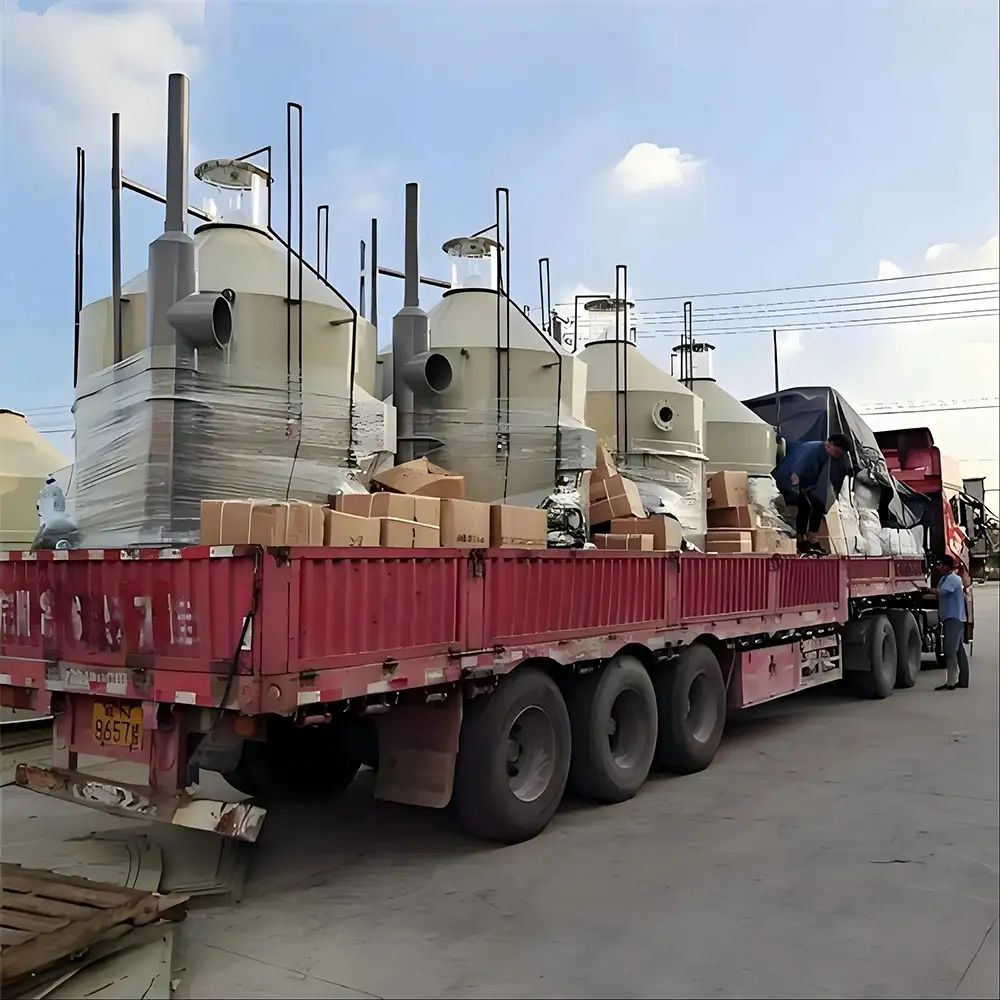
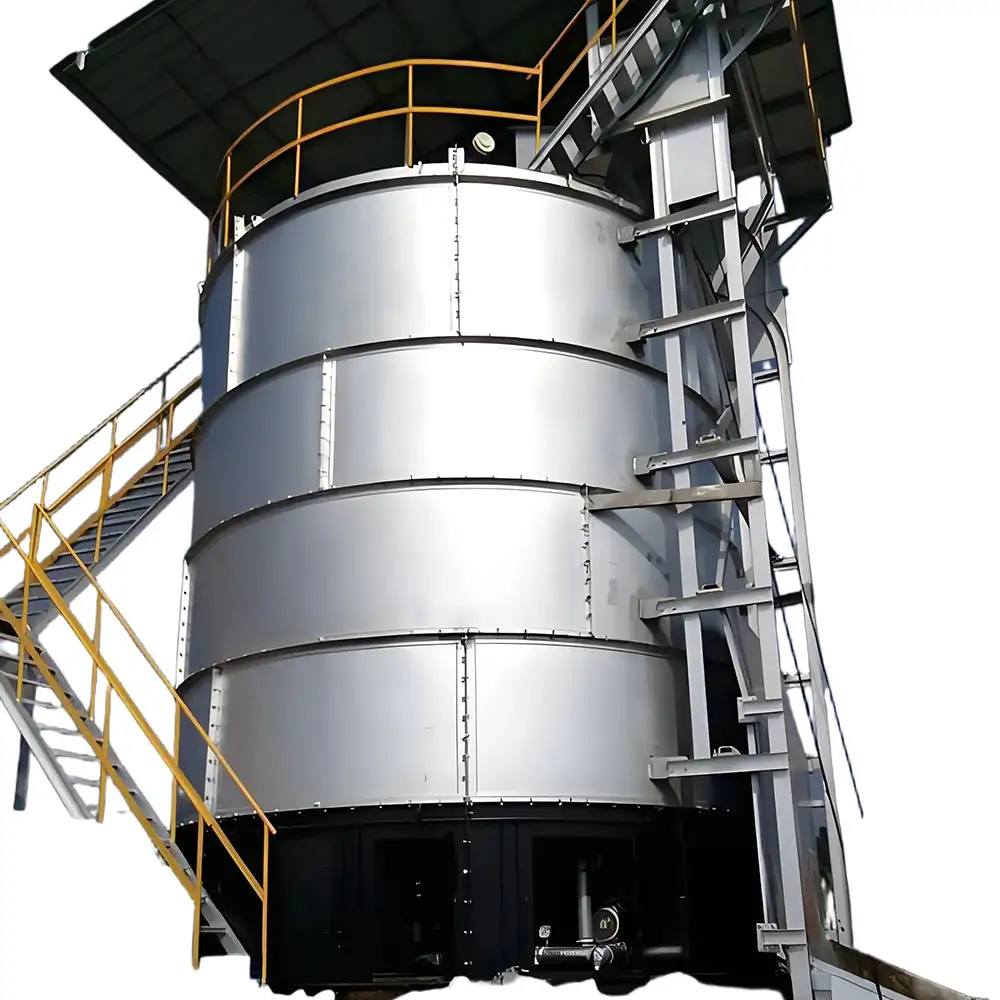
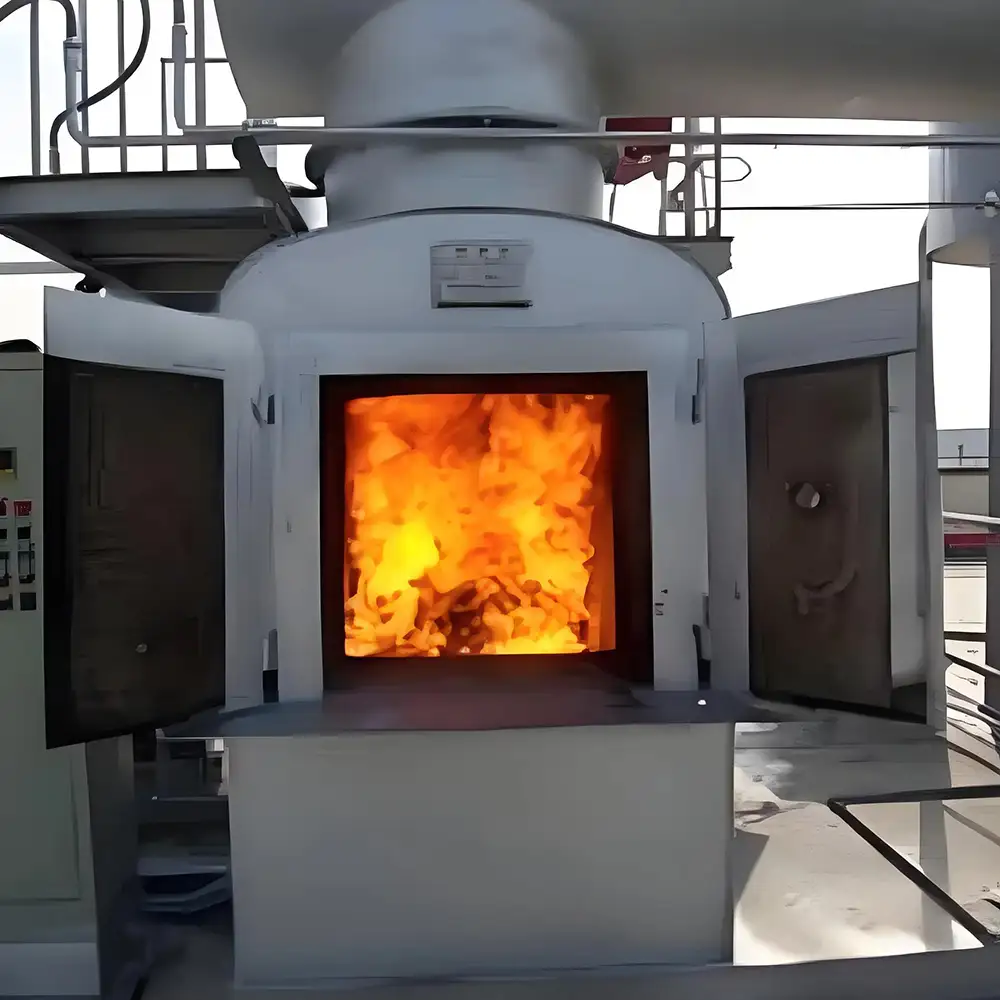
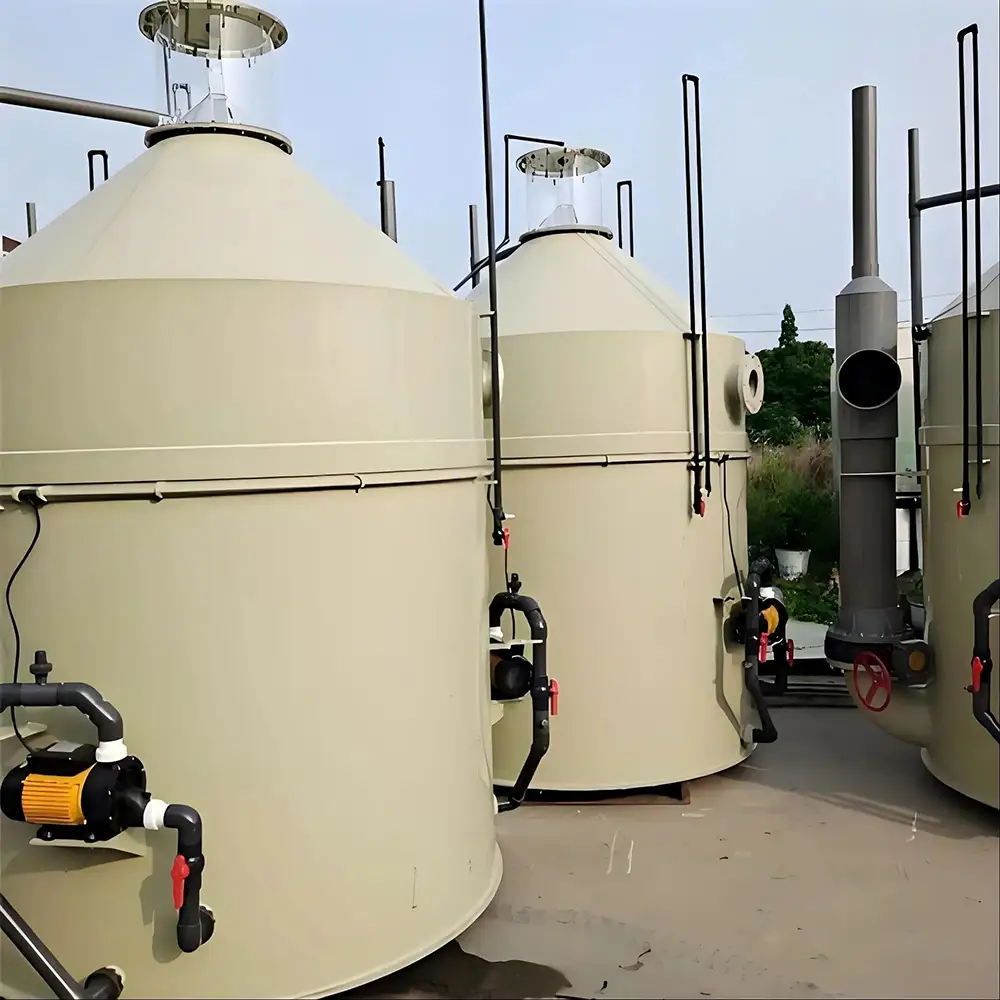
The Hazardous Waste Thermal Destruction Unit Water Treatment Plant Incinerators is an industrial thermal treatment system designed for controlled treatment of suitable hazardous, industrial, and water-treatment-related waste streams. It can be configured for waste materials that require thermal destruction or volume reduction before final residue management.
Industrial facilities and water treatment plants may generate waste streams containing organic contaminants, sludge, concentrated residues, contaminated solids, and other materials that require specialized handling. Depending on their composition, some of these materials may be suitable for controlled thermal treatment.
The system combines controlled combustion, thermal destruction, combustion gas management, and downstream treatment technologies into an integrated industrial waste management solution.
Incinerator is an environmental protection equipment that treats various types of waste (domestic waste, industrial hazardous waste, medical waste, etc.) through high-temperature oxidation. Its core goal is to convert organic waste into carbon dioxide and water, and at the same time achieve pollutant emission reduction and energy recovery through advanced technology. The following systematically introduces the incinerator from multiple dimensions:
1. Definition and core functions
Definition: Incinerator is a comprehensive treatment system that uses high-temperature (usually ≥850ºC) combustion technology, combined with physical, chemical and automatic control methods to achieve waste reduction, harmlessness and resource utilization.
Core functions:
Reduction: 90% reduction in volume and 70% reduction in weight.
Harmlessness: decomposition of dioxins, killing pathogens, and stabilizing heavy metals.
Resource utilization: waste heat power generation or heating to achieve energy recovery.
2. Working principle
High-temperature oxidation:
Organic matter is decomposed into CO, HO and heat in an oxygen-rich environment.
Pollutant control:
Dioxin: Synthesis is blocked by high temperature (≥850ºC) and sufficient residence time (≥2 seconds).
Acidic gases: lime slurry neutralizes SO and HCl.
Particles: Bag/electrostatic precipitator filtration.
3. Core component system
System module Main components Functional description
Pretreatment system Crusher, sorting equipment, garbage storage pit Crushing and classification to improve combustion uniformity
Combustion system Main combustion chamber, secondary combustion chamber, burner, grate/rotary kiln/fluidized bed High temperature decomposition of organic matter, complete incineration of harmful substances
Air supply and cooling Primary/secondary fan, air preheater, quenching tower Optimize combustion efficiency and prevent dioxin resynthesis
Emission control Bag filter, deacidification tower (dry/semi-dry/wet method), SCR/SNCR denitrification, activated carbon injection Remove particulate matter, acid gas, NOx and dioxin
Energy recovery Waste heat boiler, steam turbine generator set, heat exchanger Power generation or heating, improve energy utilization
Automation control PLC/DCS system, CEMS online monitoring, sensor network Real-time control of temperature, air volume, and emissions to ensure safe operation
Ash treatment Water-cooled slag discharger, fly ash solidification device Safe disposal of heavy metal residues
4. Main types and applicable scenarios
Type Structural features Applicable scenarios Advantages
Mechanical grate furnace Stepped grate pushes garbage Urban domestic waste, mixed waste Large processing capacity, suitable for complex components
Rotary kiln incinerator Inclined steel drum rotation (0.5-3 rpm) Hazardous waste, medical waste Fully mixed, good high temperature stability
Fluidized bed incinerator Sand layer fluidization, blast combustion Sludge, high calorific value industrial waste Uniform combustion, low temperature and low NOx emission
Plasma gasification furnace Plasma torch (>5000ºC) cracking waste Radioactive waste, extremely difficult to degrade substances Ultra-high temperature complete decomposition, no secondary pollution
V. Application field
Municipal field:
Treatment of urban domestic waste (average daily processing capacity of 100-3000 tons).
Case: Shanghai Laogang Incineration Plant (processing capacity of 6000 tons/day, power generation of 300 MW).
Industrial field:
Hazardous waste in the chemical and pharmaceutical industries (containing halogens and heavy metal waste).
Medical field:
High temperature sterilization of infectious medical waste (needles, pathological tissues, etc.).
Agricultural field:
Energy utilization of biomass waste such as animal carcasses and straw.
VI. Technical advantages and challenges
Advantages:
Rapid volume reduction: thousands of tons of waste can be processed per day, greatly reducing landfill pressure.
Energy regeneration: 1 ton of garbage generates about 300-600 kWh of electricity (equivalent to 0.3 tons of standard coal).
Strict environmental protection: The emission indicators of modern incineration plants are lower than the natural background value (such as dioxin concentration <0.1 ng TEQ/Nm³).
Challenges:
High investment cost: Construction cost is about 400,000-1 million yuan/ton of processing capacity (excluding land).
Operational complexity: Continuous monitoring of combustion parameters and pollutant emissions is required.
Public perception: "NIMBY effect" makes site selection difficult.
VII. Technical development trend
Ultra-low emission technology:
Coupling SCR+wet deacidification to achieve NOx<50 mg/Nm³ and SO<10 mg/Nm³.
Intelligent control:
AI algorithm optimizes combustion efficiency (such as predicting calorific value fluctuations and automatically adjusting air supply).
Low-carbon innovation:
Biomass coupled incineration (replacing fossil fuels), carbon capture and storage (CCS).
Small modular design:
Distributed treatment of medical or island waste (processing capacity 1-10 tons/day).
VIII. Typical process flow
Feeding: After crushing and sorting, the waste is sent into the furnace by a hydraulic push rod.
Combustion: Organic matter is decomposed in the main combustion zone (900ºC) → Secondary combustion chamber (1100ºC, 2 seconds) is completely oxidized.
Residue heat utilization: Flue gas is passed through the boiler to produce steam → Drive the steam turbine to generate electricity.
Purification and emission: Rapid cooling + deacidification + dust removal + denitrification → Clean gas is discharged through the chimney.
Residue treatment: Fly ash chelation and solidification, bottom ash is made into building materials or landfill.
Summary
As the core facility of modern waste management, the incinerator achieves a balance between pollution reduction and carbon reduction and energy recovery through high-temperature oxidation and multi-stage purification technology. Despite the challenges of cost and public acceptance, with the advancement of technology (such as near-zero emissions and intelligent operation and maintenance), its role in the global circular economy will continue to increase and become an important pillar of sustainable urban development.
Hazardous Waste Thermal Destruction
Thermal destruction uses controlled heat and combustion conditions to break down suitable combustible components in waste. A properly designed thermal treatment system provides controlled feeding, combustion air, temperature management, residence time, and gas treatment.
The actual thermal process must be designed according to the chemical and physical characteristics of the waste. Feed analysis is essential when evaluating hazardous waste applications because different substances may require different combustion and flue gas treatment configurations.
Water Treatment Plant Incinerator
A Water Treatment Plant Incinerator can be integrated into industrial wastewater and water treatment facilities where suitable sludge, residues, or concentrated organic waste require thermal treatment.
Wastewater treatment processes can produce sludge with varying levels of moisture, organic matter, inorganic solids, and chemical contaminants. Depending on its composition, properly prepared sludge may be treated thermally to reduce organic content and waste volume.
Hazardous Waste Incinerator
A Hazardous Waste Incinerator requires careful engineering because hazardous materials can contain corrosive, toxic, reactive, or otherwise regulated components.
The equipment can be configured with appropriate combustion chambers, refractory materials, feeding systems, secondary combustion, flue gas treatment, monitoring, and safety features according to the waste characteristics.
Not every hazardous waste stream is suitable for the same thermal process. Chemical compatibility and regulatory requirements must be evaluated before system selection.
Multi-Stage Thermal Treatment
A multi-stage combustion arrangement can separate the treatment of solid waste and combustion gases. The primary chamber receives and thermally treats the solid or semi-solid feed, while a secondary chamber can provide additional oxidation of combustible gases.
This configuration can support more controlled gas-phase combustion and provide additional residence time before flue gas enters downstream treatment equipment.
Primary Combustion Chamber
The primary chamber is designed to receive suitable waste and expose it to controlled thermal conditions. Depending on the incinerator design, the chamber may be stationary, rotary, or another specialized configuration.
Controlled feeding and combustion air distribution help maintain stable thermal treatment. Chamber construction and refractory lining are selected according to the operating temperature and waste chemistry.
Secondary Combustion Chamber
Combustion gases may contain unburned or partially oxidized compounds. A secondary combustion chamber provides additional controlled thermal treatment for these gases.
The secondary stage can be designed with appropriate air injection, temperature monitoring, burner support, and residence conditions according to the waste characteristics and project requirements.
Hazardous Sludge Treatment
Water treatment plants and industrial wastewater facilities may produce sludge containing organic contaminants and other concentrated materials. When technically appropriate, thermal treatment can be used as part of the sludge management process.
Sludge moisture content is an important consideration because high water content can increase energy requirements. Dewatering, drying, or other pretreatment may therefore be integrated into the overall system.
Industrial Wastewater Residue Treatment
Industrial wastewater treatment can generate concentrated residues from filtration, separation, evaporation, chemical treatment, or biological processes.
Some compatible organic residues may be considered for thermal destruction. The system configuration should be based on waste composition, calorific value, moisture, ash content, corrosiveness, and other relevant characteristics.
Corrosion-Resistant Construction
Hazardous and industrial waste may contain acidic, alkaline, saline, or chemically aggressive substances. Equipment materials must therefore be selected according to the actual feed and process conditions.
Suitable refractory linings, corrosion-resistant components, protective coatings, and appropriate structural materials can be considered where required.
Controlled Waste Feeding
Controlled feeding is important for maintaining stable combustion conditions. The system can be equipped with suitable hoppers, conveyors, pumps, screw feeders, hydraulic feeding systems, or other mechanisms according to the physical form of the waste.
Feeding equipment should be selected according to waste viscosity, particle size, moisture, bulk density, packaging, and chemical characteristics.
Flue Gas Treatment
Thermal treatment generates flue gas that may contain particulate matter, acid gases, volatile compounds, and other combustion products depending on the feed material.
A complete system can incorporate suitable gas cooling, dust collection, scrubbing, filtration, adsorption, and other treatment technologies. The final configuration should be determined by waste analysis, process conditions, emission requirements, and local regulations.
Emission Monitoring
Industrial hazardous waste treatment requires appropriate process and emission monitoring. The system can incorporate temperature sensors, pressure monitoring, oxygen monitoring, flow measurement, and other instrumentation.
Additional emission monitoring equipment can be included according to the facility's regulatory requirements and environmental management system.
Waste Volume Reduction
Thermal treatment can significantly reduce the volume of suitable combustible waste by converting organic components into combustion gases and leaving a smaller quantity of solid residue.
Actual volume reduction depends on the waste composition, moisture content, ash content, and operating conditions. Residual ash must be evaluated and managed according to its characteristics and applicable regulations.
High-Moisture Waste
Water treatment sludge can contain substantial moisture, which influences combustion efficiency and auxiliary fuel requirements.
For high-moisture feedstocks, upstream dewatering, drying, or concentration can be considered. Heat recovery from the thermal process may also be evaluated for suitable drying or process heating applications.
Automated Process Control
The thermal destruction unit can incorporate automated controls for feeding, burners, combustion air, temperature, pressure, secondary combustion, and other process parameters.
A centralized control system can help operators monitor the thermal treatment process and respond to changes in feed conditions. Automation level can be selected according to the project requirements.
Heat Recovery Options
Thermal energy generated during waste treatment may provide opportunities for heat recovery. Depending on the process design, recovered heat can potentially support combustion air preheating, sludge drying, hot water production, or other suitable plant requirements.
Heat recovery should be evaluated based on the waste's calorific value, operating schedule, thermal balance, and available heat demand.
Integrated Water Treatment Application
The incinerator can form one stage of a broader water treatment or wastewater treatment process. Upstream processes may include screening, clarification, dewatering, filtration, concentration, or sludge handling.
Downstream processes may include flue gas treatment, ash handling, monitoring, and final residue management.
Customized Hazardous Waste Treatment
Hazardous waste characteristics vary greatly between industries. Chemical plants, pharmaceutical facilities, laboratories, metal-processing factories, and water treatment plants may generate completely different waste streams.
For this reason, system engineering should be based on actual waste analysis. Configuration can include combustion chambers, burners, feeding systems, refractory materials, secondary combustion, gas treatment, ash handling, instrumentation, and automation.
B2B Industrial Waste Treatment Solution
For water treatment plants, industrial factories, environmental engineering companies, waste management contractors, chemical facilities, pharmaceutical operations, and other industrial projects, the Hazardous Waste Thermal Destruction Unit provides a controlled thermal treatment option for compatible waste streams.
Customers can provide waste composition, moisture content, calorific value, daily quantity, physical form, chemical characteristics, operating schedule, and applicable environmental requirements for technical evaluation.
Key Features
Hazardous Waste Thermal Destruction
Industrial Thermal Waste Treatment
Water Treatment Plant Application
Multi-Stage Combustion
Primary And Secondary Combustion
Controlled Waste Feeding
Corrosion-Resistant Material Options
Refractory Lined Combustion Chambers
Integrated Flue Gas Treatment
Automated Process Monitoring
Ash Handling System
Customized Thermal Treatment Configuration
Main Applications
Water Treatment Plants
Industrial Wastewater Treatment
Hazardous Waste Treatment
Industrial Waste Treatment
Hazardous Sludge Treatment
Chemical Industry Waste
Pharmaceutical Waste
Laboratory Waste
Industrial Organic Residues
Wastewater Treatment Sludge
Contaminated Industrial Waste
Thermal Waste Treatment Facilities
FAQs
1. What Is A Hazardous Waste Thermal Destruction Unit?
It is an industrial thermal treatment system designed to process suitable hazardous and industrial waste under controlled combustion and gas-treatment conditions.
2. Can It Be Used In A Water Treatment Plant?
Yes. It can be integrated into suitable water and wastewater treatment facilities for compatible sludge, organic residues, and other waste streams.
3. Can It Treat Hazardous Waste?
It can be configured for suitable hazardous waste applications, but the actual waste composition must be evaluated before equipment selection to determine the appropriate thermal and gas-treatment process.
4. What Types Of Waste Can Be Treated?
Potential applications include suitable industrial sludge, organic residues, contaminated solids, wastewater treatment residues, and other compatible combustible materials.
5. Does Hazardous Waste Require Pretreatment?
Pretreatment requirements depend on the waste. Dewatering, size reduction, mixing, concentration, neutralization, or other preparation may be necessary depending on its physical and chemical properties.
6. Can The System Include A Secondary Combustion Chamber?
Yes. A secondary combustion chamber can be incorporated to provide additional thermal treatment of combustible gases generated during primary combustion.
7. Does It Include Flue Gas Treatment?
Flue gas treatment can be integrated according to the waste composition and applicable environmental requirements. Equipment may include cooling, dust collection, scrubbing, filtration, or adsorption systems.
8. Can High-Moisture Sludge Be Treated?
Suitable high-moisture sludge may be treated, but moisture content has a significant effect on energy requirements. Dewatering or drying may be incorporated into the overall process.
9. Can The Thermal Destruction Unit Be Customized?
Yes. Feeding, combustion chambers, burners, refractory materials, secondary combustion, flue gas treatment, ash handling, automation, and monitoring can be configured according to the project.
10. What Information Is Needed For System Design?
Useful information includes waste type, chemical composition, moisture, calorific value, ash content, daily processing quantity, physical form, corrosiveness, operating schedule, and local environmental requirements.
Why Choose Us
Industrial Thermal Treatment Experience
We provide thermal waste treatment equipment for industrial, wastewater, sludge, and other specialized waste applications where controlled thermal processing is required.
Waste-Based System Engineering
Hazardous waste varies significantly between industries. We evaluate waste characteristics and process requirements to help determine appropriate combustion, feeding, refractory, and gas-treatment configurations.
Complete Flue Gas Treatment Options
The thermal treatment unit can be integrated with appropriate cooling, dust removal, scrubbing, filtration, adsorption, and monitoring equipment according to project requirements.
Customized Equipment Configuration
Feeding systems, combustion chambers, burners, secondary combustion, ash discharge, refractory materials, control systems, and supporting equipment can be configured for the intended application.
B2B Project Support
We support international customers with technical communication, process design assistance, equipment drawings, documentation, export packaging, shipping coordination, installation guidance, and after-sales support.
Integrated Water Treatment Application
The system can be incorporated into a larger wastewater and sludge treatment process, connecting upstream dewatering or concentration with thermal treatment and downstream flue gas and residue management.
Prev:Sorry, no information
Next:
Rotary Kiln Multi-Stage Combustion Facility Animal Incinerator
TAG:
Thermal Waste Treatment Equipment,
Waste Incineration Equipment,
Industrial Waste Treatment Equipment,
Industrial Sludge Incinerator,
Sludge Thermal Treatment Equipment,
Industrial Waste Combustion System,
Multi Stage Thermal Destruction,
Industrial Thermal Destruction,
Industrial Waste Thermal Destruction,
Industrial Waste Incineration Plant,
Thermal Waste Destruction Equipment,
Thermal Waste Disposal System,
Waste Incineration System,
Wastewater Treatment Incinerator,
Wastewater Sludge Incinerator,
Multi Stage Combustion Incinerator,
Wastewater Treatment Sludge Incinerator,
Hazardous Sludge Incinerator,
Hazardous Sludge Treatment Equipment,
Hazardous Sludge Thermal Treatment,
Industrial Sludge Thermal Treatment,
Multi Stage Thermal Treatment,
Water Treatment Incinerator,
Water Treatment Plant Incinerator,
Industrial Waste Disposal Equipment,
Industrial Waste Treatment System,
Water Treatment Waste Incinerator,
Industrial Waste Thermal Treatment System,
Industrial Waste Incinerator,
Industrial Waste Incineration Equipment,
Related Category:
Hazardous Waste Thermal Destruction Unit, Hazardous Waste Incinerator, Water Treatment Plant Incinerator, Industrial Was China, suppliers, manufacturers, factory, customized, wholesale, quotation, made in China