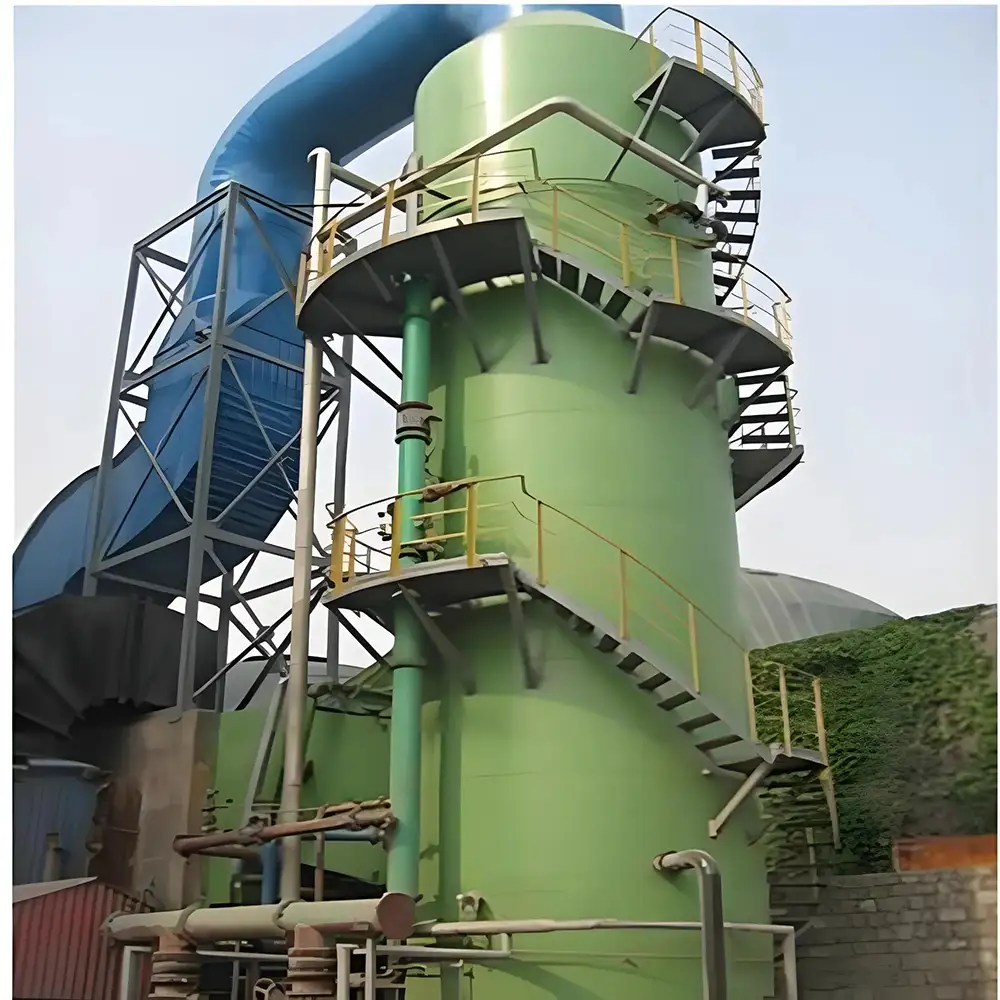
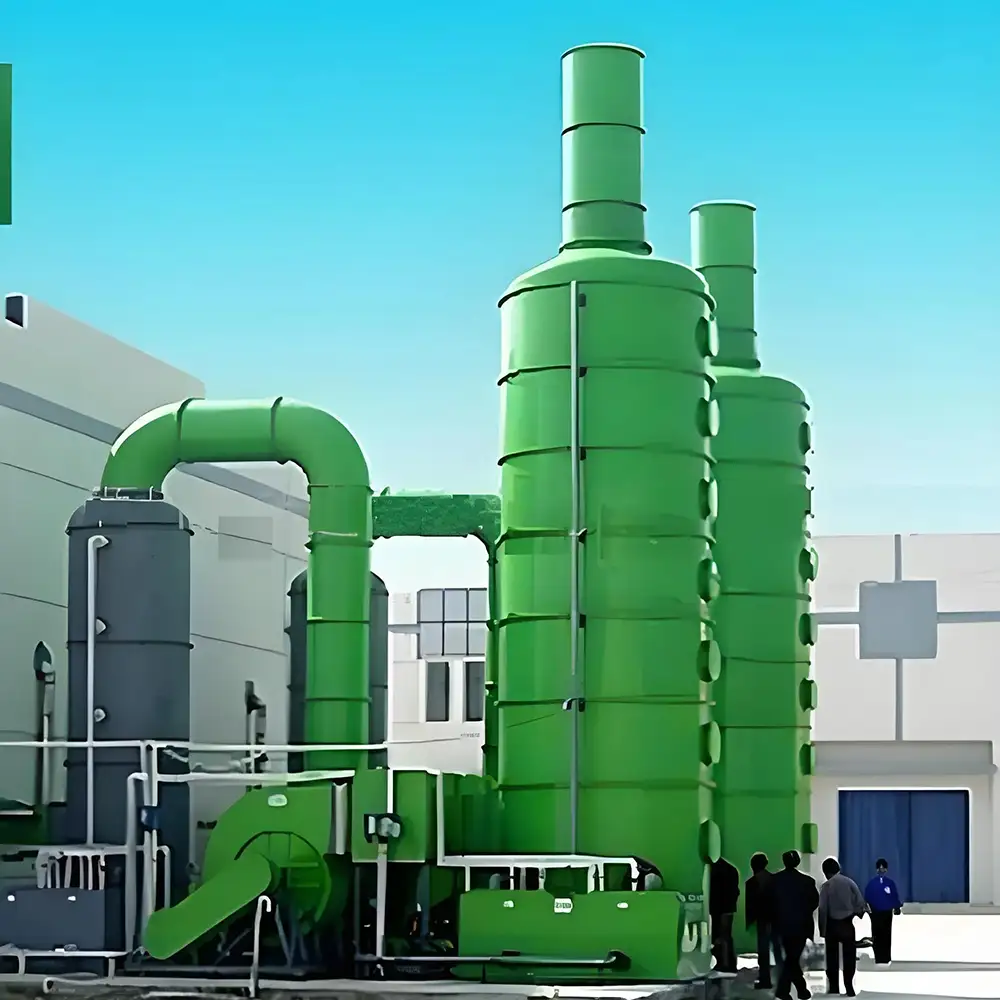
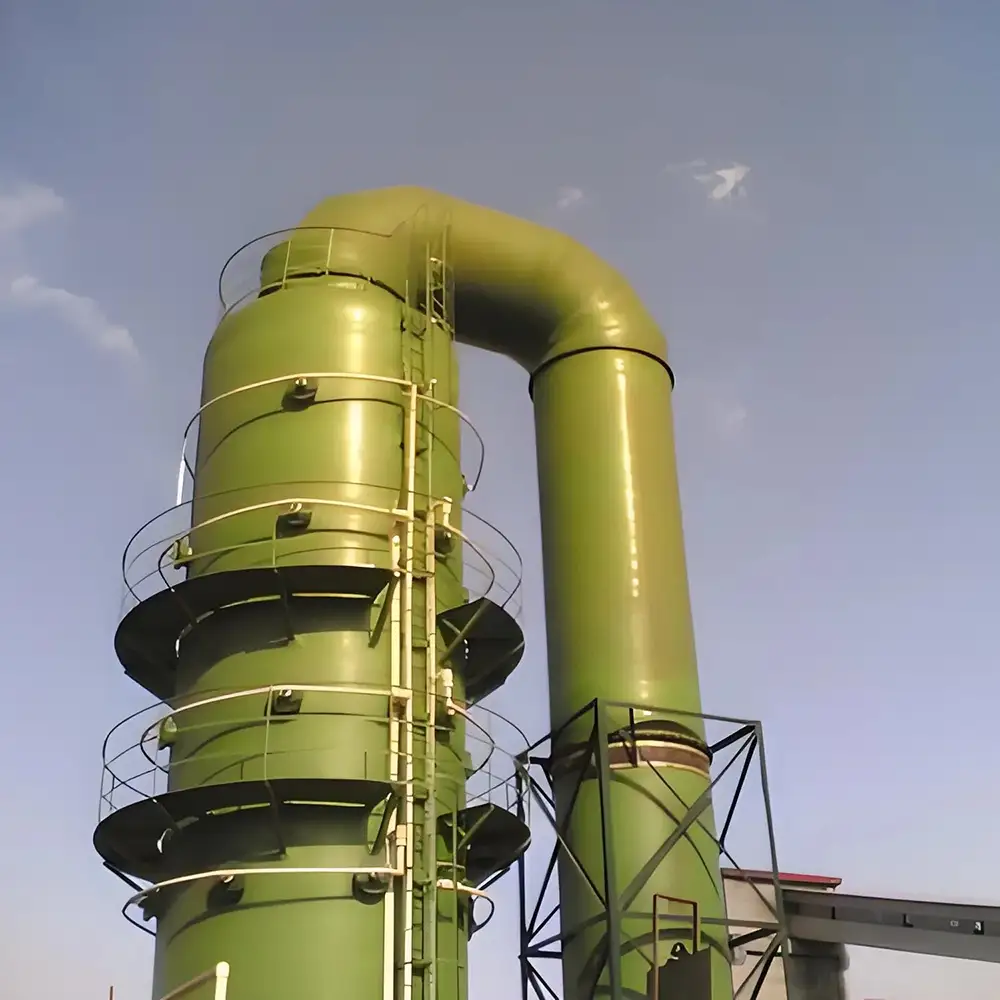
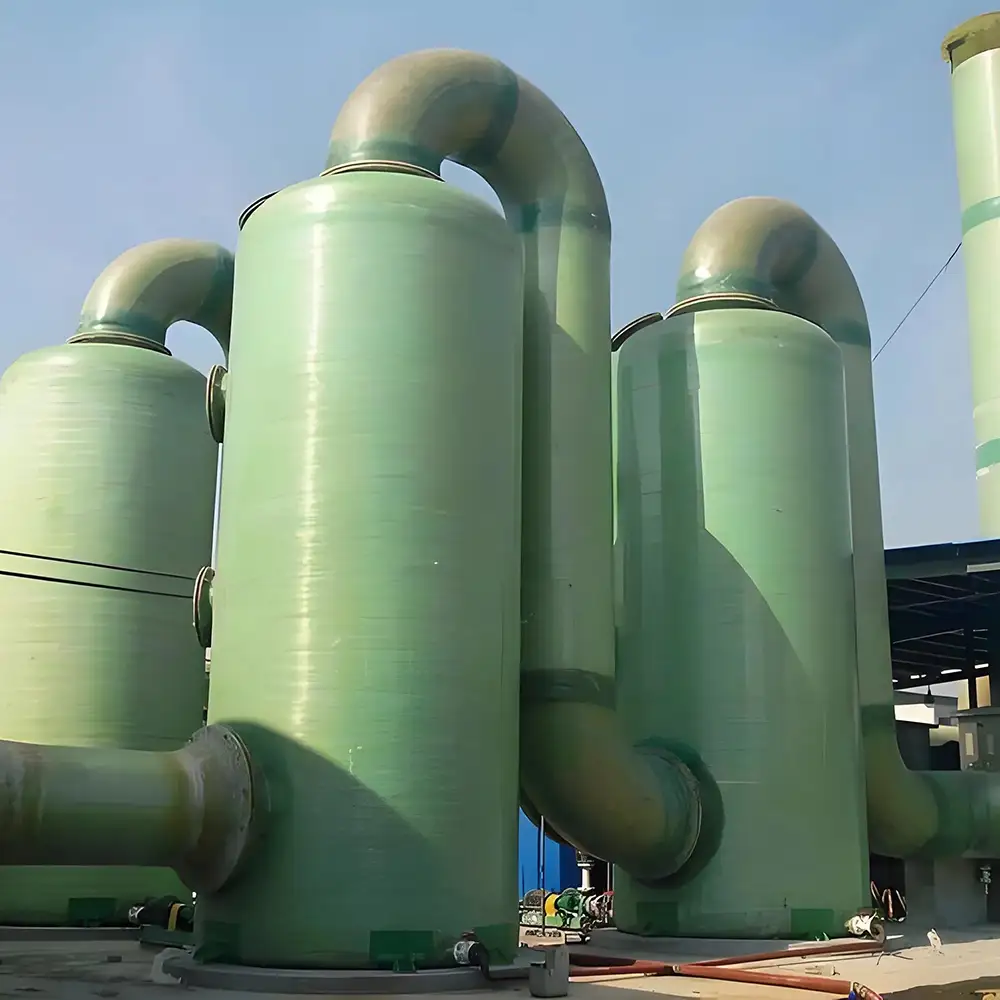
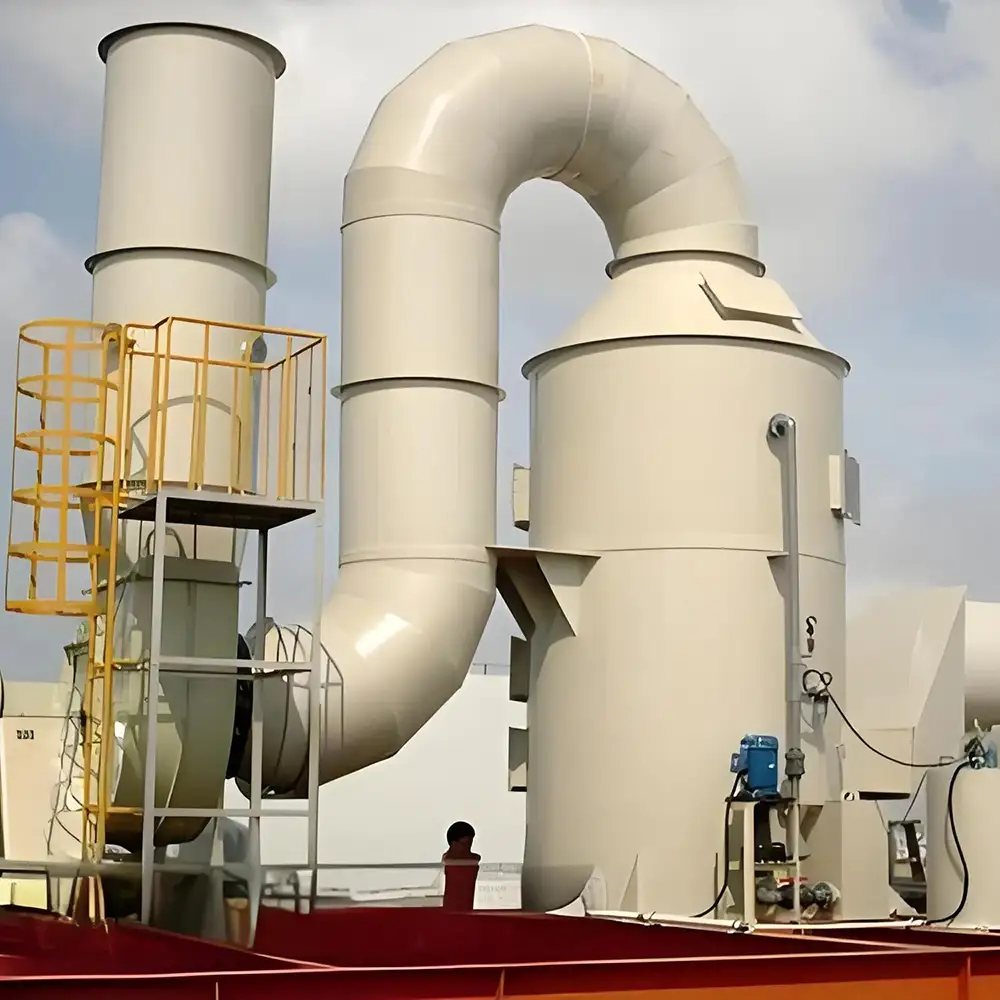
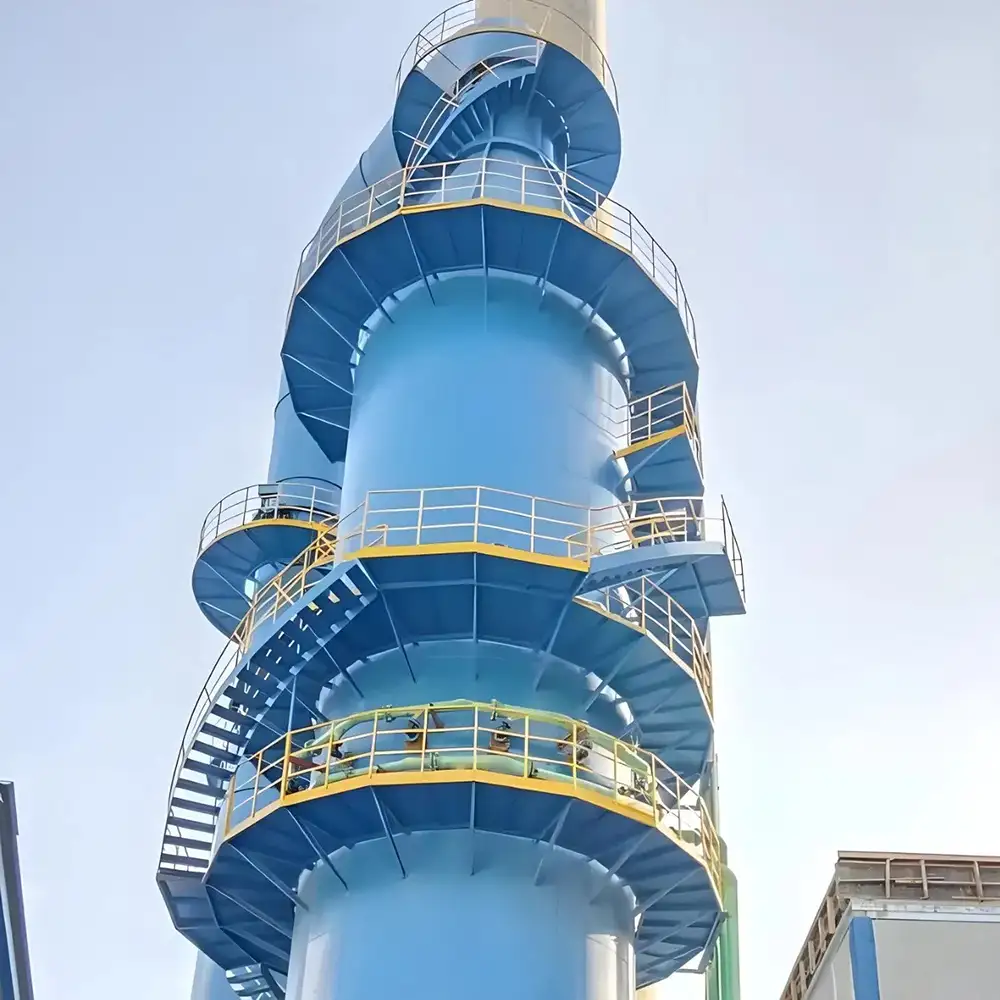
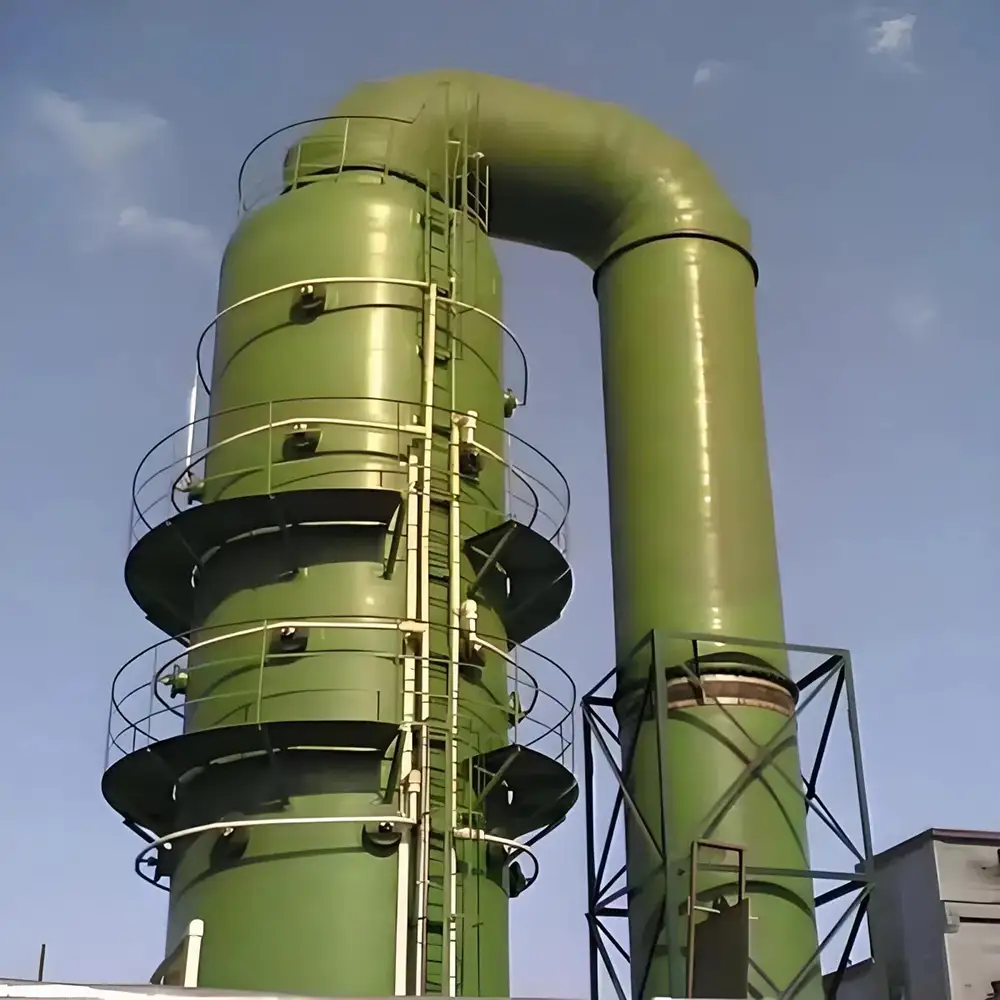
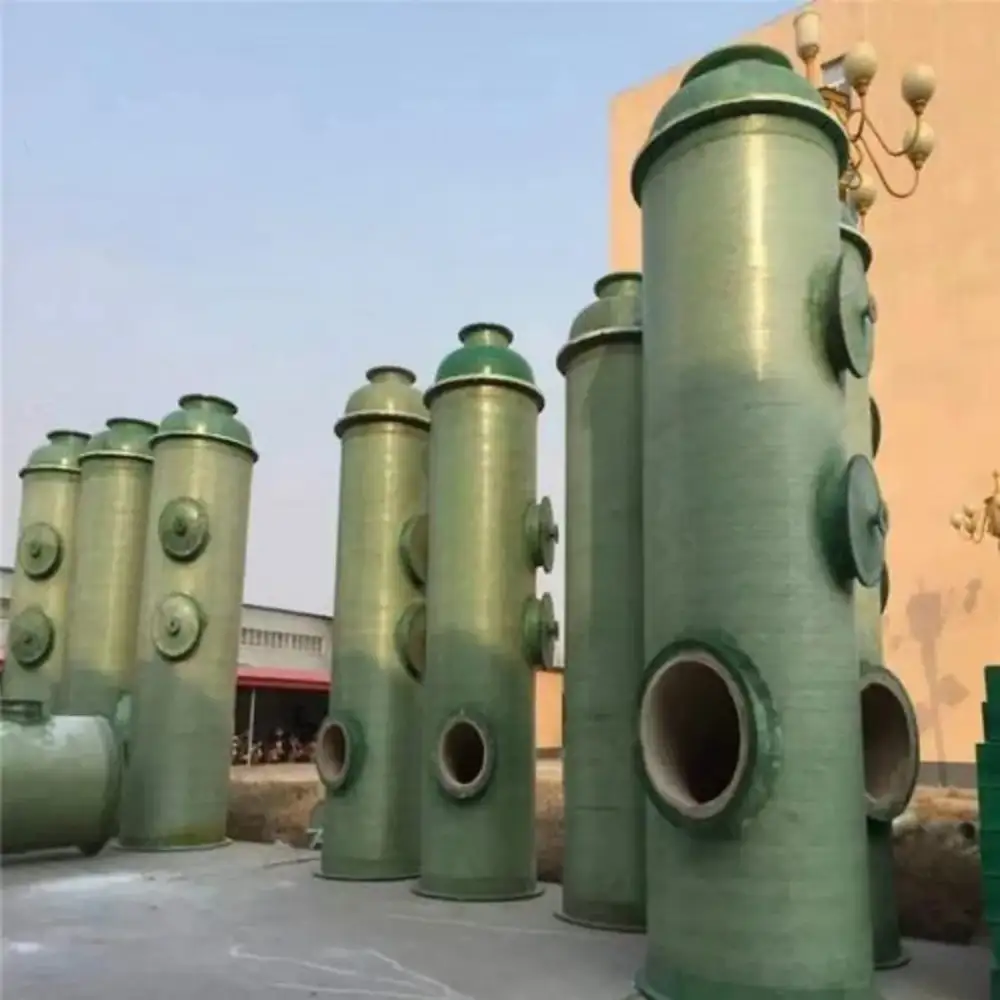
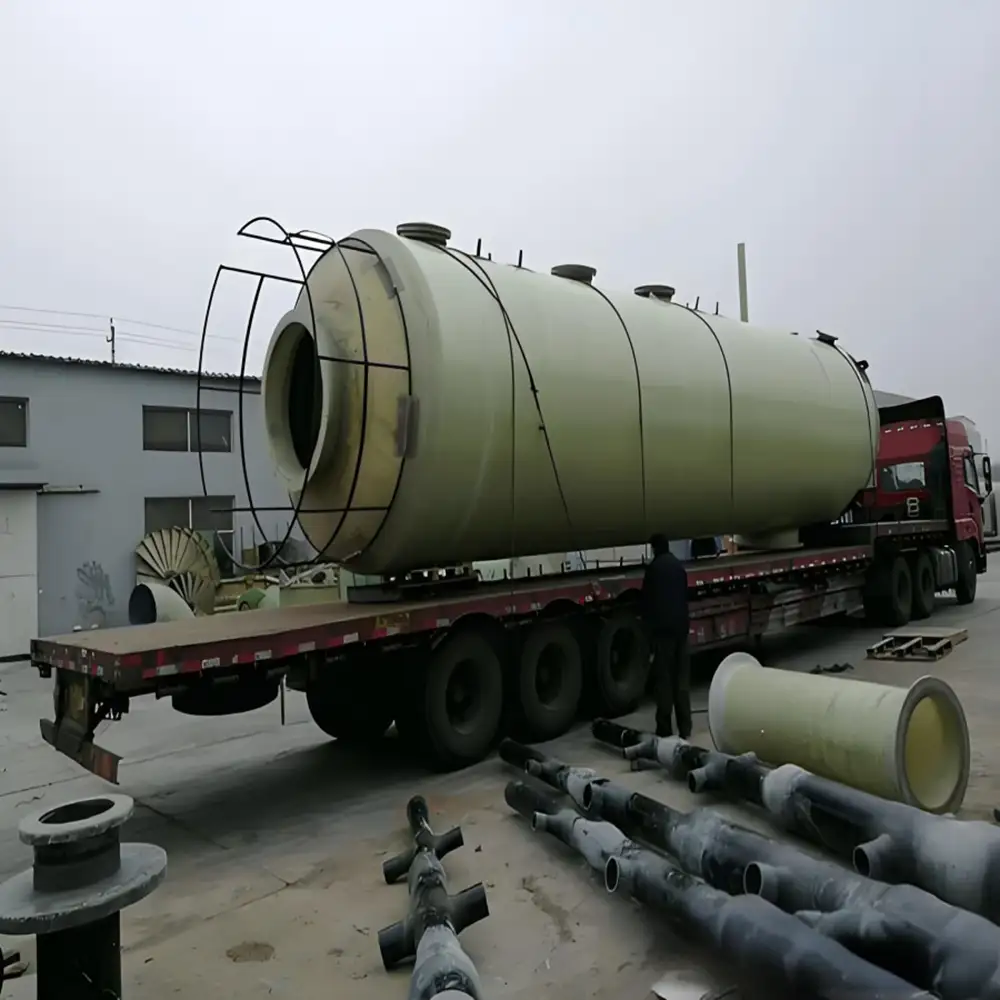
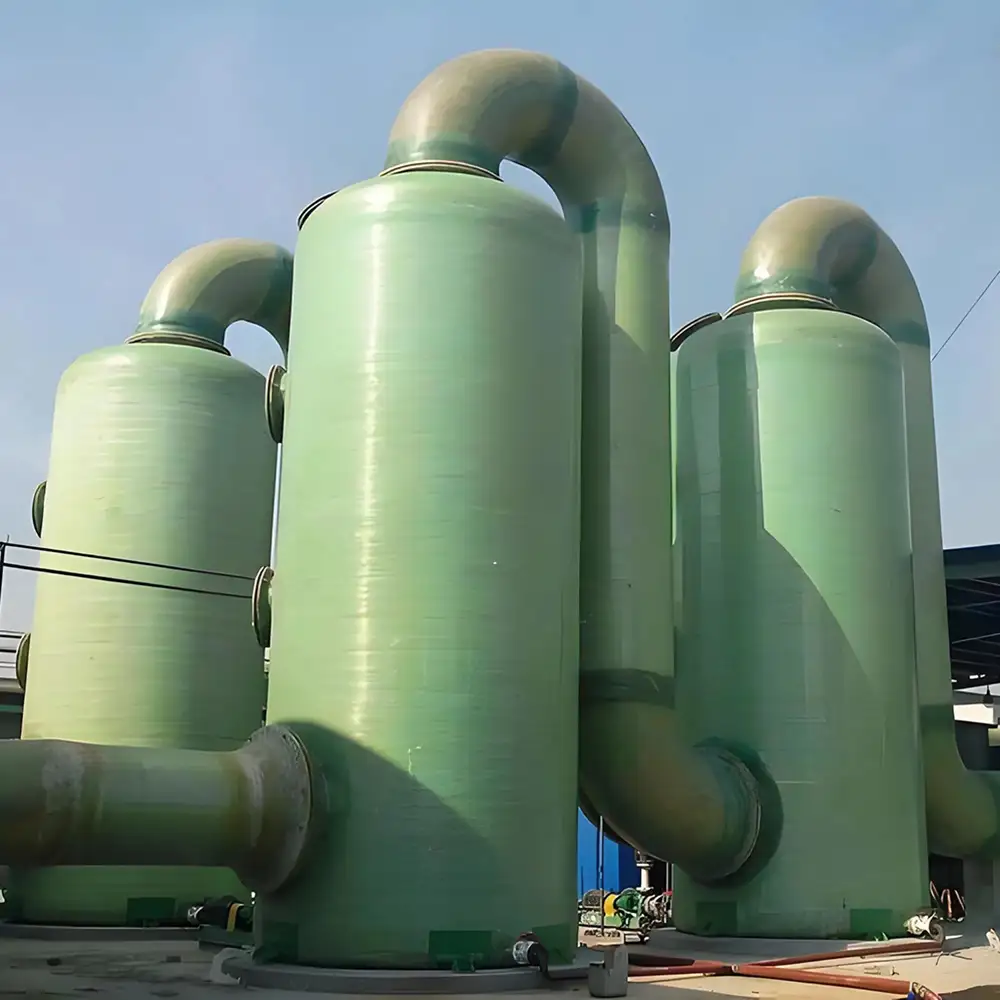
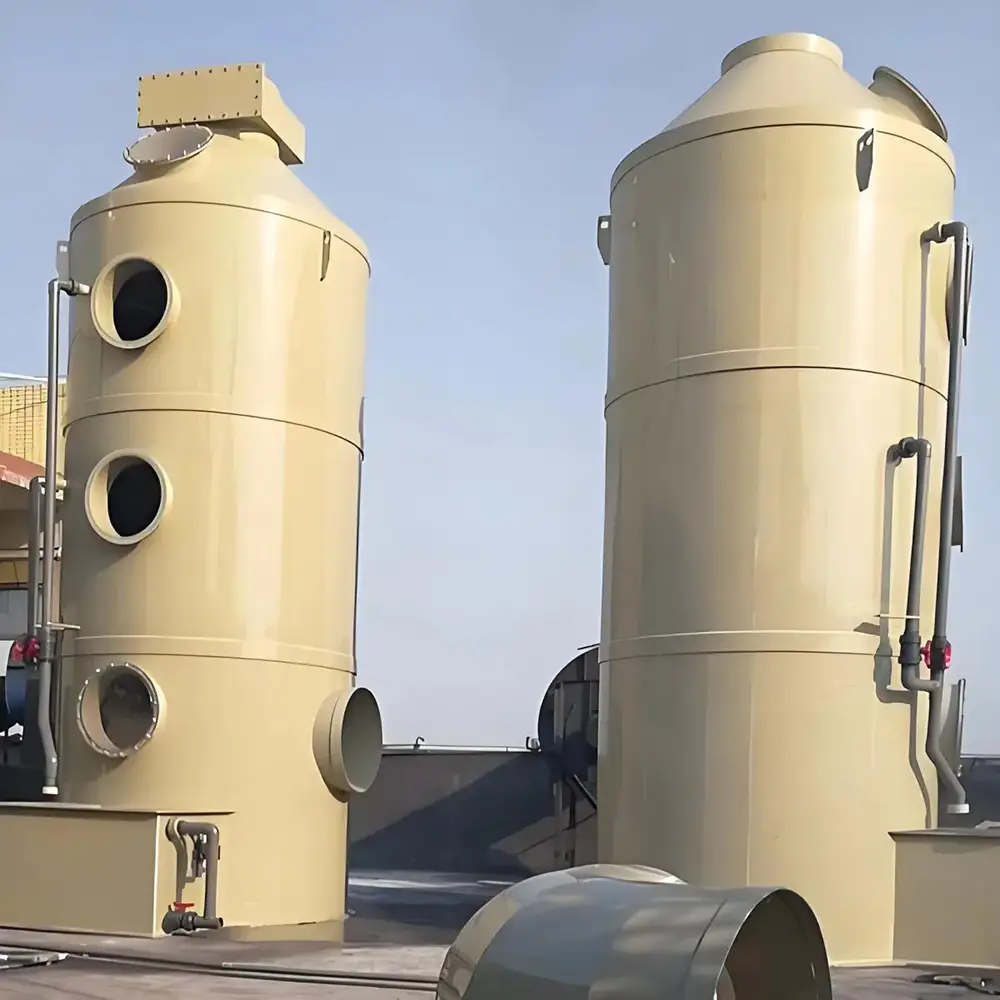
High Temperature Flue Gas Desulfurization, Denitrification and Dust Removal Treatment Equipment
High Temperature Flue Gas Desulfurization, Denitrification and Dust Removal Treatment Equipment is an integrated industrial air pollution control solution designed to treat high-temperature exhaust gas generated by boilers, furnaces, kilns, power plants, cement production, metallurgy, chemical processing, and other industrial processes. By combining desulfurization, denitrification, and dust removal functions, the system provides comprehensive treatment for sulfur dioxide, nitrogen oxides, particulate matter, and other pollutants in industrial flue gas.
Industrial combustion and thermal processing can produce high-temperature gases containing SO₂, NOx, dust, ash, acidic components, and other contaminants. Effective treatment requires equipment that can operate reliably under demanding temperature and gas-composition conditions. This integrated flue gas treatment system can be engineered according to the gas temperature, flow rate, pollutant concentration, dust loading, and required emission performance.
The system can incorporate multiple treatment technologies and process stages to achieve efficient pollutant removal while maintaining stable operation and practical energy consumption.
|
Model NO. |
Desulfurization Tower |
Thickness |
10~30mm |
|
Usage |
Environmental Protection,Industral
Chemical |
Product Categories |
Tower |
|
Molding Method |
Spray Method |
Material |
Customizable |
|
Fiber Type |
Customizable |
Type |
Polyester FRP |
|
Product Name |
Tower |
Shape |
Round Tank |
|
Diameter |
DN600~DN25000mm |
Performance |
Corrosion Resistant |
|
Product |
Customizable |
Place |
shandong |
|
Description |
PVC/FRP,PVDF/FRP,PE/FRP,Customizable |
Raw Material |
Vinyl Ester Resin+E,Customizable |
|
Storage Objects |
Gas |
Appearance |
Round Scrubbing Tower |
|
Transport Package |
Pallet |
Specification |
1-2500m3 |
|
Trademark |
WZSS |
Origin |
China |
|
HS Code |
3925100000 |
Production Capacity |
100 Pieces Annual |
High Temperature Flue Gas Treatment
High-temperature flue gas requires careful process design because excessive temperature can affect downstream treatment equipment, while rapid cooling can cause condensation and corrosion if not properly controlled.
The treatment system can include suitable cooling, heat recovery, gas conditioning, or temperature-control stages before or between purification processes. This allows the flue gas to reach appropriate operating conditions for desulfurization, denitrification, and dust removal.
Depending on the application, the equipment can be configured as a complete flue gas purification line or integrated with an existing industrial exhaust treatment system.
Flue Gas Desulfurization
Desulfurization is primarily used to reduce sulfur dioxide emissions generated by burning sulfur-containing fuels and processing sulfur-bearing materials.
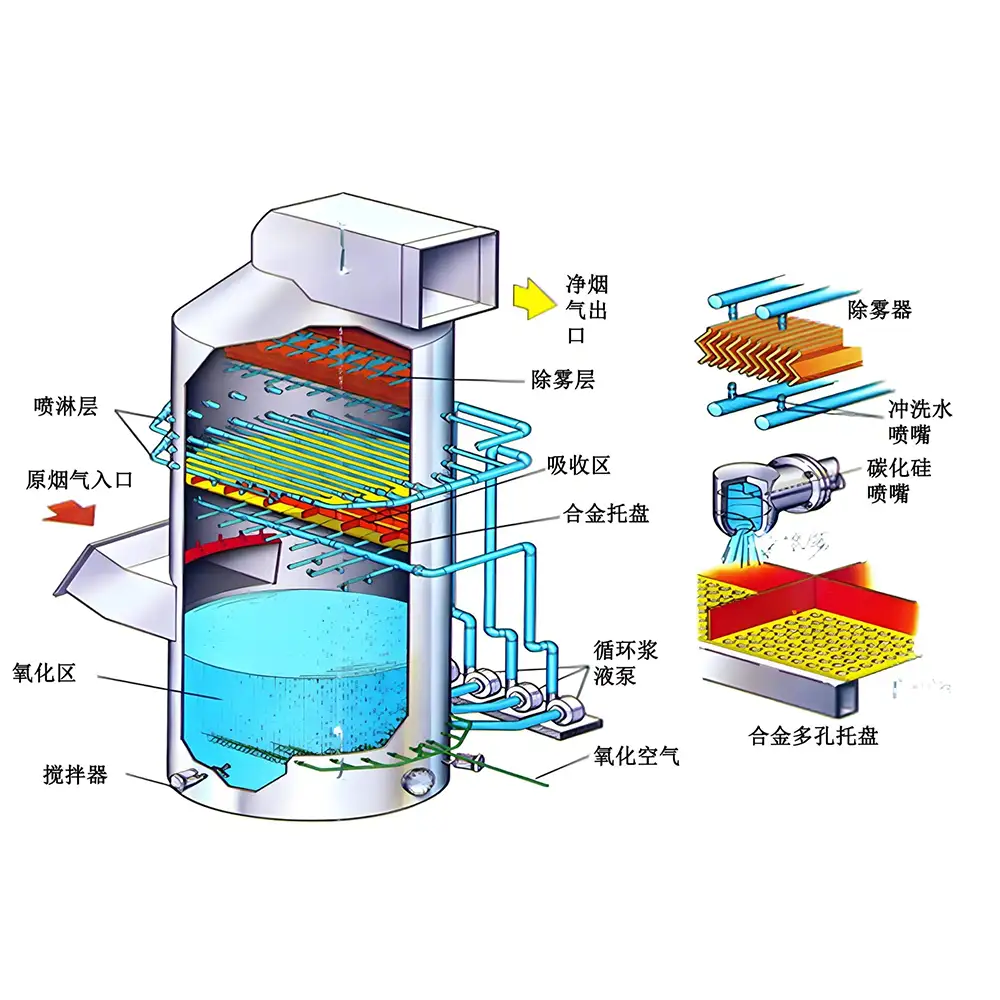
The flue gas desulfurization section provides controlled contact between the contaminated gas and a suitable absorbent or reaction medium. SO₂ is absorbed or chemically reacted to reduce its concentration before the treated gas is discharged.
Different desulfurization processes can be selected according to fuel characteristics, SO₂ concentration, gas temperature, treatment capacity, and required emission limits.
The system can use suitable spray, absorption, circulation, or other gas-liquid contact technologies to achieve stable sulfur dioxide removal.
Flue Gas Denitrification
Nitrogen oxides are another important pollutant generated by high-temperature combustion. NOx formation is closely related to combustion temperature, fuel composition, oxygen concentration, and operating conditions.
The denitrification section is designed to reduce NOx emissions from industrial flue gas. Depending on the application, technologies such as Selective Catalytic Reduction (SCR), Selective Non-Catalytic Reduction (SNCR), or other suitable denitrification processes can be incorporated.
SCR systems generally use a catalyst to promote the reaction between NOx and a reducing agent, while SNCR technology performs the reaction within an appropriate temperature range without a catalyst.
The appropriate process should be selected according to flue gas temperature, NOx concentration, required removal efficiency, and operating conditions.
Efficient Dust Removal
High-temperature industrial exhaust gas can contain large amounts of dust, ash, soot, and particulate matter. Effective dust removal is essential for meeting emission requirements and protecting downstream equipment.
The system can be integrated with suitable dust collection technologies, including bag filters, electrostatic precipitators, cyclone separators, wet scrubbers, or other particulate-control equipment.
The selection of dust removal technology depends on particle size distribution, dust concentration, gas temperature, moisture content, chemical composition, and required outlet emissions.
An appropriate dust removal stage can also help protect downstream desulfurization and denitrification equipment from excessive particulate loading.
Integrated Multi-Pollutant Control
A major advantage of this system is its ability to integrate multiple pollution-control functions into one coordinated treatment process.
Instead of using independent systems without process coordination, the desulfurization, denitrification, and dust removal stages can be engineered as a complete flue gas purification line.
Process sequencing is important because the temperature and pollutant conditions after one treatment stage can influence the performance of the next stage. Proper system design can therefore improve overall treatment efficiency and equipment reliability.
The complete system may include fans, ducts, heat exchangers, dust collectors, denitrification reactors, desulfurization towers, circulation pumps, dosing equipment, demisters, monitoring instruments, and automatic control systems.
Temperature and Gas Conditioning
High-temperature flue gas treatment requires effective temperature management. Depending on the process, gas cooling or heat recovery may be used to bring the flue gas into the appropriate temperature range for downstream purification.
Heat recovery can also improve overall energy utilization by recovering part of the thermal energy contained in the exhaust gas.
Temperature monitoring at key points helps operators maintain stable operating conditions and prevent abnormal temperature fluctuations that could affect catalysts, filters, absorbers, or other components.
Automatic Operation and Monitoring
Modern flue gas purification equipment can be equipped with an automatic control system to monitor and regulate important operating parameters.
Typical monitoring points include flue gas temperature, pressure, flow rate, SO₂ concentration, NOx concentration, oxygen level, differential pressure, absorbent circulation, and reagent dosing.
Automatic controls can coordinate fans, pumps, valves, dosing systems, dampers, and other components according to real-time operating conditions.
This improves process stability, reduces manual intervention, and makes long-term industrial operation easier to manage.
Energy-Efficient Flue Gas Purification
For continuous industrial applications, energy consumption is an important consideration. The treatment system can be optimized to balance pollutant removal performance with fan power, pump energy, pressure drop, reagent consumption, and heat recovery.
Proper equipment sizing and process configuration can help avoid excessive gas resistance and unnecessary circulation. Heat recovery can also be considered when high-temperature flue gas contains significant recoverable thermal energy.
An optimized system can therefore provide effective pollution control while supporting economical long-term operation.
Industrial Applications
High-temperature flue gas desulfurization, denitrification, and dust removal equipment can be used in many industrial applications, including:
Coal-Fired Power Plants
Industrial Boiler Systems
Cement Plants
Lime Kilns
Steel And Metallurgical Facilities
Chemical Processing Plants
Waste Incineration Systems
Biomass Combustion Systems
Mineral Processing Plants
Industrial Furnaces
Thermal Processing Equipment
Power Generation Facilities
The final process configuration should be selected according to the actual flue gas characteristics and applicable environmental requirements.
System Design and Maintenance
Reliable performance requires regular inspection and maintenance of filters, catalysts, pumps, nozzles, ducts, valves, fans, demisters, circulation systems, and other components.
Dust collection equipment should be checked for excessive pressure drop and dust accumulation. Denitrification systems require appropriate reagent management and catalyst inspection where applicable. Desulfurization systems should be monitored for scaling, blockage, circulation performance, and absorbent concentration.
A preventive maintenance program can help identify problems early and maintain stable treatment performance.
Why Choose Us
Integrated flue gas treatment requires careful coordination between temperature control, dust removal, denitrification, and desulfurization. Our solutions are designed around the actual operating conditions of each industrial emission source.
Key advantages include:
Integrated Desulfurization, Denitrification, And Dust Removal
Suitable For High-Temperature Industrial Flue Gas
Comprehensive SO₂, NOx, And Particulate Control
Flexible Treatment Process Configuration
Multiple Dust Removal Technologies Available
SCR And SNCR Denitrification Options
Efficient Gas Conditioning And Temperature Control
Automatic Monitoring And Process Control
Energy-Efficient System Optimization
Suitable For New And Existing Industrial Facilities
Easy Maintenance And Process Inspection
Designed For Continuous Industrial Operation
FAQs
1. What is high-temperature flue gas treatment equipment?
It is an industrial emission-control system designed to treat hot exhaust gas and remove pollutants such as sulfur dioxide, nitrogen oxides, and particulate matter.
2. What pollutants can this system remove?
The system can be configured to reduce SO₂, NOx, dust, ash, particulate matter, and selected acidic or soluble pollutants depending on the treatment process.
3. How does the desulfurization section work?
The desulfurization section uses a suitable absorbent or reaction process to capture and neutralize sulfur dioxide in the flue gas.
4. What denitrification technology can be used?
Depending on operating conditions, the system may use SCR, SNCR, or another appropriate NOx reduction technology.
5. Can dust removal be integrated with desulfurization and denitrification?
Yes. Dust collection can be incorporated into the overall treatment line and positioned according to gas temperature, particle characteristics, and the requirements of downstream equipment.
6. Why is temperature control important?
Different purification technologies operate effectively within specific temperature ranges. Proper temperature management helps protect equipment and maintain stable treatment performance.
7. What determines the capacity of the system?
Important factors include flue gas flow rate, inlet temperature, SO₂ concentration, NOx concentration, dust loading, gas composition, required removal efficiency, and operating hours.
8. Can the system recover heat from high-temperature flue gas?
Yes. Heat exchangers or other heat recovery equipment can be incorporated where the process conditions provide useful recoverable thermal energy.
9. Is automatic control available?
Yes. Automatic control can monitor temperature, pressure, gas flow, pollutant concentration, reagent dosing, pump operation, and other important process parameters.
10. Can this equipment be integrated into an existing plant?
Yes. The system can be engineered for existing industrial facilities after evaluating the current exhaust ducts, fans, gas flow, temperatures, pollutant concentrations, available space, and required treatment performance.
Prev:
Multifunction Exhaust Gas Treatment and Purification Equipment System Water Treatment Plant
Next:
Industrial Waste Gas Purification Optimization, Support Customization/Desulfurization Tower
TAG:
Dust Collection Equipment,
Flue Gas Treatment Equipment,
Dust Removal Equipment,
Dust Removal System,
Industrial Dust Removal,
Flue Gas Dust Removal,
Industrial Exhaust Gas Treatment,
Industrial Waste Gas Treatment,
Industrial Exhaust Gas Purification,
Flue Gas Treatment System,
Flue Gas Purification System,
Flue Gas Purification Equipment,
Industrial Flue Gas Treatment,
Industrial Flue Gas Purification,
Sulfur Dioxide Scrubber,
SO2 Removal Equipment,
Sulfur Dioxide Removal,
Sulfur Dioxide Removal Equipment,
SO2 Scrubber,
SO2 Removal System,
Desulphurization Tower,
Desulfurization Tower,
Flue Gas Desulphurization Tower,
Flue Gas Desulfurization Tower,
Desulphurization Equipment,
Desulfurization Equipment,
Flue Gas Desulfurization Equipment,
Flue Gas Desulphurization Equipment,
Flue Gas Desulfurization System,
Flue Gas Desulphurization System,
Related Category:
High Temperature Flue Gas Desulfurization Equipment, Flue Gas Denitrification Equipment, Dust Removal Treatment Equipmen China, suppliers, manufacturers, factory, customized, wholesale, quotation, made in China