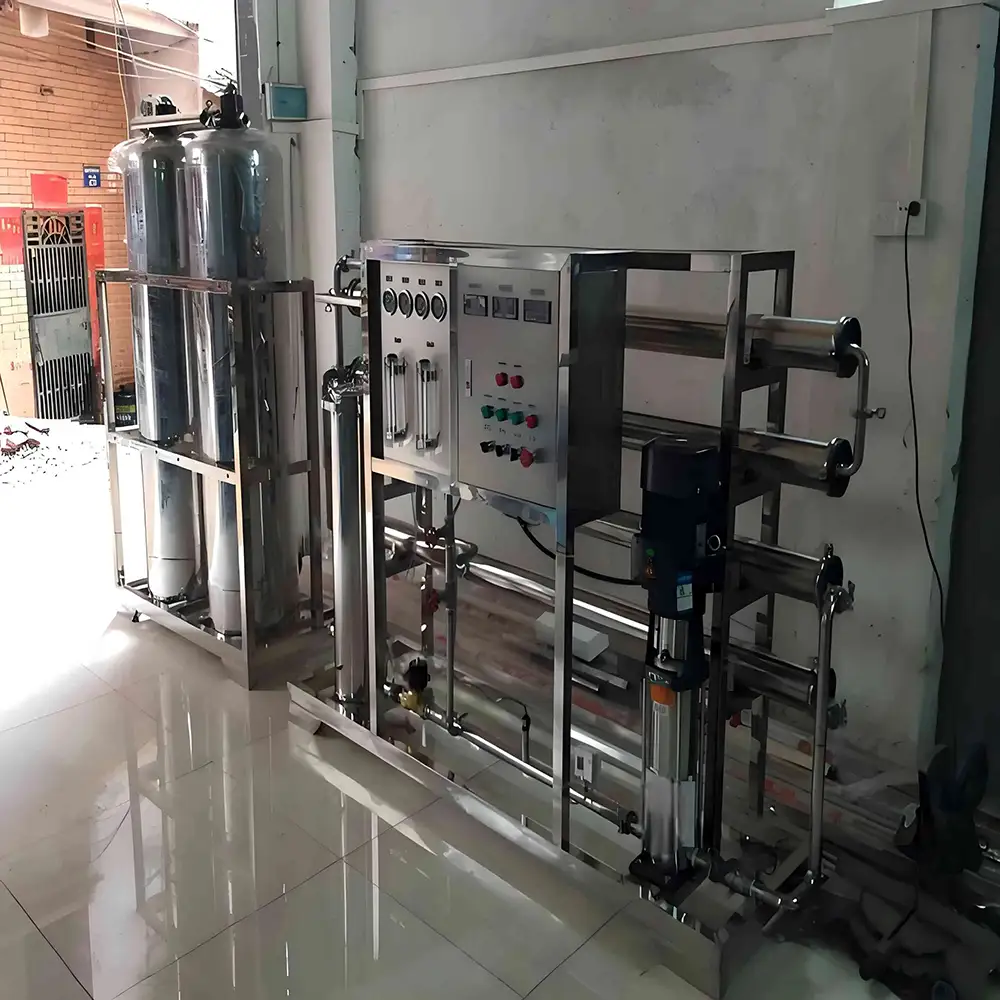
Chloride Ion Removal/Scale Removal/Sewage Treatment Plant/RO Reverse Osmosis System/Boiler Water Treatment/Papermaking Water
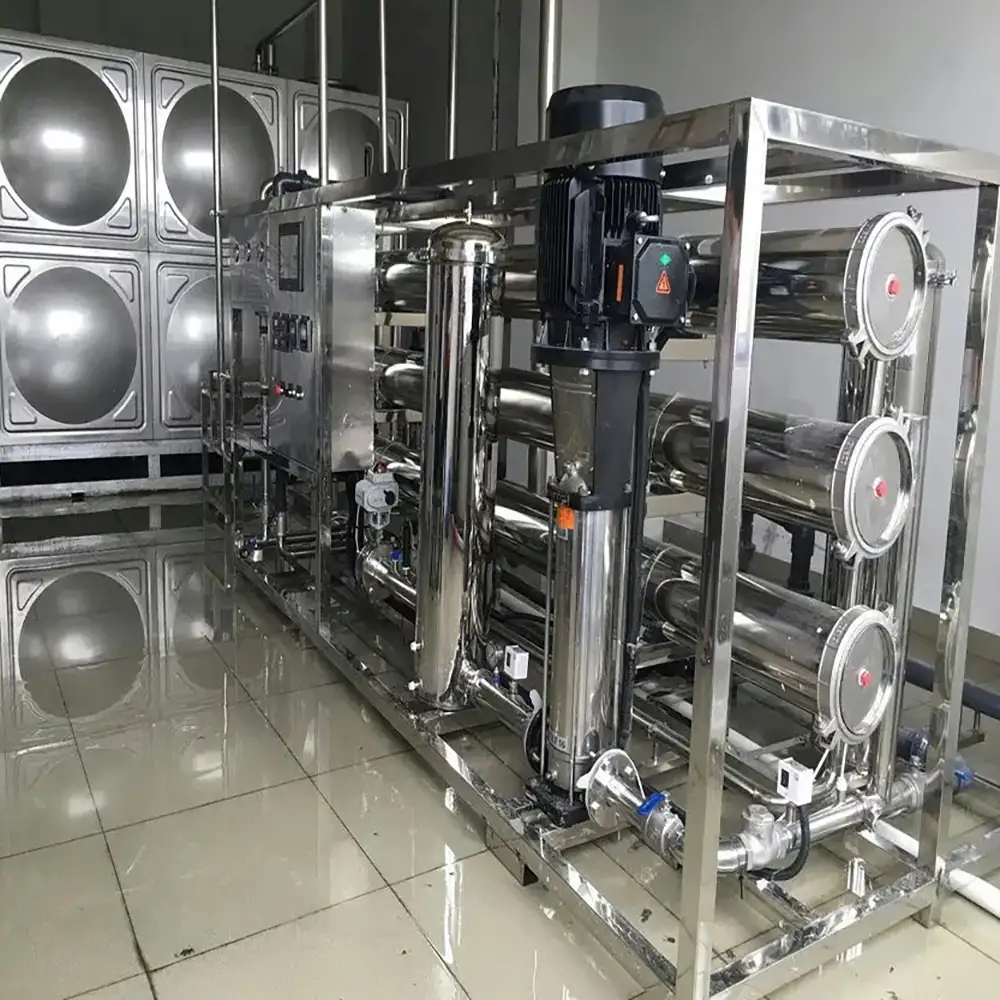
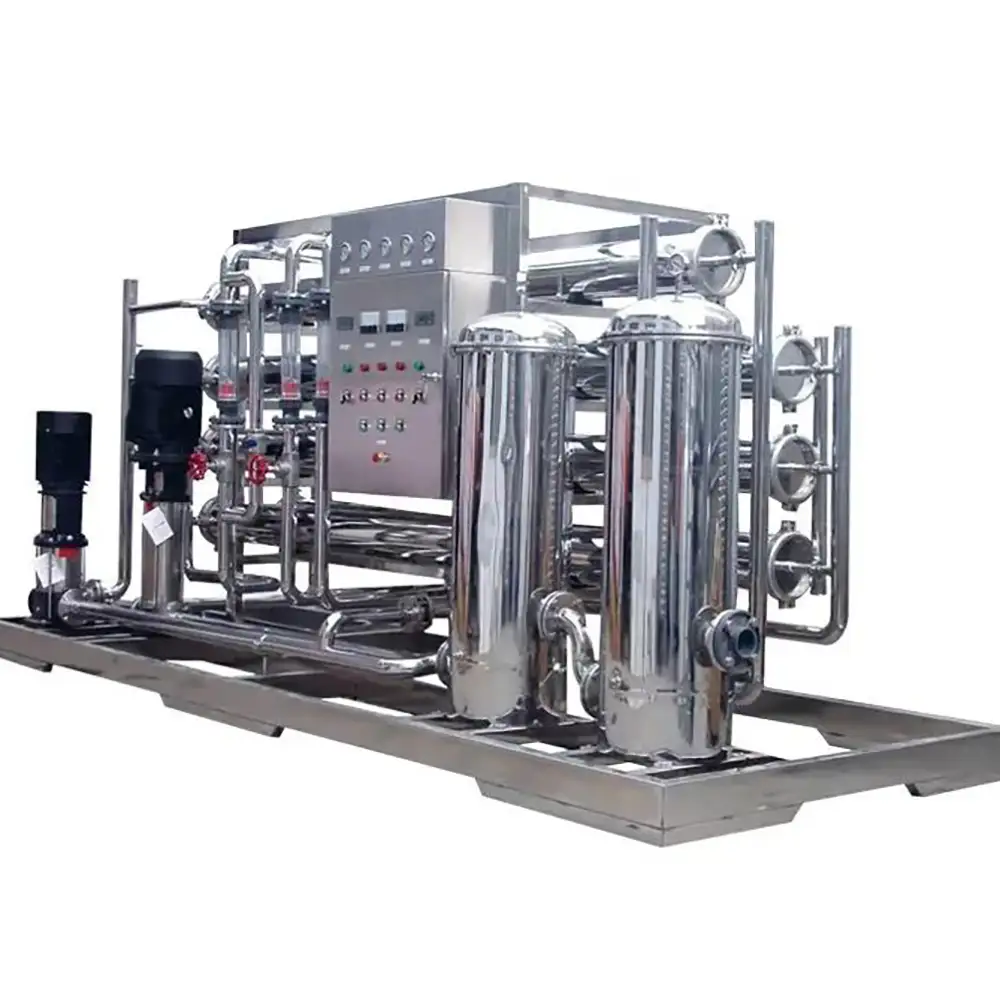
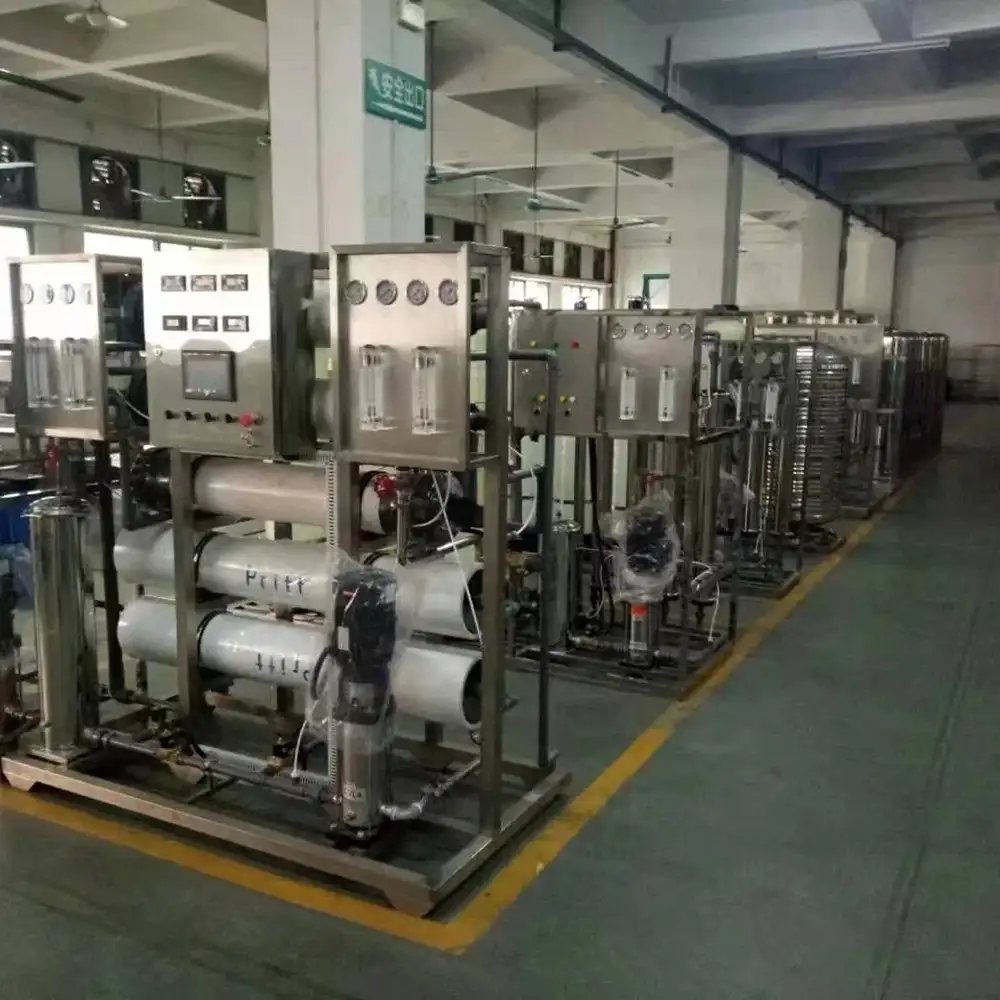
The reverse osmosis pure water equipment adopts a fully automatic control method to reduce the impact of human error on the equipment. The design of the reduction system is used in the pretreatment system to solve the irreparable impact of excessive residual chlorine on the reverse osmosis membrane. The reverse osmosis membrane selection adopts domestic first-line brand reverse osmosis membrane, with a service life of up to 3 years and an outlet water conductivity of less than 5us. The pump is a domestically produced Nanfang pump, which has low operating noise and long service life. The water recovery rate can reach more than 65%. High degree of automation, simple operation, stable water quality, and low operating cost
Chloride Ion Removal, Scale Removal, Sewage Treatment Plant, RO Reverse Osmosis System and Boiler Water Treatment
Chloride Ion Removal, Scale Removal, Sewage Treatment Plant, RO Reverse Osmosis System, and Boiler Water Treatment technologies provide comprehensive solutions for industrial water purification and wastewater management. Different industrial processes can introduce chloride ions, hardness minerals, suspended solids, organic contaminants, and dissolved salts into water. Without effective treatment, these contaminants can cause corrosion, scaling, membrane fouling, equipment damage, and unstable production performance.
A properly designed industrial water treatment system combines pretreatment, filtration, reverse osmosis, softening, wastewater treatment, and specialized contaminant-removal technologies according to the source-water characteristics and application requirements.
These treatment technologies can be used independently or integrated into a complete water treatment plant for factories, power plants, chemical facilities, food-processing plants, manufacturing facilities, commercial buildings, and other industrial applications.
|
Model NO. |
WZSS |
Method |
Biological Treatment |
|
Usage |
Industrial, Home, Agriculture, Hospital |
HS Code |
9421219990 |
|
Production Capacity |
2000 Pieces/Year |
Origin |
Shandong, China |
|
Service Life |
20 Years |
Certificate |
SGS, ISO |
|
Trademark |
Wanze Prosperity |
Principle |
Physical Filtration |
|
membrane logarithm |
custom made |
work pressure |
0.2-1.6MPa
|
Functions and uses of each component of the equipment
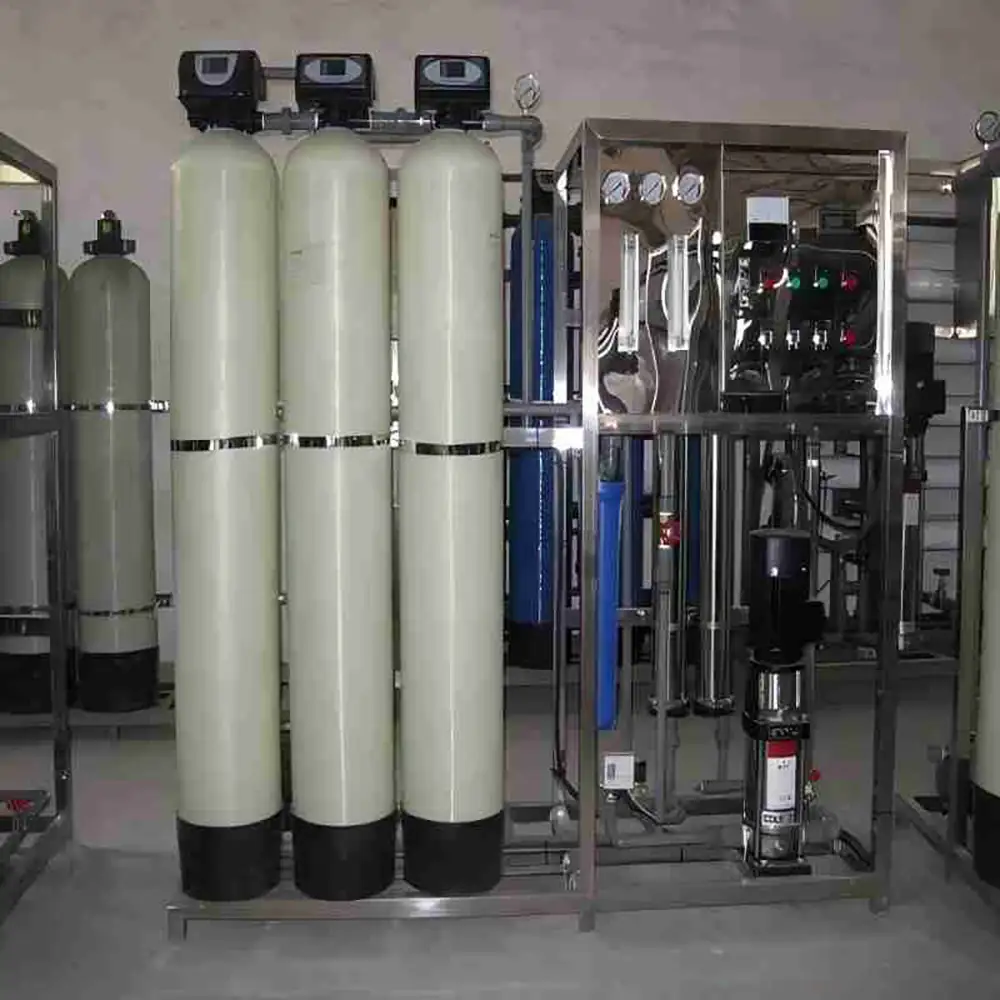
1. Raw water tank: It mainly solves the problem of unstable tap water pressure and reduces mechanical failures caused by frequent startup of the lift pump during operation or unstable tap water pressure.
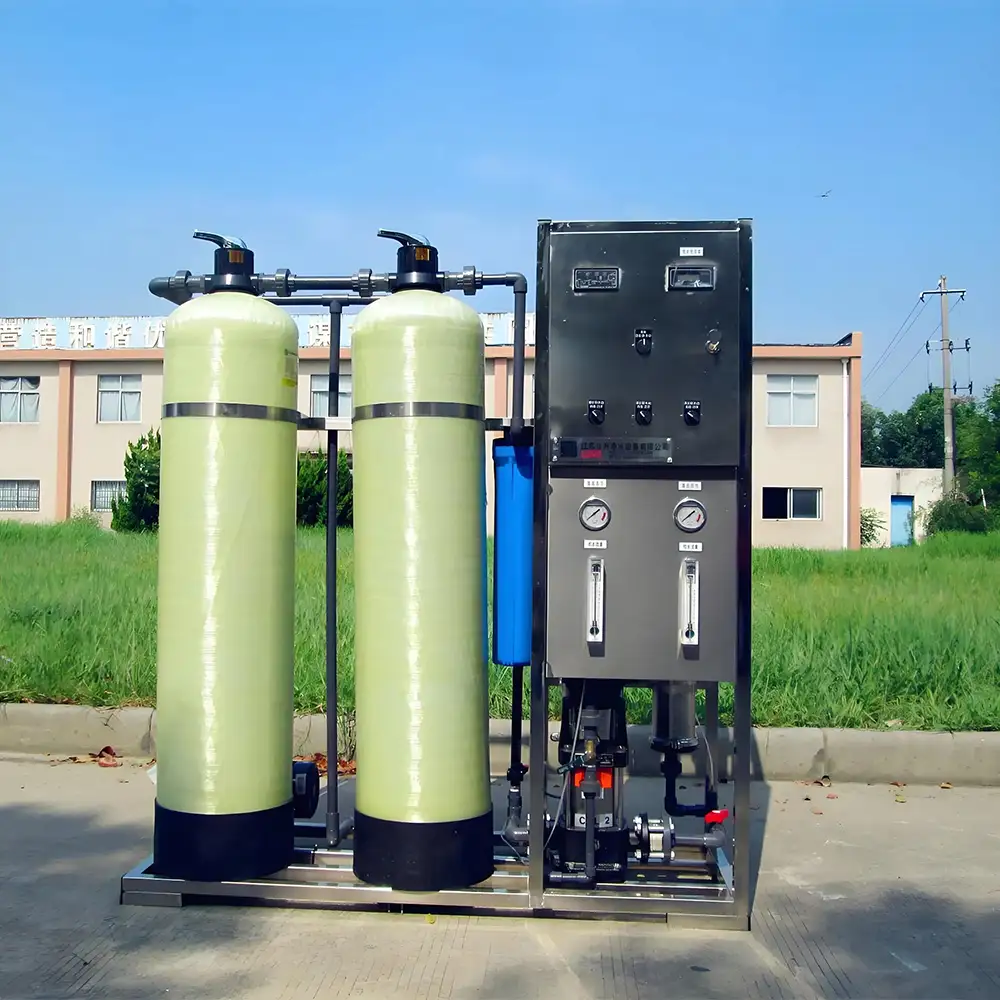
2. Quartz sand filter: Tap water enters from the upper end of the tank, and flows evenly from the upper end of the filter layer to the lower end through the upper water distributor. After passing through the filter layer, the tap water leaves the filter layer through the lower water distributor to form filtered water.
3. Activated carbon filter: The internal structure of the activated carbon filter is exactly the same as that of the quartz sand filter. After activated carbon adsorption, the residual chlorine in tap water can generally be reduced to less than 0.1mg/l.
4. Precision filter: Mainly using 5us melt-blown filter element, which can remove fine particles and further create conditions for reverse osmosis water inflow.
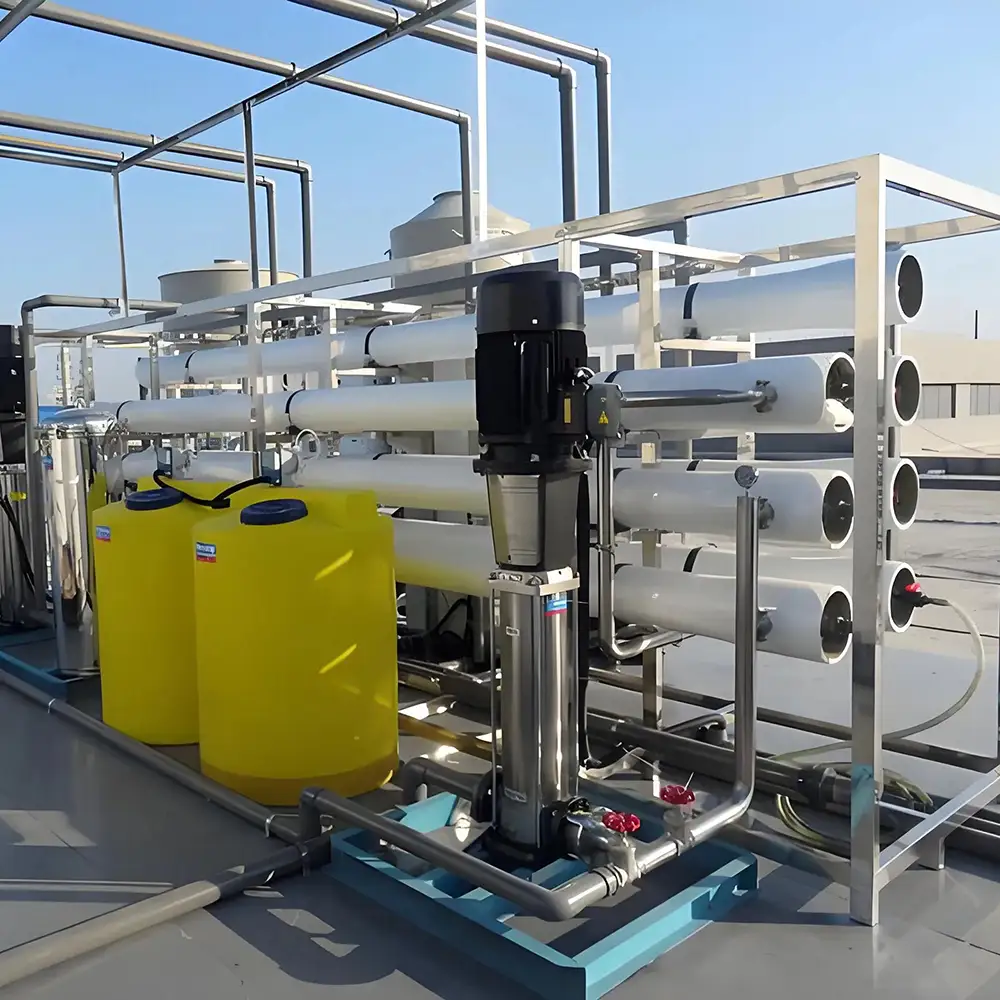
5. High-pressure pump: Provides the necessary power for reverse osmosis operation.
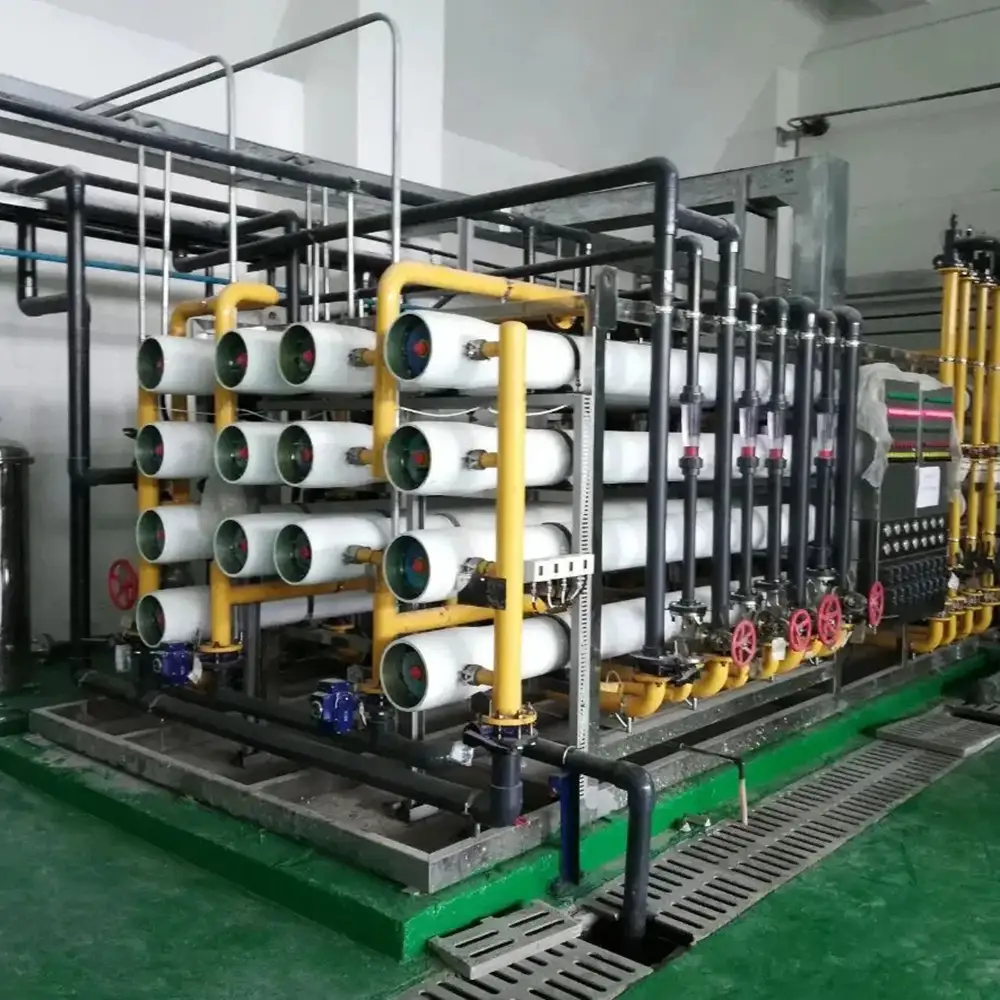
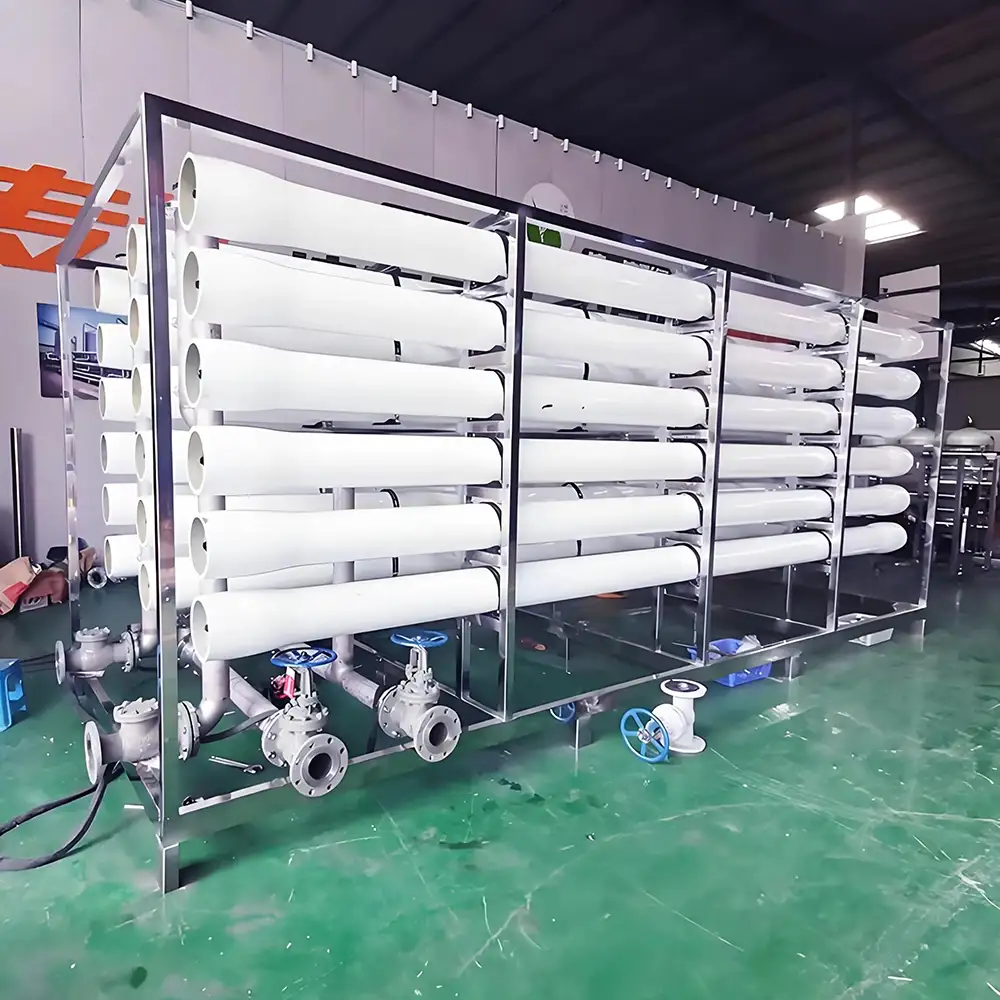
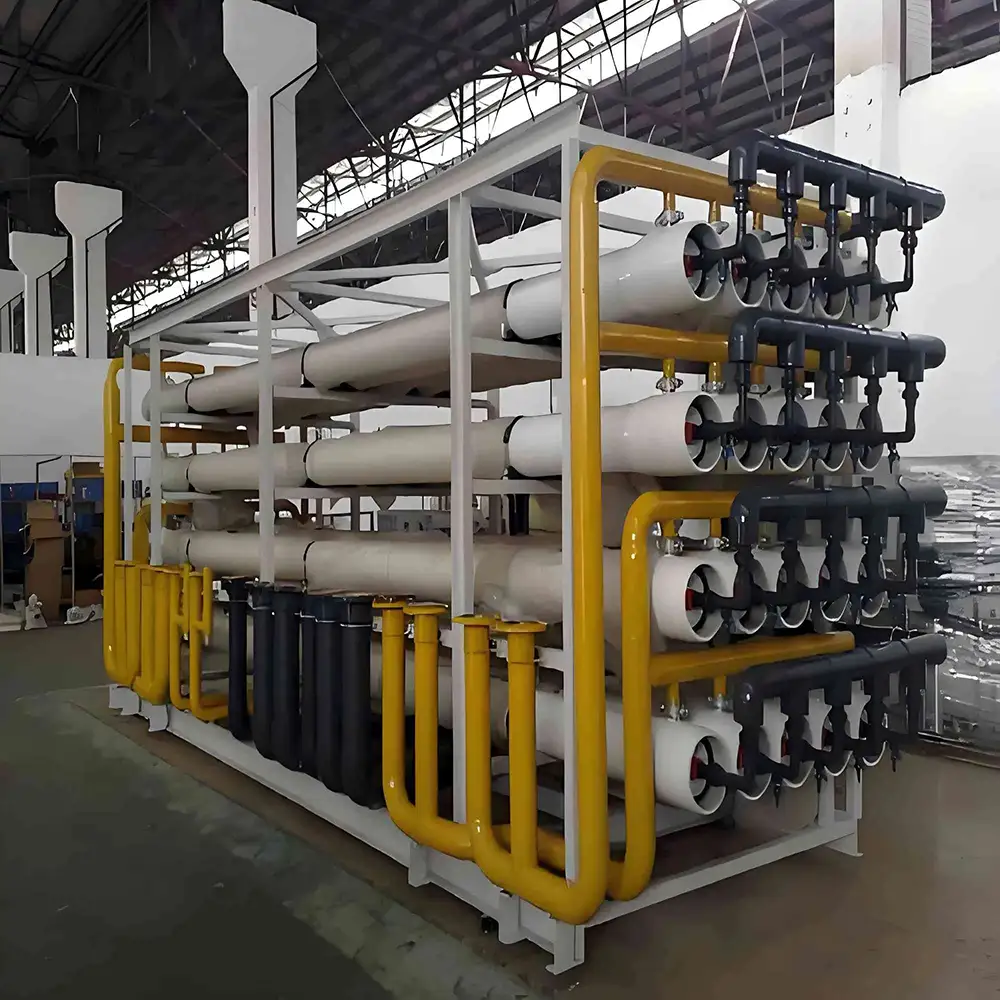
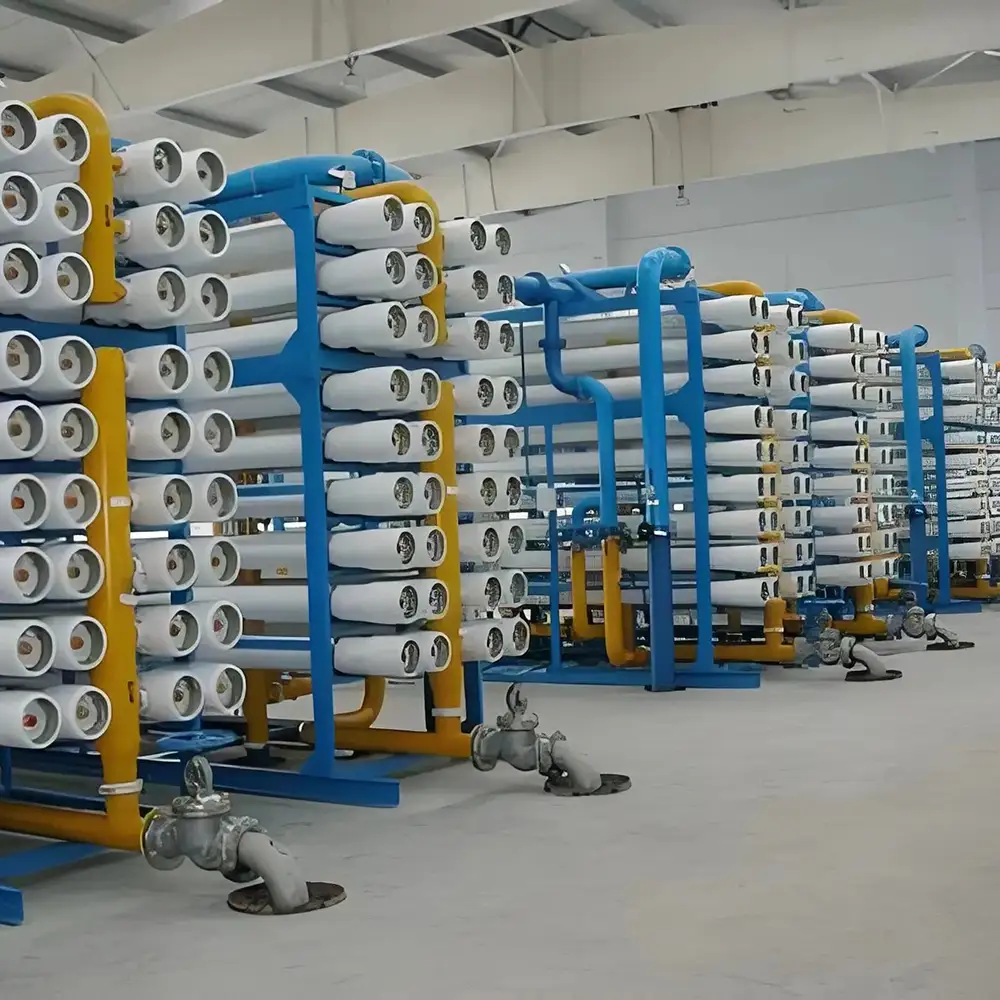
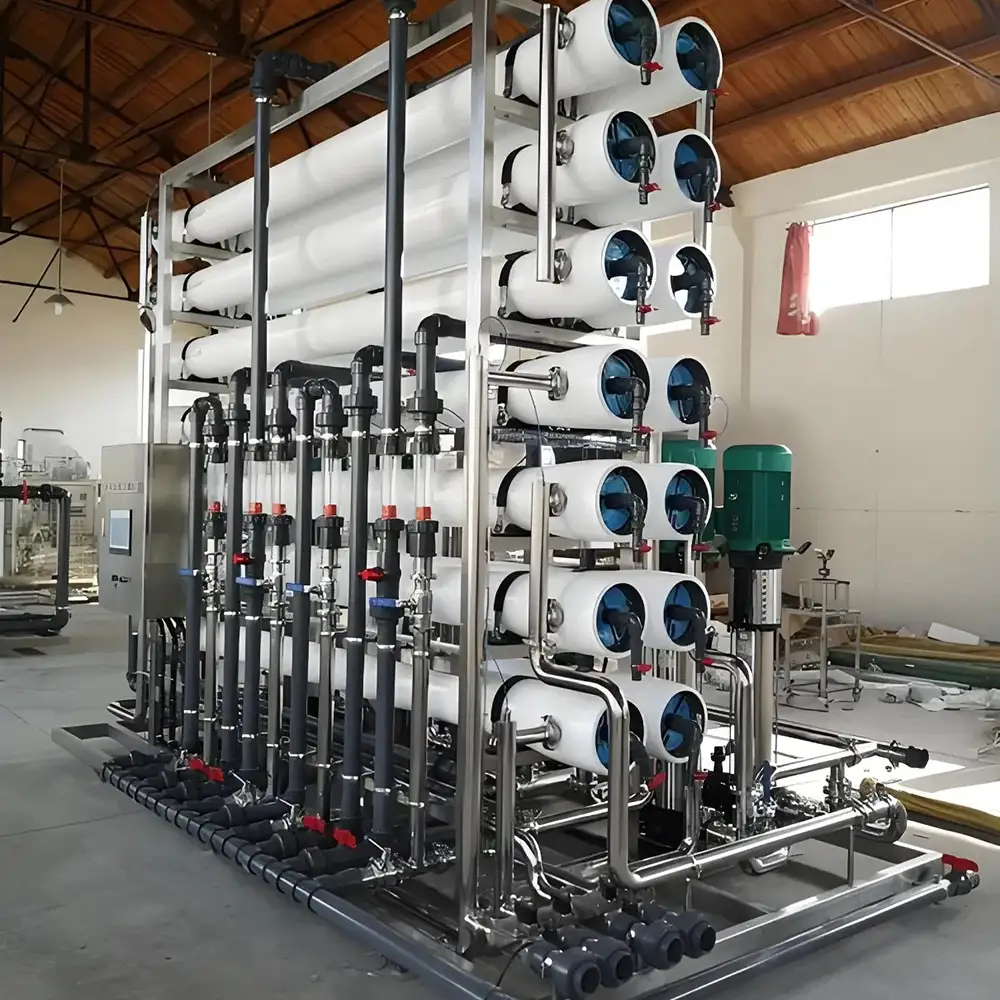
6. Reverse osmosis system: The reverse osmosis system is the core component of reverse osmosis pure water equipment. The design of reverse osmosis mainly considers three major issues: the number, brand, and arrangement of filter membrane elements.
7. Pure water tank: used to store pure water.
Chloride Ion Removal/Scale Removal/Sewage Treatment Plant/RO Reverse Osmosis System/Boiler Water Treatment/Papermaking Water
Chloride Ion Removal/Scale Removal/Sewage Treatment Plant/RO Reverse Osmosis System/Boiler Water Treatment/Papermaking Water
System control and advantages of reverse osmosis pure water equipment
1. Automatic water replenishment of the tap water tank: When the liquid level of the tap water tank reaches a low level, automatic water replenishment is performed. Stop replenishing water when it reaches a high level
2. When the water level in the tap water tank reaches a certain level, the system starts to work. When the pure water tank is full, the system stops.
3. When the tap water tank is at a low water level, water shortage protection is activated, the system stops completely, and neither manual nor automatic operations are possible.
4. The reverse osmosis system performs startup cleaning every time it is turned on. The startup cleaning time is controlled at about 30 seconds (the time is adjustable). When the reverse osmosis system has been running for a period of time, it will be cleaned regularly (the time is adjustable).
5. When the pretreatment pressure does not reach 2kg, the reverse osmosis host is protected by low pressure. Single-stage reverse osmosis water treatment equipment 1T/H, water output 1T per hour.
Chloride Ion Removal
Chloride is a naturally occurring dissolved ion that can be present in groundwater, surface water, seawater, industrial wastewater, and other water sources. Excessive chloride concentration can contribute to corrosion of metal equipment, pipelines, heat exchangers, boilers, and other water-contact components.
RO Reverse Osmosis is one of the most widely used technologies for reducing chloride ions from water. During reverse osmosis, pressure forces feed water through a semipermeable membrane while many dissolved ions, including chloride, are rejected and concentrated in the reject stream.
Depending on chloride concentration and required water quality, the system can use single-pass RO, double-pass RO, or additional polishing treatment.
Scale Removal and Scale Prevention
Scale formation is a common problem in boilers, heat exchangers, cooling systems, pipelines, RO membranes, and industrial water equipment. Hardness minerals such as calcium and magnesium can precipitate when water conditions change, creating deposits on heat-transfer surfaces and membrane elements.
Scale Removal can involve mechanical cleaning, chemical cleaning, acid cleaning, membrane cleaning, or other methods depending on the type of deposit.
For continuous operation, scale prevention is generally preferable to repeated scale removal. Water softening, antiscalant dosing, effective pretreatment, and RO membrane treatment can help control scaling before it becomes a serious operational problem.
RO Reverse Osmosis System
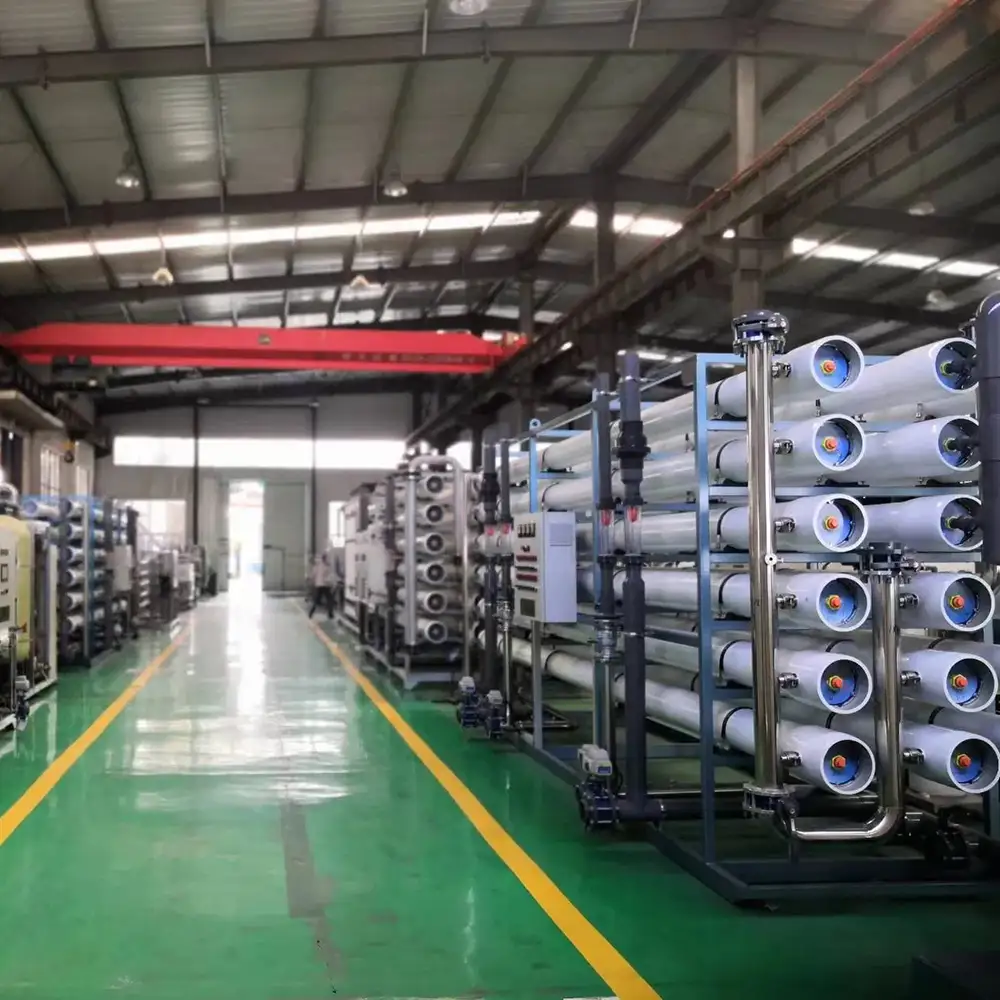
The RO Reverse Osmosis System is the core purification technology for many industrial water treatment applications. It uses high-pressure pumps and semipermeable membranes to reduce dissolved salts, chloride ions, minerals, total dissolved solids, and other contaminants.
Before entering the RO membrane, feed water may pass through multimedia filters, activated carbon filters, softeners, cartridge filters, or other pretreatment equipment.
Effective pretreatment helps reduce suspended solids, chlorine, hardness, and other substances that may cause membrane fouling or scaling.
The RO system can be configured according to feed-water quality, required capacity, recovery rate, operating pressure, and final water-quality requirements.
Boiler Water Treatment
Boiler systems require carefully controlled water quality because dissolved minerals and suspended contaminants can cause scale, corrosion, carryover, and reduced heat-transfer efficiency.
Boiler Water Treatment commonly includes pretreatment, softening, filtration, reverse osmosis, demineralization, chemical dosing, and other processes depending on boiler pressure and water-quality requirements.
RO water treatment can be used to produce high-quality boiler feed water by reducing dissolved salts and other contaminants before water enters the boiler system.
Proper feed-water treatment helps protect boiler components, reduce deposits, improve heat-transfer efficiency, and support stable boiler operation.
Sewage Treatment Plant
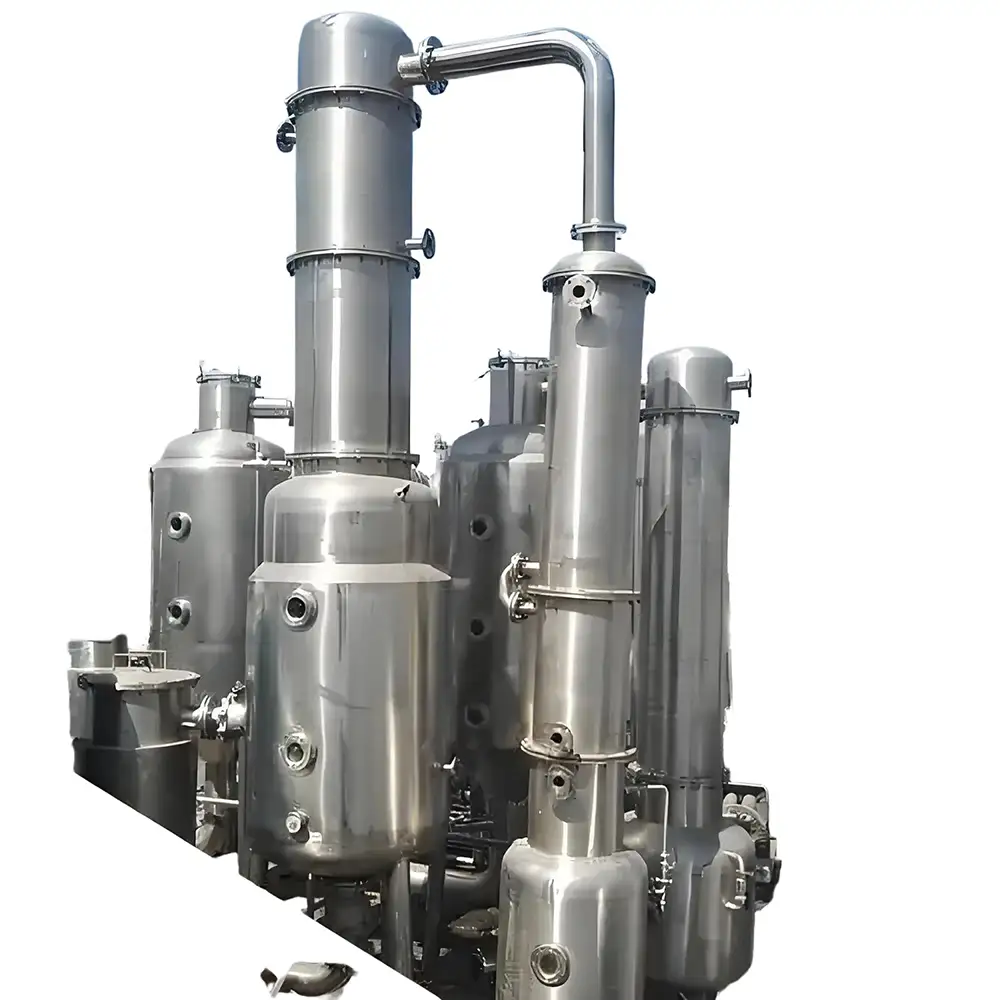
A Sewage Treatment Plant is designed to remove physical, biological, and chemical contaminants from municipal or industrial wastewater before discharge, reuse, or further treatment.
Typical sewage treatment processes may include screening, grit removal, primary clarification, biological treatment, secondary sedimentation, filtration, disinfection, sludge treatment, and advanced water purification.
For industrial wastewater, additional processes may be required to address high COD, BOD, suspended solids, ammonia, nitrogen, phosphorus, oil, heavy metals, salts, or other site-specific contaminants.
RO treatment can be installed as an advanced polishing stage when treated wastewater needs to meet higher water-quality requirements for reuse or specialized industrial applications.
Integrated Industrial Water Treatment
A complete water treatment project may combine several technologies rather than relying on one process.
A typical treatment sequence can include:
Raw water intake and screening
Multimedia filtration
Activated carbon filtration
Water softening or antiscalant dosing
Cartridge filtration
RO Reverse Osmosis
Purified-water storage
UV or other disinfection
Industrial wastewater treatment
Advanced filtration or water reuse
The exact process depends on the source water and target water quality.
Efficient Membrane Filtration
RO membrane performance depends on feed-water pressure, temperature, membrane condition, pretreatment, recovery rate, and contaminant concentration.
Properly designed pretreatment can reduce fouling and scaling, helping maintain stable permeate flow and water quality. Automatic monitoring of conductivity, pressure, flow rate, and other parameters can help operators identify changes in system performance.
For high-salinity or difficult feed water, specialized membrane configurations and multiple treatment stages may be used.
Automatic Operation and Control
Modern industrial water treatment plants can be equipped with programmable logic controllers, automatic valves, pressure sensors, flow meters, conductivity meters, water-level sensors, and chemical dosing systems.
Automatic controls can manage pumps, filtration cycles, backwashing, regeneration, RO operation, tank filling, and system shutdown.
Monitoring important parameters allows operators to identify abnormal conditions and perform preventive maintenance before problems become severe.
Water Recovery and Reuse
Water reuse is becoming increasingly important for industrial facilities seeking to reduce freshwater consumption and wastewater discharge.
Treated wastewater can potentially be reused for cooling-tower makeup, equipment washing, process water, boiler pretreatment, irrigation, or other non-potable applications, depending on the treatment process and required water quality.
RO treatment can provide an additional purification stage for applications requiring reduced dissolved solids and improved water quality.
Applications
These water treatment technologies can be applied to:
Boiler Feed Water Treatment
Industrial Process Water Treatment
Industrial Wastewater Treatment
Sewage Treatment Plants
Chemical Manufacturing
Food and Beverage Processing
Pharmaceutical Production
Power Plant Water Treatment
Cooling Tower Water Treatment
Electronics Manufacturing
Mining Wastewater Treatment
Industrial Water Reuse
High-TDS Wastewater Treatment
Brackish Water Treatment
Why Choose Us?
Selecting the right water treatment system requires careful evaluation of raw-water chemistry, contaminant concentration, flow rate, treatment capacity, water-quality targets, and operating conditions.
Our solutions focus on:
Chloride ion reduction
Scale removal and prevention
Advanced RO reverse osmosis treatment
Boiler feed-water purification
Industrial sewage and wastewater treatment
Multi-stage filtration and pretreatment
Automatic control and monitoring
Efficient membrane protection
Water recovery and reuse
Flexible treatment plant configurations
Each system can be configured around the actual water-quality analysis and application requirements.
FAQs
1. How can chloride ions be removed from water?
Reverse osmosis is one of the most effective commonly used technologies for reducing chloride ions. Other technologies may be selected depending on chloride concentration and final water-quality requirements.
2. Can RO remove chloride from boiler feed water?
Yes. RO can significantly reduce chloride and other dissolved salts before water enters a boiler treatment system.
3. What causes scale in industrial water systems?
Scale is commonly caused by calcium, magnesium, silica, and other dissolved substances that precipitate under certain temperature and chemical conditions.
4. How can RO membrane scaling be prevented?
Water softening, antiscalant dosing, effective pretreatment, proper recovery control, and routine membrane maintenance can help prevent or reduce scaling.
5. What is a sewage treatment plant?
A sewage treatment plant removes physical, biological, and chemical contaminants from wastewater so the treated water can be discharged or reused according to applicable requirements.
6. Can RO be used after sewage treatment?
Yes. RO can serve as an advanced treatment or polishing stage when treated wastewater needs further reduction of dissolved salts and other contaminants for reuse.
7. What is boiler water treatment?
Boiler water treatment is a combination of processes designed to control hardness, dissolved salts, suspended solids, corrosion, and scale in boiler feed and boiler water.
8. Can one plant handle both wastewater and RO treatment?
Yes. A centralized treatment system can integrate wastewater treatment, filtration, RO, disinfection, and water reuse processes according to project requirements.
9. How often should RO membranes be cleaned?
Cleaning frequency depends on feed-water quality, pretreatment, operating pressure, flow changes, and membrane fouling or scaling.
10. Can the system be designed for industrial water reuse?
Yes. Treatment processes can be configured to recover and reuse water for suitable industrial applications, helping reduce freshwater consumption and wastewater discharge.
Prev:
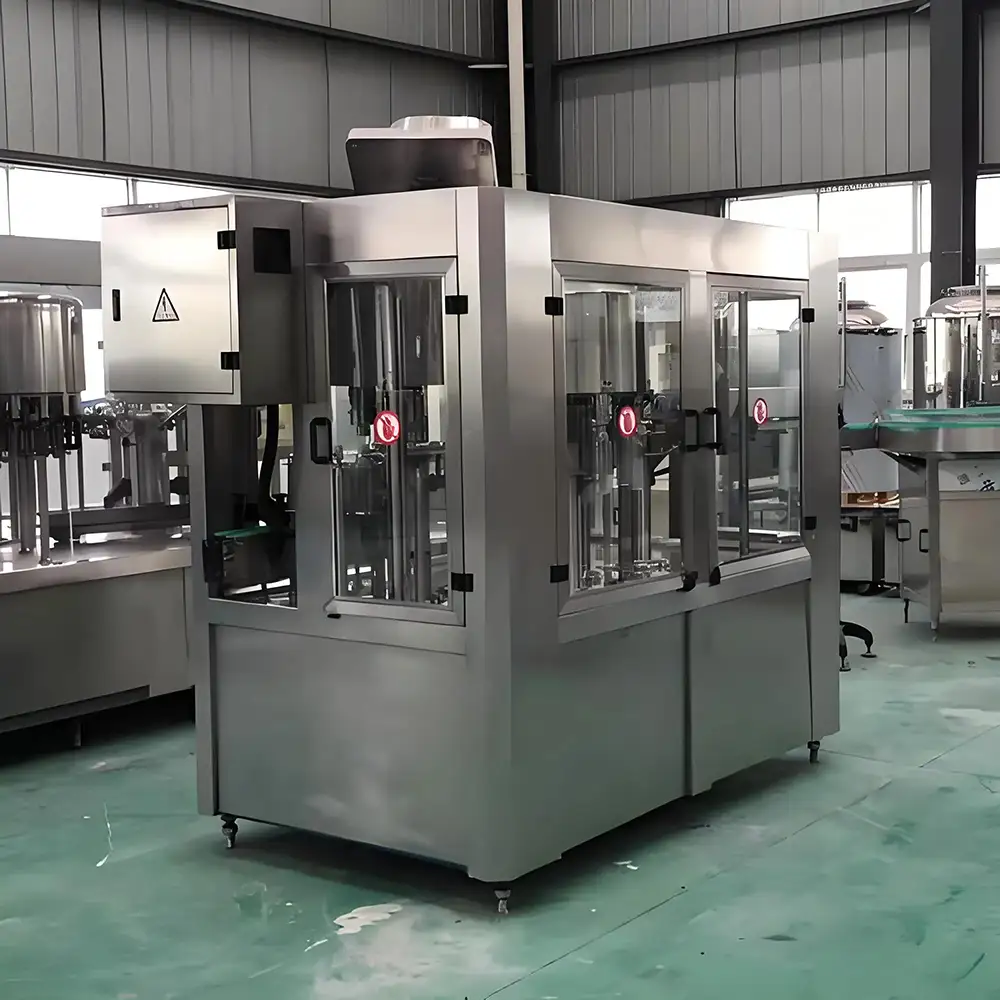
Energy-Saving and Environmentally Friendly Barreled Water + Bottle Water Dual-Line Equipment
Next:Sorry, no information
TAG:
Industrial Wastewater Treatment,
Sewage Treatment Plant,
Industrial Sewage Treatment,
Wastewater Treatment Equipment,
Wastewater Treatment Plant,
Cooling Tower Water Treatment,
High Purity Water Treatment,
Reverse Osmosis Water Treatment,
Industrial Wastewater Purification,
Industrial Water Treatment Plant,
Wastewater Treatment System,
Industrial Water Treatment,
Industrial Water Recycling,
Water Treatment Plant,
High TDS Wastewater Treatment,
Industrial Water Purification,
Industrial RO Water Treatment,
RO Water Treatment Plant,
Water Reuse System,
Industrial Reverse Osmosis System,
Industrial RO System,
Industrial Water Reuse,
Industrial Effluent Treatment,
Water Recycling System,
Process Water Treatment,
Industrial Water Filtration,
Industrial RO Water Purification,
RO Membrane System,
RO Membrane Filtration,
RO Membrane Water Treatment,
Related Category:
Chloride Ion Removal,Scale Removal,Sewage Treatment Plant,RO Reverse Osmosis System,Boiler Water Treatment China, suppliers, manufacturers, factory, customized, wholesale, quotation, made in China