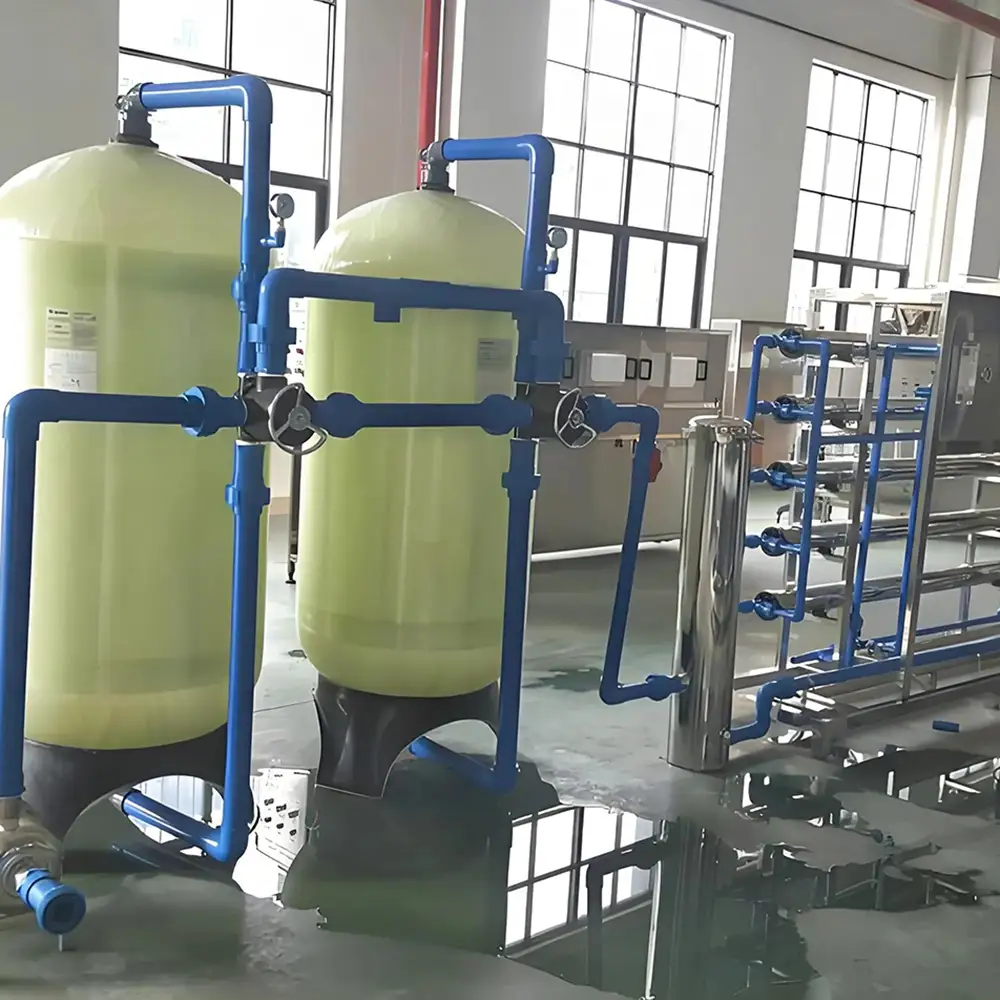
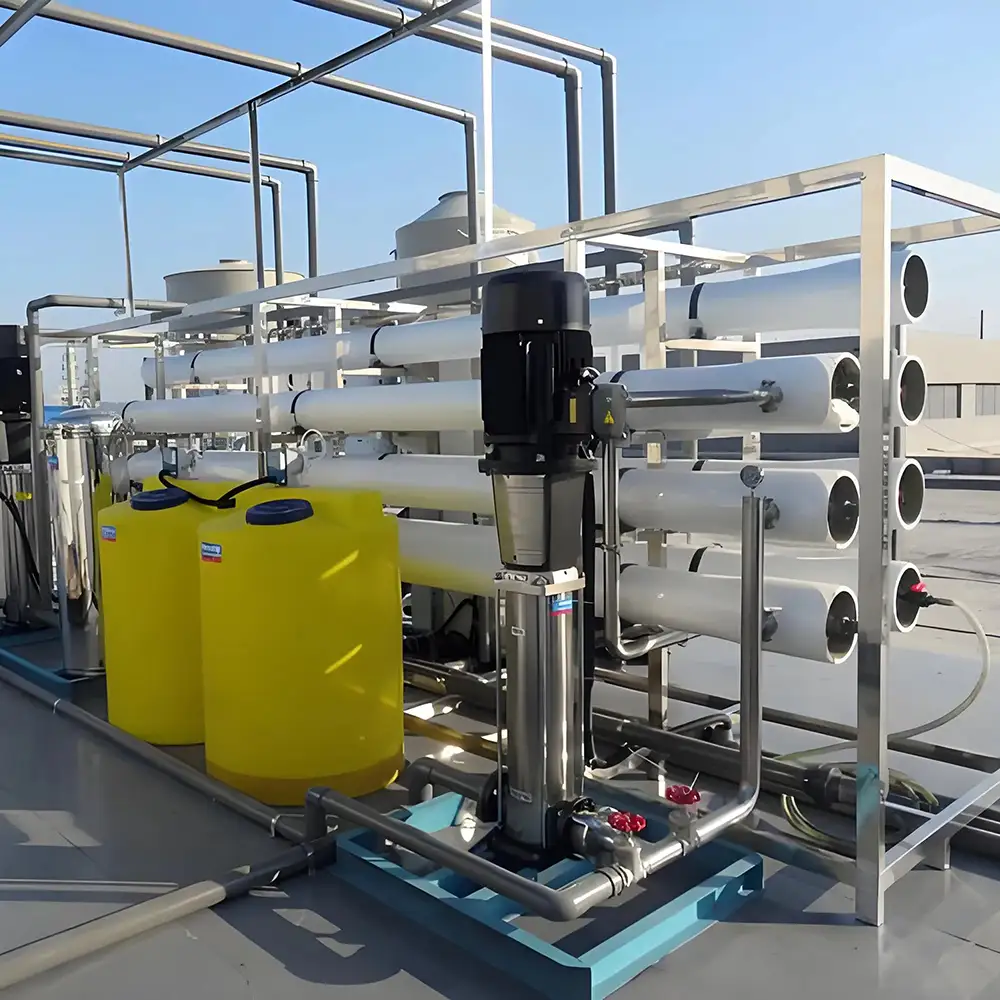
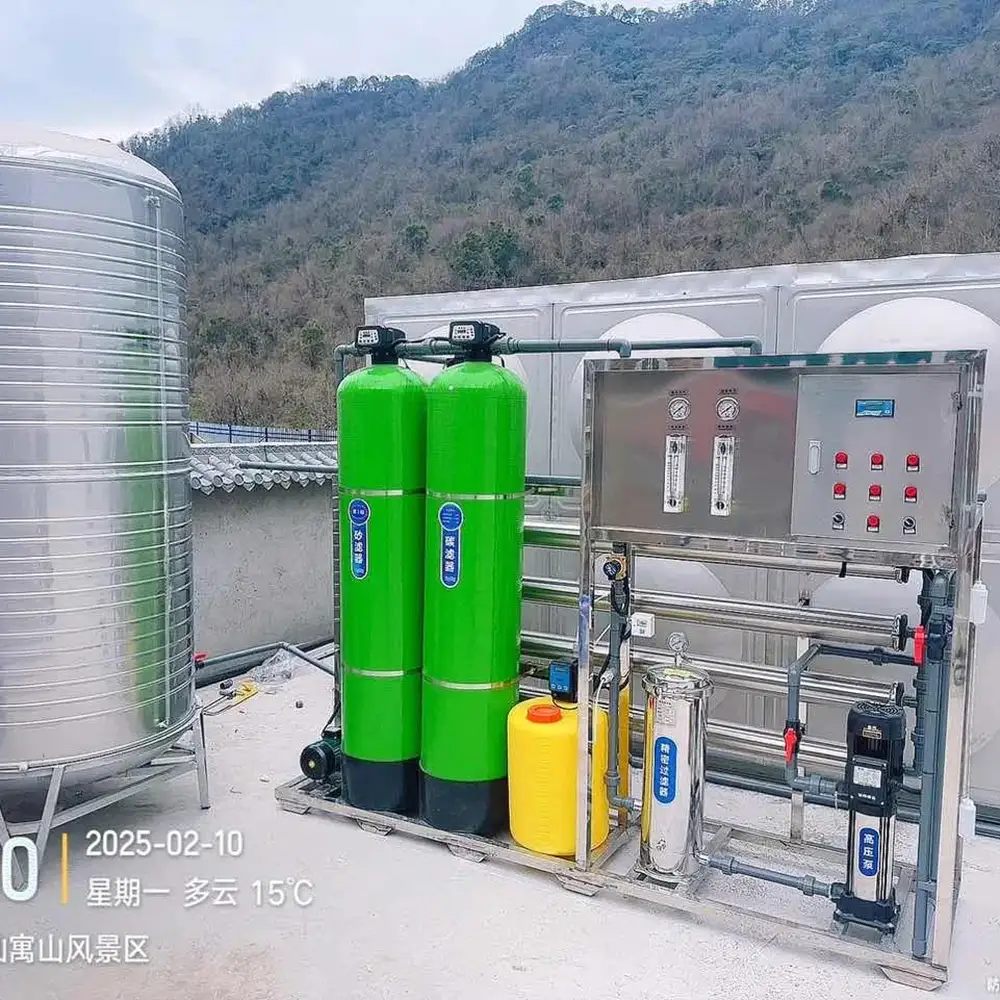
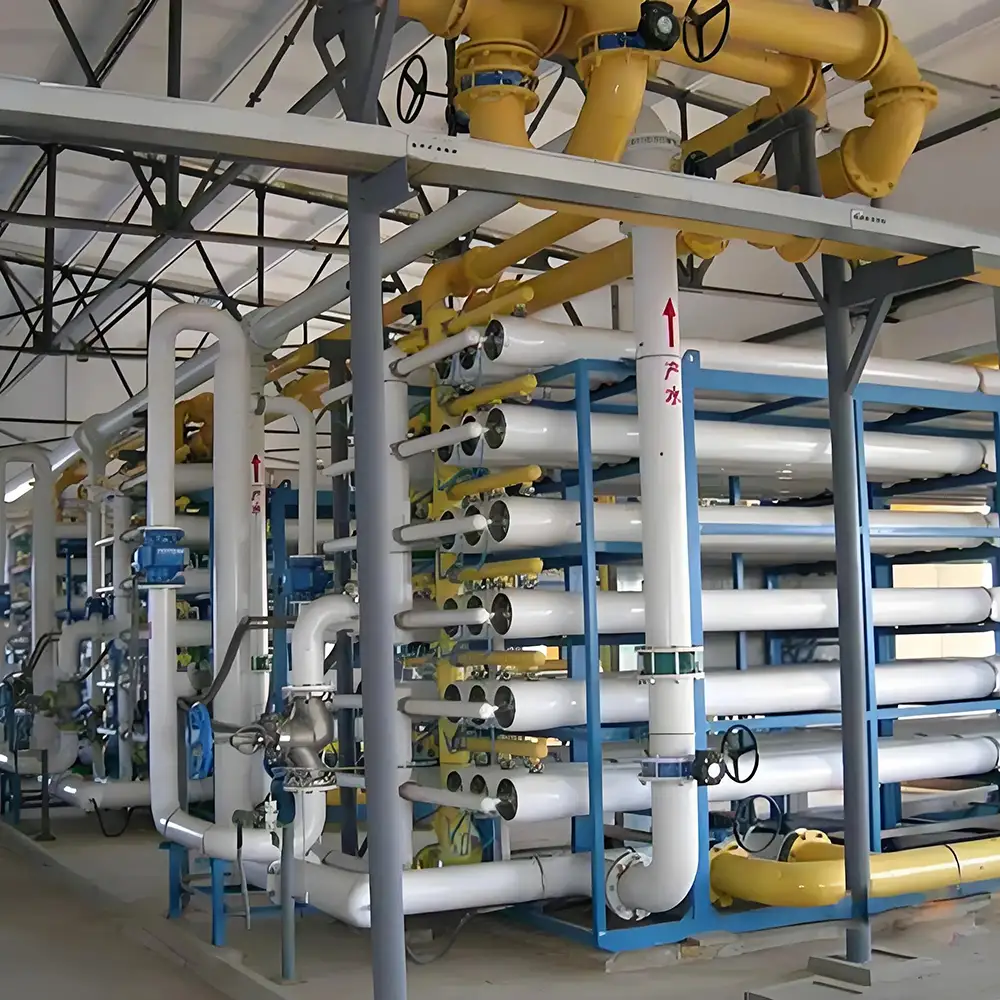
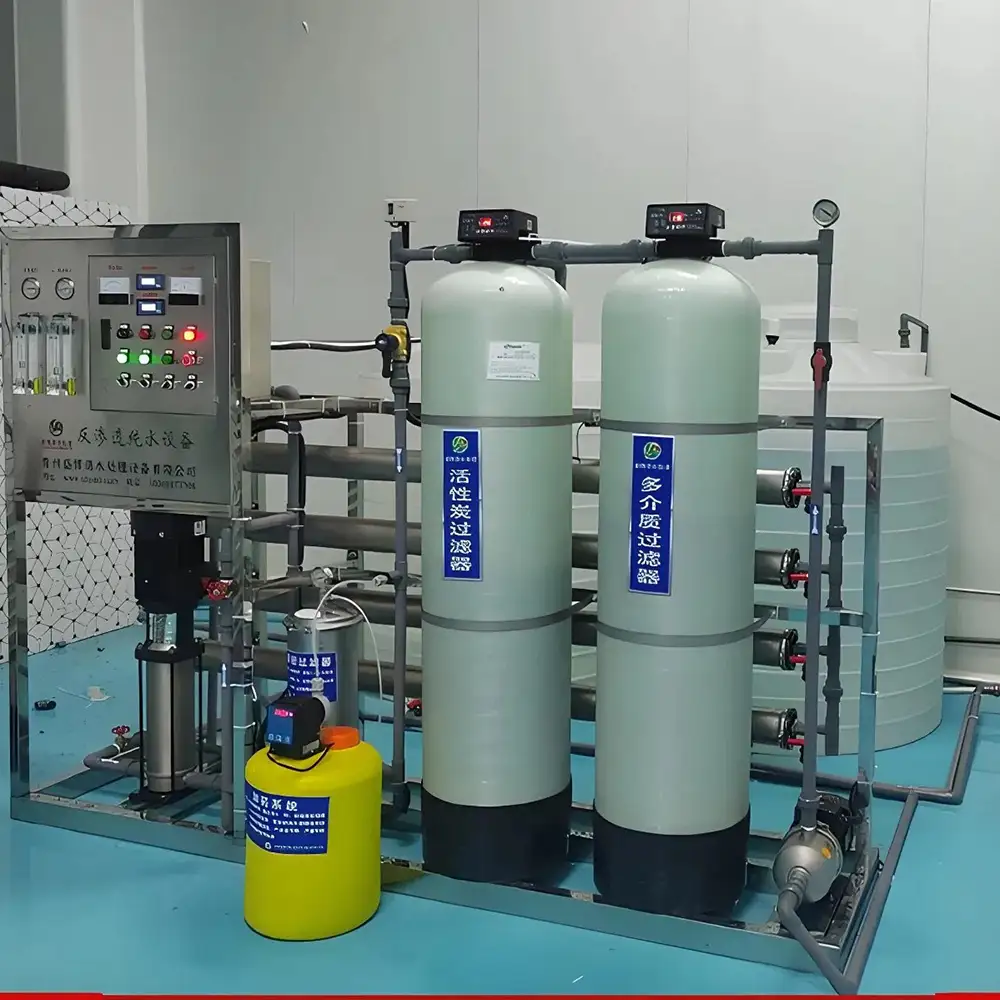
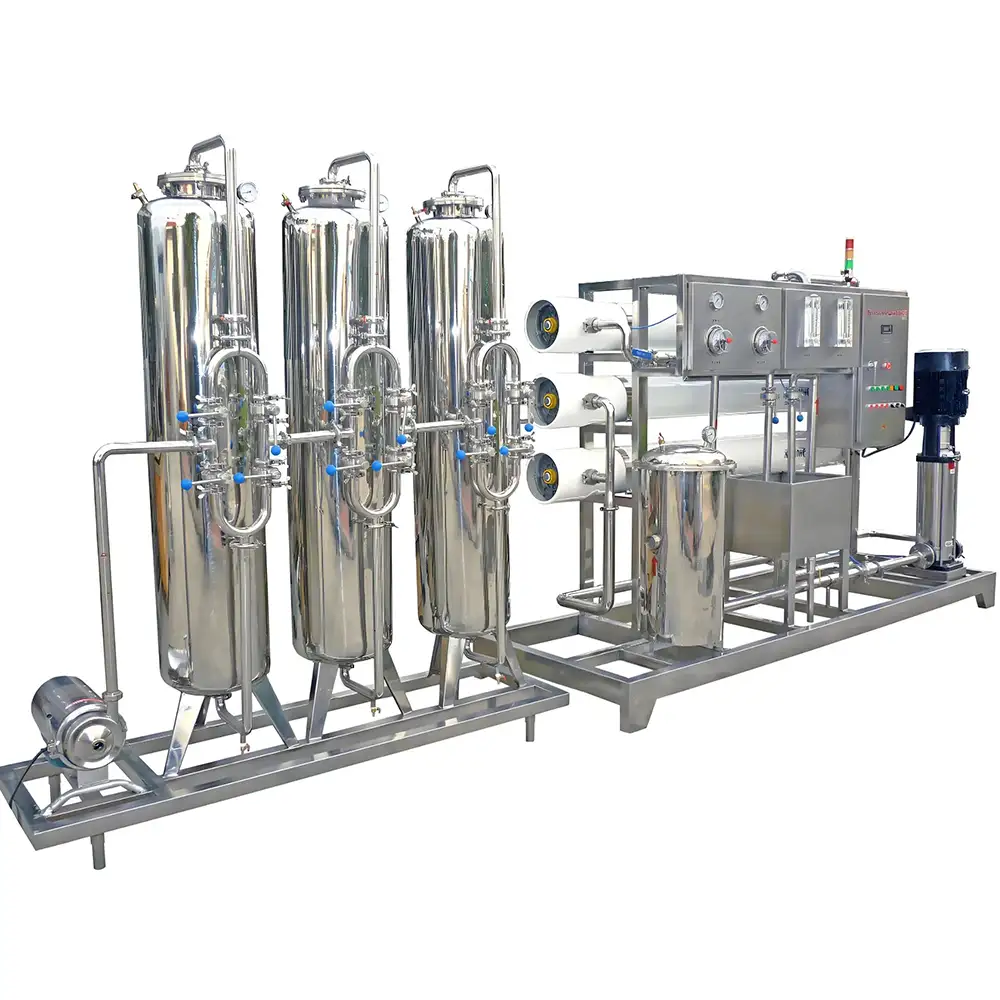
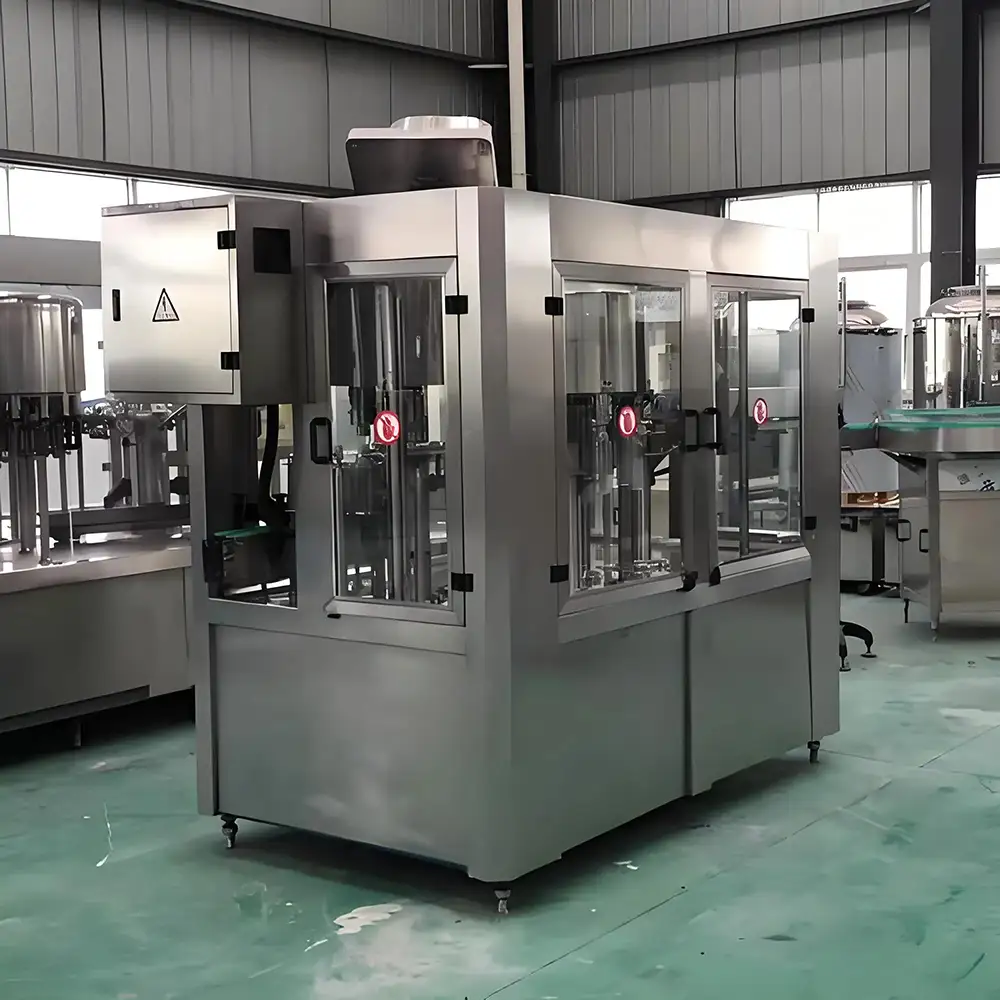
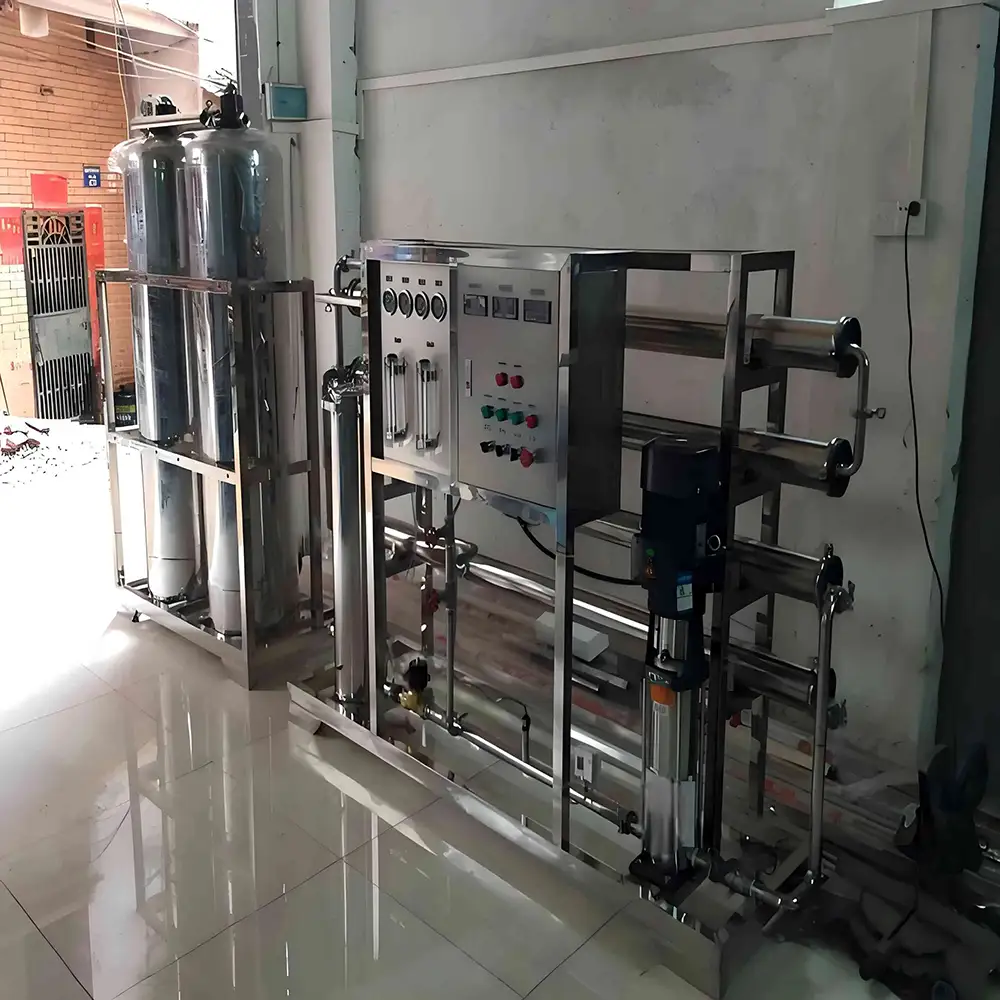
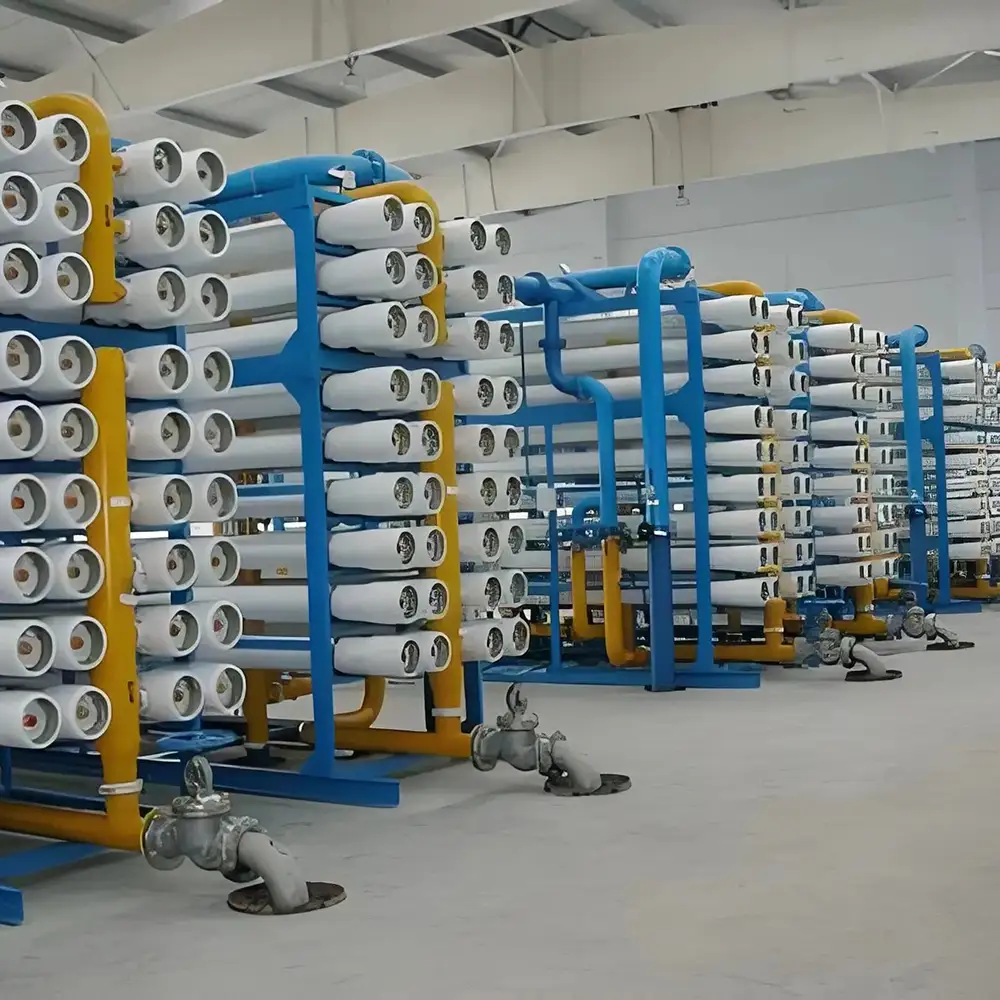
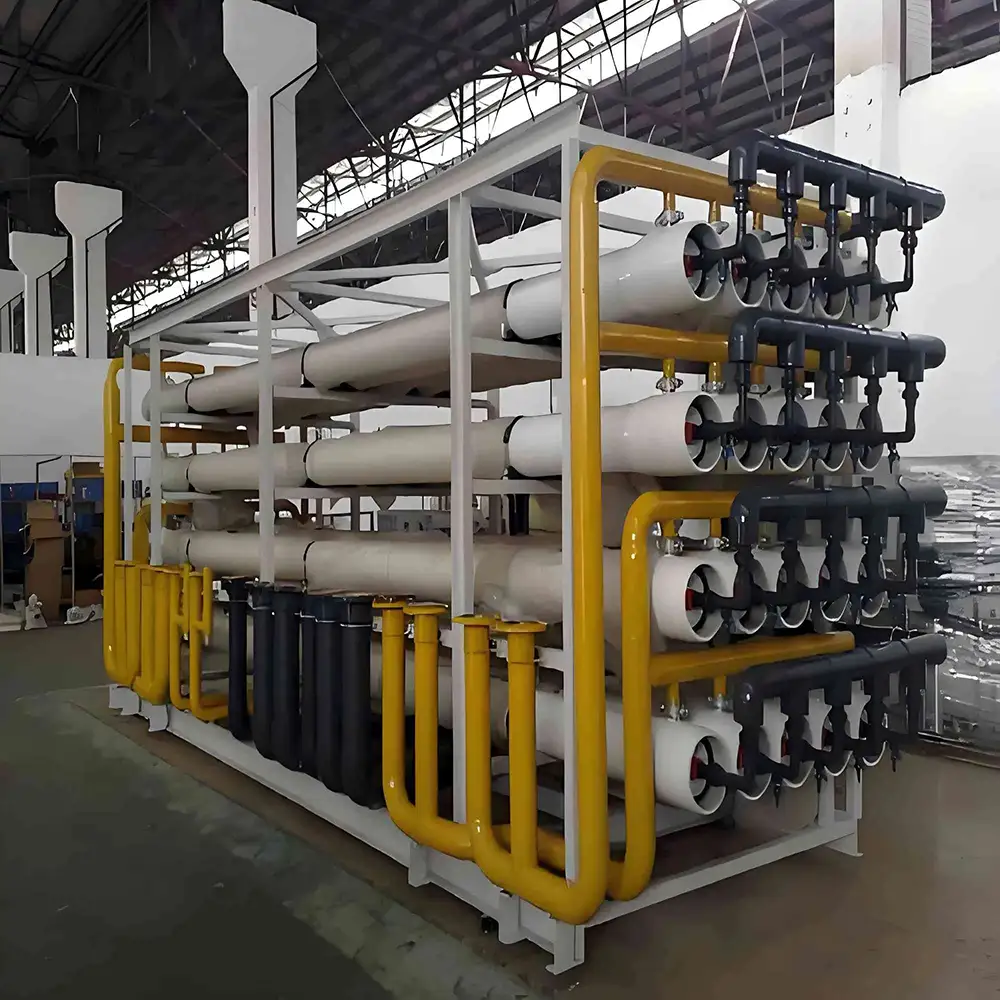
Supermarket Water Purification Reverse Osmosis Treatment Equipment
Supermarket Water Purification Reverse Osmosis Treatment Equipment is designed to provide reliable and efficient water purification for supermarkets, food retail stores, commercial facilities, beverage preparation areas, and other businesses that require a consistent supply of high-quality purified water. By combining advanced pretreatment, precision filtration, and reverse osmosis membrane technology, the system can reduce dissolved solids, suspended particles, chlorine, unpleasant odors, microorganisms, and other unwanted contaminants from incoming water.
Water quality is important in modern supermarkets. Purified water may be used for food preparation, beverage production, ice making, cleaning, fresh food processing, bakery operations, deli departments, coffee stations, and other applications. An appropriately designed reverse osmosis water treatment system can help improve water quality while reducing dependence on bottled water and providing a centralized purification solution.
|
Model NO. |
wzss |
Handling method |
Physical Treatment |
|
Usage |
Industrial, Home, Agriculture, Hospital, Urban |
Trademark |
Wanze Prosperity |
|
Types |
Package, Compact, Small, Mini |
Applications |
Industrial, Municipal, Domestic, Medical, Ship |
|
Transport Package |
Container Standard Packing |
Features |
Remove Cod BOD |
|
Material |
Remove Cod BOD |
Function |
Removing Escherichia coli, harmful bacteria |
|
Voltage |
220V/ 380V/ Customerized |
Installation Type |
Underground / Onground |
|
Colour |
white |
Use for |
Mineral, Printing, Chemical, Dyeing, Starch |
|
Production Capacity |
2000 Sets/Year |
Origin |
China |
Efficient Reverse Osmosis Water Purification
Reverse osmosis is a membrane-based purification technology that uses pressure to force water through a semipermeable membrane. The membrane allows water molecules to pass while rejecting many dissolved salts, minerals, heavy metals, organic contaminants, and other impurities.
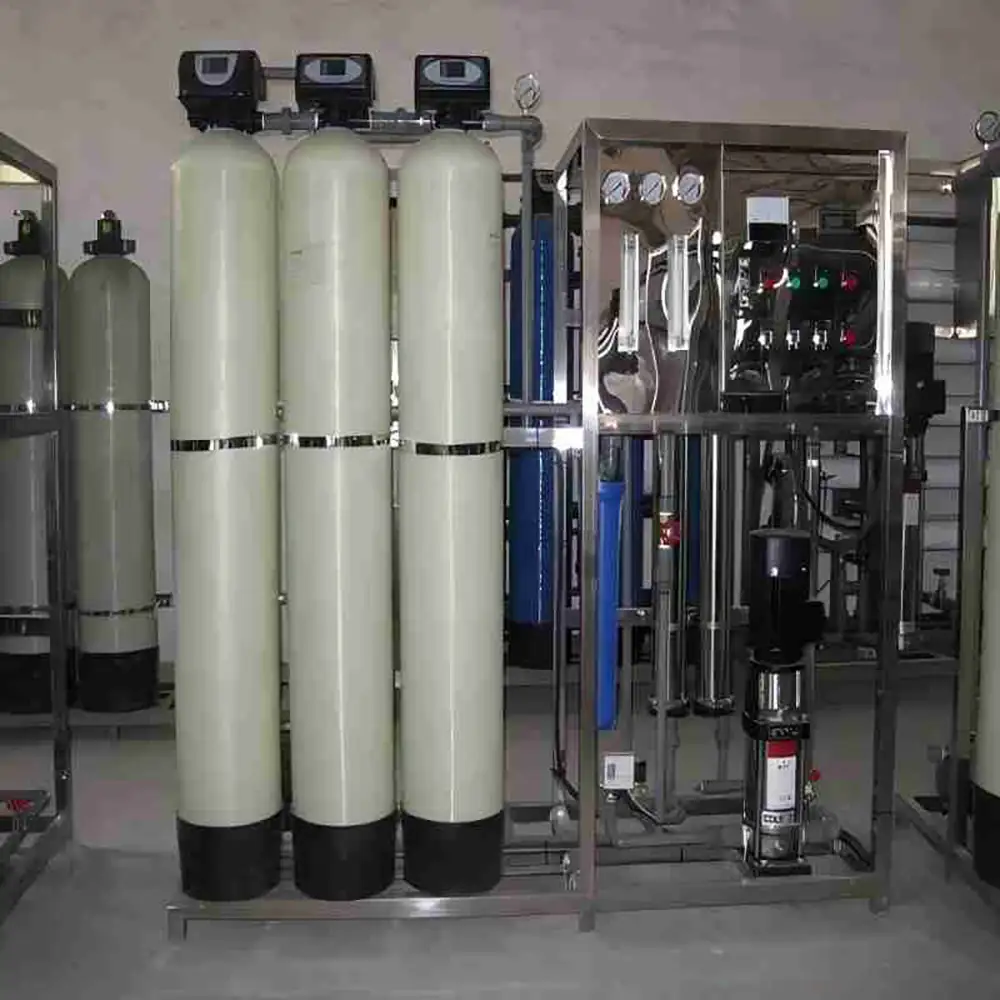
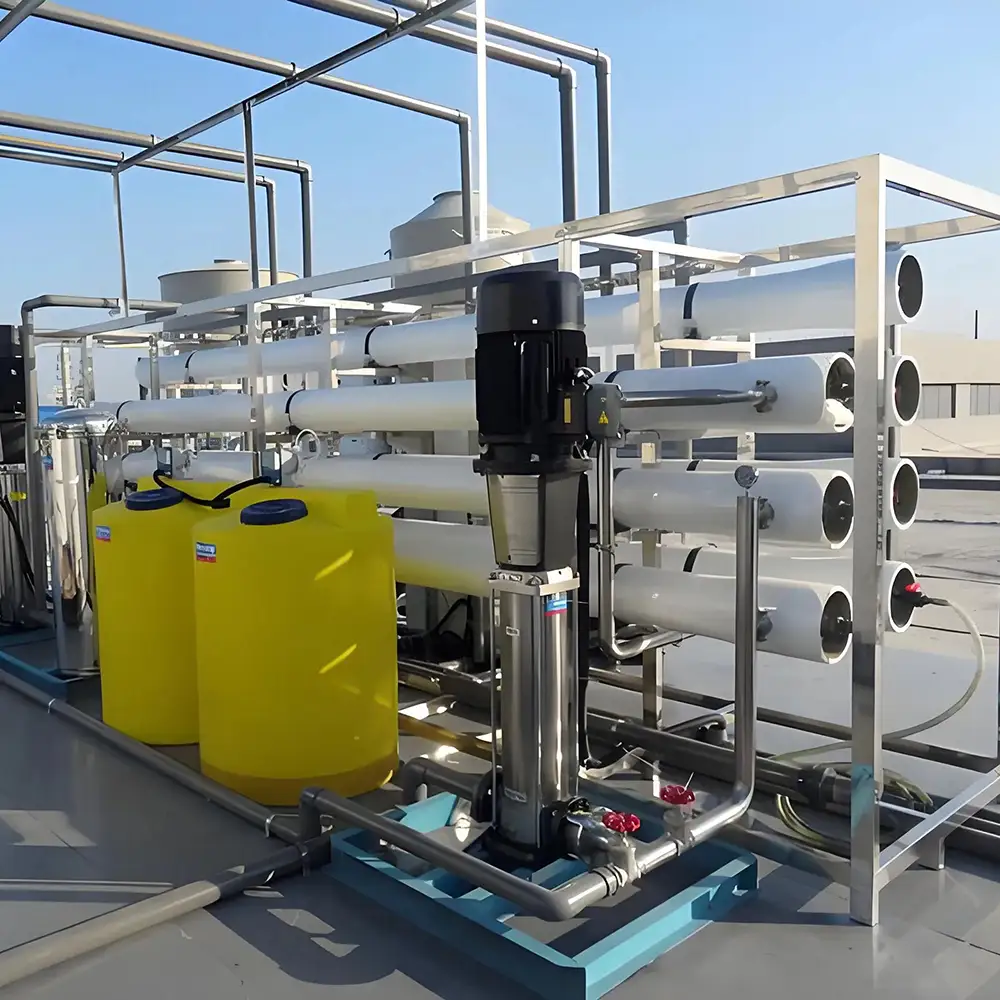
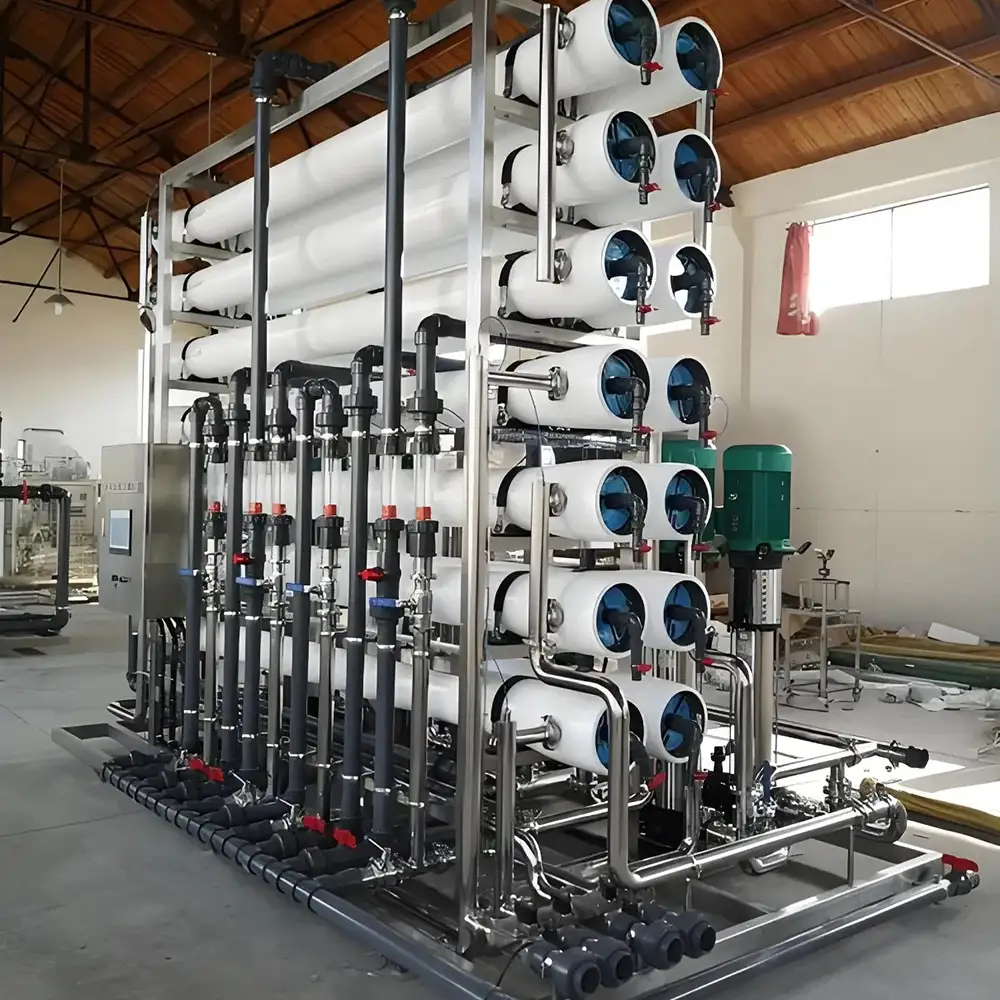
A supermarket RO water treatment system normally includes multiple treatment stages. Depending on the quality of the source water and the required final water quality, the system may include a raw water tank, feed pump, multimedia filter, activated carbon filter, cartridge filter, high-pressure pump, RO membrane housing, reverse osmosis membranes, control system, and purified water storage tank.
Pretreatment is particularly important because it protects the RO membrane from excessive fouling and scaling. Multimedia filtration can reduce suspended solids, while activated carbon filtration can help remove chlorine, organic compounds, odors, and unpleasant tastes. Cartridge filtration provides additional fine-particle protection before water enters the RO membrane system.
Designed for Supermarket Applications
Supermarkets have different water consumption patterns depending on their size and operations. A small retail store may require a compact commercial RO system, while a large supermarket or food distribution facility may need a higher-capacity industrial water purification plant.
The equipment can be configured according to required flow rate, raw water quality, operating pressure, water recovery rate, installation space, and final water quality requirements. Modular designs can also make installation, maintenance, and future capacity expansion easier.
Typical applications include supermarket drinking water systems, food preparation, bakery water supply, beverage stations, coffee shops located inside supermarkets, ice machines, fresh produce processing, meat and seafood departments, deli operations, cleaning water, and other commercial water applications.
Stable Water Quality and Reliable Operation
Consistent water quality is one of the major advantages of a centralized reverse osmosis treatment system. Instead of relying entirely on packaged bottled water, businesses can produce purified water on demand.
The RO membrane removes a broad range of dissolved contaminants, helping reduce total dissolved solids and improving the taste and appearance of treated water. When combined with appropriate pretreatment and post-treatment equipment, the system can provide stable water quality for demanding commercial applications.
Depending on the project requirements, additional technologies such as ultraviolet sterilization, ozone treatment, remineralization, pH adjustment, or final polishing filtration can be integrated into the purification line.
Energy-Efficient Commercial Water Treatment
Modern reverse osmosis systems are designed to balance purification performance, water recovery, operating pressure, and energy consumption. High-efficiency pumps, optimized membrane configurations, automatic controls, and suitable pretreatment can help reduce unnecessary operating costs.
The system can also be equipped with automatic flushing and pressure monitoring functions to support membrane performance. Proper maintenance of filters and membranes is essential for maintaining stable production capacity and extending equipment service life.
For supermarkets with high daily water consumption, centralized RO purification can provide a practical alternative to purchasing large quantities of bottled water. It can reduce packaging waste, simplify water management, and provide purified water closer to the point of use.
Flexible Configuration and Installation
Supermarket Water Purification Reverse Osmosis Treatment Equipment can be customized according to the customer's water source and application requirements. Systems can be supplied in different capacities and configurations for municipal water, well water, or other suitable feedwater sources.
Compact skid-mounted designs are suitable for facilities with limited installation space. Larger systems can be integrated with pretreatment tanks, water storage tanks, automatic control cabinets, booster pumps, and distribution pipelines.
For projects requiring continuous water supply, multiple RO units can also be configured in parallel. This arrangement can improve operational flexibility and provide additional capacity during peak demand periods.
Easy Operation and Maintenance
A properly configured RO system is designed for straightforward operation and maintenance. Automatic control systems can monitor important operating parameters such as inlet pressure, RO pressure, flow rate, conductivity, and water level.
Routine maintenance normally includes replacing pretreatment filter media when required, changing cartridge filters, checking pumps and valves, cleaning or replacing RO membranes when necessary, and monitoring treated water quality.
Regular maintenance helps prevent membrane fouling and scaling while maintaining stable water production. The actual maintenance schedule depends on raw water quality, operating hours, pretreatment performance, and system capacity.
Why Choose Us?
Choosing the right supermarket water purification system requires more than selecting an RO membrane. The complete treatment process should be designed around the source water, required capacity, target water quality, available installation space, and operating conditions.
Our Supermarket Water Purification Reverse Osmosis Treatment Equipment can be configured as a complete water treatment solution with pretreatment, RO purification, storage, control, and optional post-treatment functions. This approach helps ensure that every major stage of the purification process works together efficiently.
We focus on practical equipment configuration, stable operation, convenient maintenance, and long-term performance. Whether the application is a supermarket beverage station, food processing area, commercial kitchen, bakery, ice-making facility, or large retail complex, the system can be designed around actual water consumption requirements.
Frequently Asked Questions
1. What does a supermarket reverse osmosis system remove?
A reverse osmosis system can reduce many dissolved salts, total dissolved solids, heavy metals, suspended contaminants, and other impurities. Actual removal performance depends on the membrane, feedwater quality, operating conditions, and system configuration.
2. Can this equipment be used for drinking water?
Yes. An appropriately designed and maintained RO system can be used for drinking water applications when the complete system meets the applicable water quality and regulatory requirements.
3. What pretreatment does an RO system need?
Common pretreatment includes multimedia filtration, activated carbon filtration, and cartridge filtration. The exact configuration depends on the raw water analysis.
4. How often should RO membranes be replaced?
There is no universal replacement interval. Membrane life depends on feedwater quality, pretreatment, operating conditions, cleaning frequency, and maintenance. Membrane performance should be monitored regularly.
5. Can the system handle high supermarket water demand?
Yes. RO systems can be designed with different capacities, and multiple membrane units can be installed in parallel for higher production requirements.
6. Can UV sterilization be added?
Yes. UV sterilization can be integrated as an additional treatment stage when microbial control is required.
7. Is the system fully automatic?
The equipment can be configured with automatic controls for functions such as pump operation, flushing, water level control, pressure monitoring, and system protection.
8. Can the equipment be installed in a limited space?
Yes. Compact and skid-mounted configurations can be designed for locations where installation space is limited.
9. What information is needed to select an RO system?
Important information includes raw water source, water analysis, required water production capacity, operating hours, target water quality, installation conditions, and intended application.
10. Can the system be used for food and beverage applications?
Yes. With appropriate materials, pretreatment, post-treatment, sanitation procedures, and compliance with applicable requirements, RO water treatment can support many food and beverage applications.
Prev:
Water Purification Reverse Osmosis Membrane Treatment Equipment Sewage Treatment Plant
Next:
Water Purifier/Advanced Water Filtration Equipment /RO/ Drinking Water
TAG:
Industrial Water Treatment,
Water Filtration System,
Water Treatment Plant,
Water Treatment Equipment,
Membrane Water Treatment,
Industrial Water Purification,
Water Purification System,
Industrial RO Water Treatment,
RO Water Treatment Plant,
Commercial RO System,
Drinking Water Purification,
RO Membrane System,
RO Filtration System,
Reverse Osmosis Water Purification,
Reverse Osmosis System,
Water Purification Plant,
RO Water Purification Equipment,
Commercial Water Filtration,
Commercial Water Treatment,
Commercial Water Purification System,
Commercial RO Water Treatment,
Reverse Osmosis Treatment Equipment,
Supermarket Water Purification,
Supermarket Reverse Osmosis System,
Supermarket Water Treatment,
Related Category:
Supermarket Water Purification Equipment,Supermarket Reverse Osmosis System,Commercial RO Water Treatment Equipment China, suppliers, manufacturers, factory, customized, wholesale, quotation, made in China